What is A Vacuum Pump?
A vacuum pump is a device used to remove gas molecules from an enclosed space, creating a partial vacuum. It operates by mechanically transferring gas molecules from a low-pressure region (inlet) to a high-pressure region (outlet).
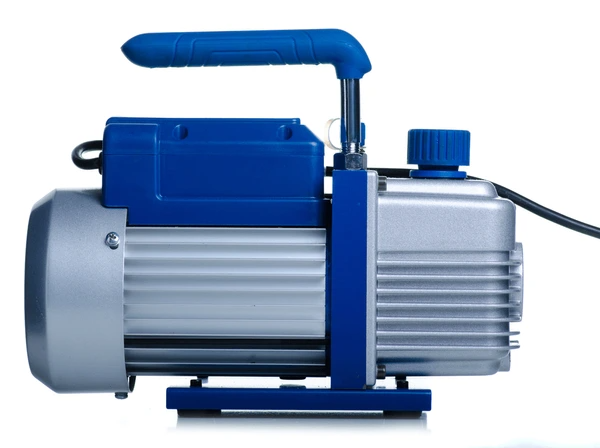
How Does A Vacuum Pump Work?
Vacuum pumps create a partial vacuum by removing gas molecules from a sealed volume, allowing the remaining molecules to be evacuated. The main principles are:
- Positive displacement pumps (rotary vane, scroll, diaphragm) trap gas and force it out through an exhaust.
- Momentum transfer pumps (turbomolecular, molecular drag) use high-speed rotating blades to impart momentum to gas molecules towards the exhaust.
- Entrapment pumps (cryopumps, sputter-ion pumps) condense or ionize gas molecules onto cold surfaces or titanium liners
Types of Vacuum Pumps
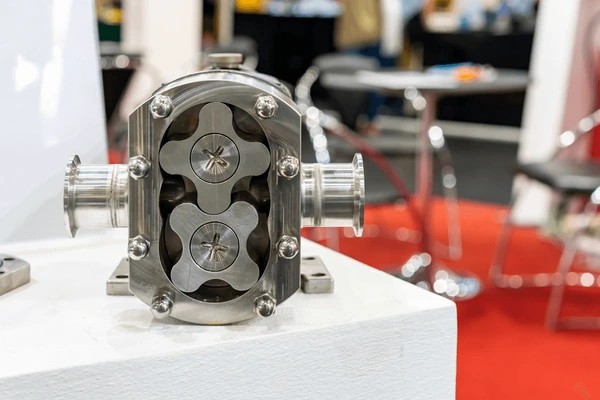
Positive Displacement Vacuum Pumps
- Rotary Vane Pumps: Consist of a rotor with vanes that rotate eccentrically in a cavity. Suitable for rough vacuum applications down to 10^-3 mbar. Used in chemical, pharmaceutical, and food processing industries.
- Scroll Pumps: Employ two spiral-shaped scrolls that orbit eccentrically to pump gas. Provide oil-free, dry vacuum down to 10^-2 mbar. Used in semiconductor, analytical, and R&D applications.
- Liquid Ring Pumps: Utilize a liquid ring to create a seal between the rotor and casing. Suitable for handling vapors, corrosive gases, and particulates down to 25 mbar. Widely used in chemical, petrochemical, and power industries.
Kinetic Vacuum Pumps
- Molecular Drag Pumps: Employ a high-speed rotor to transfer momentum to gas molecules. Achieve high vacuum levels down to 10^-8 mbar. Used in analytical instruments, particle accelerators, and thin-film deposition systems.
- Turbomolecular Pumps: Consist of a high-speed rotor with angled blades that impart momentum to gas molecules. Provide clean, oil-free vacuum down to 10^-10 mbar. Essential in semiconductor, optics, and surface science applications.
Entrapment Vacuum Pumps
- Cryopumps: Trap gases by condensation on a cryogenically cooled surface. Achieve ultra-high vacuum levels down to 10^-12 mbar. Used in particle accelerators, space simulation chambers, and surface analysis instruments.
- Ion Pumps: Ionize and trap gas molecules using high-voltage electrodes. Provide clean, vibration-free vacuum down to 10^-11 mbar. Used in mass spectrometers, particle accelerators, and vacuum-insulated systems.
Hybrid and Specialized Vacuum Pumps
- Combination Pumps: Integrate multiple pumping mechanisms in a single unit, such as a roots pump and a molecular drag pump. Provide high pumping speed and wide operating range.
- Dry Scroll Pumps: Scroll pumps that operate without lubricating fluids. Suitable for clean, dry vacuum applications in semiconductor, analytical, and R&D industries.
- Vacuum Blowers: Positive displacement pumps for rough vacuum applications down to 0.1 mbar. Used in vacuum packaging, vacuum forming, and vacuum coating processes.
Benefits of Vacuum Pumps
Enabling Vacuum Environments
Vacuum pumps are essential for creating and maintaining vacuum environments, which are crucial for numerous industrial and scientific applications. They enable processes that require low-pressure conditions, such as:
- Semiconductor manufacturing
- Vacuum deposition for thin-film coatings
- Electron microscopy and surface analysis
- Vacuum distillation and drying
Improved Process Efficiency and Quality
By removing gases and contaminants from the process environment, vacuum pumps contribute to:
- Increased product purity and quality
- Enhanced reaction rates and yields in chemical processes
- Reduced risk of oxidation and contamination
- Improved material properties (e.g., strength, porosity)
Energy Savings and Operational Efficiency
Vacuum pumps can lead to significant energy savings and improved operational efficiency by:
- Optimizing pump performance to match process load
- Reducing pump wear and maintenance requirements
- Enabling efficient gas transfer and minimizing flow losses
Versatility and Adaptability
Vacuum pumps offer versatility and adaptability to various applications due to:
- Availability of different pump types (e.g., rotary, diffusion, turbomolecular)
- Ability to handle corrosive, flammable, or hazardous gases
- Compatibility with a wide range of operating pressures
Compact and Integrated Designs
Modern vacuum pump designs offer compact and integrated solutions, enabling:
- Space-saving installations in confined areas
- Integration with other system components for streamlined operation
- Modular and scalable configurations to meet varying process requirements
Applications of Vacuum Pumps
Semiconductor Manufacturing
Vacuum pumps are essential in semiconductor manufacturing for creating the necessary vacuum conditions for processes like integrated circuit fabrication, flat panel display production, and optoelectronic device manufacturing. These processes involve high-temperature treatments and multiple thin-film depositions, which require low-pressure environments facilitated by vacuum pumps. The variable operative connection between the high-vacuum and rough vacuum modules in the pump allows for adjustable suction power ratios, preventing excessive power consumption and improving overall pumping efficiency.
Optical Coating
Vacuum pumps are indispensable in optical coating processes, where specialized thin films are deposited on optical components to modify their refractive and reflective properties, enabling desired optical effects and colors. The vacuum environment ensures the self-cleaning and wear-resistant properties of the coatings.
Electron Microscopy
High-precision instruments like transmission electron microscopes (TEM) and scanning electron microscopes (SEM) require ultra-high vacuum conditions for operation. Vacuum pumps enable the creation of these environments, preventing electron beam scattering and absorption by gas molecules, ensuring high-quality imaging based on electron-matter interactions.
Medical and Pharmaceutical Applications
Vacuum pumps find applications in medical device manufacturing, pharmaceutical processes, and vacuum-assisted wound therapy. They facilitate processes like freeze-drying, vacuum packaging, and controlled atmospheric conditions for sensitive materials and operations.
Industrial Processes
Across various industries, vacuum pumps are employed in processes such as vacuum distillation, vacuum metallurgy, space simulation, thin-film deposition for microelectronics, and surface analysis 16. They enable the creation of controlled low-pressure environments essential for these processes, contributing to product quality and process efficiency.
Environmental and Energy Applications
Vacuum pumps play a role in environmental control chambers, simulating atmospheric conditions at different elevations for acclimatization purposes. They are also utilized in energy-efficient applications like waste heat recovery, industrial furnaces, and water purification processes.
Maintenance and Troubleshooting
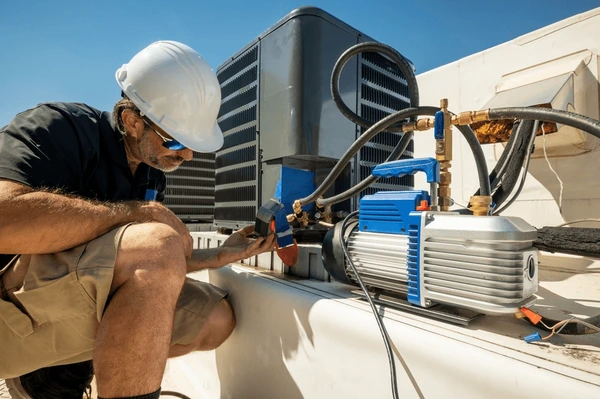
Vacuum pumps are crucial tools for maintenance and commissioning of systems like HVAC-R (Heating, Ventilation, Air Conditioning, and Refrigeration). They enable vacuum testing, leak detection, and system evacuation, ensuring proper operation and performance.
Application Cases
| Product/Project | Technical Outcomes | Application Scenarios |
|---|---|---|
| Semiconductor Manufacturing Vacuum Pumps | Enables low-pressure environments for integrated circuit fabrication, flat panel display production, and optoelectronic device manufacturing. Adjustable suction power ratios prevent excessive power consumption and improve overall pumping efficiency. | Semiconductor manufacturing processes involving high-temperature treatments and multiple thin-film depositions. |
| Optical Coating Vacuum Pumps | Facilitates the deposition of specialized thin films on optical components, ensuring self-cleaning and wear-resistant properties of the coatings. | Optical coating processes for modifying the refractive and reflective properties of optical components. |
| Electron Microscopy Vacuum Pumps | Maintains ultra-high vacuum conditions required for high-precision instruments like transmission electron microscopes (TEM) and scanning electron microscopes (SEM). | Electron microscopy techniques for high-resolution imaging and analysis of materials. |
| Vacuum Packaging Systems | Extends the shelf life of perishable foods by removing air and moisture, preventing oxidation and microbial growth. Improves product quality and reduces waste. | Food and pharmaceutical packaging processes for preserving freshness and maintaining sterility. |
| Industrial Vacuum Furnaces | Enables high-temperature heat treatment processes in a controlled, oxygen-free environment, preventing oxidation and contamination of materials. | Heat treatment processes for metals, ceramics, and other materials in industries like aerospace, automotive, and electronics. |
Latest Technical Innovations of Vacuum Pumps
Modular Vacuum Pump Design
A modular vacuum pump design with variable operative connections between high-vacuum and rough vacuum modules allows automatically adjusting the ratio of suction powers. This prevents excessive drive power for the high-vacuum module and increases overall pumping efficiency, especially at high suction pressures. The modules can be driven at different speeds or traversed by different gas flows for optimized performance.
Improved Cooling Capabilities
Vacuum pumps with a hollow area connected to the pump outlet in a gas-conducting manner enable effective cooling in pump areas prone to heating. This reduces maintenance needs, increases performance, and extends operating life. The existing air cooling system connected to the pump outlet can introduce the cooling gas efficiently.
Particle Protection Mechanisms
To prevent damage from ingested particles, especially in turbomolecular pumps with rapidly rotating components, vacuum pumps can integrate protective devices with grids fastened to the shaft bearing support. This eliminates the need for separate protective grilles while ensuring pump stability and efficiency.
Advanced Sealing Technologies
Gas-lubricated mechanical seals create a non-contact, wear-free, fluid-tight seal between the working space and storage space in vacuum pumps. This prevents fluid exchange, maintains vacuum quality, and reduces the risk of component damage compared to conventional shaft seals.
Intelligent Control Systems
Vacuum pumps with integrated pressure sensors, communication units, and control logic circuits can detect vacuum pressures, monitor power usage, and control pump operation accordingly. This enables efficient vacuum testing during maintenance or commissioning of systems like HVAC-R while communicating data to remote devices.
Energy-Efficient Designs
Vacuum systems with multiple pumps connected in parallel, where at least one pump is a variable speed drive (VSD), can reduce energy consumption. As the performance of one pump increases, the other VSD pump can reduce its performance while maintaining the set pressure, optimizing overall efficiency.
Technical Challenges of Vacuum Pumps
| Modular Vacuum Pump Design | Developing a modular vacuum pump design with variable operative connections between high-vacuum and rough vacuum modules to automatically adjust the ratio of suction powers, preventing excessive drive power for the high-vacuum module and increasing overall pumping efficiency. |
| Improved Cooling Capabilities | Integrating a hollow area connected to the pump outlet in a gas-conducting manner to enable effective cooling in pump areas prone to heating, reducing maintenance needs, increasing performance, and extending operating life. |
| Particle Protection Mechanisms | Integrating protective devices with grids fastened to the shaft bearing support to prevent damage from ingested particles, eliminating the need for separate protective grilles while ensuring pump stability and efficiency. |
| Variable Speed Drive Control | Implementing variable speed drive control for vacuum pumps to match their performance to the load supplied by the processing chamber, reducing energy consumption and pump wear when underutilized. |
| Ceramic Rotor Components | Incorporating ceramic materials for at least one rotor component in vacuum pumps to improve performance, particularly in turbomolecular pumps, by enhancing heat resistance and durability. |
To get detailed scientific explanations of the vacuum pumps, try Patsnap Eureka.