
Anti-H2S stress corrosion high pressure resistant forgings and method for manufacturing same
A stress corrosion and hydrogen sulfide resistance technology is applied in the field of hydrogen sulfide stress corrosion resistance and high pressure forgings for large blowout preventers and their manufacturing fields. The effect of reducing the formation trend of non-metallic inclusions, improving hardenability, and increasing the density of steel
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Patents(China)
- Current Assignee / Owner
- Publication Date
- 2010-05-19
Smart Images
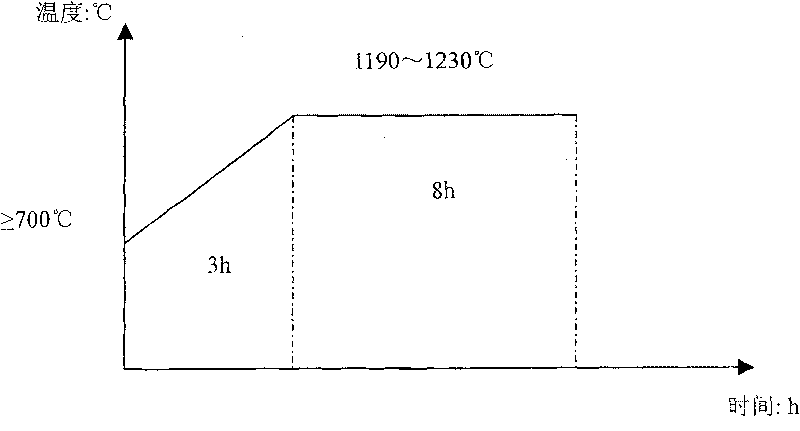
Figure 1 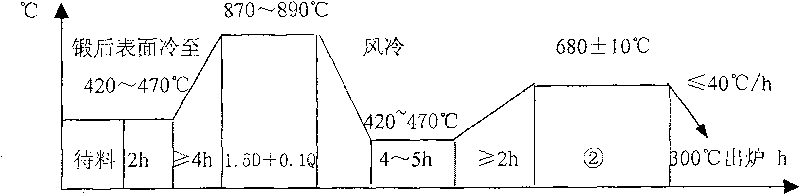
Figure 2 
Figure 3
Abstract
Description
technical field
[0001] The invention relates to a hydrogen sulfide stress corrosion resistant high pressure forging for a large blowout preventer and a manufacturing method thereof. Background technique
[0002] During downhole operations, when the formation is open, if effective measures cannot be taken to control the high bottom pressure, bottom fluid (oil, gas and water) may flow into the wellbore uncontrollably and spray to the ground in large quantities. This is a blowout . Blowout accidents have great harm to the life and property safety of personnel near the well site, the environment around oil and gas wells, and underground oil and gas resources. Therefore, a blowout preventer should be installed at the oil well / gas wellhead, and it should be activated urgently to seal the wellhead when a blowout occurs, so as to avoid large economic losses.
[0003] The blowout preventer not only bears the huge pressure at the bottom of the oil well, but also bears the H in the o...
Examples
Embodiment 1
[0053] Its chemical composition is shown in Table 1, and the rest are Fe and unavoidable impurities;
[0054] Table 1
[0055]
[0056] After electric furnace smelting, refining outside the furnace and vacuum degassing, 35 tons of steel ingots are poured, demoulded and sent to the fast forging heating furnace for heating 12 hours after casting. The heating rate is heated to 1210°C and then kept for 8 hours. The heating process curve is shown in figure 1 Shown; the heating rate of the steel ingot and the soaking time in the high temperature section are controlled reasonably.
[0057] figure 2 It is a process curve diagram of normalizing and tempering treatment of forgings according to the present invention. Pre-normalizing treatment is carried out by air cooling after forging, and the temperature is kept at 420-470 ° C for 2 hours. The normalizing temperature is 870-890°C, and the holding time is 21 hours, so that the structure can be fully transformed and stable austen...