
Drip irrigation pipe head binding method
A bonding method and technology for drip irrigation pipes, which are applied in botany equipment and methods, climate change adaptation, gardening, etc., can solve problems such as difficult control, high defective rate, and drippers that have not been preheated, so as to improve productivity and Adhesive strength, effect of improving compressive strength
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Patents(China)
- Current Assignee / Owner
- Publication Date
- 2006-03-08
- Estimated Expiration
- Not applicable · inactive patent
Smart Images
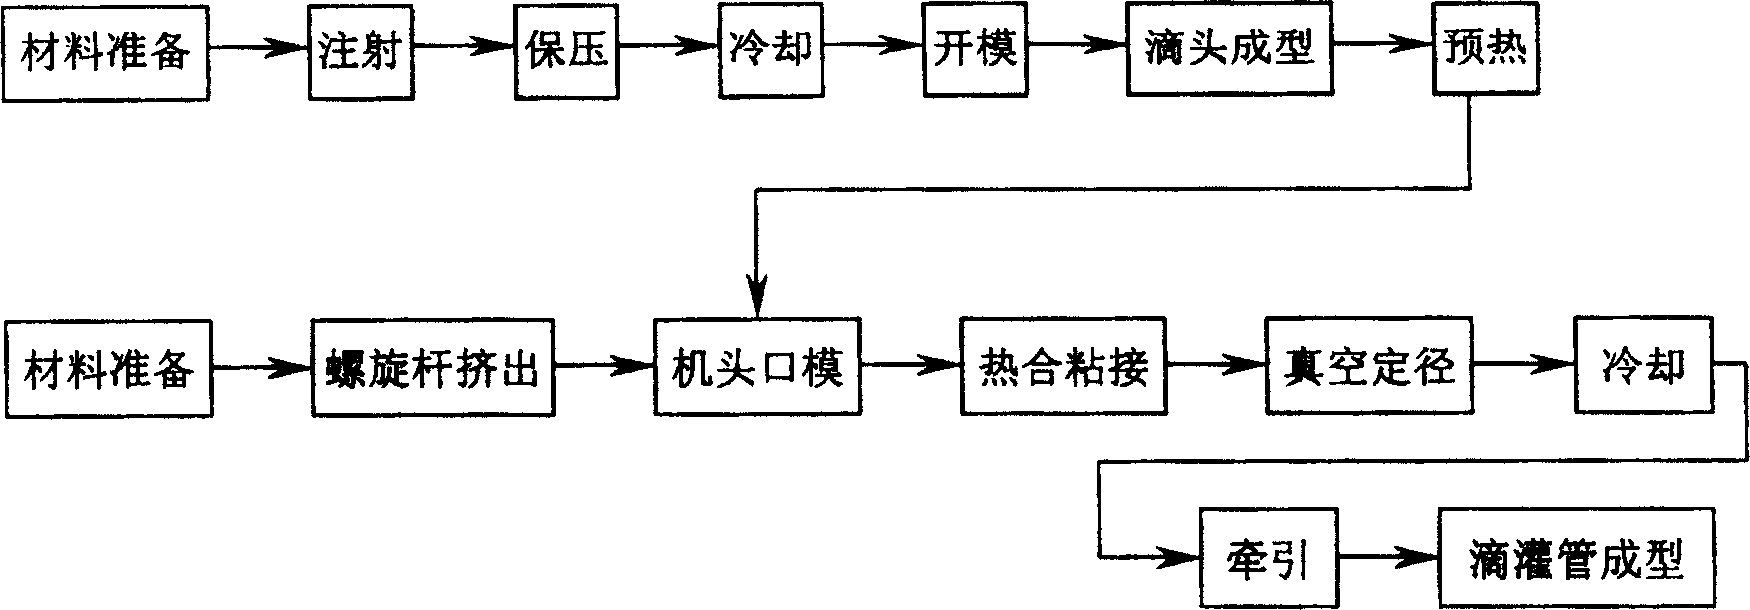
Figure 1
Abstract
Description
technical field
[0001] The patent of the invention relates to the production, processing and technology of a drip irrigation pipe, in particular to a bonding method for drip irrigation pipe emitters. Background technique
[0002] The existing drip irrigation pipe dripper bonding, first, the dripper has not been preheated; second, the formula of the dripper material and the tube embryo material is very different, and the tube embryo material is required to be soft and elastic, and it must be suitable for extrusion processing. Process conditions, the material is mainly high-pressure polyethylene, the melt index is generally 1 to 2, and the dripper has to withstand the impact of punching, which requires relatively high strength and hardness, and is suitable for the requirements of the injection molding process. The material is mainly low-pressure polyethylene. , The melt index is generally around 10, which requires the temperature of the head and die to be controlled at around ...
Examples
Embodiment Construction
[0007] The present invention will be further described below in conjunction with the accompanying drawings.
[0008] According to the technical scheme, the material formula and method steps are:
[0009] 1. Material preparation: The selection of dripper and tube embryo material is the basis of the processing technology, that is, the material must not only meet the performance of the product, the injection molding (extrusion) processing technology, but also meet the bonding processing technology. Therefore, (1) The dripper material should have certain strength and hardness, and it should also be suitable for the processing technology of injection molding. Its melt index is 6-8, and the material formula is high pressure polyethylene: low pressure polyethylene: medium density polyethylene = 2 : 6: 2 (mass ratio); tube embryo material should have a certain degree of flexibility to meet the extrusion process, its melt index is 6-8, and the material formula is high pressure polyethy...