
Air knife pressure real-time optimization control method and system in galvanizing process
A technology of optimized control and air knife pressure, applied in hot-dip plating process, coating, metal material coating process, etc., can solve the problems of slow correction of coating thickness deviation, difficulty in establishing a system model, overshoot of control quantity, etc.
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Applications(China)
- Current Assignee / Owner
- Publication Date
- 2017-05-10
Smart Images
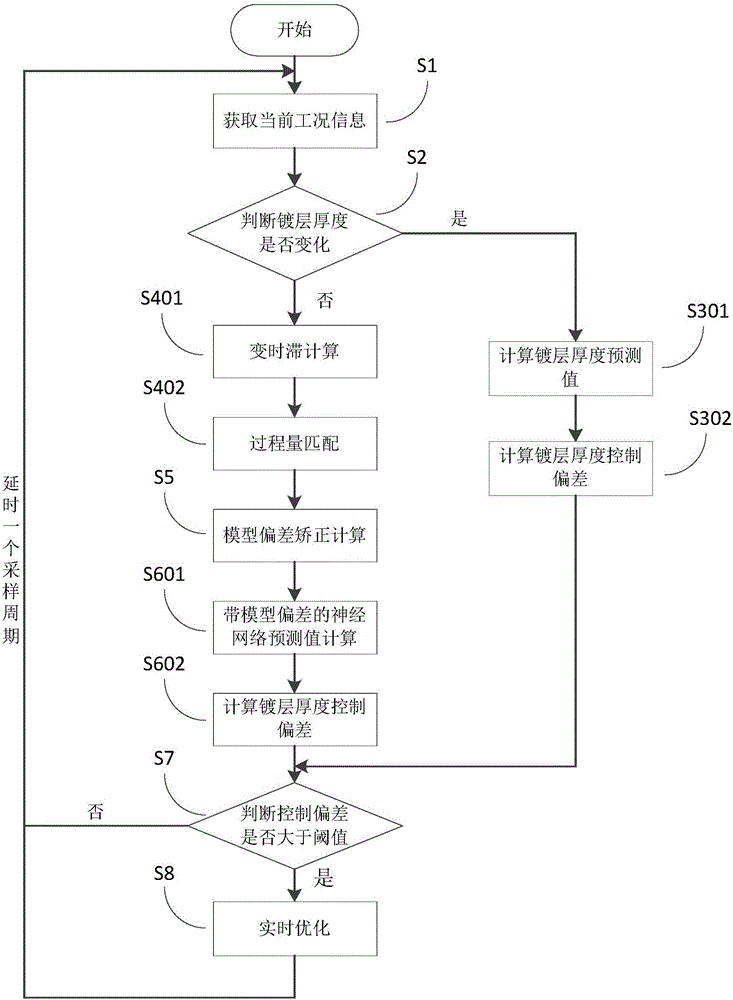
Figure 1 
Figure 2 
Figure 3
Abstract
Description
technical field
[0001] The invention relates to the technical field of galvanizing technology and the technical field of real-time optimization control of industrial process, in particular to a method and system for real-time optimization control of air knife pressure in the galvanizing process. Background technique
[0002] Entering the 21st century, our country is moving from a big steel country to a strong steel country. Adjusting industrial structure, developing deep processing and high value-added products, and improving product competitiveness are the development directions of my country's iron and steel industry.
[0003] However, according to statistics, metal products discarded due to corrosion in my country account for one-third of the world's total annual metal output, which shows that solving the corrosion problem of steel has very important economic significance for our country. The galvanizing process can effectively prevent steel corrosion and prolong the ser...
Examples
Embodiment Construction
[0089] The embodiments of the present invention are described in detail below. This embodiment is implemented on the premise of the technical solution of the present invention, and detailed implementation methods and specific operating procedures are provided, but the protection scope of the present invention is not limited to the following implementation example. The meaning of each symbol among the present invention is referring to the following table:
[0090] The embodiment of the present application provides a method for real-time optimal control of air knife pressure in the galvanizing process, such as figure 1 shown, including the following steps:
[0091] S1. Obtain the working condition information at the current moment, including air knife distance D(t), air knife pressure P(t), production line speed S(t), coating thickness measurement value CW_act(t) and coating thickness setting value CW_set( t);
[0092] S2, determine whether formula (1) is established, if yes,...