
Rolling method of small and medium shipbuilding flat-bulb steel
A small and medium-sized ball technology, applied in the field of section steel rolling, can solve the problems of backward production technology, high tooling consumption, poor surface quality, etc., and achieve the effect of improving surface quality, improving production efficiency, and reducing rolling passes.
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Applications(China)
- Current Assignee / Owner
- Publication Date
- 2018-11-13
- Estimated Expiration
- Not applicable · inactive patent
Smart Images
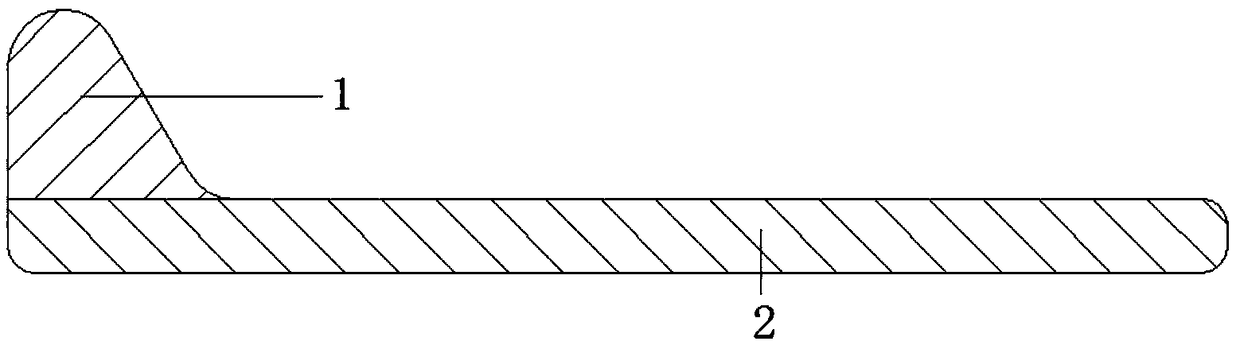
Figure 1 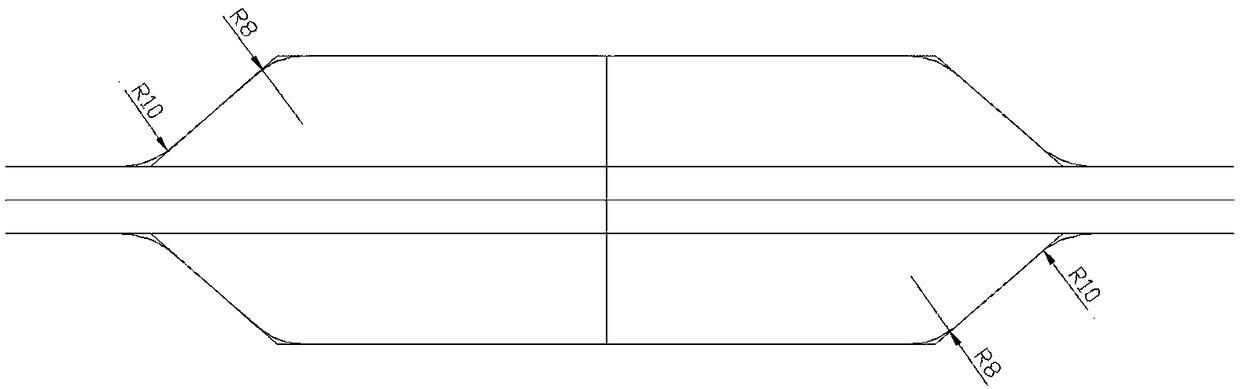
Figure 2 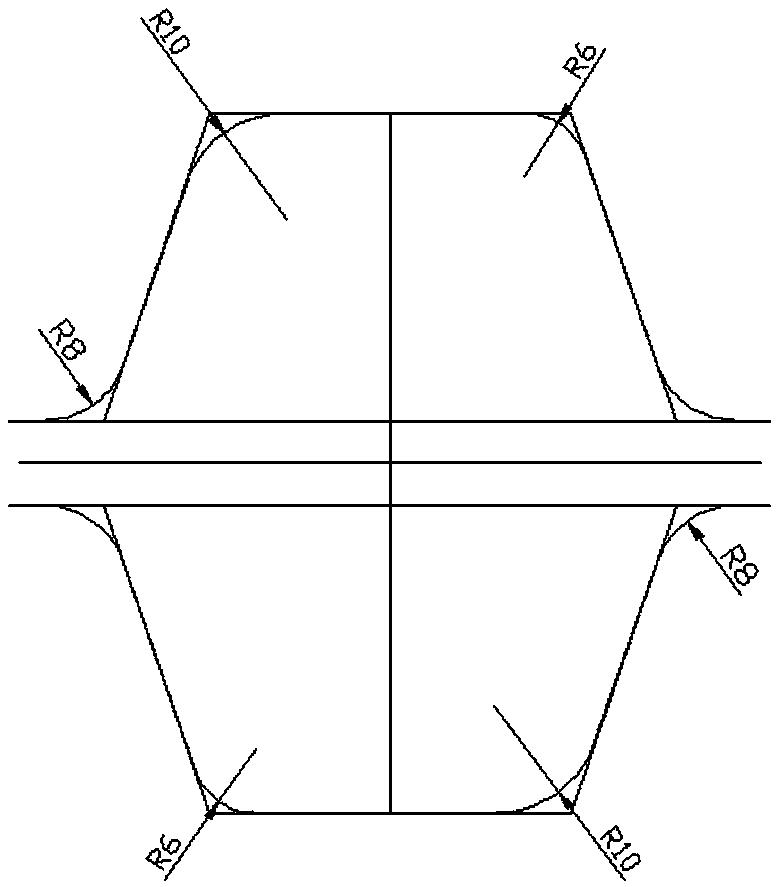
Figure 3
Abstract
Description
technical field
[0001] The invention relates to the technical field of section steel rolling, in particular to a rolling method of small and medium-sized shipbuilding flat bulbs. Background technique
[0002] Bulb flat steel is a key structural steel in shipbuilding steel. Small and medium-sized bulb flat steel refers to a bulb flat steel with a web width of less than 160mm; with the development of the shipbuilding industry, the demand for bulb flat steel continues to increase. At the same time, the requirements for its finished product rate are getting higher and higher. At present, the production technology of domestic bulb flat steel is relatively backward, the yield rate is low, the consumption of tooling is high, and the surface quality is poor. Therefore, the development of a new rolling process of bulbous flat steel for shipbuilding has become an important research goal for domestic steel rolling mills. Contents of the invention
[0003] The invention provides a r...
Examples
Embodiment Construction
[0027] The specific embodiment of the present invention will be further described below in conjunction with accompanying drawing:
[0028] A rolling method of small and medium-sized shipbuilding flat bulbs according to the present invention adopts a direct rolling method for rolling, and the rolling equipment includes 3-5 shifts of three-roller type steel mills, and each shift of three-roller type steel mills is divided into rows layout; the specific rolling process includes the following steps:
[0029] 1) Rough rolling, including several passes of rolling process; in this step, box-shaped pass rolling is completed, and the rolled piece is rolled out of a bulbous flat steel special-shaped section;
[0030] 2) Intermediate rolling, including several rolling passes; in this step, the distribution of the metal amount between the ball head 1 and the web 2 is completed; the rough-rolled special-shaped rolled piece is forced to widen by a large reduction, and it is completed at one...