
Method for repairing heat recovery steam generator tube-to-header damage
a heat recovery steam generator and head-to-header technology, which is applied in the direction of electrical wiring devices, lighting and heating apparatus, soldering apparatus, etc., can solve the problems of thermal fatigue failure at the toe of the tube weld, life limiting factors of many heat recovery steam generators, and difficulty in repairing heat exchanger tubes and head-to-header damage, etc., to reduce the number of welds and the time required
Patent Information
- Authority / Receiving Office
- US · United States
- Patent Type
- Applications(United States)
- Current Assignee / Owner
- Publication Date
- 2009-09-10
- Estimated Expiration
- Not applicable · inactive patent
Smart Images
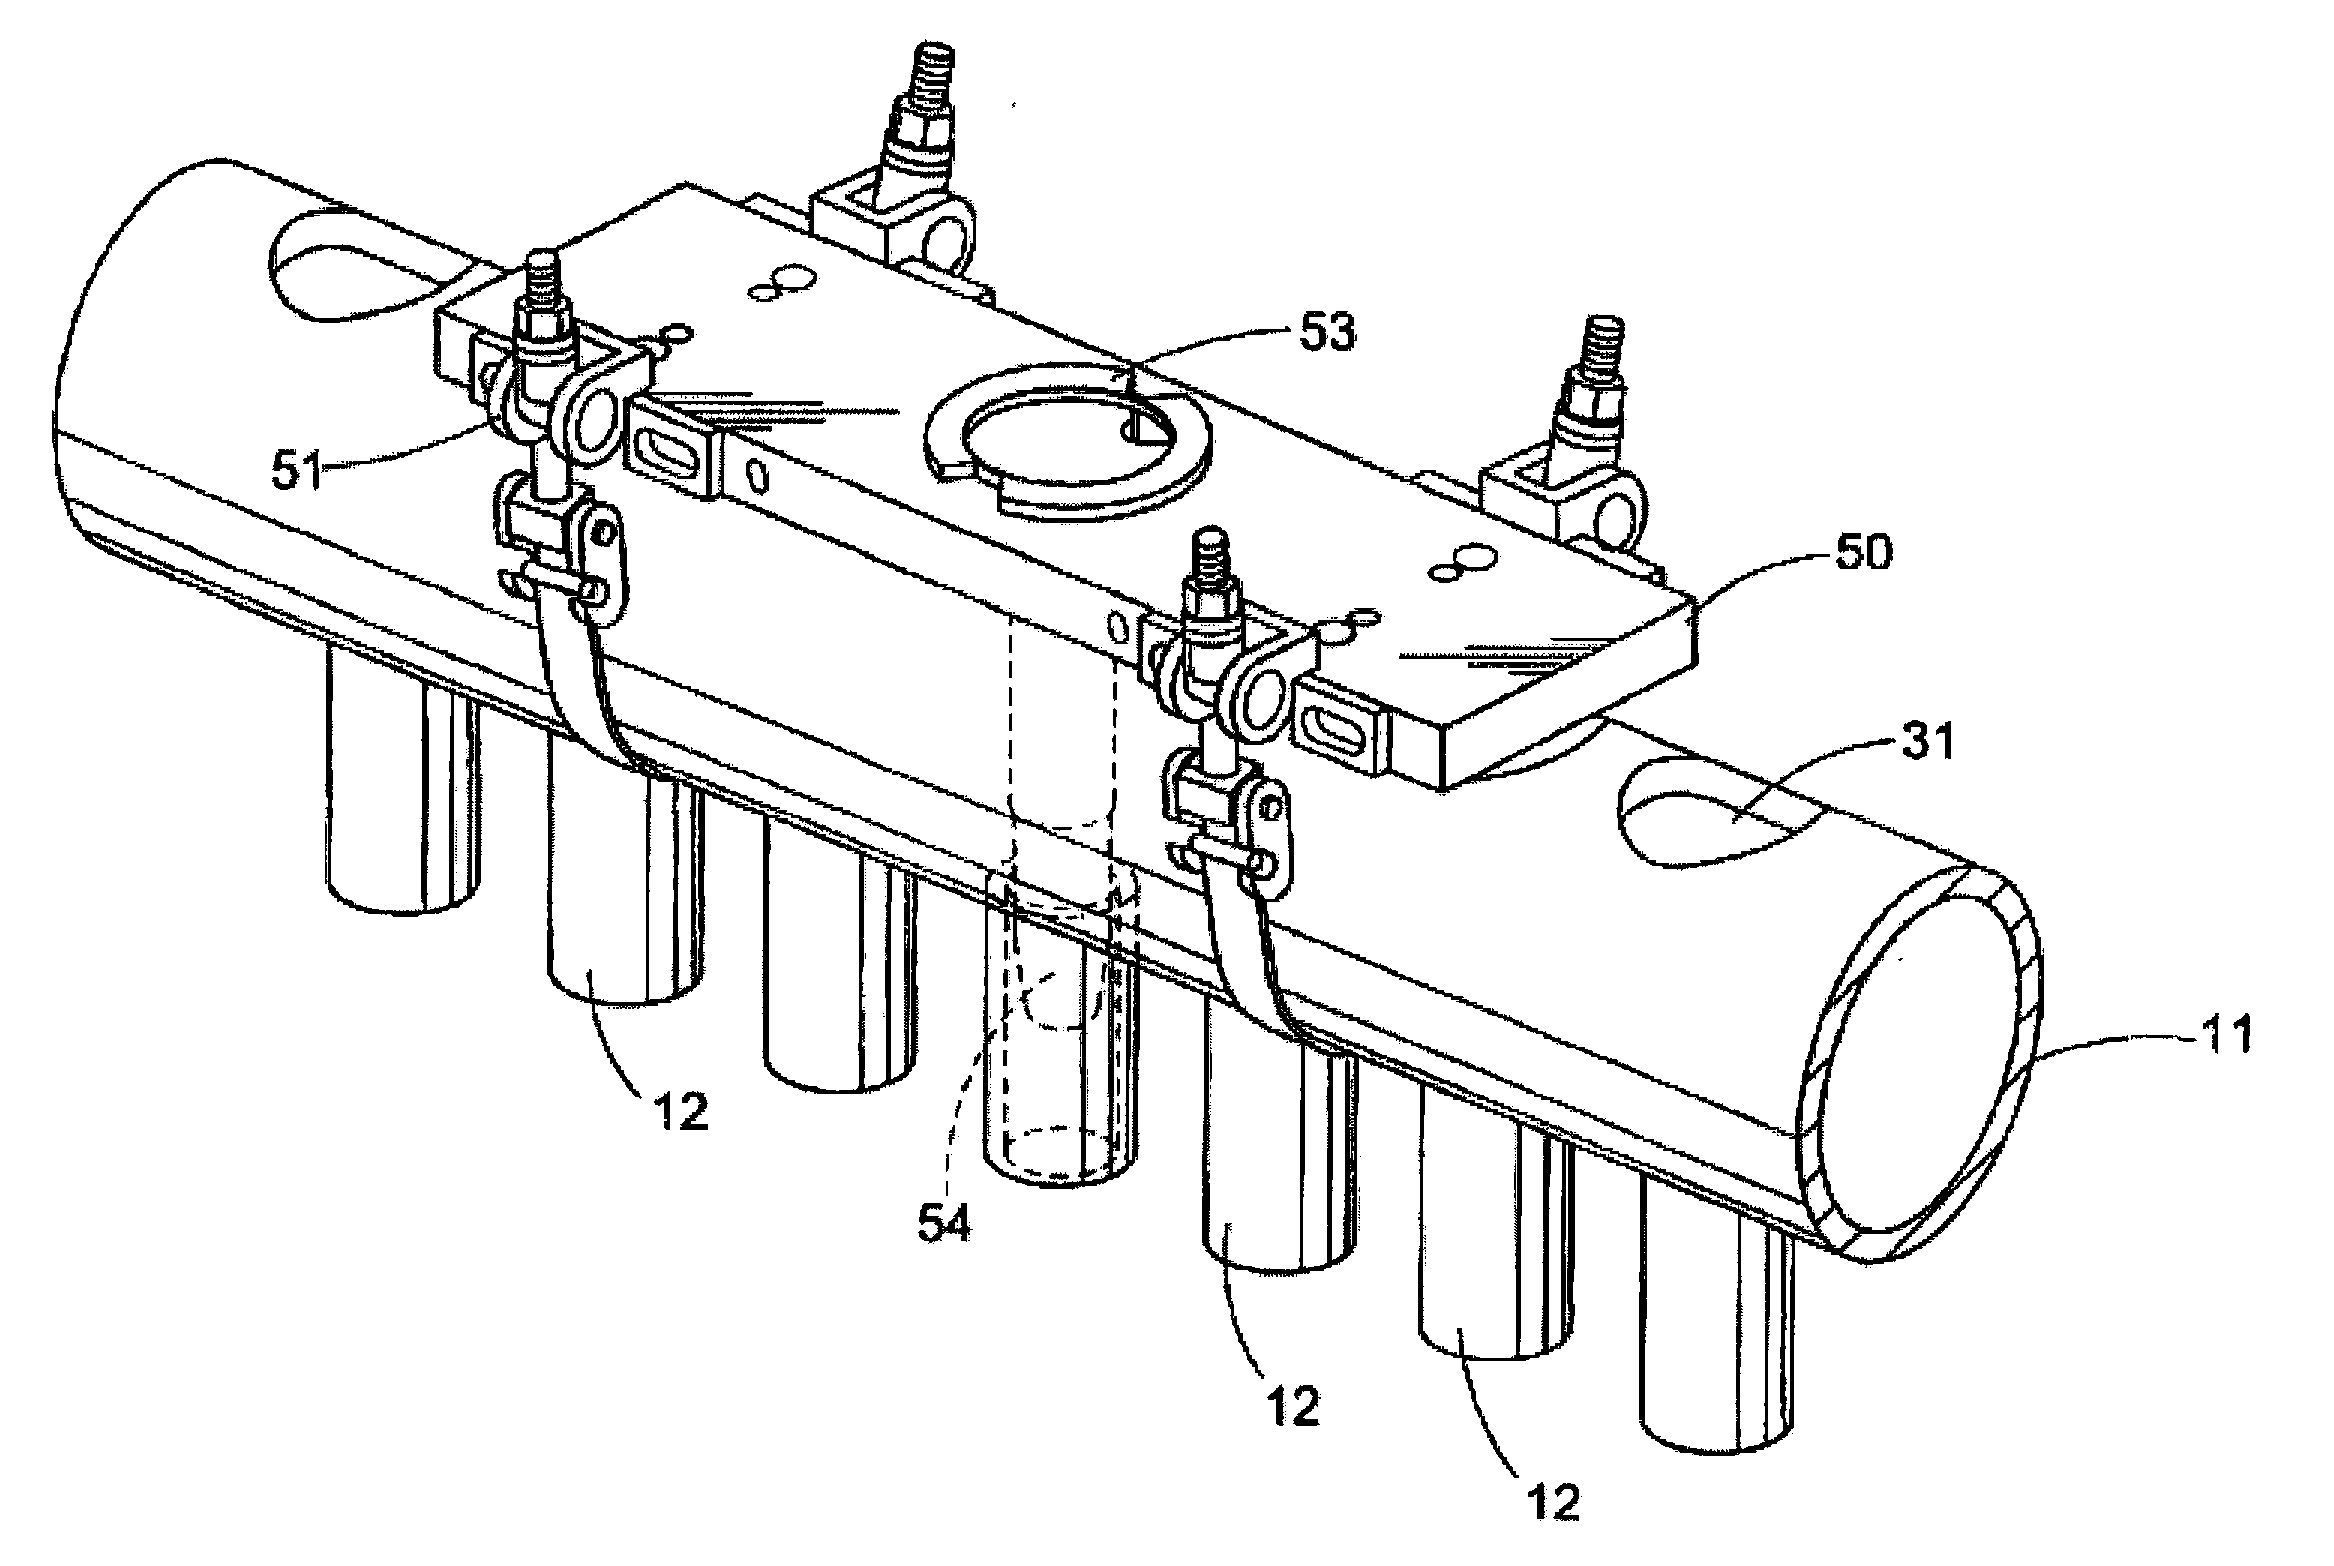
Figure 1 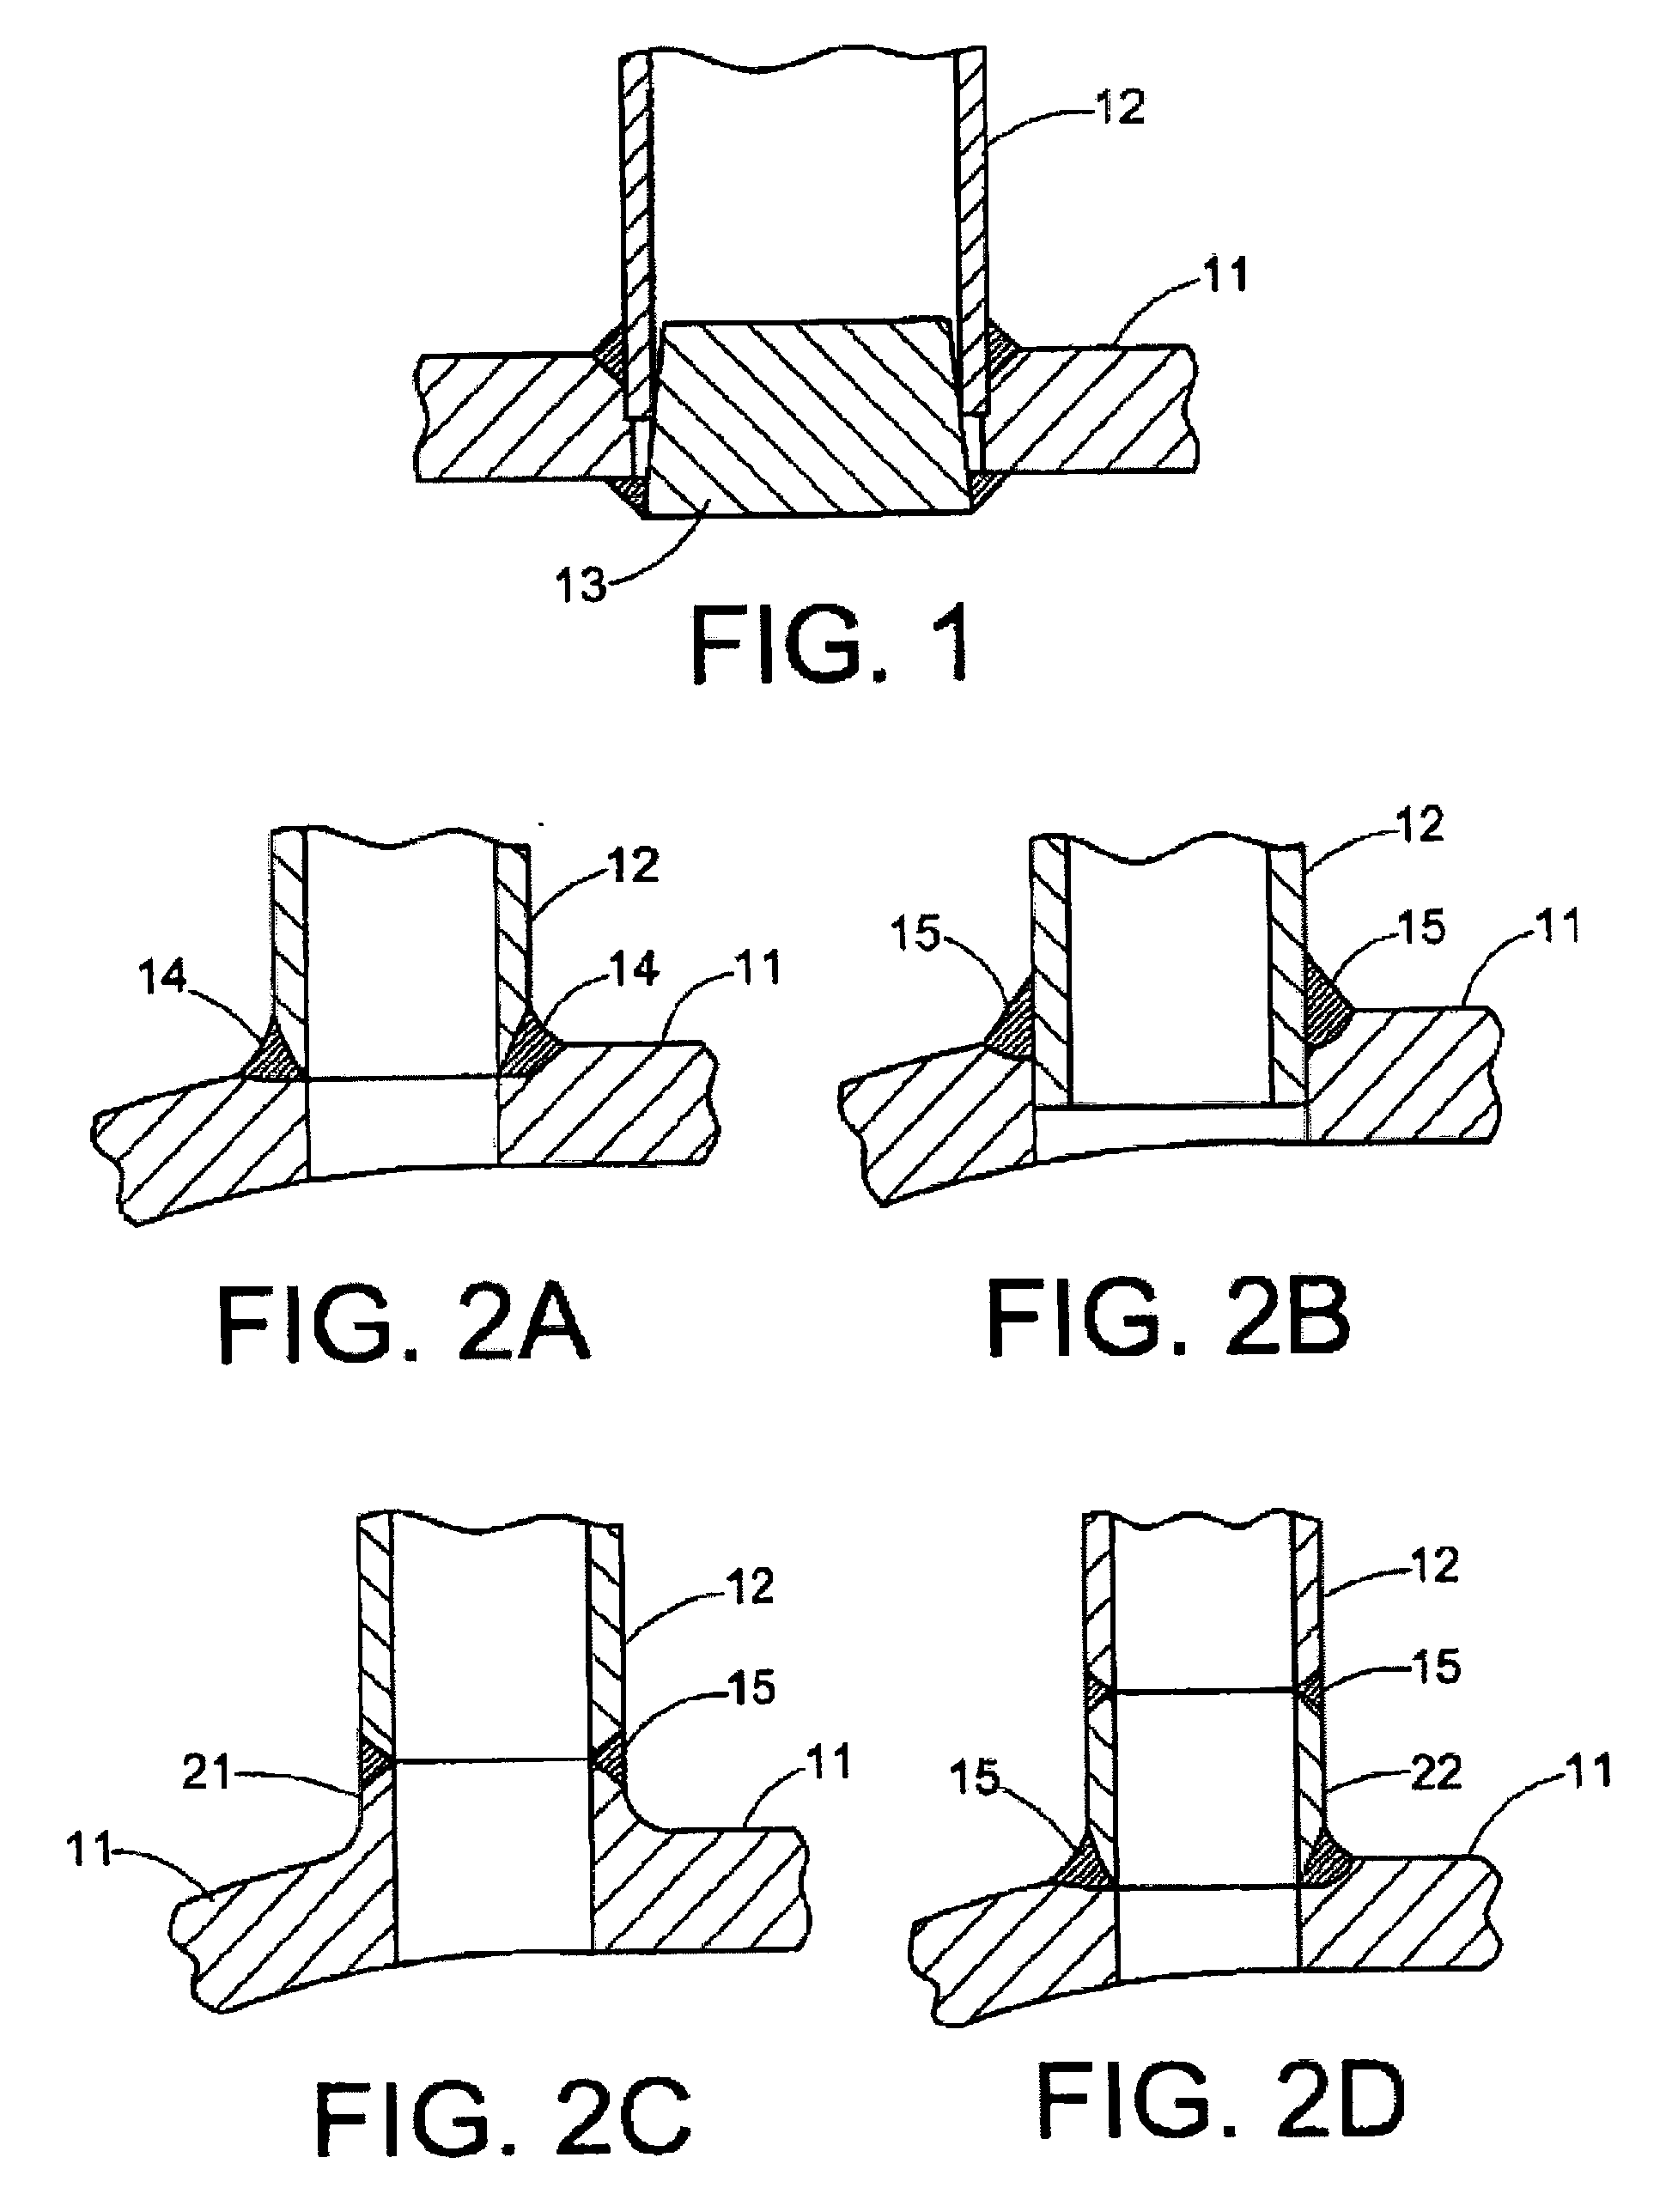
Figure 2 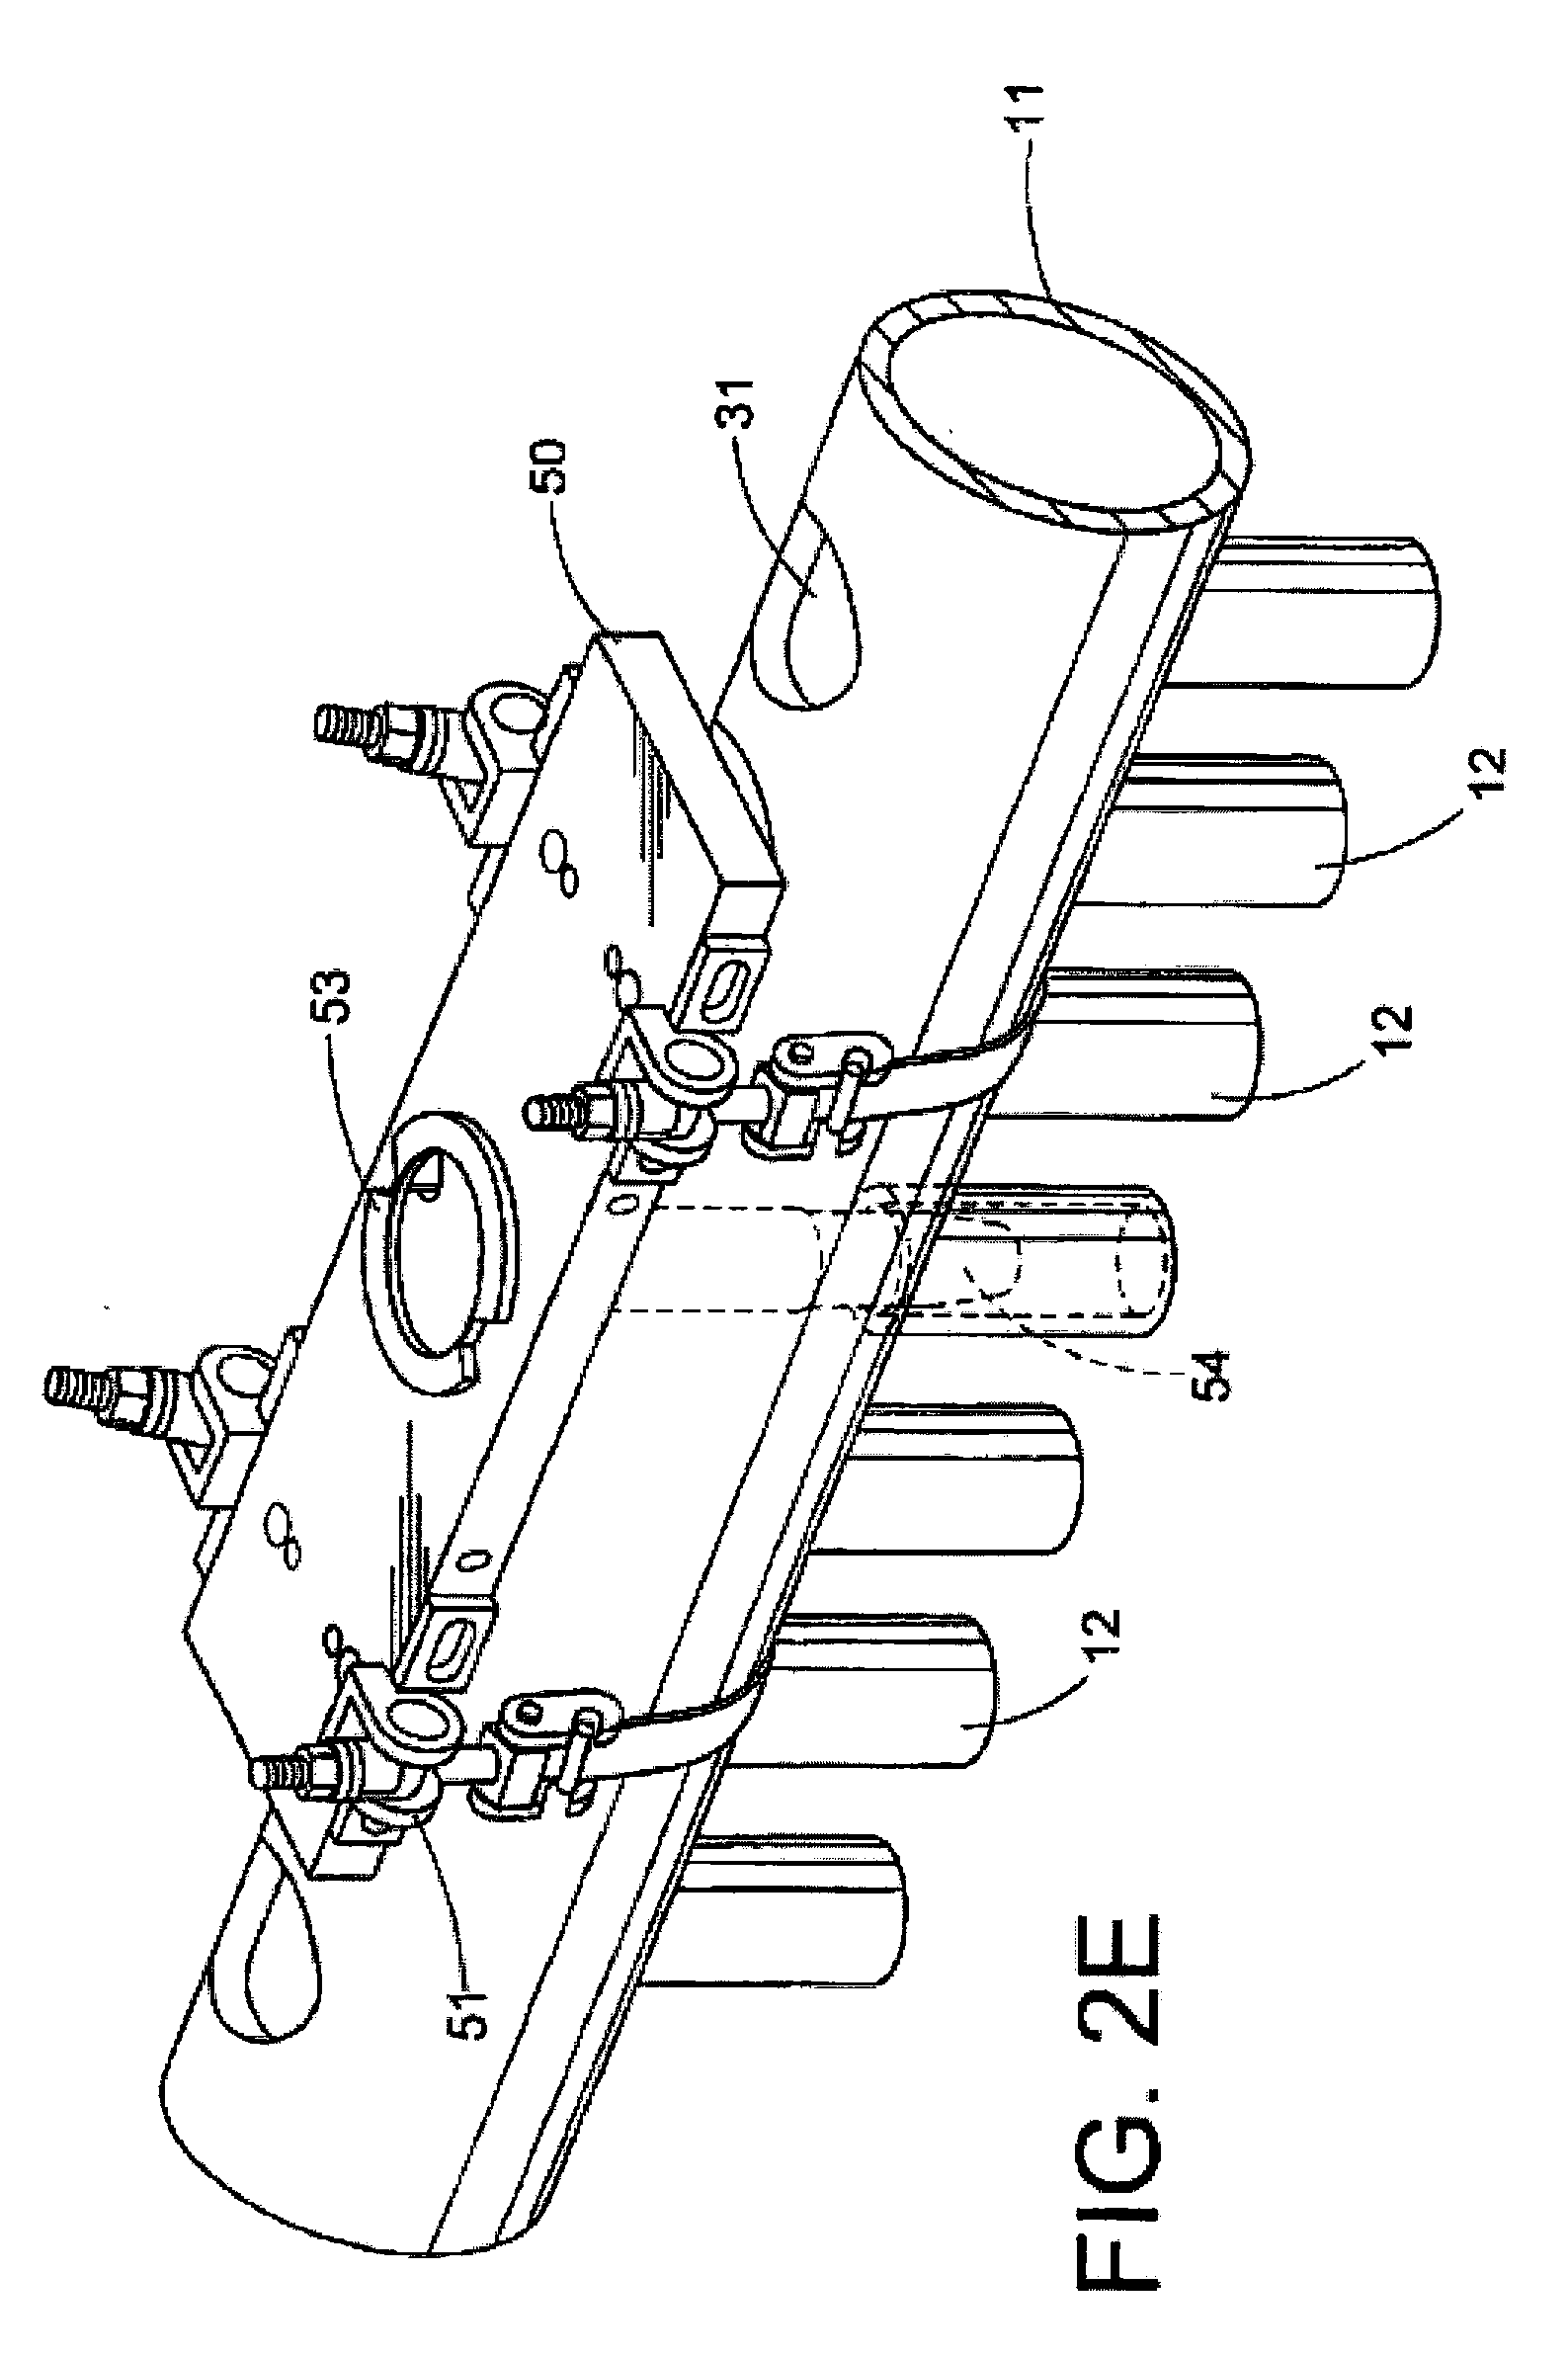
Figure 3
Abstract
Description
CROSS REFERENCE TO RELATED APPLICATIONS
[0001] This application is a continuation of U.S. Ser. No. 11 / 364,604, filed on Feb. 28, 2006, which claims the benefit of the filing date of U.S. Provisional Application for Patent Ser. No. 60 / 656,959 filed Feb. 28, 2005, both of which are incorporated herein by reference.FIELD OF INVENTION
[0002] The present invention is directed to a method for repairing heat exchanger tube and tube attachment damage, such as for heat transfer applications. More specifically, the disclosed method is related to a method for repairing a heat recovery steam generator (HSRG) tube damage and tube to header attachment damage, for applications such as electricity producing power plants, such as fossil fuel plants.BACKGROUND
[0003] One of the life limiting factors for many heat recovery steam generators (HRSGs) is associated with damage that occurs at header-to-tube attachments. This attachment is particularly troublesome due to thermal differences experienced between th...
Examples
Embodiment Construction
[0031]The present method provides a more pragmatic approach to address HRSG header-to-tube attachment damage than is currently used by industry today. This form of repair is often more difficult than conventional tube repairs due to limited access to the damage location. As a result, tube and header to tube attachment failures are often left in place and simply plugged. FIG. I illustrates a plug weld configuration. Plugging requires removal of an access window within the header 11 one hundred eighty (180) degrees away from the stub tube 12 attachment location, machining and insertion of a plug 13 into the damaged tube bore, welding of the plug into place, and then re-installation of the window.
[0032]Repair methodology is complicated by the number of different attachment configurations used by industry. Header to tube attachment weld designs used by original equipment manufacturers (OEMs) include:
[0033]a) partial penetration welds 14 (shown in FIG. 2A);
[0034]b) fall penetration welds...