
Bitumen-impregnated type composite steel wire rope for railway and production method thereof
A production method and asphalt-impregnated technology, which is applied in the asphalt-impregnated composite steel wire rope used in railways and its production field, can solve the problems that the composite steel wire rope cannot meet the design requirements of high-speed railways, and can not meet the requirements, so as to ensure work efficiency and work safety , high tensile strength and high filling factor
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Applications(China)
- Current Assignee / Owner
- Publication Date
- 2015-05-13
Smart Images
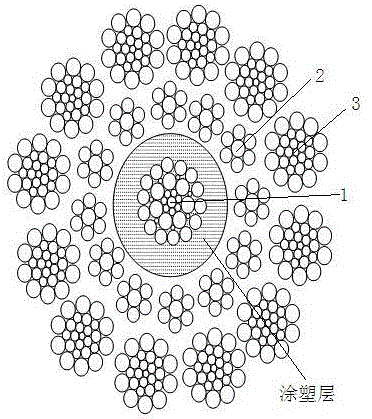
Figure 1 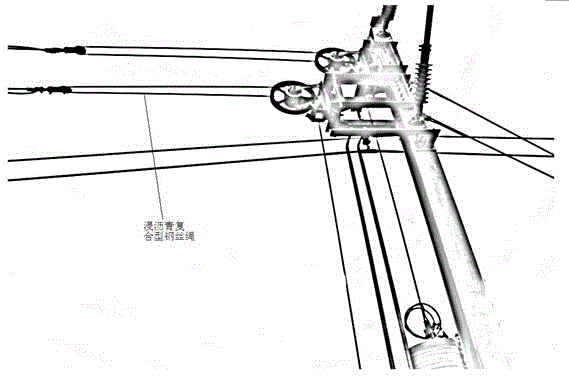
Figure 2
Abstract
Description
technical field
[0001] The invention belongs to the technical field of steel wire rope applications, and in particular relates to an asphalt-soaked composite steel wire rope for railways and a production method thereof. Background technique
[0002] With the development of high-speed railways in China and the world, more and more special steel wire ropes are used for electrified railways, and the requirements for their quality and performance are getting higher and higher. The requirements for the composite steel wire ropes used in railway compensation devices are also getting higher and higher. On the premise of considering the reasonable cooperation of the rope and the wheel and the small increase of the wheel groove of the overall device, the diameter of the composite steel wire rope basically does not increase, and higher requirements are put forward for the breaking force of the composite steel wire rope, and the composite steel wire rope is required to have a stronger ...
Examples
Embodiment 1
[0035] Another aspect of the present invention provides a production method of asphalt-impregnated composite steel wire rope for railway, the structure of the asphalt-impregnated composite steel wire rope for railway is 12×26WS+12×7+1×36SFi, and the tensile strength of single-strand structure is greater than Equal to 2300Mpa, the knotting tension is greater than or equal to 55%, the number of torsion resistance is greater than or equal to 21, the tension of the inner strands is greater than or equal to 2300KN, and the tension of the outer strands is greater than or equal to 6000KN, which includes the following steps,
[0036] Step 1. For the wire rod, use SWRH72A with a diameter of 5.5 mm.
[0037] Step 2. Rough drawing. Use a straight wire drawing machine model 11 / 560 to draw a 5.5 mm diameter SWRH72A wire into a 2.0 mm SWRH72A. The drawing process is 5.5-4.9-4.4-4.0-3.7-3.4- 3.1-2.8-2.5-2.2-2.0.
[0038] Step 3, heat treatment, choose a gas-fired type 32 electric heating fu...
Embodiment 2
[0048] Another aspect of the present invention provides a production method of asphalt-impregnated composite steel wire rope for railway, the structure of the asphalt-impregnated composite steel wire rope for railway is 12×26WS+12×7+1×36SFi, and the tensile strength of single-strand structure is greater than Equal to 2300Mpa, the knotting tension is greater than or equal to 55%, the number of torsion resistance is greater than or equal to 21, the tension of the inner strands is greater than or equal to 2300KN, and the tension of the outer strands is greater than or equal to 6000KN, which includes the following steps,
[0049] Step 1. For the wire rod, use SWRH72A with a diameter of 5.5 mm.
[0050] Step 2. Rough drawing. Use a straight wire drawing machine model 11 / 560 to draw a 5.5 mm diameter SWRH72A wire into a 2.0 mm SWRH72A. The drawing process is 5.5-4.9-4.4-4.0-3.7-3.4- 3.1-2.8-2.5-2.2-2.0.
[0051] Step 3, heat treatment, choose a gas-fired type 32 electric heating fu...
Embodiment 3
[0062] Another aspect of the present invention provides a production method of asphalt-impregnated composite steel wire rope for railway, the structure of the asphalt-impregnated composite steel wire rope for railway is 12×26WS+12×7+1×36SFi, and the tensile strength of single-strand structure is greater than Equal to 2300Mpa, the knotting tension is greater than or equal to 55%, the number of torsion resistance is greater than or equal to 21, the tension of the inner strands is greater than or equal to 2300KN, and the tension of the outer strands is greater than or equal to 6000KN, which includes the following steps,
[0063] Step 1. For the wire rod, use SWRH72A with a diameter of 5.5 mm.
[0064] Step 2. Rough drawing. Use a straight wire drawing machine model 11 / 560 to draw a 5.5 mm diameter SWRH72A wire into a 2.0 mm SWRH72A. The drawing process is 5.5-4.9-4.4-4.0-3.7-3.4- 3.1-2.8-2.5-2.2-2.0.
[0065] Step 3, heat treatment, choose a gas-fired type 32 electric heating fu...