
Quick clamping positioning tool for processing shutter
A clamping positioning and tooling technology, used in positioning devices, clamping devices, metal processing equipment, etc., can solve the problems of poor fixing stability, low positioning accuracy, low processing efficiency, etc., to increase the cutting amount and improve production efficiency. , the effect of improving processing efficiency
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Applications(China)
- Current Assignee / Owner
- Publication Date
- 2019-01-15
Smart Images
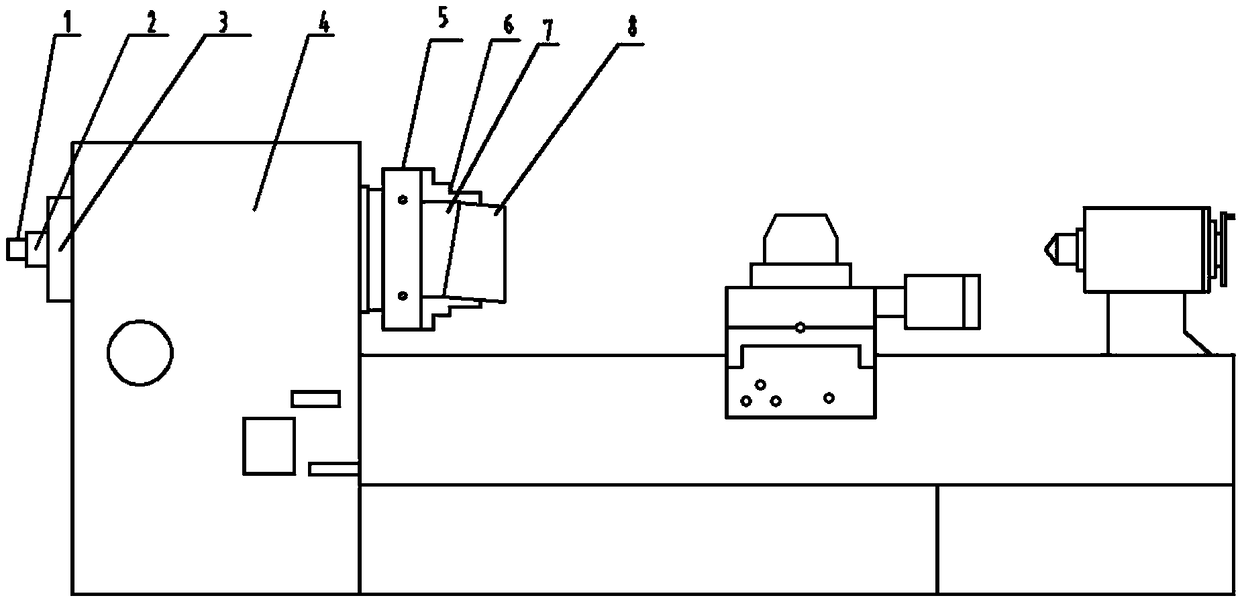
Figure 1 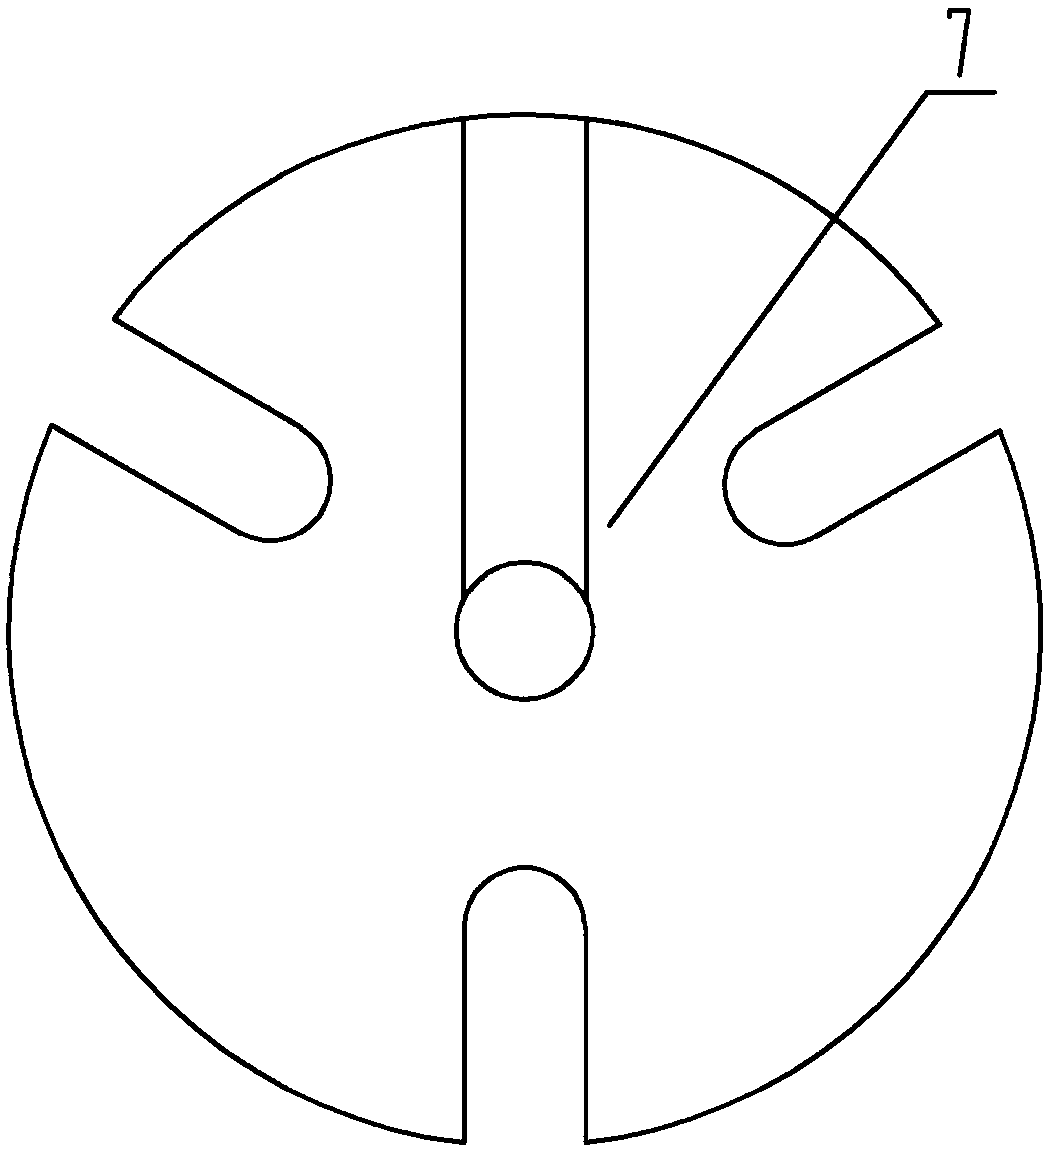
Figure 2
Abstract
Description
technical field
[0001] The invention relates to the technical field of valve gate processing, in particular to a fast clamping and positioning tool for processing gates. Background technique
[0002] With the rapid development of the processing and manufacturing industry, machining at home and abroad has developed to a relatively mature stage. The rapid clamping and positioning of workpieces on machine tools has become an indispensable part of machining. As machine tool technology develops in the direction of high speed, high efficiency and precision Driven by the drive, machine tool fixtures are also developing in the direction of high precision, high efficiency, general purpose and economical application.
[0003] 1) In order to improve the production efficiency of machine tools, there are more and more fixture products for continuous and efficient clamping. In order to reduce the clamping time of the workpiece, the quick clamping and positioning tooling is constantly bein...
Examples
Embodiment Construction
[0018] The technical solution of this patent will be further described in detail below in conjunction with specific embodiments.
[0019] see Figure 1-2 , a fast clamping and positioning tool for processing gates, including 10° tire tooling 7 and extended three claws 6, the 10° tire tooling 7 is detachably fixed on the three-jaw chuck 5 of the machine tool 4, and the extended three-jaw 6 It is fixed on the outside of the three-jaw chuck 5.
[0020] The machine tool 4 is a horizontal machine tool.
[0021] The 10° tire tooling 7 is fixed by the nut 2 and the stopper 3 after the screw rod 1 penetrates the main shaft hole of the machine tool 4 .
[0022] The gate 8 to be processed is clamped on the extended three claws 6 .
[0023] Specifically: the machine tool 4 is connected with a fixed three-jaw chuck 5, and the lengthened three-jaw 6 is installed on the three-jaw chuck 5, and the three-jaw chuck 5 and the lengthened three-jaw 6 are equipped with a 10° tire tooling 7; the...