
A sand-coated iron mold process for the production of driving wheel steel castings
A technology of sand-coating iron molds and steel castings, which is applied to the improvement of process efficiency, casting molds, and casting mold components. Effects of tensile strength, high impact toughness, and high productivity
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Patents(China)
- Current Assignee / Owner
- Publication Date
- 2022-01-04
Smart Images
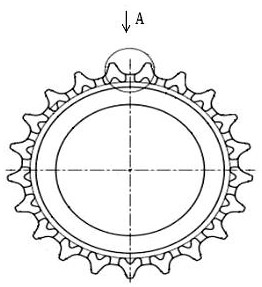
Figure 1 
Figure 2 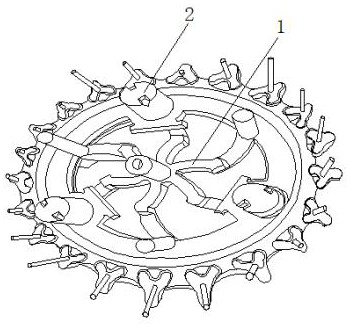
Figure 3
Abstract
Description
technical field
[0001] The invention relates to a sand-coating technology for iron molds, in particular to a sand-coating technology for iron molds used in the production of steel castings for driving wheels, and belongs to the technical field of sand-coating iron molds. Background technique
[0002] As our country enters the era of industrialization, in order to protect the health of the people, the country has continuously increased its efforts to protect the environment, and the management of "three wastes" has become more and more strict. The traditional cast steel production process has seriously affected the health of the people, and Cause serious pollution to the environment. For decades, the production of large and medium-sized steel castings in my country mostly adopts the traditional water glass sand molding process. Production of steel parts. However, due to the poor collapsibility of water glass sand and the low reuse rate of old sand, the shortcomings of the ol...
Examples
Embodiment 1
[0053] like Figure 1 to Figure 6 The iron mold sand-covering process shown for the production of driving wheel steel castings includes the following steps:
[0054] The first step, modeling,
[0055] 1) When molding, first place the sand box in the annealing furnace to preheat to 260°C, heat the mold to 180~220°C, and evenly open six inflow channels 1 of 40*40mm in * shape on the casting, and in Three heating risers 2 of Φ80*110mm are evenly arranged at the non-heating joints of the inner ring of the casting;
[0056] 2) After the mold and the sand box are tightly attached, the sand shooting is ready to start, the sand shooting pressure is adjusted to 0.55~0.6MPa, and the mold locking pressure is adjusted to 8~8.5MPa;
[0057] 3) Add 500kg of coated sand special for casting steel into the sand shooting bucket, and do a good job of screening, filtering and dust removal, and carry out the sand shooting operation. The gas volume is 80,000ml, the pouring time for each case is ...