
Design method of middle blank and prefabricating blank during conical shell forgeable piece forming process
A conical cylinder and forming process technology, applied in the field of forging, can solve the problems of reducing the machining allowance of conical cylinder forgings, the accuracy of machining dimensions cannot be guaranteed, and shortening the production cycle of products, so as to reduce research costs and shorten the production cycle , The effect of shortening the product production cycle
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Patents(China)
- Current Assignee / Owner
- Publication Date
- 2010-07-21
Smart Images
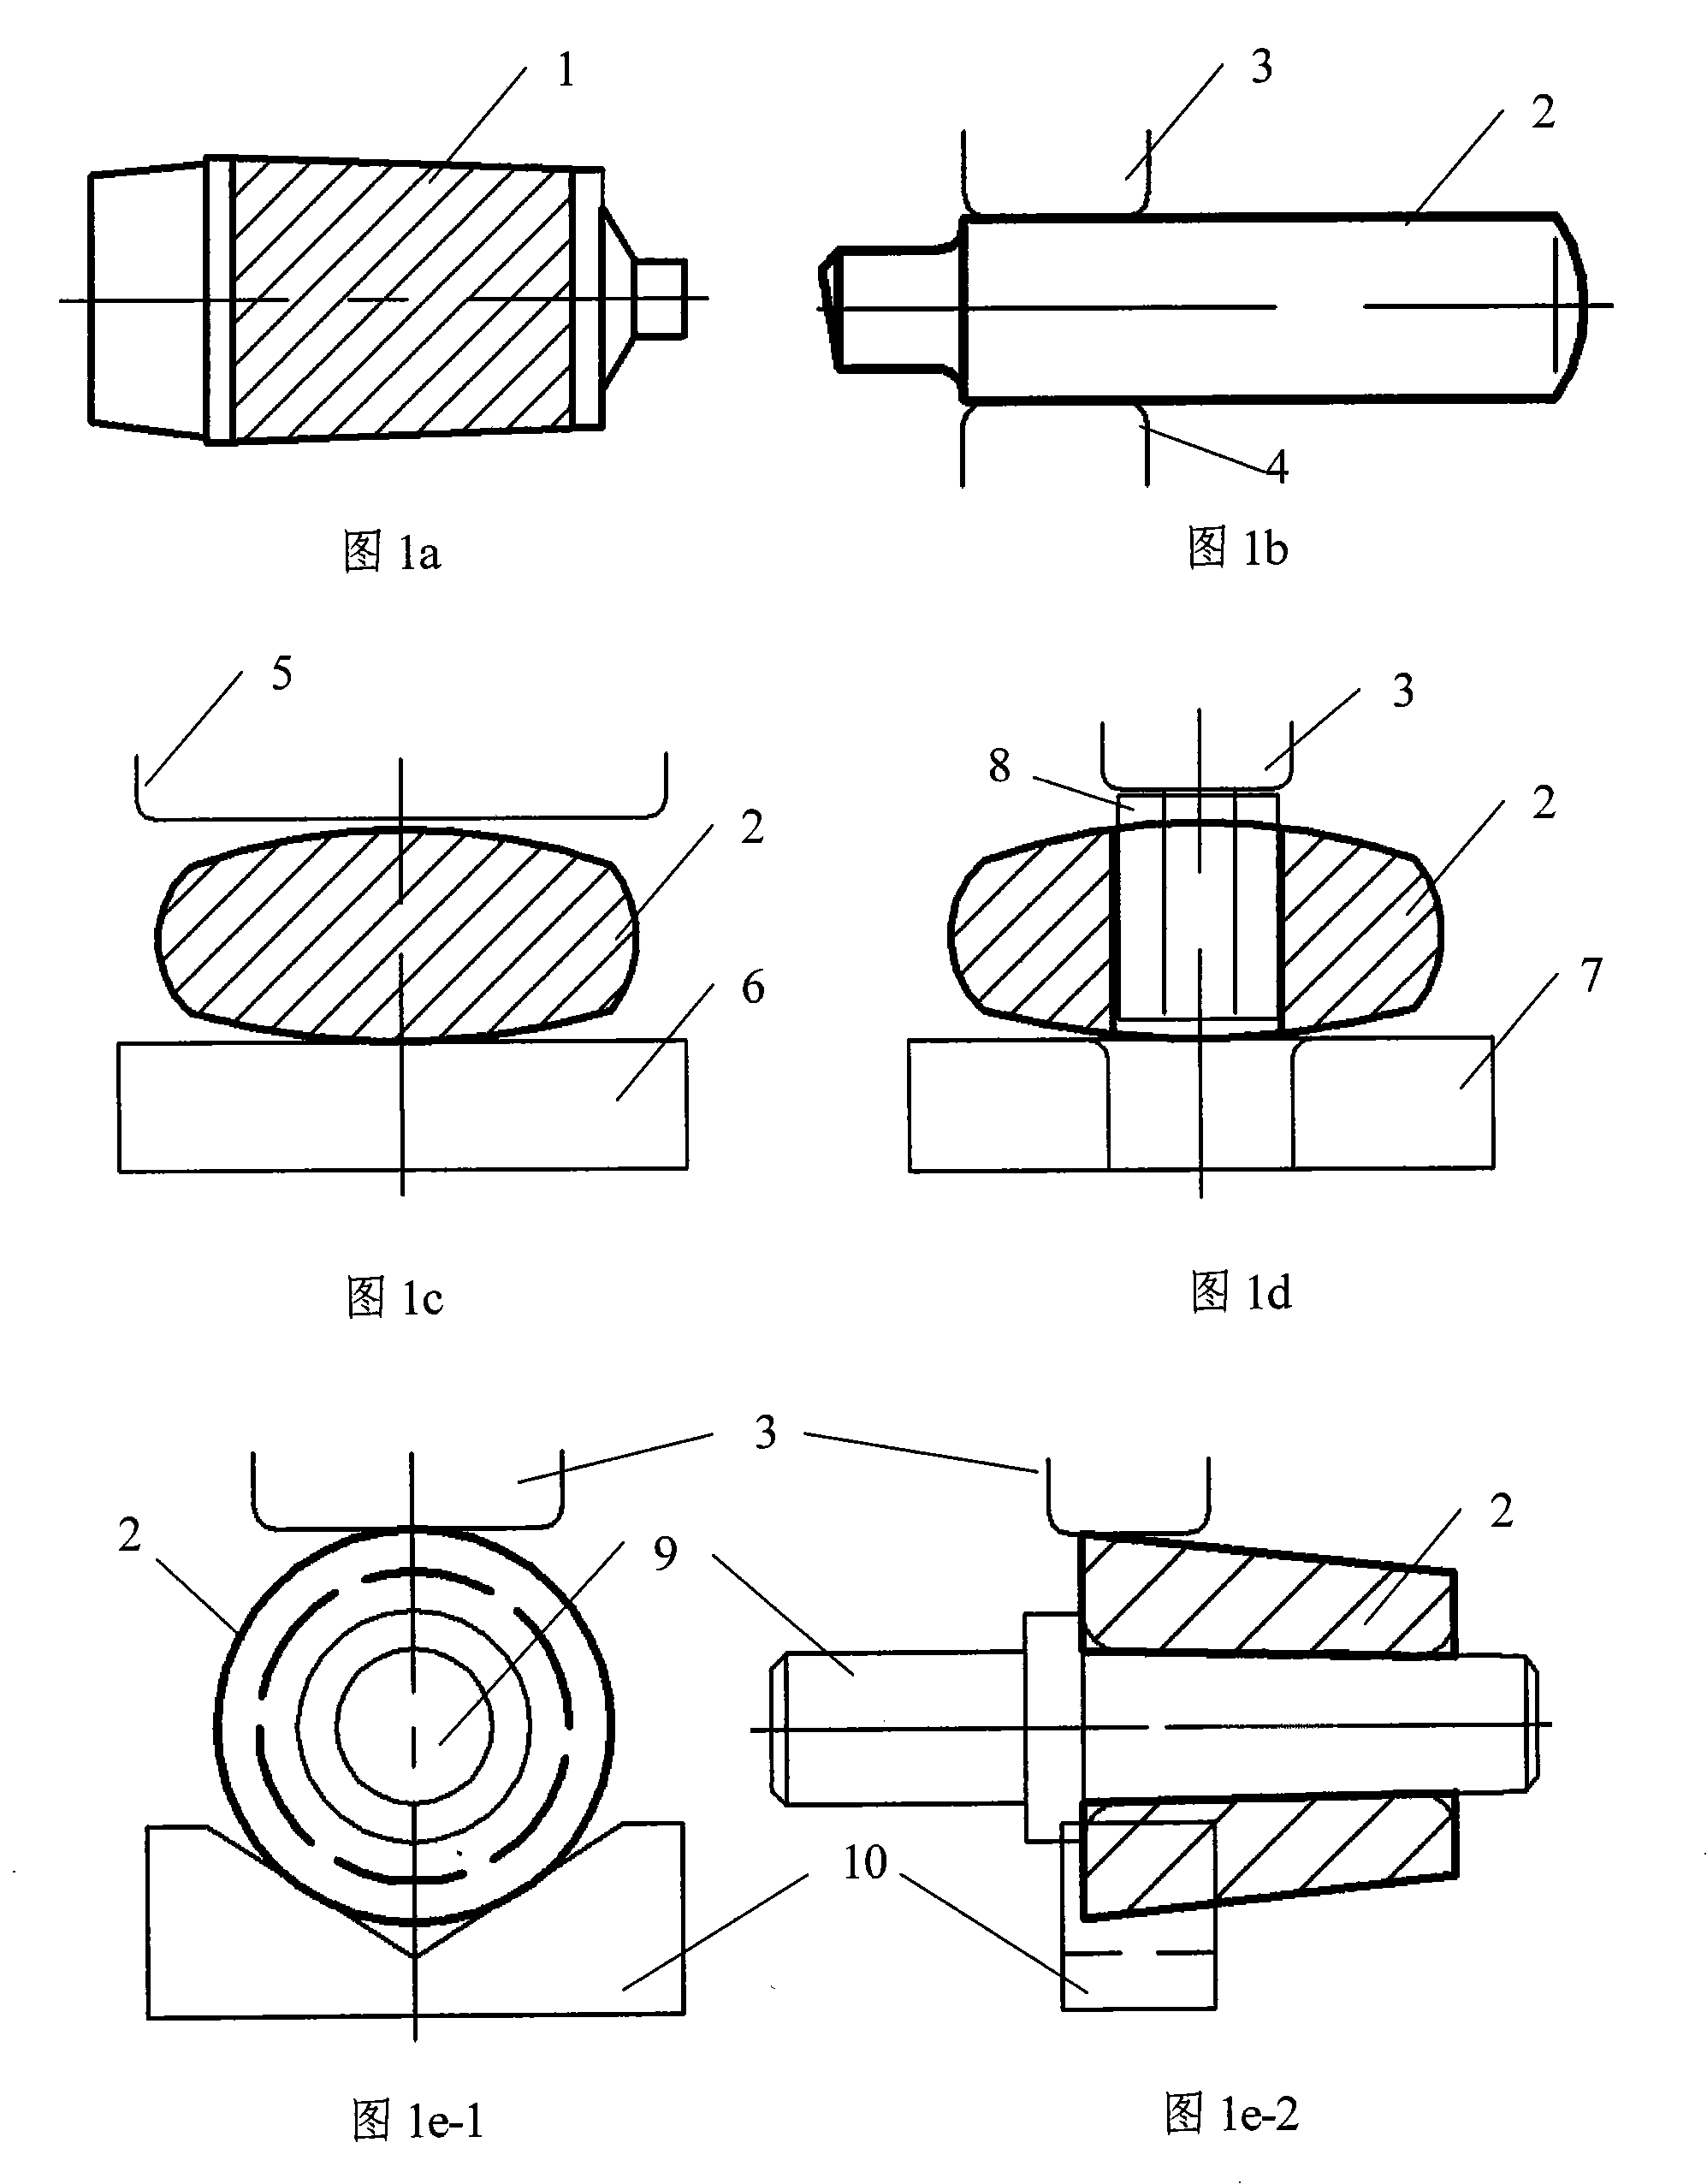
Figure 1 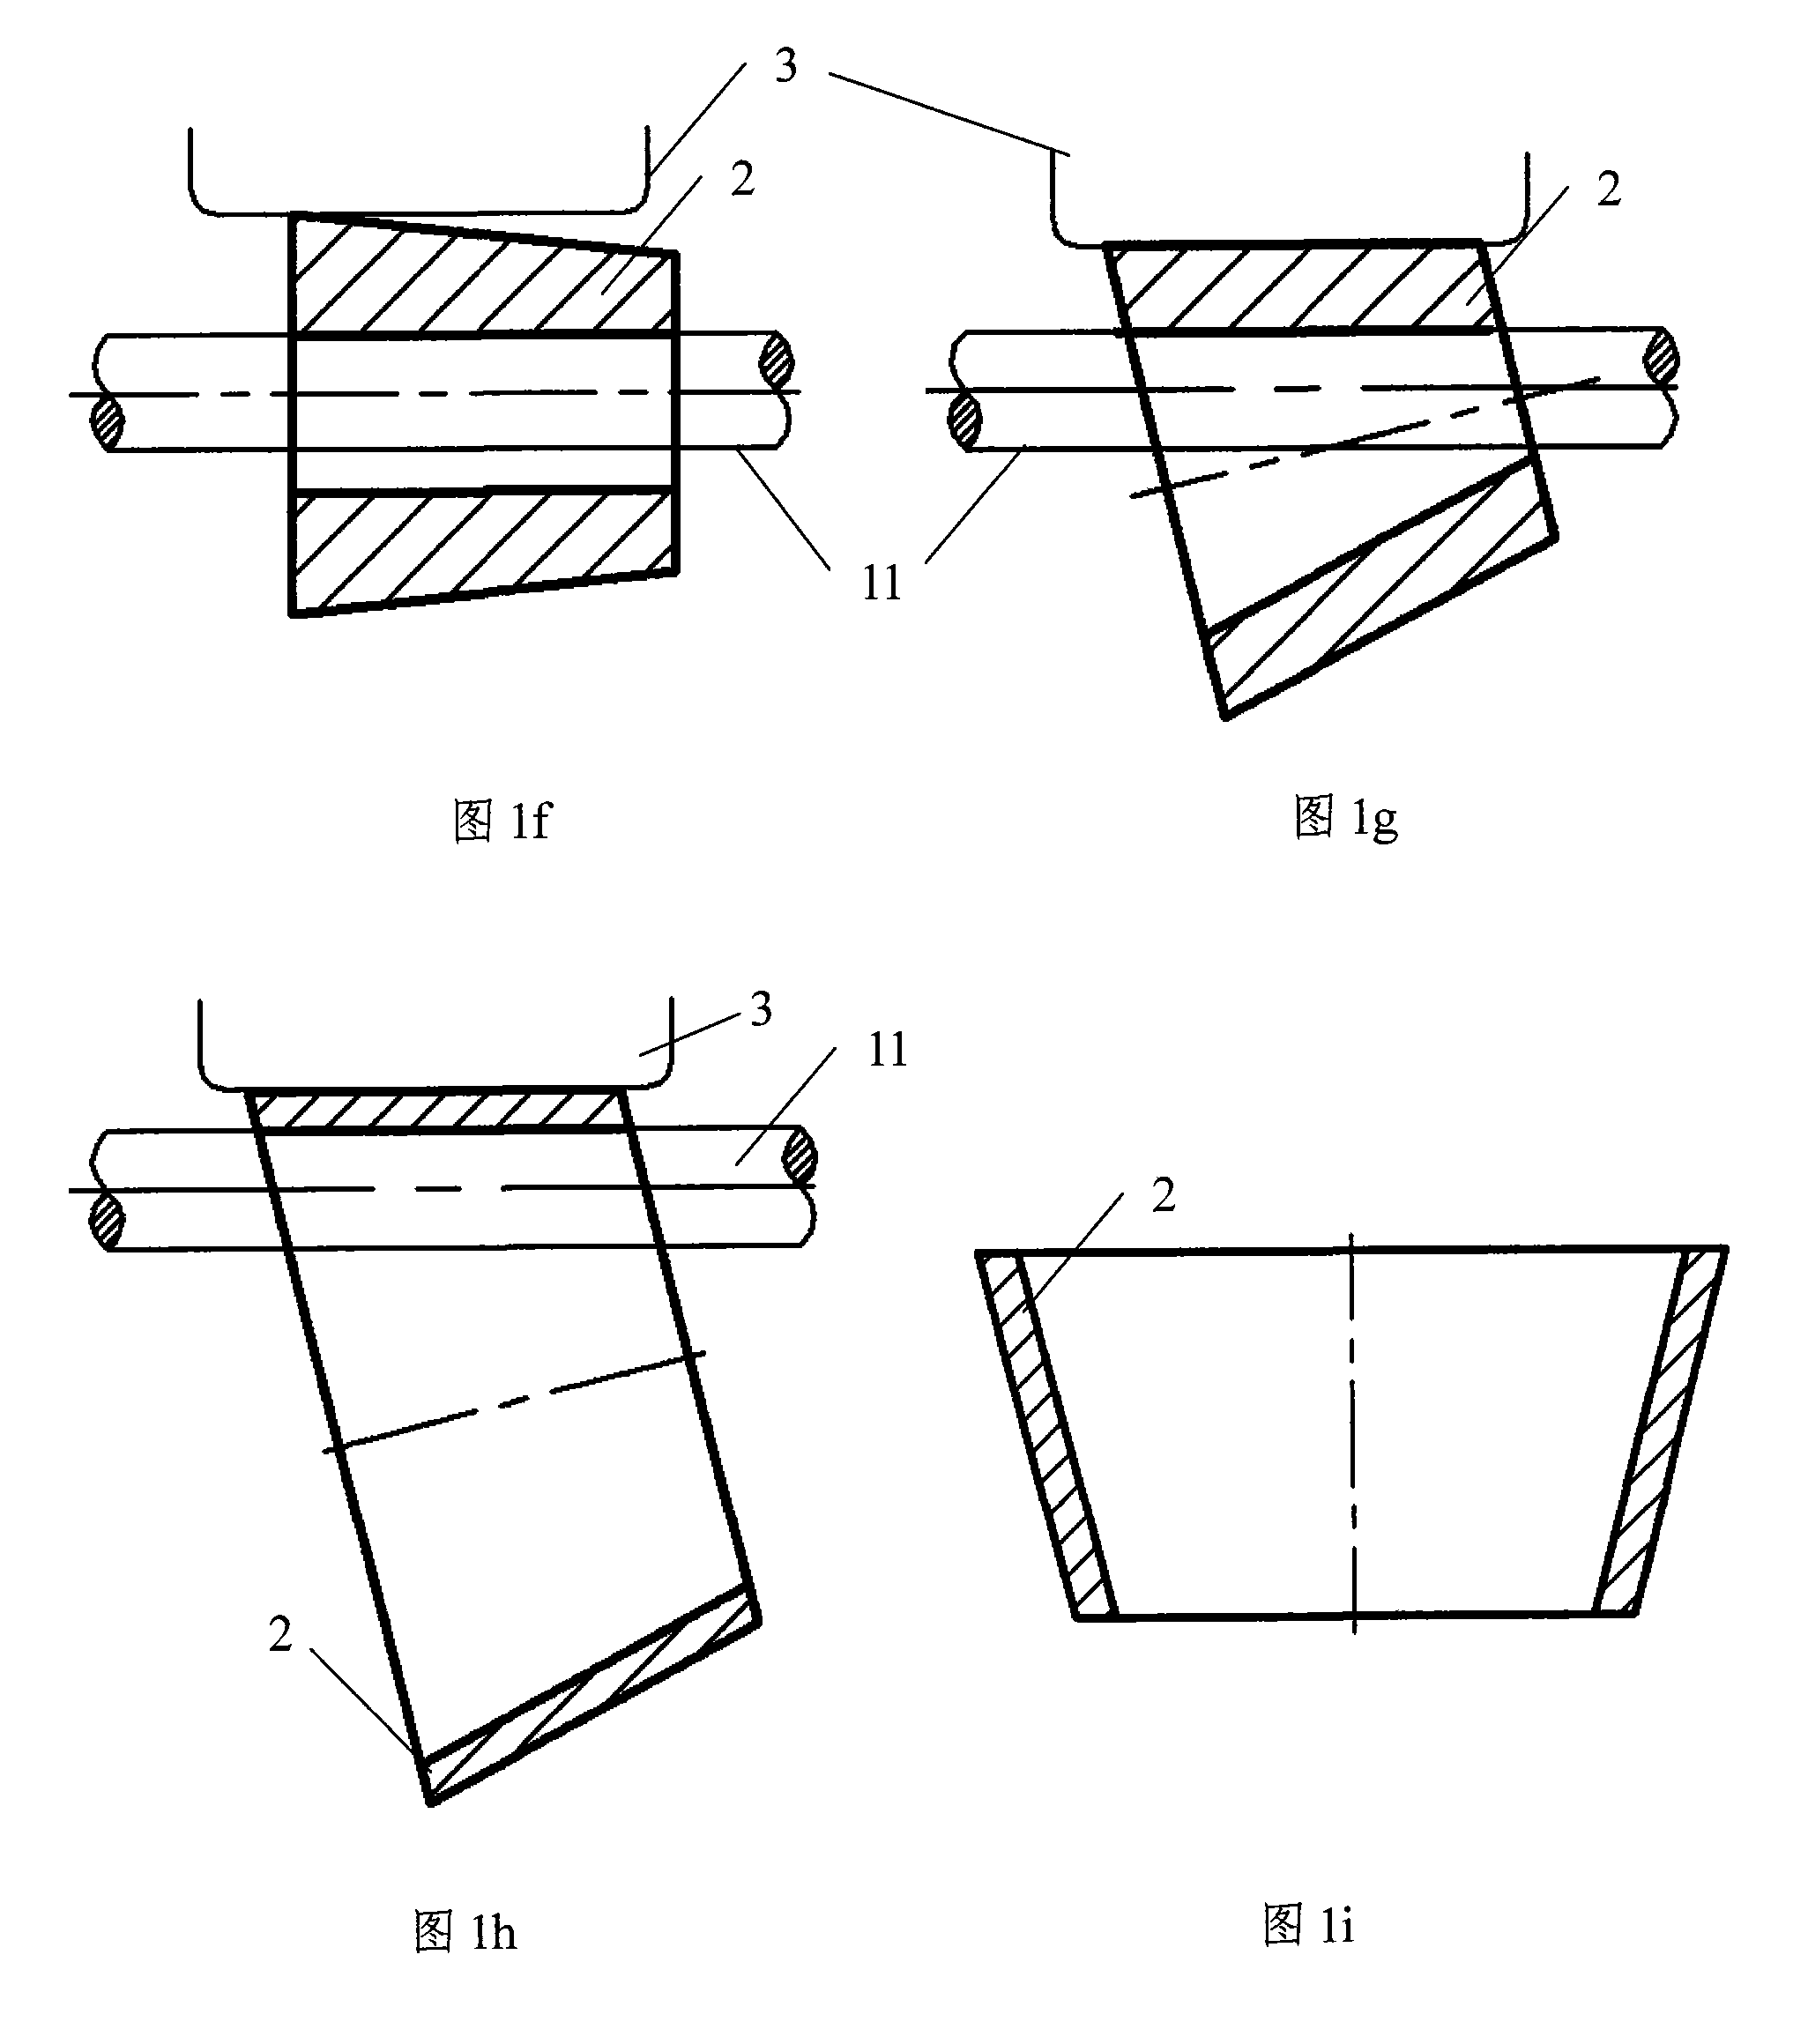
Figure 2 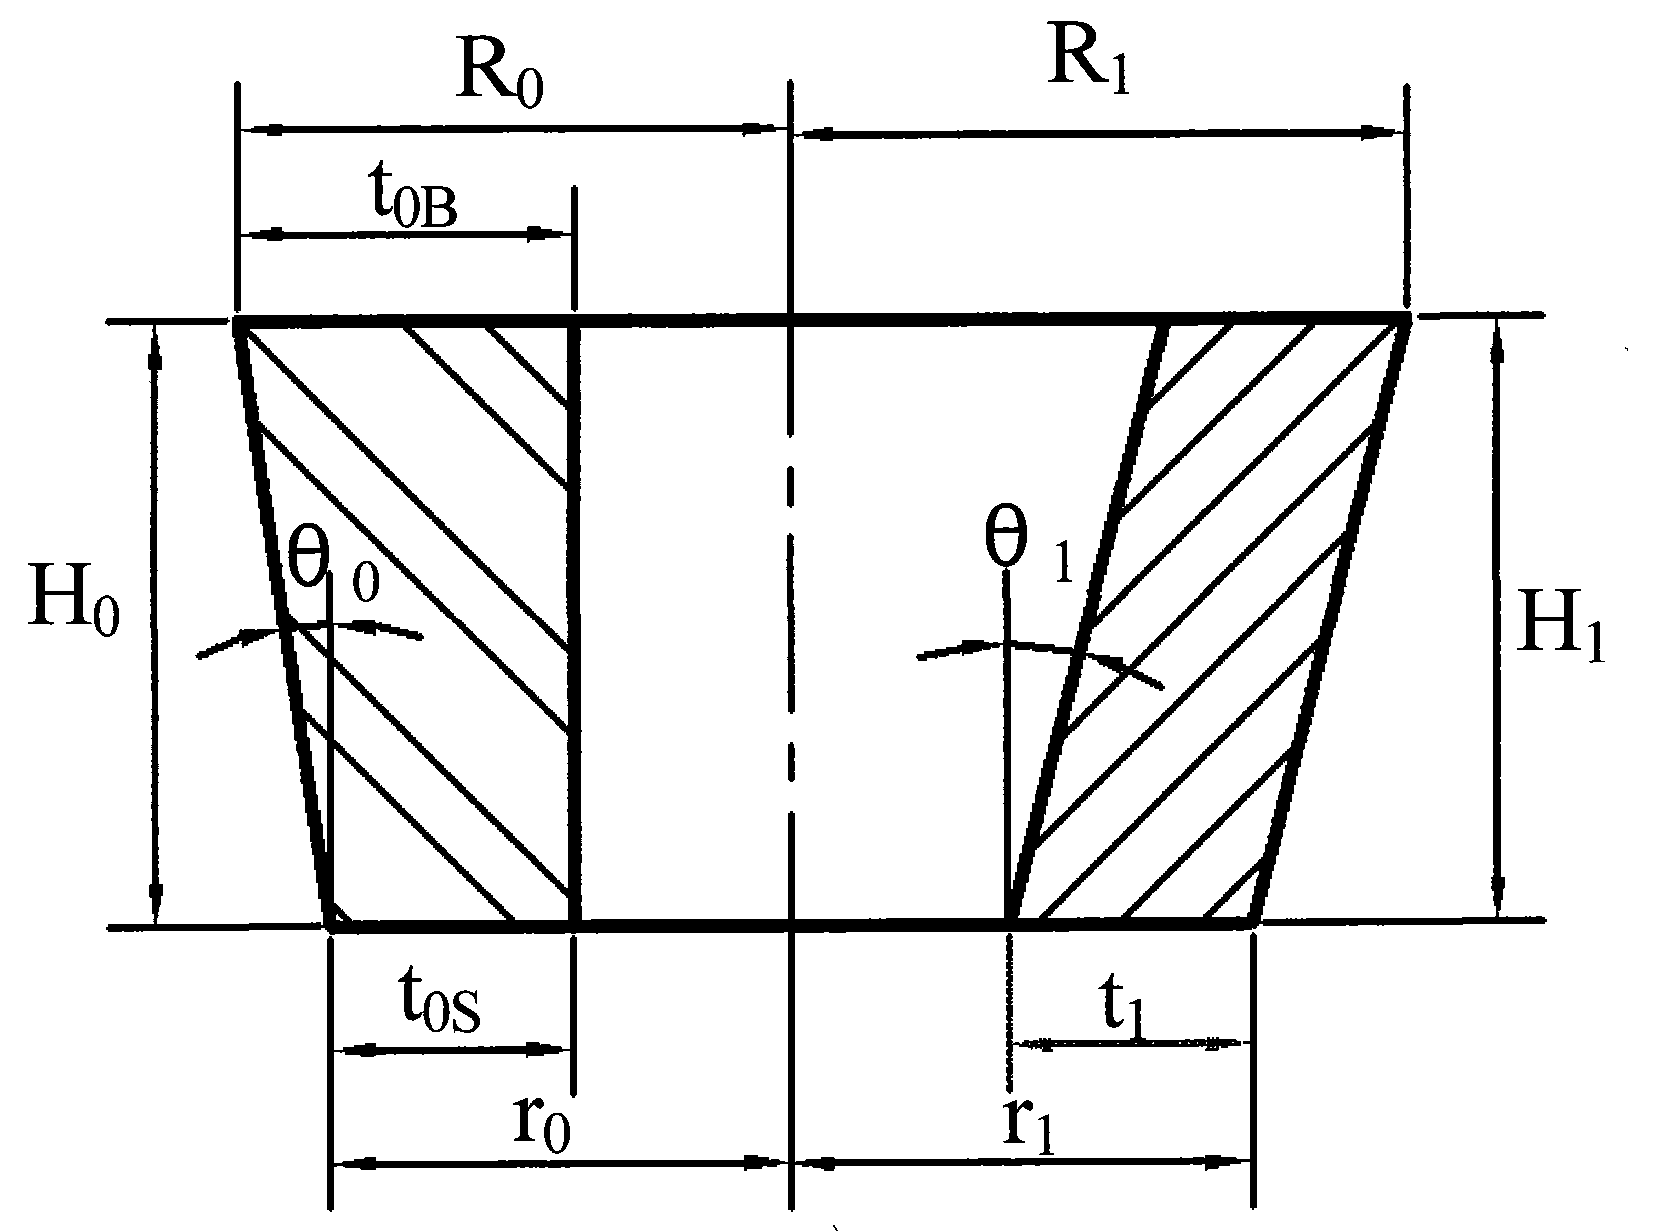
Figure 3
Abstract
Description
technical field
[0001] The invention belongs to the field of forging, specifically a design method for an intermediate billet and a preform in the forming process of a conical cylinder forging of a nuclear power and hydrogenation reactor, which is suitable for forming a conical cylinder forging of a nuclear power and hydrogenation reactor Process design and manufacturing process. Background technique
[0002] The conical cylinder is one of the most important parts of nuclear power evaporators and petrochemical hydrogenation reactors. Forgings often weigh more than 100 tons and have a diameter of more than 5 meters. Due to their special service environment, there are extremely high impacts on the structure and performance of forgings. It is very difficult to manufacture such forgings. At present, most of such forgings in my country rely on imports, and sometimes they cannot be bought even with money, which seriously restricts the development of my country's nuclear power and p...
Examples
Embodiment
[0114] The forged part in this embodiment is a pilot test forging of a conical cylinder of a certain type of nuclear power evaporator, and the inner diameter of the large end of the final forging is required to be r 2 =815mm, outer diameter R 2 =1000mm, wall thickness t 2 =185mm, height H 2 =1350mm, taper θ 2 = 11.1°. take k 1 =1.07,k 2 = 1.05, δ = 1.65.
[0115] In the process of reaming from the intermediate billet to the final forging, it can be obtained from the formula (4):
[0116] h 1 =H 2 / k 2 =1350 / 1.05=1286mm
[0117] From formula (12):
[0118] t 1 =δ·t 2 =1.65×185=305mm
[0119] From the formula (6):
[0120] R 1 = t 1 2 + k 2 ( 2 R 2 t ...