
Large acceleration control method for ensuring finish rolling temperature
A technology of acceleration control and finish rolling temperature, applied in temperature control, roll speed control, metal rolling, etc., can solve the problems of affecting rolling rhythm, increasing plastic deformation heat, unfavorable finish rolling temperature control, etc., to ensure temperature stability performance, improve the effect of rolling rhythm
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Applications(China)
- Current Assignee / Owner
- Publication Date
- 2017-10-24
Smart Images
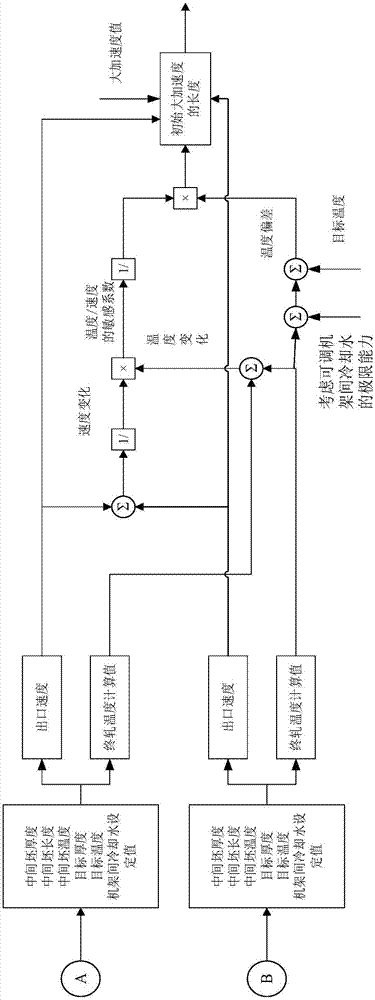
Figure 1 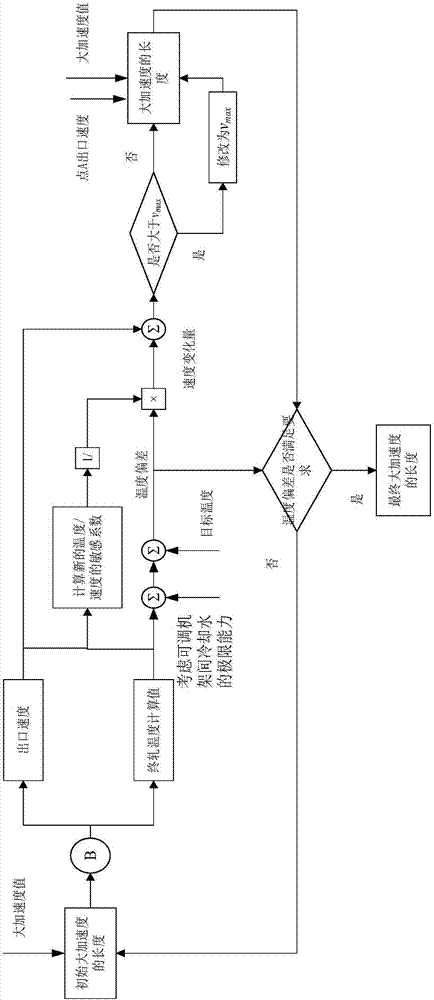
Figure 2 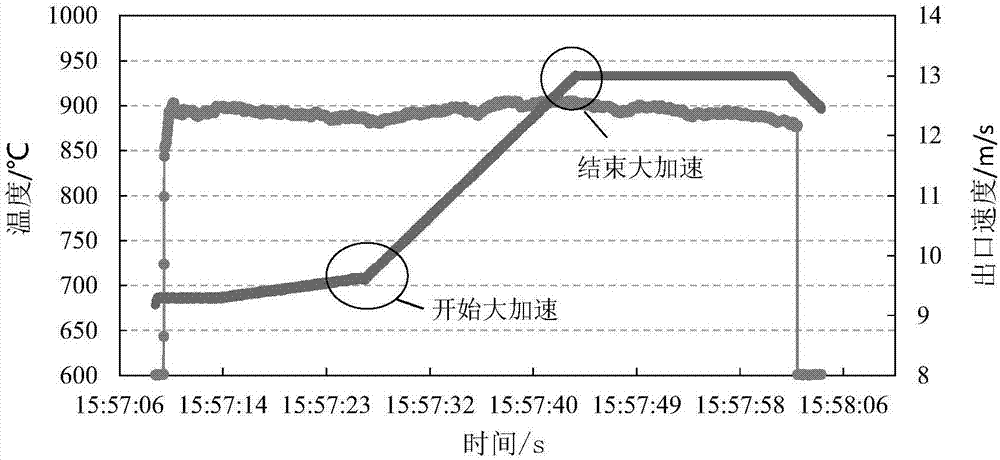
Figure 3
Abstract
Description
technical field
[0001] The invention belongs to the field of temperature control in the rolling process, and in particular relates to a large-acceleration control method for ensuring the finish rolling temperature. Background technique
[0002] The finish rolling temperature is one of the key factors in the quality control of hot-rolled strip, which not only affects the microstructure and properties of the rolled strip, but also affects the metallographic structure and mechanical properties of the rolled strip. Therefore, in order to realize the temperature control of the finish rolling, it is necessary to ensure that the strip head reaches the target temperature and the uniformity of the finish rolling temperature over the entire length of the strip to meet the physical properties of the strip throughout the length.
[0003] Due to the different residence time of the strip steel in the air, the finish rolling temperature of the strip steel is different in the whole length. ...
Examples
Embodiment Construction
[0033] The embodiment of the present invention provides a large-acceleration control method to ensure the finish rolling temperature, which uses actual process data to calculate the length of the large-acceleration region of the strip, and is applied to the field of temperature control in the rolling process. Select steel type SDC01, specification 3.0*1570mm, take large acceleration as an example, the process parameters are shown in Table 1, and the description is as follows.
[0034] Table 1 Process parameters of each pass of finish rolling
[0035]
[0036] (1) Determine two points in the length direction of the intermediate billet. The determination principle is: when coiling and loading, the position in the length direction of the intermediate billet is point A, which is 9.043m away from the head of the intermediate billet; The position l is determined as point B, and the initial value of l is 3m, which is 12.043m from the head position of the intermediate billet;
[0...