
Machining process of wind power bearing sealing rubber strip
A technology of bearing sealing and processing technology, which is applied in the field of vulcanization molding processing technology, can solve the problems that the density of the rubber strip cannot meet the requirements, cannot fully meet the product use requirements, and poor quality stability, so as to meet the requirements of density, compression performance and Improve wear resistance, meet the effect of uniformity and consistency
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Applications(China)
- Current Assignee / Owner
- Publication Date
- 2011-09-14
Smart Images
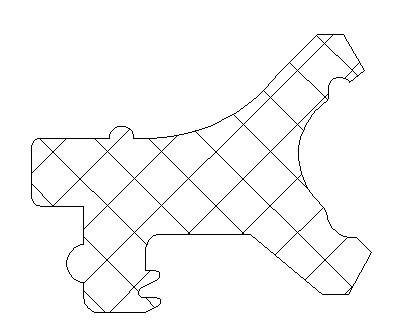
Figure 1 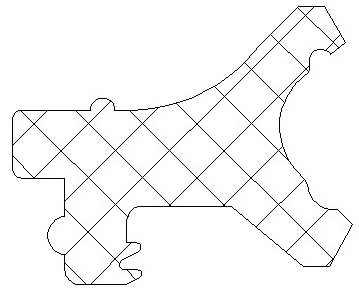
Figure 2
Abstract
Description
technical field
[0001] The invention relates to a vulcanization molding processing technology, in particular to a processing technology of a wind power bearing sealing rubber strip. Background technique
[0002] At present, wind power bearing sealing strips are widely used in wind power main engine yaw bearings and pitch bearings, and play a sealing role in key parts. Whether it is yaw or pitch, the following requirements need to be met:
[0003] ① There is a certain pressure on the lubricating grease inside the bearing, which requires a certain strength and stiffness for the key lip part of the sealing strip.
[0004] ②The fan rotates with the wind direction at high altitude, and the blades will rotate continuously as long as the wind force permits, which requires the sealing strip to have considerable wear resistance.
[0005] ③ After the sealing strip is embedded in the sealing position of the bearing, it has been working in a compressed state, which requires that the d...
Examples
Embodiment Construction
[0023] The present invention will be described in further detail below in conjunction with the accompanying drawings and embodiments.
[0024] A processing technology for wind power bearing sealing strips, the material is oil-resistant and weather-resistant rubber, the hardness of the rubber is 70~75°Shore A, the process steps are as follows:
[0025] a. Filter the mixed rubber material with a filter to ensure that the rubber material is free of impurities;
[0026] b. Preform the rubber material with the mouth of the extruder to ensure the size of the rubber material so as to meet its weight requirements;
[0027] c. Preheat the preformed mixed rubber to increase its fluidity;
[0028] d. Draw the preformed rubber to each cavity with a jig and place it neatly;
[0029] e. Close the mold and start vulcanization molding;
[0030] f. Trim the vulcanized and formed product, remove the burr to make a wind power bearing sealing strip that meets the assembly requirements.
[003...