
Car body underframe assembly and its welding process
A welding process and underframe technology, applied in the field of rail transit car body manufacturing system, can solve problems such as wrong assembly, missing assembly, cumbersome process, etc., achieve the effects of reducing the amount of adjustment, cleaning the site, and improving production efficiency
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Patents(China)
- Current Assignee / Owner
- Publication Date
- 2022-05-10
Smart Images
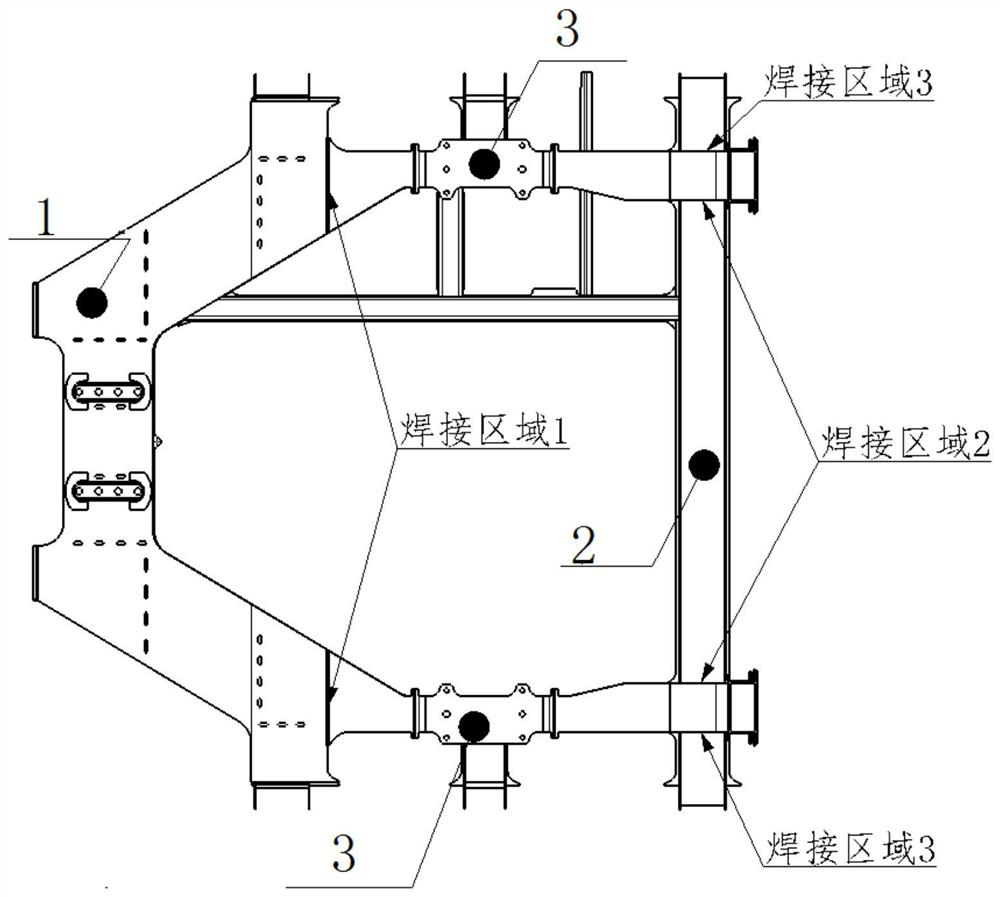
Figure 1 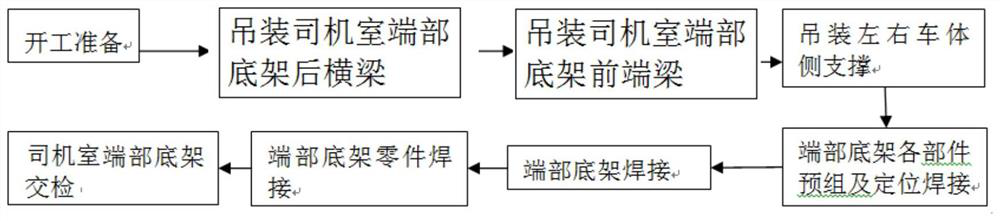
Figure 2 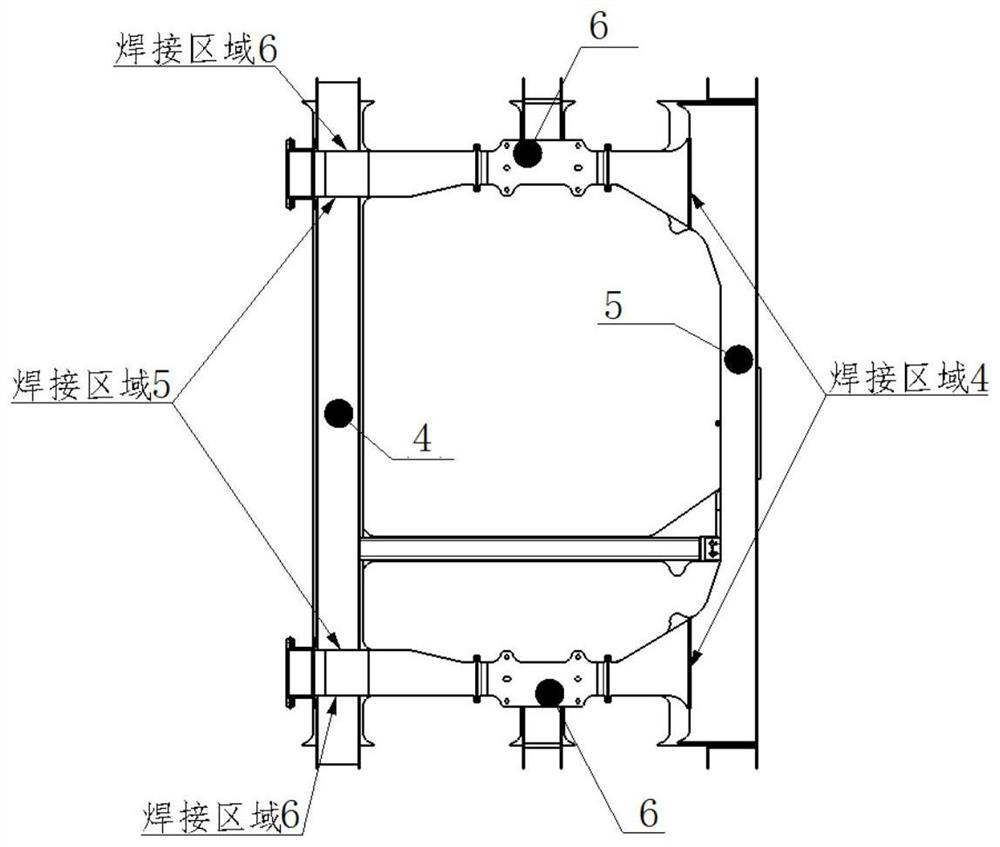
Figure 3
Abstract
Description
technical field
[0001] The invention relates to a rail transit car body manufacturing system, which is applied to the assembly and welding work of the car body part chassis, in particular to a car body chassis assembly and a welding process thereof. Background technique
[0002] The underframe of the car body is a steel structure underframe made of high-strength carbon structural steel material, which is spliced by blanking and processing of plates. The weight of the whole underframe assembly is 1.4 tons, and the thickness of the used plate is 3-4.8mm, so the amount of used plate is very large.
[0003] The existing technology is to directly carry out tailor welding on the assembly welding tooling. The plates at the tailor welding site are chaotic, and it is easy to have wrong and missing installation. For the whole welding process, the process is complicated, the efficiency is low, and the quality is poor. The requirements for welding personnel are also particularly high...
Examples
Embodiment Construction
[0033] The present invention will be further described below in conjunction with the accompanying drawings and embodiments.
[0034] like Figure 1 to Figure 2 As shown, the assembly welding process of the cab end chassis 7 includes the following processes:
[0035] 1) Hoist the components of the underframe 7 at the end of the cab (the rear beam 2 at the end of the cab, the front beam 1 at the end of the cab and the side support 3) to the tooling by means of a crane, and ensure that the components are aligned with the center line of the tooling Or parallel, pre-clamped by positioning clamping device; 2) Measure and adjust the size of the bottom frame at the end of the driver's cab. Positioning welding can only be performed after the size is qualified. The bottom frame at the end of the cab needs to confirm that the size meets the design requirements.
[0036] Complete the welding work between the various components in the order of assembly: first complete the welding of the r...