
A kind of low yield ratio high plastic ultrafine grain high strength steel and its manufacturing method
A technology with ultra-fine grains and low yield ratio, applied in the field of high-strength steel, can solve unsolved problems such as yield ratio, and achieve the effects of stable production process, low cost and low yield ratio
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Applications(China)
- Current Assignee / Owner
- Publication Date
- 2011-12-14
- Estimated Expiration
- Not applicable · inactive patent
Smart Images
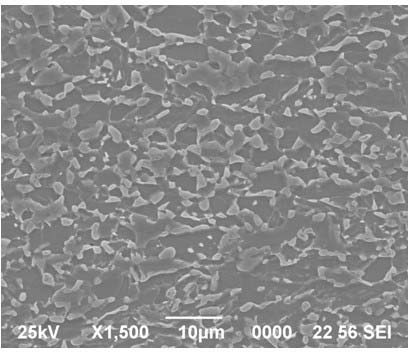
Figure 1 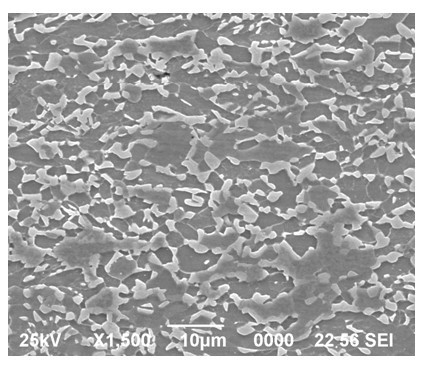
Figure 2 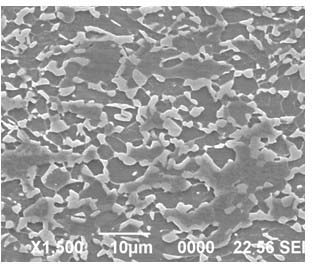
Figure 3
Abstract
Description
technical field
[0001] The invention relates to a high-strength steel, in particular to a high-strength steel with low yield ratio, high plasticity, ultra-fine grain and a manufacturing method thereof. Background technique
[0002] In the 21st century, steel is still the dominant structural material, and no material can completely replace steel. With the development of society and economy, the iron and steel industry is facing three major pressures: saving resources, saving energy, and protecting the environment. Therefore, improving steel quality, reducing costs, developing human-friendly steel materials, and greatly improving their comprehensive mechanical properties have become the main directions of steel material research. Among them, the low-cost production of fine-grained high-strength steel using thermomechanical controlled rolling technology (TMCP) and deformation-induced ferrite transformation technology (DIFT) is the development direction of the current metallurg...
Examples
Embodiment Construction
[0020] A low yield ratio high plastic ultrafine grain high strength steel, according to the production process of the present invention, the actual chemical composition of the steel of the present invention is smelted and rolled as shown in Table 1.
[0021] A method for manufacturing ultra-fine-grained high-strength steel with low yield ratio and high plasticity, the specific requirements of the manufacturing method are as follows:
[0022] Rolling process: controlled rolling and controlled cooling process is adopted, the heating temperature of the continuous casting slab before rolling is 1180 ℃ ~ 1200 ℃; two-stage controlled rolling is adopted in the austenite recrystallization zone and austenite non-recrystallization zone, and each pass of rough rolling The secondary reduction rate is 10-15%, the rough rolling final rolling temperature is 1000-1050℃, and the rough rolling is 1.6-2.0 times the thickness of the finished product. The intermediate billet is 1.6-2.0 times the th...