
3C product charging connector shell highlight process
A charging interface and product technology, which is applied in the direction of manufacturing tools, metal processing equipment, grinding/polishing equipment, etc., can solve problems such as increased cost, dimensional fluctuations, cumulative tolerances of manufacturing processes, etc., to reduce product production costs and improve dimensional stability , The effect of reducing material loss
Patent Information
- Authority / Receiving Office
- CN · China
- Current Assignee / Owner
- Publication Date
- 2018-07-24
Smart Images
Figure 1 
Figure 2 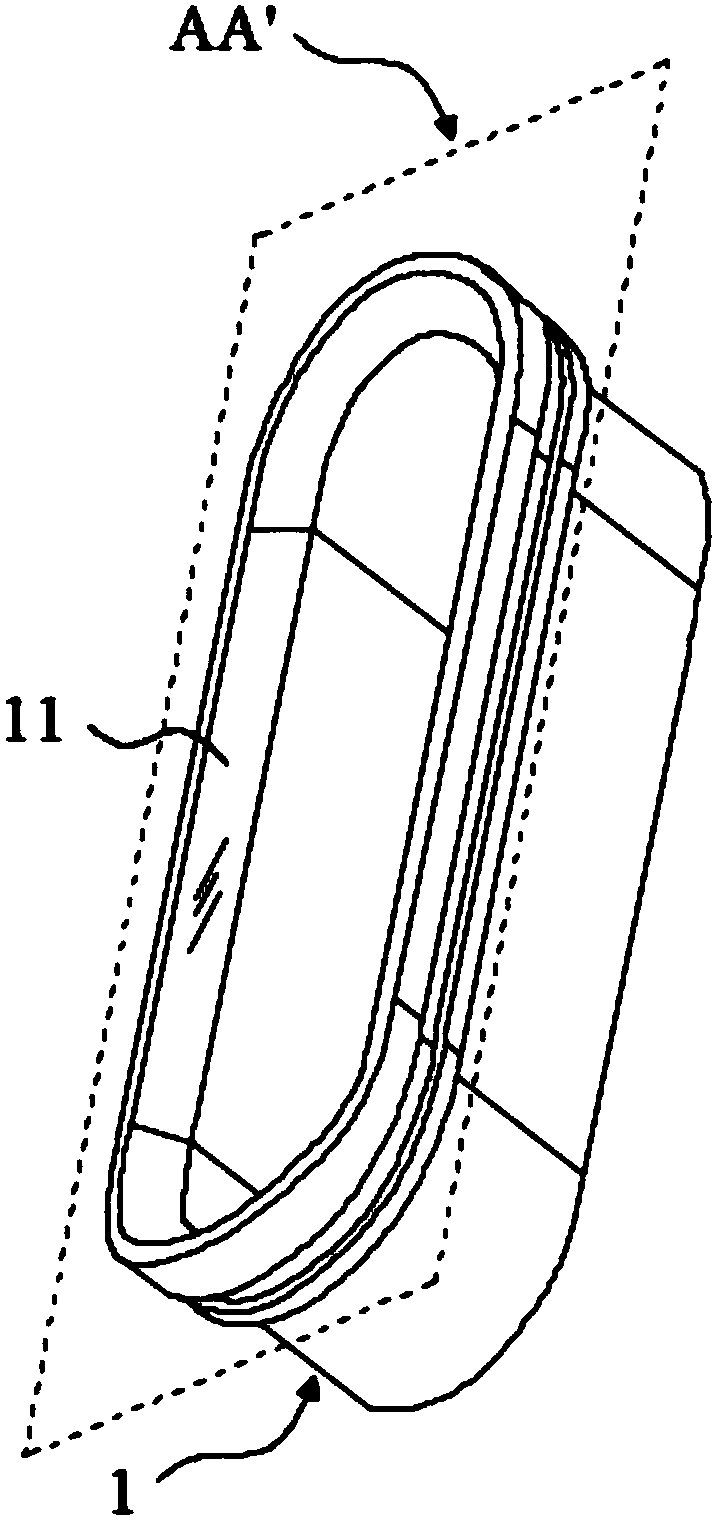
Figure 3
Abstract
Description
technical field
[0001] The invention relates to the technical field of processing parts of 3C products, in particular to a high-gloss process for charging interface shells of 3C products. Background technique
[0002] like figure 1 As shown, the charging interface of 3C products such as mobile phones and tablet computers is provided with a charging interface shell 1, and the inner side of the entrance of the charging interface shell 1 has a high-gloss surface 11, which is the key processing part of the high-gloss process. Usually, the width of the inlet of the charging interface case 1 is not more than 2 mm. Figure 5 The processing flow of the charging interface case 1 in the prior art is schematically given. In the prior art, the charging interface shell 1 with preset shape and size processed by CNC numerical control equipment is ground in a vibration grinder to remove residual burrs after CNC processing, and after cleaning and drying, sandblasting, cleaning and drying ...
Examples
Embodiment 1
[0065] Add 6kg of spherical chrome corundum with a specification of Φ7mm and charging interface shell 1 formed by 2400 CNC equipment into the grinding barrel of the rolling grinder, and rotate at a constant speed of 1400 rpm for 3 minutes. After the ground charging interface case 1 is cleaned, dried and sand-blasted, the above-mentioned charging interface case 1 and 6 kg of spherical zirconia grinding stones with a specification of Φ0.8 mm are added to the grinding barrel of the rolling mill together to Rotate at 1700 rpm for 5 min. After grinding, the obtained charging interface case 1 is cleaned and dried, and finally a finished charging interface case 1 with a high-gloss and high-gloss surface 11 is obtained.
Embodiment 2
[0067] Add 6kg of spherical chrome corundum with a specification of Φ8mm and the charging interface shell 1 formed by 3000 CNC numerical control equipment into the grinding barrel of the rolling grinder, and rotate at a speed of 1500 rpm for 4 minutes. After the ground charging interface case 1 has been cleaned, dried and sand-blasted, the above-mentioned charging interface case 1 and 6 kg of spherical zirconia grinding stones with a specification of Φ1 mm are added to the grinding barrel of the rolling mill, and the grinding process is performed at 1800 rpm. Rotate evenly for 8 minutes at a speed of 1 / min. After grinding, the obtained charging interface case 1 is cleaned and dried, and finally a finished charging interface case 1 with a high-gloss and high-gloss surface 11 is obtained.
Embodiment 3
[0069] Add 6 kg of spherical chrome corundum with a specification of Φ9 mm and charging interface shell 1 formed by 3600 CNC numerical control equipment into the grinding bucket of the rolling grinder, and rotate it at a speed of 1600 rpm for 5 minutes. After the ground charging interface shell 1 is cleaned, dried and sandblasted, the charging interface shell 1 and 6 kg of spherical zirconia grinding stones with a specification of Φ1.2 mm are added to the grinding bucket of the rolling grinder to Rotate evenly for 10 minutes at a speed of 1900 rpm. After grinding, the obtained charging interface case 1 is cleaned and dried, and finally a finished charging interface case 1 with a high-gloss and high-gloss surface 11 is obtained.