
Stirring head and its welding process for friction stir welding of aluminum alloy with large gap
A friction stir welding and stirring head technology, which is applied in welding equipment, metal processing equipment, manufacturing tools, etc., can solve the problems of inconsistent matching gaps of battery boxes, easy to produce defects, etc., to reduce assembly accuracy requirements, promote metal flow, The effect of broadening application prospects
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Patents(China)
- Current Assignee / Owner
- Publication Date
- 2022-03-29
Smart Images
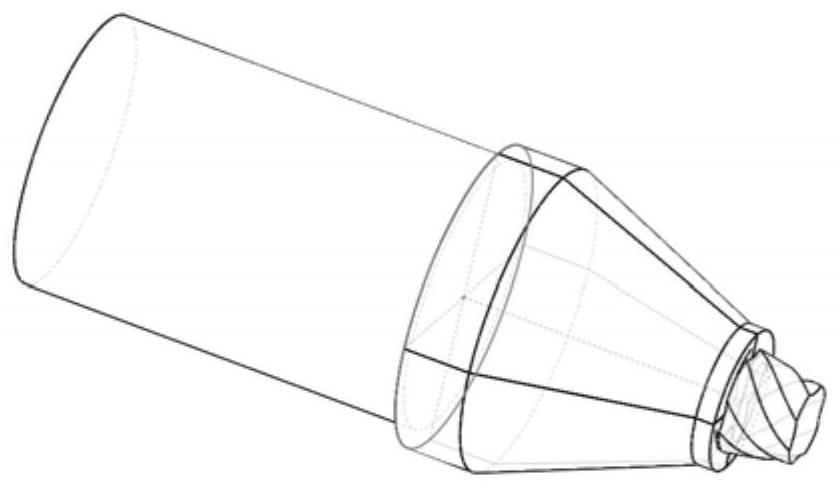
Figure 1 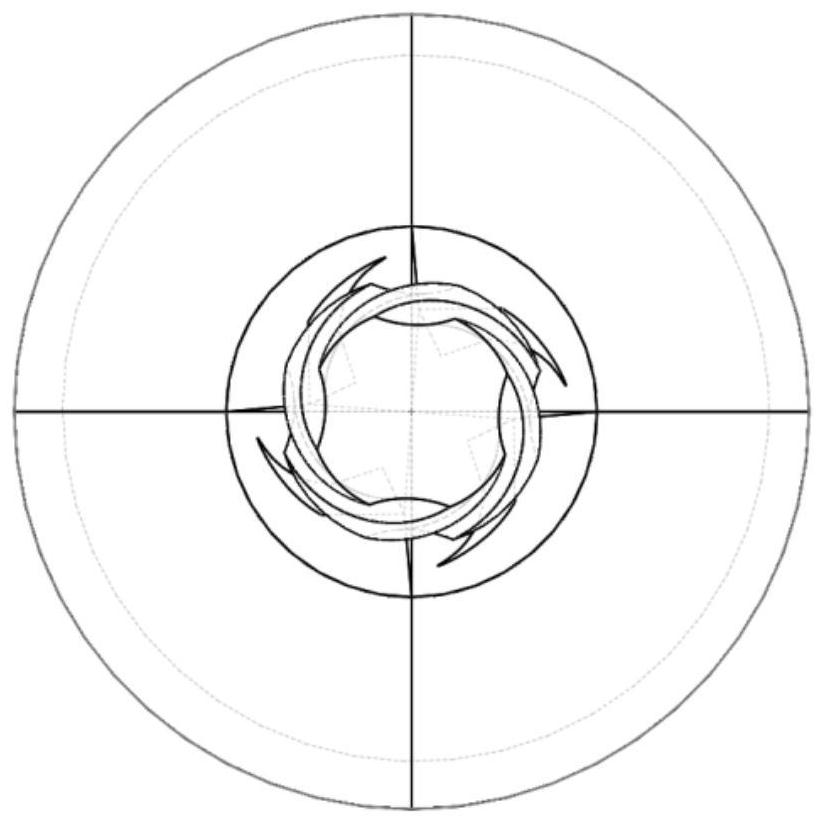
Figure 2 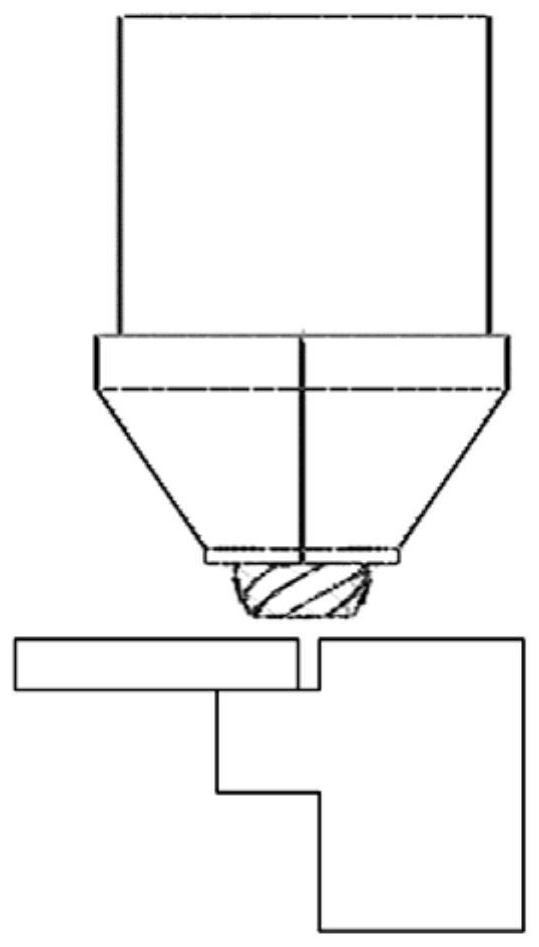
Figure 3
Abstract
Description
technical field
[0001] The invention relates to the field of thin-plate aluminum alloy welding for battery boxes of new energy vehicles, in particular to a stirring head for friction stir welding of large-gap thin-plate aluminum alloys and a welding process thereof. Background technique
[0002] According to the principles of automotive engineering, the influence of the weight of the car body on power consumption is considered. At present, the battery box of new energy vehicles is mainly made of aluminum alloy. Considering the box structure, welding process, post-weld deformation and other factors comprehensively, the friction stir welding is determined as the main welding method for the box bottom plate. Limited by the processing accuracy of the bottom plate and the influence of the bending process of the frame, during the assembly process of the bottom plate and the frame, the matching gap between the bottom plate and the frame is often not uniform, and there is a situati...
Examples
Embodiment 1
[0041] The thickness of the plate is 2.5mm, the distance between the shoulders of the stirring head is 10mm, the diameter of the stirring needle is 8mm, the ratio of the diameter of the stirring needle to the diameter of the shoulder is 0.8, the length of the stirring needle is 2.3mm, and the distance between the shoulders of the stirring head is 10mm. There are 3 counterclockwise table-building vortex patterns, and 2 spiral grooves are arranged on the stirring needle.
[0042] The specific steps are as follows:
[0043] Step 1: Clean the 2.5mm thick aluminum alloy with alcohol to clean the surface of the metal plate and the oil and oxides on the interface and other substances that hinder the welding process. Place the cleaned plate on the workbench and pass it through the pressure plate and other tools Fix the plate on the workbench, and select a stirring head with a stirring pin length of 2.3 mm according to the thickness of the plate to be welded.
[0044]Step 2: Move the ...
Embodiment 2
[0048] The thickness of the selected plate and the size of the stirring pin are the same as in Example 1.
[0049] The specific implementation steps are as follows:
[0050] Step 1: Clean the 2.5mm thick aluminum alloy with alcohol to clean the surface of the metal plate and the oil and oxides on the interface and other substances that hinder the welding process. Place the cleaned plate on the workbench and pass it through the pressure plate and other tools Fix the plate on the workbench, and select a stirring head with a stirring pin length of 2.3 mm according to the thickness of the plate to be welded.
[0051] Step 2: Move the stirring head to the starting position of the weld, adjust the position of the stirring head so that the center of the stirring needle coincides with the center line of the weld, and move the stirring head down until the end surface of the stirring needle contacts the surface of the workpiece and stop.
[0052] Step 3: Set the welding parameters, the...
Embodiment 3
[0055] The thickness of the selected plate and the size of the stirring pin are the same as in Example 1.
[0056] The specific implementation steps are as follows:
[0057] Step 1: Clean the 2.5mm thick aluminum alloy with alcohol to clean the surface of the metal plate and the oil and oxides on the interface and other substances that hinder the welding process. Place the cleaned plate on the workbench and pass it through the pressure plate and other tools Fix the plate on the workbench, and select a stirring head with a stirring pin length of 2.3 mm according to the thickness of the plate to be welded.
[0058] Step 2: Move the stirring head to the starting position of the weld, adjust the position of the stirring head so that the center of the stirring needle coincides with the center line of the weld, and move the stirring head down until the end surface of the stirring needle contacts the surface of the workpiece and stop.
[0059] Step 3: Set the welding parameters, the...