
Method for shot peening a gas carburised steel
a gas carburized steel and peening technology, applied in the field of shot peening, can solve the problem that the methods of these studies are difficult to apply to gas carburized steel with a soft layer on the surface, and achieve the effect of high compressive residual stress and high fatigue strength
Patent Information
- Authority / Receiving Office
- US · United States
- Current Assignee / Owner
- Publication Date
- 2013-05-16
- Estimated Expiration
- Not applicable · inactive patent
Smart Images
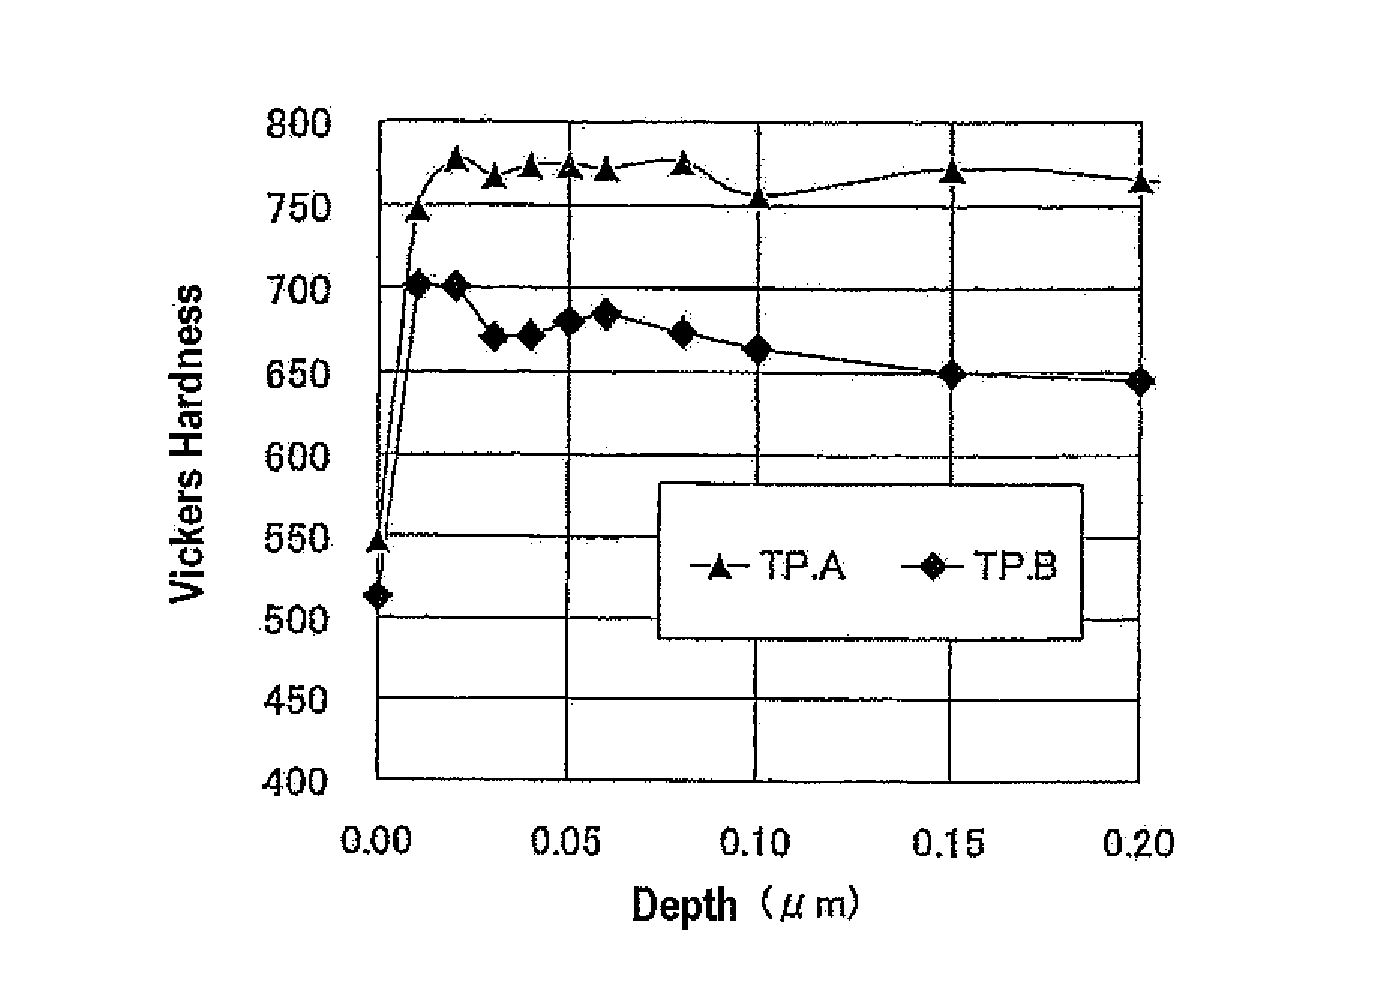
Figure 1 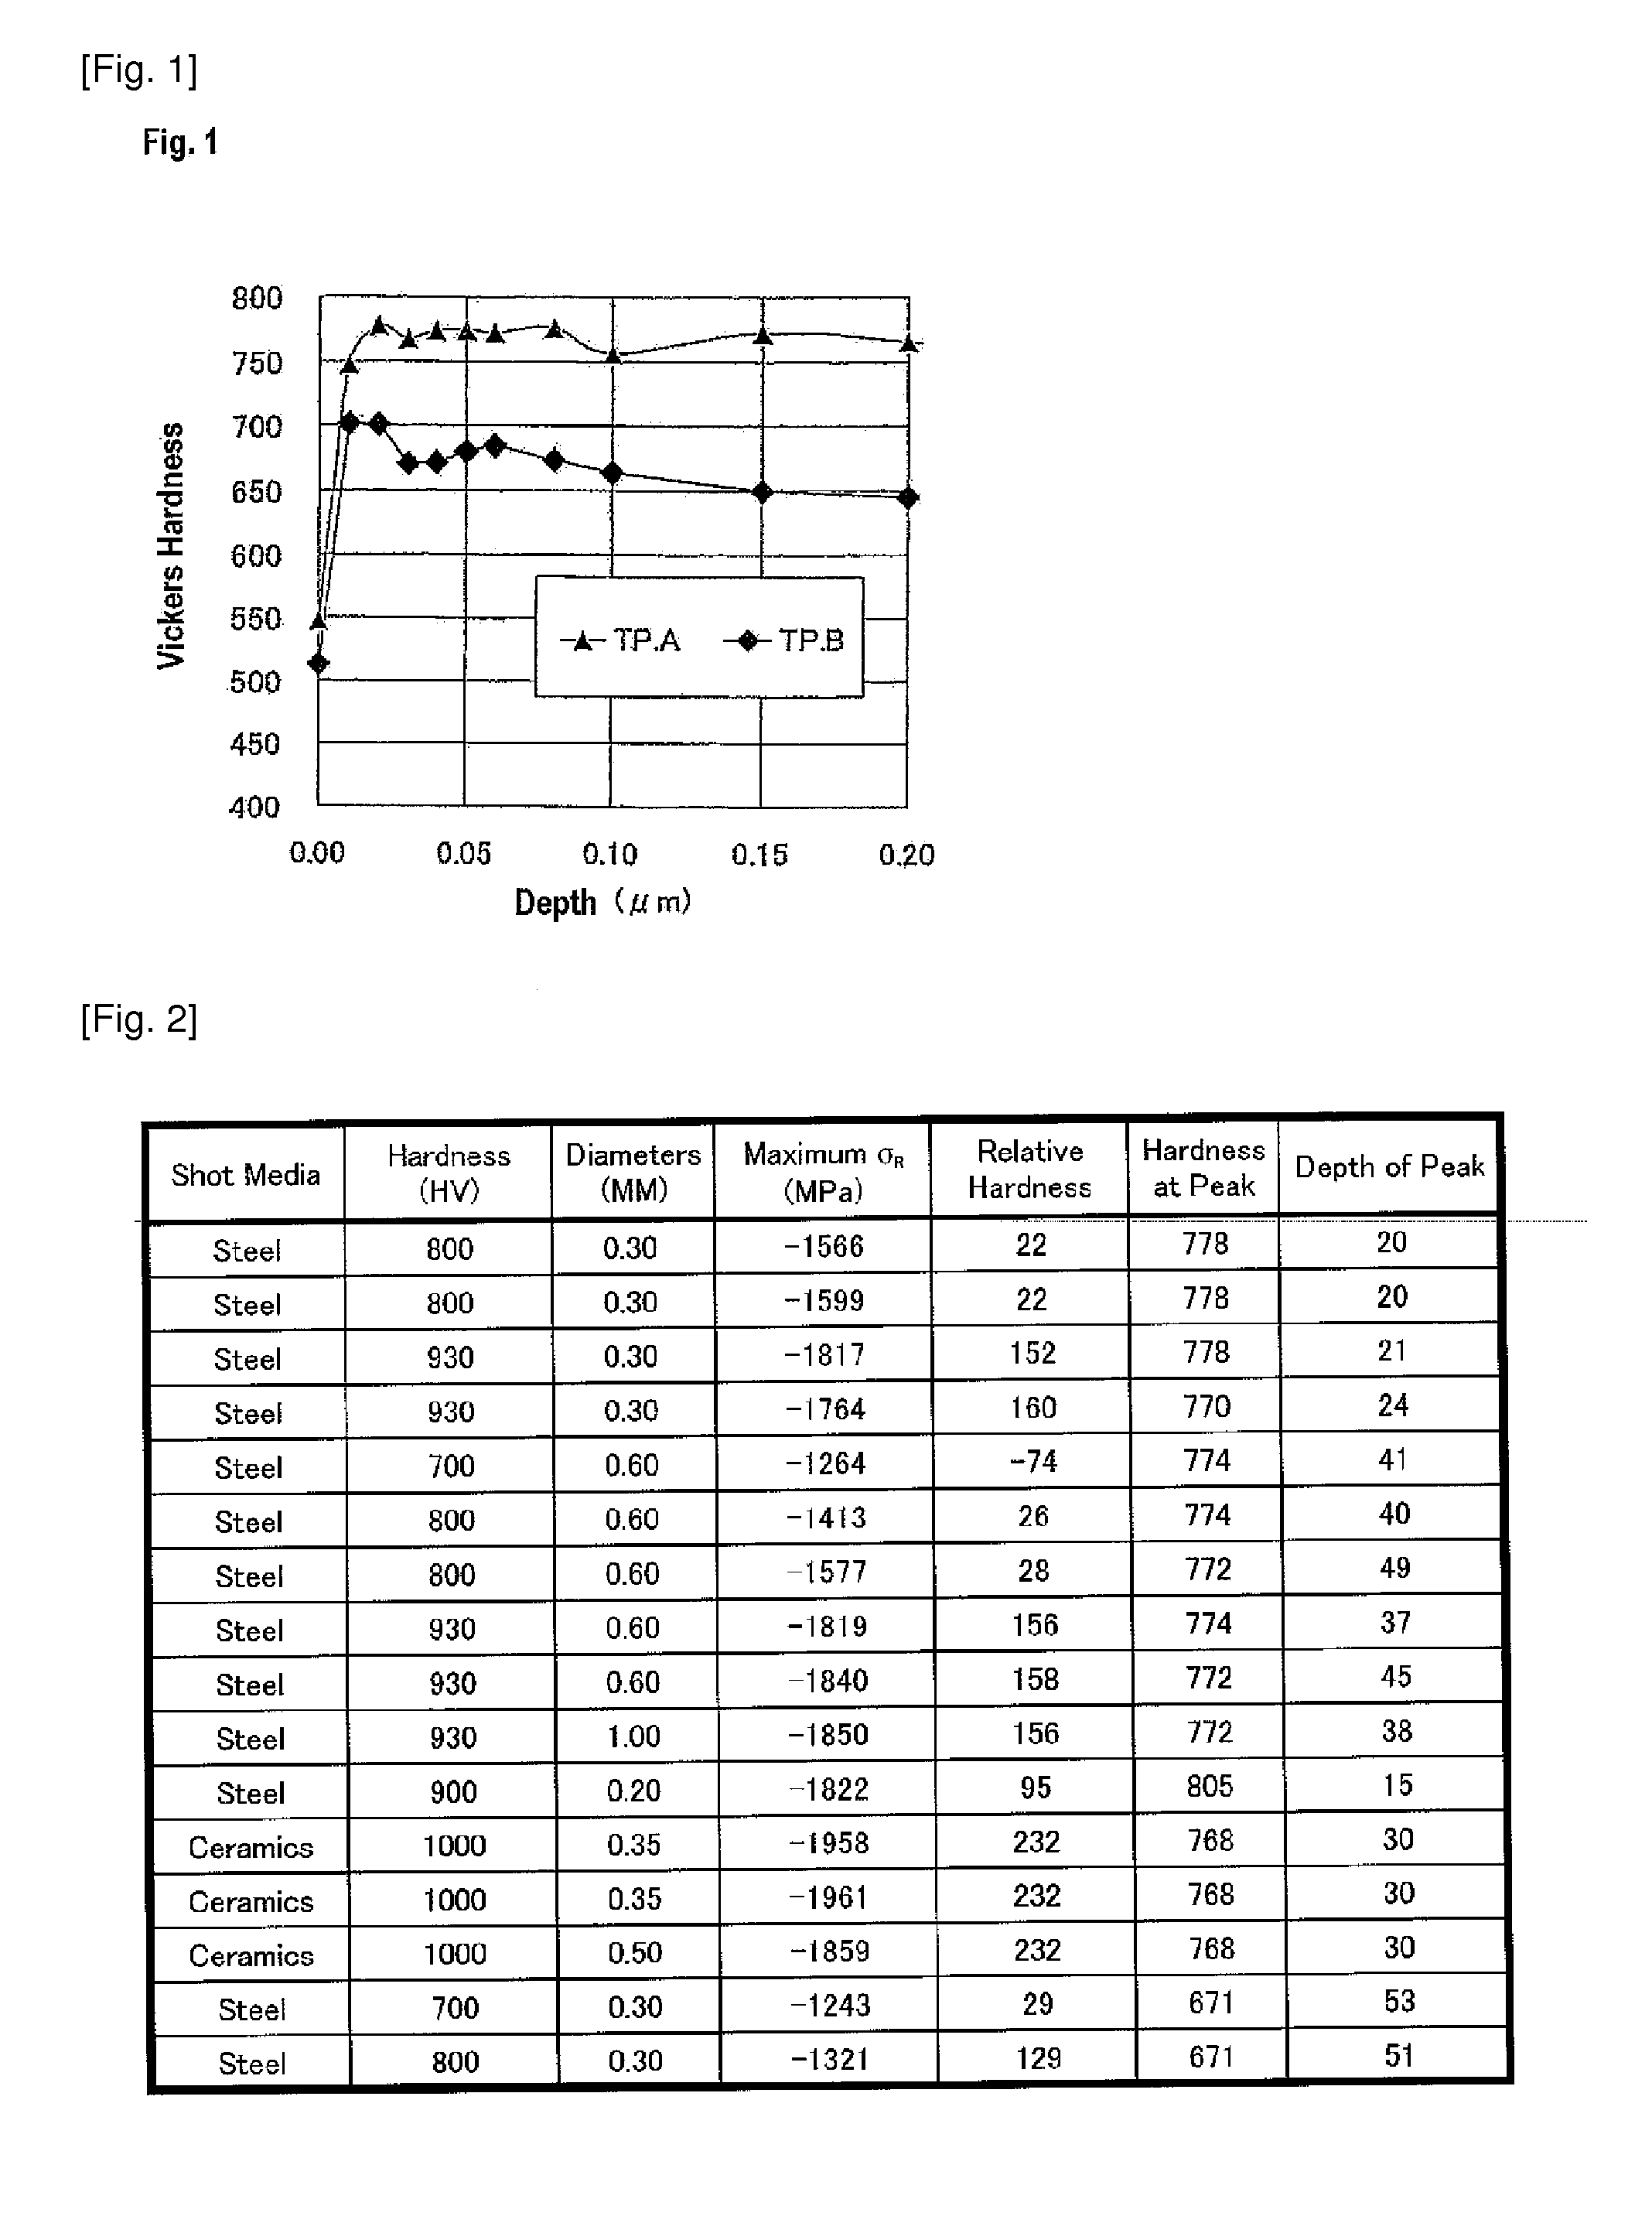
Figure 2 
Figure 3
Abstract
Description
TECHNICAL FIELD
[0001] The present invention relates to a method for shot peening. Specifically, it relates to a method for shot-peening a gas carburized steel.BACKGROUND ART
[0002] Conventionally, shot peening has been known to produce compressive residual stresses and to increase hardness to improve the fatigue strength of gears (see authored by the Society of Shot Peening Technology of Japan; Fatigue of Metals and Shot Peening; published by Gendai Kogaku-sha; 2004). Further, to achieve high fatigue strength aimed at reducing the weight of parts, a method for increasing compressive residual stresses produced by shot peening has been known (see Kazuyoshi Ogawa and Takashi Asano; Theoretical Prediction of Residual Stress Produced by Shot Peening for Hardened Steel; Transactions of JSSR, No. 48 (2003) pp. 31-38).
[0003] However, in these studies only the mean values of the hardness on the surface of, or near the surface of, the material are focused on. Thus the methods by these studies a...
Examples
Embodiment Construction
[0027]Below, the embodiments of the present invention are described with reference to the drawings.
[0028]FIG. 1 is a graph showing the distribution of the hardness of the processed steels that were used in the embodiments. The abscissa denotes depths (micrometer) from the surface of the steel, and the ordinate denotes the Vickers hardness. A gas carburized steel is used for the processed steels. In the drawing, “TP.A” and “TP.B” denote the steels which have been tempered at 180 degree C. and 180 degree C., respectively.
[0029]FIG. 2 is a table showing the conditions and the results of shot peening that were used in the embodiments. A compressive-air shot peening system was used. Shot media that have a hardness of 700 HV to 1,000 HV and diameters (the mean diameters) of 0.2 to 1.0 mm were used.
[0030]The
“Maximum σR”
in the table denotes the maximum compressive residual stresses in the processed steels. The compressive residual stresses were measured by using a micro-stress analyzer that...