
Ceramic bond gross blow hole repairing grinding wheel and manufacturing method thereof
A ceramic bond, large pores technology, used in ceramic products, grinding/polishing equipment, abrasives, etc., can solve the problem of inability to enter the actual grinding, to avoid weak bonding, improve hardness, and ensure safety performance. Effect
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Applications(China)
- Current Assignee / Owner
- Publication Date
- 2013-06-26
Smart Images
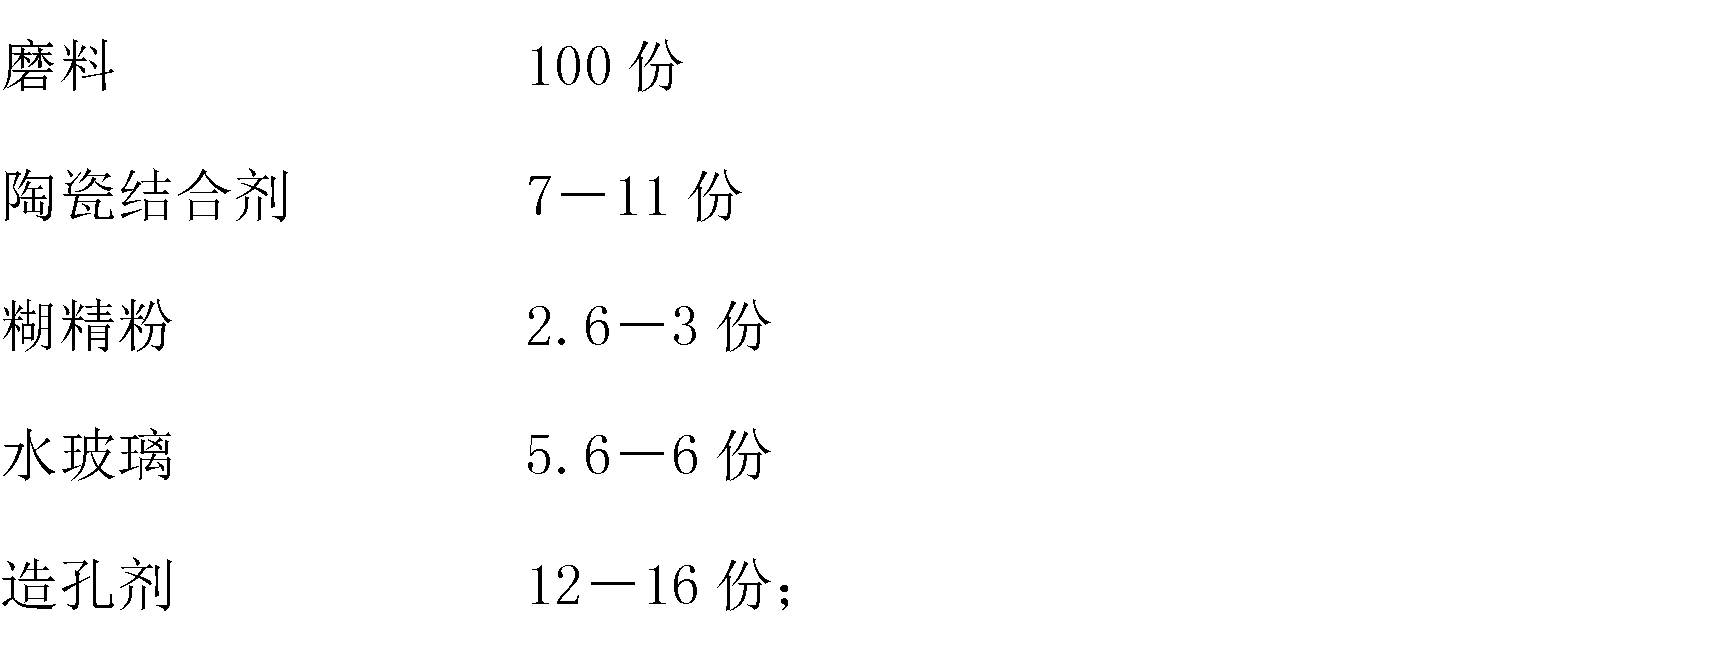
Figure 1 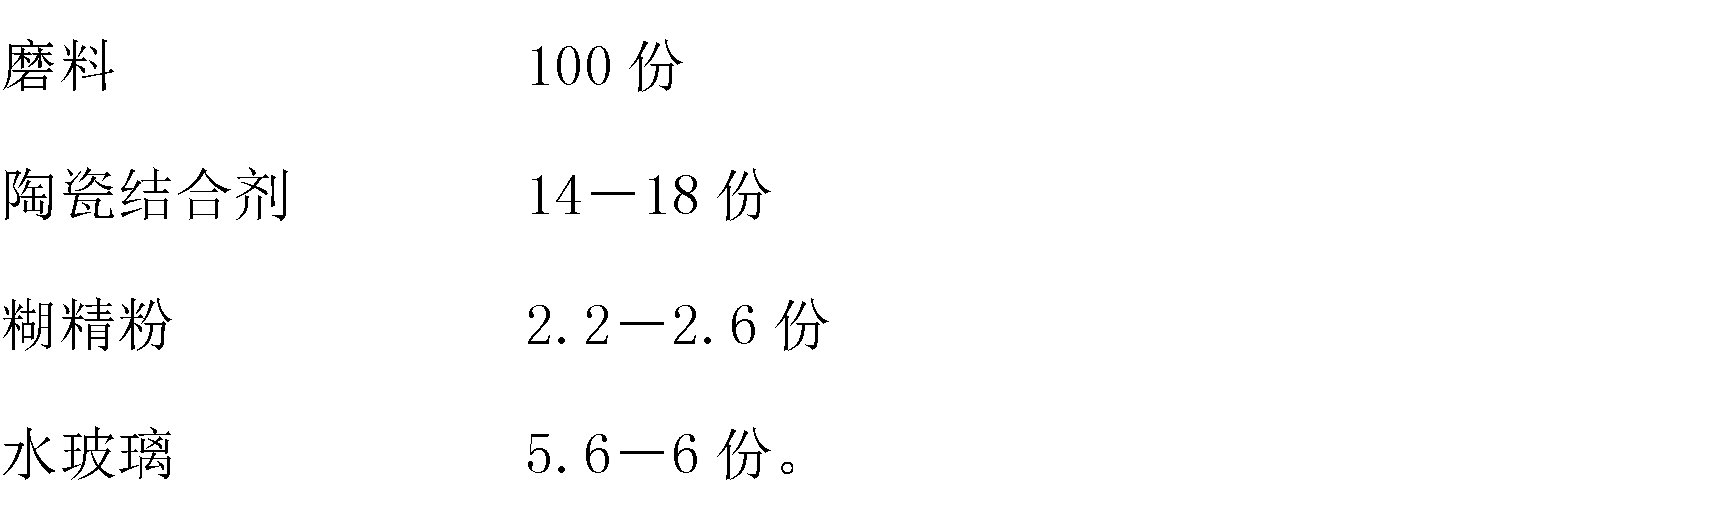
Figure 2
Abstract
Description
technical field
[0001] The invention relates to a dressing grinding wheel and a preparation method thereof, in particular to a vitrified bond macroporous grinding wheel and a preparation method thereof, belonging to the technical field of special abrasive tool manufacturing. Background technique
[0002] When grinding the rails along the railway line, the milling and grinding car is usually used to mill the rail surface first and then grind it. That is, the milling cutter disc composed of milling cutters is used to rough the surface of the rail, and then the grinding wheel is used for precise grinding. Most of the special grinding wheels for rail grinding in the prior art are resin-bonded coarse grinding wheels, which belong to the grinding method of vertical shaft grinding, that is, the grinding wheel faces the rail tread for grinding. The domestic grinding wheel industry has conducted in-depth research on resin-bonded vertical grinding wheels, and has basically mastered t...
Examples
Embodiment 1
[0022] A method for preparing a vitrified large-pore grinding wheel, the preparation steps are as follows: (1) First prepare a vitrified bond, put 18 parts of clay powder, 63 parts of feldspar powder and 14 parts of boron glass powder in a ceramic pot In the ball mill, add Φ10-15mm ceramic balls accounting for 15% of the mass of the mixture, and then perform ball milling at a speed of 960r / min for 4 hours, and pack the material into bags for later use; Pretreatment: Put the walnut shell particles into the countercurrent mixer, then add liquid phenolic resin PF2127, the mass ratio of walnut shell particles and liquid phenolic resin PF2127 is 100:15, then stir for 5 minutes to mix well, until the walnut shell particles are completely wetted Evenly placed in a metal container, dried at 80°C for 20 minutes, then passed through a 12-mesh sieve, and finally hardened in an oven at 180°C for 20 minutes, and sealed for later use after cooling; (3) Processing process: core: 100 parts of ...
Embodiment 2
[0024] A method for preparing a vitrified large-pore grinding wheel, the preparation steps are as follows: (1) First prepare a vitrified bond, put 20 parts of clay powder, 65 parts of feldspar powder and 15 parts of boron glass powder in a ceramic pot In the ball mill, add Φ10-15mm ceramic balls accounting for 18% of the mass of the mixture, and then perform ball milling at a speed of 960r / min for 5 hours, and pack the material into bags for later use; Pretreatment: Put the walnut shell particles into the countercurrent mixer, then add liquid phenolic resin PF2127, the mass ratio of walnut shell particles and liquid phenolic resin PF2127 is 100:18, then stir for 8 minutes to mix well, until the walnut shell particles are completely wetted Evenly placed in a metal container, dried at 90°C for 25 minutes, then passed through a 12-mesh sieve, and finally hardened in an oven at 180°C for 25 minutes, and sealed for later use after cooling; (3) Processing process: core: 100 parts of ...
Embodiment 3
[0026]A method for preparing a vitrified large-pore grinding wheel, the preparation steps are as follows: (1) First prepare a vitrified bond, put 22 parts of clay powder, 67 parts of feldspar powder and 16 parts of boron glass powder in a ceramic pot In the ball mill, add Φ10-15mm ceramic balls accounting for 20% of the mass of the mixture, and then perform ball milling at a speed of 960r / min for 6 hours, and pack the material into bags for use; Pretreatment: Put the walnut shell particles into the countercurrent mixer, then add liquid phenolic resin PF2127, the mass ratio of walnut shell particles and liquid phenolic resin PF2127 is 100:20, then stir for 10 minutes to mix well, until the walnut shell particles are completely wetted Evenly placed in a metal container, dried at 100°C for 30 minutes, then passed through a 12-mesh sieve, and finally hardened in an oven at 180°C for 30 minutes, and sealed for later use after cooling; (3) Processing process: core: 100 parts of parti...