
Patents
Literature
5787 results about "Grinding wheel" patented technology
Efficacy Topic
Property
Owner
Technical Advancement
Application Domain
Technology Topic
Technology Field Word
Patent Country/Region
Patent Type
Patent Status
Application Year
Inventor
A grinding wheel is a wheel composed of an abrasive compound and used for various grinding (abrasive cutting) and abrasive machining operations. Such wheels are used in grinding machines. The wheels are generally made from a composite material consisting of coarse-particle aggregate pressed and bonded together by a cementing matrix (called the bond in grinding wheel terminology) to form a solid, circular shape. Various profiles and cross sections are available depending on the intended usage for the wheel. They may also be made from a solid steel or aluminium disc with particles bonded to the surface. Today most grinding wheels are artificial composites made with artificial aggregates, but the history of grinding wheels began with natural composite stones, such as those used for millstones.
Crankshaft connecting rod grinding force dynamic error compensation method and system
InactiveCN120363032AGrinding feed controlAutomatic grinding controlFrequency spectrumControl engineering
The invention relates to the technical field of grinding machining, and particularly discloses a crankshaft connecting rod grinding force dynamic error compensation method and system.The method comprises the steps that a prediction reference signal is collected; a grinding force signal of the grinding wheel spindle is collected based on a piezoelectric sensor; extracting spectrum characteristic parameters according to the predicted reference signal; predicting grinding force fluctuation information according to the spectrum characteristic parameters; a feedforward compensation instruction is generated according to the grinding force fluctuation information; generating a feedback compensation instruction according to the difference between the grinding force signal and the target grinding force of the current task; synthesizing the feedforward compensation instruction and the feedback compensation instruction to generate a compensation control instruction; according to the method, a control strategy combining feedforward and feedback is adopted, the response speed and compensation precision of a system to dynamic changes of grinding force are remarkably improved, accordingly, elastic deformation caused by fluctuation of the grinding force is effectively restrained, and finally the grinding machining precision and surface quality of key parts of the crankshaft connecting rod are improved.

Owner:LIAOCHENG HAOZHUO MASCH MFG CO LTD
Online compensation method for abrasion loss of blade grinding wheel
The invention relates to the technical field of grinding machining, and discloses a blade grinding wheel abrasion loss online compensation method which comprises the steps that a dynamic hexagonal detection grid is constructed based on the rotating phase of a grinding wheel, non-repeated high-density sampling is achieved through a Fibonacci spiral expansion path, a detection area is dynamically adjusted to reduce the overlapping rate, and the blade grinding wheel abrasion loss is obtained. Micron-sized wear transition is accurately captured; dispersing the abrasion loss into minimum compensation units, constructing a dynamic state equation in combination with grinding force, dressing displacement and workpiece errors, introducing an attenuation coefficient related to the service life of a dressing wheel, and automatically correcting a model drift error; a grading triggering strategy of residual uncompensated quantity is adopted, dynamic decision making of a processing period is combined, and through integral multiple compensation and a margin temporary storage mechanism, it is ensured that long-term accumulative errors are restrained at the submicron level while overmodulation oscillation is avoided. Through the synergistic effect of space-time coupling detection, discrete-continuous double-domain modeling and intelligent compensation decision, the grinding wheel abrasion compensation precision and the system stability are remarkably improved.

Owner:HUNAN YIFAN GAODE PRECISION TECH CO LTD
Metal grinding machine tool grinding wheel wear compensation type intelligent control system
The invention discloses a metal grinding machine tool grinding wheel wear compensation type intelligent control system, and relates to the technical field of mechanical manufacturing automation, and the system comprises a contact type reference detection module which is used for obtaining the initial contour and reference wear loss of a grinding wheel through discrete point measurement in a non-machining state; the multi-parameter non-contact real-time detection module is used for collecting acoustic emission, vibration and spindle current signals in the grinding process through three types of sensors; the grinding environment sensing module collects the temperature of a grinding area and the cutting fluid concentration; the intelligent control unit receives reference data and an environment signal, performs deep learning on a wear loss prediction model after multi-source data fusion, performs periodic reference calibration, analyzes the dynamic wear loss, and synchronously transmits the data to the data storage and tracing module; the executing mechanism adjusts grinding wheel feed amount compensation according to the dynamic abrasion loss; and the data storage and tracing module stores full-process data in real time. According to the system, high-precision and real-time wear compensation is achieved, the machining precision and consistency are improved, and high-end manufacturing requirements are met.

Owner:HANGZHOU CANWANG TECHNOLOGY CO LTD
Steel pipe polishing device
InactiveCN106826528AEasy to operateSimple structurePolishing machinesGrinding machine componentsSteel tubeMagnet
The invention discloses a steel pipe polishing equipment, which comprises a steel pipe polishing equipment body. A main valve of a polishing motor is arranged in the main body of the steel pipe polishing equipment; a polishing handle is arranged on the main valve of the polishing motor; The valve is provided with a rotating roller; the front end of the rotating roller is provided with polishing bristles; one side of the rotating roller is provided with an outer throwing roller; a clamping spring is arranged between the outer throwing roller and the rotating roller; The outer throwing roller is provided with an outer throwing brush; a symmetrical magnet is arranged between the outer throwing brush and the polishing bristles; a polishing wheel is arranged on the outer throwing brush and the polishing bristles; the polishing The grinding wheels are arranged in a figure-eight shape. Its structure is simple, easy to use, and easy to operate. It can realize the polishing of the outer surface and the inner wall. The polishing is fast and uniform, with high efficiency and convenient use.
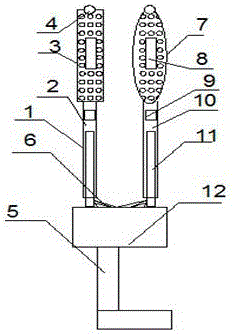
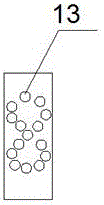
Owner:何盼
Precise grinding equipment for cast steel sleeve
PendingCN120190735ARevolution surface grinding machinesGrinding work supportsGrinding wheelSteel casting
The invention relates to the technical field of sleeve grinding, and discloses cast steel sleeve precise grinding equipment which comprises a grinding wheel grinding mechanism, a chuck is installed below the grinding wheel grinding mechanism, a plurality of clamping jaws are installed in the chuck, and the tops of the clamping jaws do not exceed the upper surface of the chuck. An outer clamping jaw away from the circle center of the chuck and an inner supporting jaw close to the circle center of the chuck are installed on the surfaces of the clamping jaws correspondingly, a transmission range extending piece capable of enabling the outer clamping jaw and the inner supporting jaw to do range extending motion is installed on the surface of each clamping jaw, and rack limiting pieces used for limiting the outer clamping jaw and the inner supporting jaw to do one-way range extending motion are installed on the inner wall of the chuck. Through the design of the outer clamping jaw and the inner supporting jaw, compatibility of outer wall polishing and inner wall polishing in the same working procedure is achieved, compared with a traditional single inner supporting or outer clamping mode, the problem of polishing blind areas caused by clamp occupying is avoided, it is ensured that the inner wall and the outer wall of the cast steel sleeve can be completely machined at a time, two-time clamping is not needed, and the machining efficiency is improved. And the processing efficiency and the integrity are obviously improved.

Owner:JIANGSU YUZHEN MASCH TECH CO LTD
Large-size grinding wheel concentricity error measurement method and system based on machine vision
The invention discloses a large-size grinding wheel concentricity error measurement method and system based on machine vision, and relates to the technical field of grinding wheel concentricity error measurement, and the method comprises the steps: calibrating an industrial CCD camera through PyCharm software, collecting a part of images of a grinding wheel, and carrying out the RGB three-channel extraction, gray conversion, filtering and binary segmentation processing of the collected images; secondly, a Canny edge operator is adopted to carry out coarse positioning on the edge of the image, and then a novel edge judgment criterion is established to construct an edge detection model with sub-pixel-level precision; and finally, carrying out feature fusion on sub-pixel contours of RGB channels, clustering extracted discrete point sets by using an improved DBSCAN algorithm, and then carrying out ring fitting by using improved RANSAC to realize accurate measurement of the inner and outer diameters and concentricity of the grinding wheel.

Owner:ZHENGZHOU UNIVERSITY OF LIGHT INDUSTRY
Numerical control grinding machine debugging control system based on intelligent industry
The invention relates to the technical field of automatic control, in particular to a numerical control grinding machine debugging control system based on intelligent industry, which comprises a wear area division module, a grinding wheel regulation and control module, a basic compensation value analysis module, a thermal error compensation module and a management database, according to the system, the abrasion area of the surface of the grinding wheel at each time point is obtained through threshold segmentation of the surface image of the grinding wheel at each time point, and the parameters of the grinding wheel are regulated and controlled based on the deviation value between the actual power and the target power of the grinding wheel at each time point; the instantaneous position error change rate of machine tool motion is calculated by collecting instruction positions and actual positions of machine tool motion at all sampling moments, so that a basic compensation value is obtained through analysis, a thermal compensation value is obtained through prediction of a temperature-thermal error mapping relation, a compensation value is obtained by combining the basic compensation value, and the compensation value is superposed to the instruction positions. And the self-adaptive optimization of the whole polishing process is realized.

Owner:SHANDONG MICROCRYSTALLINE AUTOMATION CO LTD
Cast pipe inner wall polishing device and system
The invention discloses a cast pipe inner wall grinding device and system and relates to the technical field of grinding equipment, the cast pipe inner wall grinding system comprises a rack, a rotary supporting device and a cast pipe inner wall grinding device, and the cast pipe inner wall grinding device comprises a grinding feeding mechanism, an anti-swing mechanism and a grinding mechanism; the grinding feeding mechanism comprises a first linear driving device, a first rotating power source, an outer fixing sleeve and an inner rotating shaft, the anti-swing mechanism comprises an outer rotating sleeve, a positioning wheel assembly and a distance adjusting mechanism, and the grinding mechanism comprises a second linear driving device and a grinding wheel body. The outer fixing sleeve is radially supported through the positioning wheel assembly, radial swing of the grinding wheel shaft is restrained, and the grinding stability can be improved; the distance adjusting mechanism can dynamically adjust the distance between the positioning wheel assemblies to adapt to cast pipes with different calibers; and the second linear driving device drives the grinding wheel to move in the radial direction, constant-pressure grinding is achieved in cooperation with the pressure detection device, the grinding rhythm is dynamically adjusted, the grinding effect can be improved, and the grinding consistency is improved.

Owner:HANDAN COLLEGE +1
Laser cutting equipment
The utility model provides laser cutting equipment which comprises two symmetrically-arranged supports, first supporting plates and second supporting plates, the two first supporting plates are installed on the opposite sides of the supports, the two second supporting plates are installed on the tops of the supports, and the opposite sides of the two first supporting plates are provided with grinding assemblies. A laser cutting assembly is arranged on the top of the second supporting plate, and a clamping assembly used for clamping the plate is further arranged on one side of the second supporting plate. The first sliding plate is in sliding fit with the opposite sides of the two first supporting plates through electric sliding rails, the first sliding block is in sliding fit with the first sliding plate through the electric sliding rails, a first hydraulic rod is fixedly installed at the bottom of the first sliding block, and the telescopic end of the first hydraulic rod penetrates through the first sliding block and is fixedly provided with a first motor. By arranging the grinding wheel, slag generated on the back face of a plate can be ground and cleaned, the situation that the back face of the plate is uneven due to the slag is avoided, and therefore the cutting efficiency and quality are improved.

Owner:ANHUI BAICHAO LASER TECH CO LTD
Efficient cooling grinding wheel applied to ultrasonic machining
ActiveCN120244830AGrinding machine componentsGrinding/polishing safety devicesInterference fitUltrasonic machining
The invention discloses an efficient cooling grinding wheel applied to ultrasonic machining, and relates to the technical field of ultrasonic auxiliary grinding machining tools, the efficient cooling grinding wheel comprises an upper ultrasonic grinding wheel base rod and a lower ultrasonic grinding wheel grinding head, and the ultrasonic grinding wheel base rod and the ultrasonic grinding wheel grinding head are of an integrated structure; the interior of the ultrasonic grinding wheel base rod is hollow and extends to the bottom of the ultrasonic grinding wheel grinding head without penetrating, the interior of the ultrasonic grinding wheel base rod is in threaded connection or interference fit with a sleeve, the interior of the sleeve is hollow and serves as a main cooling liquid flow channel, the diameter of the interior of the sleeve is the main cooling liquid flow channel, and the diameter of the main flow channel can be changed; a plurality of round holes are formed in the grinding wheel grinding head to serve as cooling liquid flow channels of the grinding head, inlets of the cooling liquid flow channels of the grinding head are connected with the tail end of the main cooling liquid flow channel, outlets of the cooling liquid flow channels of the grinding head are located at the machining position in the grinding process, and cooling liquid grooves are machined in the cooling liquid outlets of the grinding head. And inner cavities of the main cooling liquid flow channel and the grinding head cooling liquid flow channel are provided with rifling structures with variable screw pitches and variable number.

Owner:DALIAN UNIV OF TECH
Shoe sole wear resistance detection device
The invention provides a shoe sole wear resistance detection device, and belongs to the technical field of wear resistance detection, the shoe sole wear resistance detection device comprises an instrument body and a shoe sole sample formed by punching a shoe sole, and further comprises a simulation detection assembly and a dust removal cleaning assembly; under the guidance of the guide ring, the first support arm can periodically move up and down, the process simulates the dynamic change of the pressure borne by the sole in different gait stages when a person walks, and in combination with the rotation of the sole sample, not only is the vertical pressure change simulated, but also the friction force in different directions can be simulated through relative sliding. The stress state of the shoe sole in the walking process is restored, so that the detection is closer to the actual use scene; the dust removal system is driven by the power of the detection device to operate, so that all-directional coverage of the whole abrasion area is realized, the retention time of dust in the detection area is reduced, dust interference can be avoided, the state of a sole sample before and after detection is only influenced by abrasion of a grinding wheel, and the detection result more truly reflects the abrasion resistance of the sole.

Owner:ANHUI RUIMAI SHOES CO LTD
Grinding force closed-loop control and flutter suppression system for crankshaft variable stiffness machining
PendingCN121132421ARevolution surface grinding machinesGrinding drivesLoop controlControl engineering
The invention particularly relates to a grinding force closed-loop control and flutter suppression system for crankshaft variable stiffness machining, and aims to solve the problems of unstable grinding force, flutter and surface defects caused by time-varying stiffness characteristics of a crankshaft due to a multi-crank throw and cantilever supporting structure. The system comprises a grinding force detection module, a control module and an execution module. The grinding force detection module is arranged in a grinding wheel and crankshaft contact area and collects grinding force signals in real time. The control module receives an actual grinding force signal, compares the actual grinding force signal with a target value, and outputs a compensation instruction and a suppression instruction; the compensation instruction is generated by adopting a self-adaptive PID or fuzzy PID algorithm based on force deviation, and the grinding wheel feeding speed or the main shaft rotating speed is dynamically adjusted to stabilize the grinding force; and extracting a high-frequency component of the force signal as a flutter feature, identifying a flutter bud through time-frequency analysis, and generating an anti-phase displacement instruction to suppress flutter. The execution module adjusts feeding or rotating speed according to the compensation instruction and adjusts radial displacement of the crankshaft or the grinding wheel according to the suppression instruction.

Owner:LIAOCHENG HAOZHUO MASCH MFG CO LTD
Multi-discharge efficient precision machining equipment and method for milling cutter
The invention discloses a multi-discharge efficient precision machining device and method for a milling cutter. The multi-discharge efficient precision machining device comprises a high-precision machining tool, an electric spark machining pulse power supply, a discharge monitoring device and a detection device. The high-precision machining machine tool comprises an electric spark machining machine tool, a spindle, a grinding wheel, a workbench and a machine tool body. The main shaft supports accurate movement in three directions; stable and controllable pulse current and voltage are output through the electric spark machining pulse power supply; a voltage probe and a current probe are arranged on the discharge monitoring device, and discharge voltage and current data are collected in real time through the voltage probe and the current probe; the detection device comprises a non-contact optical measuring instrument, the abrasion of the grinding wheel is monitored through the non-contact optical measuring instrument, meanwhile, the machining allowance of the milling cutter blank placed on the workbench and the size precision after finish machining are measured, and the surface quality of the milling cutter is detected; the machining precision and efficiency of the milling cutter are improved, and efficient precision machining of the milling cutter is achieved.

Owner:NANJING UNIV OF AERONAUTICS & ASTRONAUTICS +1
Micro engine blade temperature control ultrasonic composite liquid gallium auxiliary grinding device and method
The invention belongs to the technical field of liquid metal coating and infiltration in grinding machining, and particularly relates to a temperature-control ultrasonic composite liquid gallium auxiliary grinding device and method for a micro engine blade, and the device comprises a fluid conveying module, a temperature adjusting module, a machining module, an ultrasonic vibration module and an electromagnetic field generator. Temperature control of liquid gallium is achieved by arranging a microwave cavity and a cooling system, stable supply is guaranteed through inert gas and a liquid gallium conveying pipeline, and uniform coating and ultrasonic vibration infiltration on the surface of the blade of the micro engine are achieved by combining an ultrasonic transduction assembly and a spraying nozzle. The electromagnetic field generator further enhances the adhesion and lubrication effects of the liquid gallium on the grinding wheel and the blades. The defects of insufficient grinding temperature control and lubrication of a traditional grinding wheel are overcome, the grinding temperature rise and the friction coefficient are effectively reduced, thermal damage and surface deformation are avoided, and the machining precision and the surface quality of complex curved surfaces and tenon tooth parts are improved.

Owner:HUNAN INSTITUTE OF SCIENCE AND TECHNOLOGY
Metal sealing ring machining device with clamping function
ActiveCN223235930UGrinding drivesAbrasive surface conditioning devicesElectric machineGrinding wheel
The utility model relates to the technical field of sealing ring machining, and discloses a metal sealing ring machining device with a clamping function, which comprises a working table, an air cylinder is fixedly arranged at the top of the working table and can drive a moving plate to move up and down, and the moving plate is fixedly arranged at the bottom of a piston rod at the output end of the air cylinder and can drive the moving plate to move up and down. According to the metal sealing ring machining device with the clamping function, when a sealing ring needs to be polished, an air cylinder is started to drive the motor to move downwards, the moving plate can drive a connecting rod to push an extrusion rod, the motor is driven to move upwards, and the extrusion rod is driven to move downwards; and meanwhile, a Z-shaped rod can push a rotating rod to enable a rotating disc to rotate, a cylindrical rod can drive a clamping block to move outwards, the inner ring of the sealing ring can be clamped, in this way, the sealing ring can be clamped more tightly, and the situation that polishing is poor, and secondary machining is needed is avoided.

Owner:WUXI WEIYIFA PRECISION MACHINERY
Cylinder body casting polishing device and polishing process thereof
The invention relates to the field of grinding machinery, and discloses a cylinder body casting grinding device and a grinding process thereof.The device comprises a frame body and a controller, a three-jaw chuck is arranged on the frame body, and a to-be-ground cylinder body is clamped through the three-jaw chuck; a grinding mechanism is further arranged on one side of the frame body and comprises a hydraulic telescopic cylinder and a driving part, the hydraulic telescopic cylinder is fixedly installed on the frame body, the driving part is fixedly installed at the end of the hydraulic telescopic cylinder, and the output end of the driving part is in transmission connection with a grinding shaft; a grinding shell is fixedly arranged at the end of the grinding shaft, multiple stages of grinding wheels are arranged in the grinding shell, an alternating assembly is further arranged in the grinding shell, and the alternating assembly is used for pushing the different stages of grinding wheels to sequentially stretch out of the grinding shell to conduct the grinding action of the cylinder body. By means of the mechanism, real-time replacement of different levels of grinding wheels in the working state in the cylinder body is achieved, and the grinding efficiency is higher.

Owner:JIANGSU WANLIU MASCH MFG CO LTD
Grinding state and grinding wheel wear monitoring system and method based on multi-sensor fusion
PendingCN120190763ABatteries circuit arrangementsGrinding feed controlVibration amplitudeNetwork model
The invention discloses a grinding state and grinding wheel wear monitoring system and method based on multi-sensor fusion, which realize multi-physical-quantity coupling modeling and improve the monitoring precision through cooperative deployment of micro array thermocouples, strain force sensors and vibration sensors and in combination with a time domain and frequency domain feature extraction technology. The system adopts a non-contact power supply design, electromagnetic induction power generation is driven through rotation of the main shaft, real-time signal processing and wireless transmission of a circuit board in the grinding wheel are supported, and the problem of power supply in a high-speed rotation scene is solved. And meanwhile, dimension reduction processing is conducted on the multi-sensor features through an offline network model, self-adaptive adjustment of grinding parameters and ultrasonic amplitude is achieved through dynamic regulation and control logic, and the downtime and the rejection rate are remarkably reduced. The method has remarkable creativity, practicability and economic benefits, fills the blank of fragmentation monitoring and regulation and control lag in the prior art, and improves the stability and machining quality of the grinding process.

Owner:NANJING UNIV OF AERONAUTICS & ASTRONAUTICS
Polishing device for hardware part machining
InactiveCN120244731ARevolution surface grinding machinesGrinding drivesRotational axisElectric machine
The invention relates to the technical field of shaft sleeve polishing, in particular to a polishing device for hardware part machining. Comprising a mounting frame, a rotating disc, a driving motor I, a support, an arc-shaped plate, a guide rod and the like, the rotating disc is rotationally connected to the mounting frame, U-shaped through holes and round holes are evenly formed in the rotating disc in the circumferential direction at intervals, the driving motor I is connected to the mounting frame, the end of a rotating shaft of the rotating disc is connected with an output shaft of the driving motor I, and the support is connected to the top face of the mounting frame; the arc-shaped plates are circumferentially and evenly connected to the rotating disc at intervals, and the guide rods are connected to the side face of the support. The arc-shaped plate is driven by the rotating disc to rotate intermittently, all the shaft sleeves can be sequentially conveyed to the position behind the grinding wheels, then the shaft sleeves can be driven by the electric roller to rotate in the arc-shaped plate, and then the two grinding wheels can be driven by the electric push rod to move backwards to make contact with the outer walls and the inner walls of the shaft sleeves correspondingly. The two grinding wheels can grind and polish the outer wall and the inner wall of the shaft sleeve at the same time, and the polishing efficiency is improved.

Owner:杨备芳
Tooth profile grinding wheel thermal drift modeling and wear life prediction method and system
The invention discloses a tooth profile grinding wheel thermal drift modeling and wear life prediction method and system. The method comprises the four stages of thermal drift path network construction, drift differentiation feature extraction, irregular fragmentation recombination and dynamic judgment feedback. A tooth surface multi-region temperature response sequence is collected, a thermal drift path network is established, and a drift differentiation feature set is generated by using a multi-period path evolution relationship so as to distinguish short-period thermal disturbance and trend drift interference; and irregular recombination and energy constraint optimization are carried out on the path based on the thermal response structure boundary to form a response structure unit with thermal-force coupling association. The system further achieves judgment sequence self-learning according to an energy feedback and weight updating mechanism, and therefore the abrasion state and remaining life prediction result of the tooth profile grinding wheel is output. According to the method, dynamic correction of grinding thermal response behaviors and intelligent life evaluation are achieved.

Owner:JIANGSU YIDING TRANSMISSION MASCH CO LTD
Workpiece grinding management method, system and equipment
ActiveCN120155808AGrinding feed controlAutomatic grinding controlKernel principal component analysisControl engineering
The invention relates to the technical field of metal grinding machining, in particular to a workpiece grinding management method, system and equipment, and the method comprises the following steps: acquiring workpiece information and grinding machining information; a multi-scale management model is established according to the workpiece information and the grinding machining information, and a management threshold value is set in the multi-scale management model; the multi-scale management model obtains a plurality of machining parameters in the grinding machining information according to a set time interval, then the machining parameters serve as initial features, the initial features are fused to obtain management features, through kernel principal component analysis feature fusion and fuzzy control, the abrasion state of the grinding wheel can be dynamically recognized, a nonlinear compensation strategy is generated, and the accuracy of the grinding wheel is improved. Specifically, when principal components extracted through kernel principal component analysis show that the grinding wheel enters an accelerated wear stage, the fuzzy controller can automatically adjust the compensation intensity according to the error change rate, and compensation deviation caused by linear hypothesis in a traditional method is avoided.

Owner:NINGJIANG MASCH TOOL GRP CO LTD
Grinding wheel wear degree identification method and device based on adaptive neural fuzzy reasoning
The invention discloses a grinding wheel wear degree identification method and device based on adaptive neural fuzzy reasoning. The method comprises the steps that a grinding temperature signal, grinding force and the surface quality of a workpiece are obtained; determining the abrasion stage of the grinding wheel according to the surface quality, the grinding force and the grinding temperature; extracting the total number of thermal pulses in the grinding temperature signal as the number of dynamic effective abrasive particles; a grinding wheel surface topography graph is obtained, abrasive dust and abrasive particle abrasion in the grinding wheel surface topography graph are recognized and distinguished through an HSV segmentation method, the area rate is calculated, and the abrasive dust proportion and the abrasive particle abrasion proportion are obtained; and the abrasive dust proportion, the abrasive particle abrasion proportion and the dynamic effective abrasive particle number serve as input, the abrasion stage serves as output, the self-adaptive neural fuzzy inference system is trained, and the trained self-adaptive neural fuzzy inference system is obtained for abrasion degree recognition. According to the method, the abrasion condition of the grinding wheel can be accurately and conveniently judged by utilizing the self-adaptive neural fuzzy reasoning technology and synthesizing the multi-dimensional characteristic signals in the grinding process.

Owner:HUAQIAO UNIVERSITY
Face gear worm grinding machine error compensation method based on sensitivity analysis and multi-source error mapping model
The invention discloses a face gear worm grinding machine error compensation method based on sensitivity analysis and a multi-source error mapping model, which comprises the following steps of: 1, constructing a multi-source error-tooth surface error mapping model based on a vector decomposition and truncation function method, the truncation function method is used for quantitatively describing propagation mechanisms of geometric errors and thermal errors in a machining chain and influences of the propagation mechanisms on tooth surface deviation, and high-order error terms are eliminated to improve calculation efficiency; 2, responding to the output of the mapping model, applying an improved Morris sensitivity analysis method, distributing a weighting coefficient higher than a geometric error component for a thermal error component, and calculating a weighting sensitivity coefficient so as to identify a key error component which has the greatest influence on the tooth surface precision; and 3, based on the key error component, a motion axis compensation value is generated through an error compensation model, and the compensation value is input into a machine tool control system to adjust the relative position of the worm grinding wheel and the workpiece, so that the tooth surface error is reduced.

Owner:CHONGQING UNIV
Z1-Z2 linkage removal amount control and grinding wheel loss optimization method for double-shaft DFG grinding machine
The invention relates to the technical field of precision machining, discloses a double-shaft DFG grinding machine Z1-Z2 linkage removal amount control and grinding wheel loss optimization method and system, and aims to solve the problems of unreasonable Z1-Z2 removal amount distribution, inaccurate grinding wheel loss control and poor wafer surface damage adaptability of existing DFG grinding. According to the method and system, Z1 rough grinding parameters are determined and adjusted through multi-objective optimization and self-adaptive control by means of the initial morphology and material characteristics of a wafer; in combination with a Z1 result, a deep learning model is utilized to intelligently distribute Z2 accurate grinding removal amount and parameters, and adaptive adjustment and abnormal Air Cut are realized; and meanwhile, the grinding parameters are continuously optimized by adopting the grinding wheel loss prediction model. By adopting the technical scheme, the grinding efficiency and precision can be remarkably improved, the service life of the grinding wheel is prolonged, the cost is reduced, and the problems of removal amount distribution, grinding wheel loss and wafer damage are solved.

Owner:ANHUI FULLERDE CHANGJIANG SEMICON MATERIALS CO LTD
Energy-saving reciprocating rubber roller polishing device for textile auxiliary machine
InactiveCN120190688ARevolution surface grinding machinesAbrasive surface conditioning devicesSuction forceGrinding wheel
The invention relates to the technical field of rubber roller polishing, and particularly discloses an energy-saving reciprocating rubber roller polishing device for a textile auxiliary machine, clamping parts are fixedly connected to the two sides of the top of a workbench, a cooling part is fixedly connected to the middle of the top of the workbench, a transmission part is fixedly connected to the top of the workbench, and the transmission part is fixedly connected to the top of the workbench. And the inner side of the grinding part is in threaded connection with the output end of the transmission part, the grinding part comprises a base, the inner side of the base is in threaded connection with the output end of the transmission part, and a grinding shell is fixedly connected to the top of the base. According to the energy-saving reciprocating type rubber roller grinding device for the textile auxiliary machine, the connecting mechanism is arranged, chippings falling during grinding wheel cleaning can be sucked into the connecting shell through suction force generated by work of the connecting mechanism, the bottom plate on the inner side of the connecting shell is provided with an inclined face and is provided with a round hole, and the chippings can be ground into the grinding wheel under the combined action of gravity and the suction force; and the materials smoothly enter the baffle frame through the round holes for centralized collection.

Owner:WUXI TONGLI TEXTILE MASCH TECH CO LTD
Eccentric shaft grinding control method capable of avoiding workpiece collision
The invention relates to the technical field of feeding amount control, in particular to an eccentric shaft grinding control method capable of avoiding workpiece collision, which comprises the following steps: in the process of grinding an eccentric shaft by a processing machine tool, acquiring the actual rotating speed of a grinding wheel at each moment in a preset local time period before the current moment and the actual feeding amount of the grinding wheel at the current moment in real time; calculating the rotating speed variation; determining the friction balance degree of the grinding wheel at the current moment; and the abrasion coefficient of the grinding wheel at the current moment is obtained, the adjusted feeding amount of the grinding wheel at the current moment is determined, and the feeding amount of the grinding wheel is controlled and adjusted through a control algorithm. The feeding amount of the grinding wheel is adjusted in real time, the feeding amount of the grinding wheel is controlled more accurately, collision and impact in the grinding process are effectively avoided, the risk of damage to workpieces and equipment is reduced, and the machining precision of the eccentric shaft is improved.

Owner:HANDAN HENGGONG METALLURGICAL MACHINERY CO LTD
Feed motion calculation method for double-output-shaft five-axis numerical control tool grinding machine
The invention discloses a feeding motion calculation method for a double-output-shaft five-axis numerical control tool grinding machine, and the method specifically comprises the steps: building a unified coordinate system according to the mechanism characteristics and solving demands of the grinding machine, and the unified coordinate system comprises a machine tool coordinate system, a machining coordinate system, a workpiece coordinate system and a grinding wheel coordinate system; grinding machine structure parameters are set and comprise the offset of the original point of a machining coordinate system relative to the C axis, grinding machine structure offset examples of the offset of the original point of the machining coordinate system relative to the B axis, the grinding wheel installation distance and the grinding wheel installation direction; a universal grinding machine feeding kinematics equation is established by considering the inward and outward mounting conditions of main shafts at the left end and the right end of the grinding wheel; and solving based on grinding wheel installation transformation and grinding machine stroke constraint. According to the method for solving the partitioned selective solution based on the actual travel limit of the machine tool, the solution is more universal and practical, the actual travel limit of the machine tool is met, and the method has good adaptability.


Owner:SOUTHWEST JIAOTONG UNIV
Grinding wheel online state monitoring system and method based on multi-sensor fusion
The invention discloses a grinding wheel online state monitoring system and method based on multi-sensor fusion. The monitoring system is composed of an acquisition module, a data preprocessing module and a man-machine interaction module. Firstly, multi-source information collection is carried out through a sensor, then time-frequency domain analysis and wavelet transformation are carried out on the collected information in a targeted mode, and data feature values are extracted; according to the method, image characteristic values such as a Hilbert spectrum are obtained through Hilbert-Huang transform and fast Fourier transform, high-dimensional data are subjected to importance evaluation through a reelief algorithm to obtain multi-modal data with high correlation, a ResNet-DenseNet-LSTM hybrid network model is built, accurate monitoring of the online state of the grinding wheel is achieved through data driving, and the accuracy of the online state of the grinding wheel is improved. And finally, integrating a monitoring algorithm in an upper computer interface. According to the invention, sufficient monitoring precision and accuracy can be ensured, online monitoring is realized, and a complicated process of offline data processing is avoided.

Owner:HARBIN INST OF TECH +2
Crankshaft outer circle and end face integrated grinding equipment and grinding method
The invention relates to crankshaft outer circle and end face integrated grinding equipment and a grinding method, and relates to the field of grinding equipment. According to the technical scheme, a single grinding machine is used for replacing three grinding machines in the original process, equipment investment is greatly reduced, labor and energy consumption are saved, the production efficiency is improved due to process concentration, and meanwhile the problems that an existing process is large in occupied area and large in labor consumption are solved; the outer circle and the end face of the crankshaft part can be synchronously ground through one-time clamping, positioning errors caused by multiple times of clamping are avoided, a numerical control system can conveniently monitor and compensate machining errors in real time, and the high-precision requirement is guaranteed. Specifically, a grinding wheel spindle is matched with an axial driving assembly to achieve synchronous grinding of the outer circle and the end face of the crankshaft. Diamond needles are welded to the outer circle and the side face of the grinding wheel dressing diamond roller in a buried mode, and dressing of the outer circles of a fixed grinding wheel and a movable grinding wheel and the end face of the movable grinding wheel can be completed. A metal guide wheel is selected to support a crankshaft spiral groove face, guide wheel abrasion is reduced, and grinding precision and efficiency are further guaranteed.

Owner:WU XI SHI MING XIN JI CHUANG YOU XIAN GONG SI
Automobile production stamping part burr treatment device
The invention discloses an automobile production stamping part burr treatment device and relates to the technical field of workpiece machining, the automobile production stamping part burr treatment device comprises a workbench and a workpiece needing burr treatment, a supporting plate is fixedly installed at the top of the workbench, a conveying assembly is arranged at the front end of the supporting plate, and a burr treatment assembly for conducting burr treatment on the workpiece is arranged on the supporting plate; the conveying assembly is used for conveying the workpieces to one side of the burr processing assembly. According to the automobile production stamping part burr treatment device, the first grinding wheel is responsible for grinding the surface of the end of a workpiece, the second grinding wheel is focused on burr cleaning of the edge of the workpiece, the two grinding wheels work at the same time, and burr treatment of the end and the edge of the workpiece can be completed at a time; the complex operation of multiple times of clamping and different working procedures in a traditional treatment mode is avoided, the treatment efficiency is improved, meanwhile, positioning errors possibly caused by multiple times of clamping are reduced, and the overall treatment quality of the workpiece is guaranteed.

Owner:JILING PROVINCE ADAVANTAGE MOULD CO LTD
Centerless grinding machine based on laser online measurement and automatic compensation functions
ActiveCN120480686ARevolution surface grinding machinesGrinding feed controlLaser detectionGrinding wheel
The invention discloses a centerless grinding machine based on laser on-line measurement and automatic compensation functions, and relates to the technical field of machine tool machining equipment. Rectangular protection covers are symmetrically arranged above a movement cavity; the driving assembly is arranged in a movement cavity formed in the base, one end of the driving assembly is connected with the inner wall of the movement cavity, and the other end of the driving assembly is in intermittent fit with the rectangular protection cover; the grinding wheel is slidably arranged in the rectangular protection cover on one side; the guide wheel is slidably arranged in the rectangular protection cover on the other side, the center line of the grinding wheel is parallel to the center line of the guide wheel, a workpiece supporting plate is arranged between the grinding wheel and the guide wheel, and the adjusting assemblies are arranged on the sides, away from the driving assembly, of the grinding wheel and the guide wheel correspondingly. The workpiece is ground into the preset size, the diameter of the ground workpiece is detected through the laser detector, and if the diameter does not meet the standard, the distance between the grinding wheel and the guide wheel is finely adjusted through the adjusting assembly.

Owner:JIANGSU TRI M SPECIAL METALS