
Steel tube used for hollow stabilizer bar of automobile and manufacturing method of steel tube
A manufacturing method and technology for a stabilizer bar, which are applied in the field of steel pipes for hollow stabilizer bars for automobiles and the manufacturing field thereof, can solve the problems of high manufacturing cost and unsatisfactory torsional fatigue performance of products, and achieve low price, ensure anti-torsion fatigue performance, and ensure cooling The effect of bend formability
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Applications(China)
- Current Assignee / Owner
- Publication Date
- 2019-03-05
Smart Images
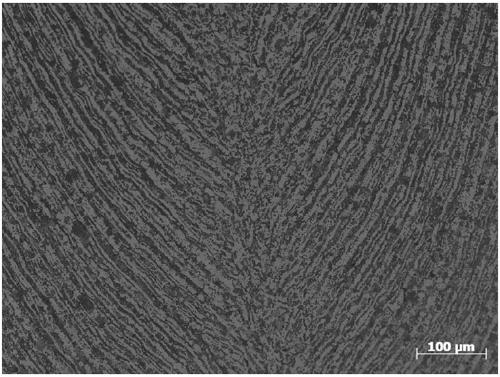
Figure 1 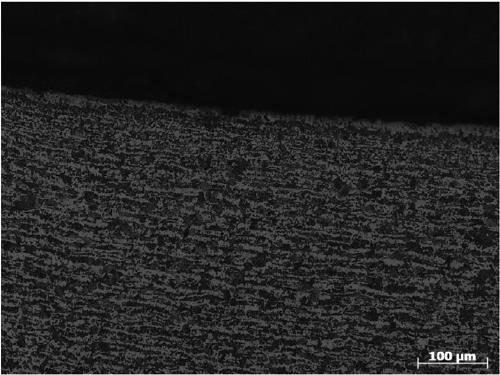
Figure 2 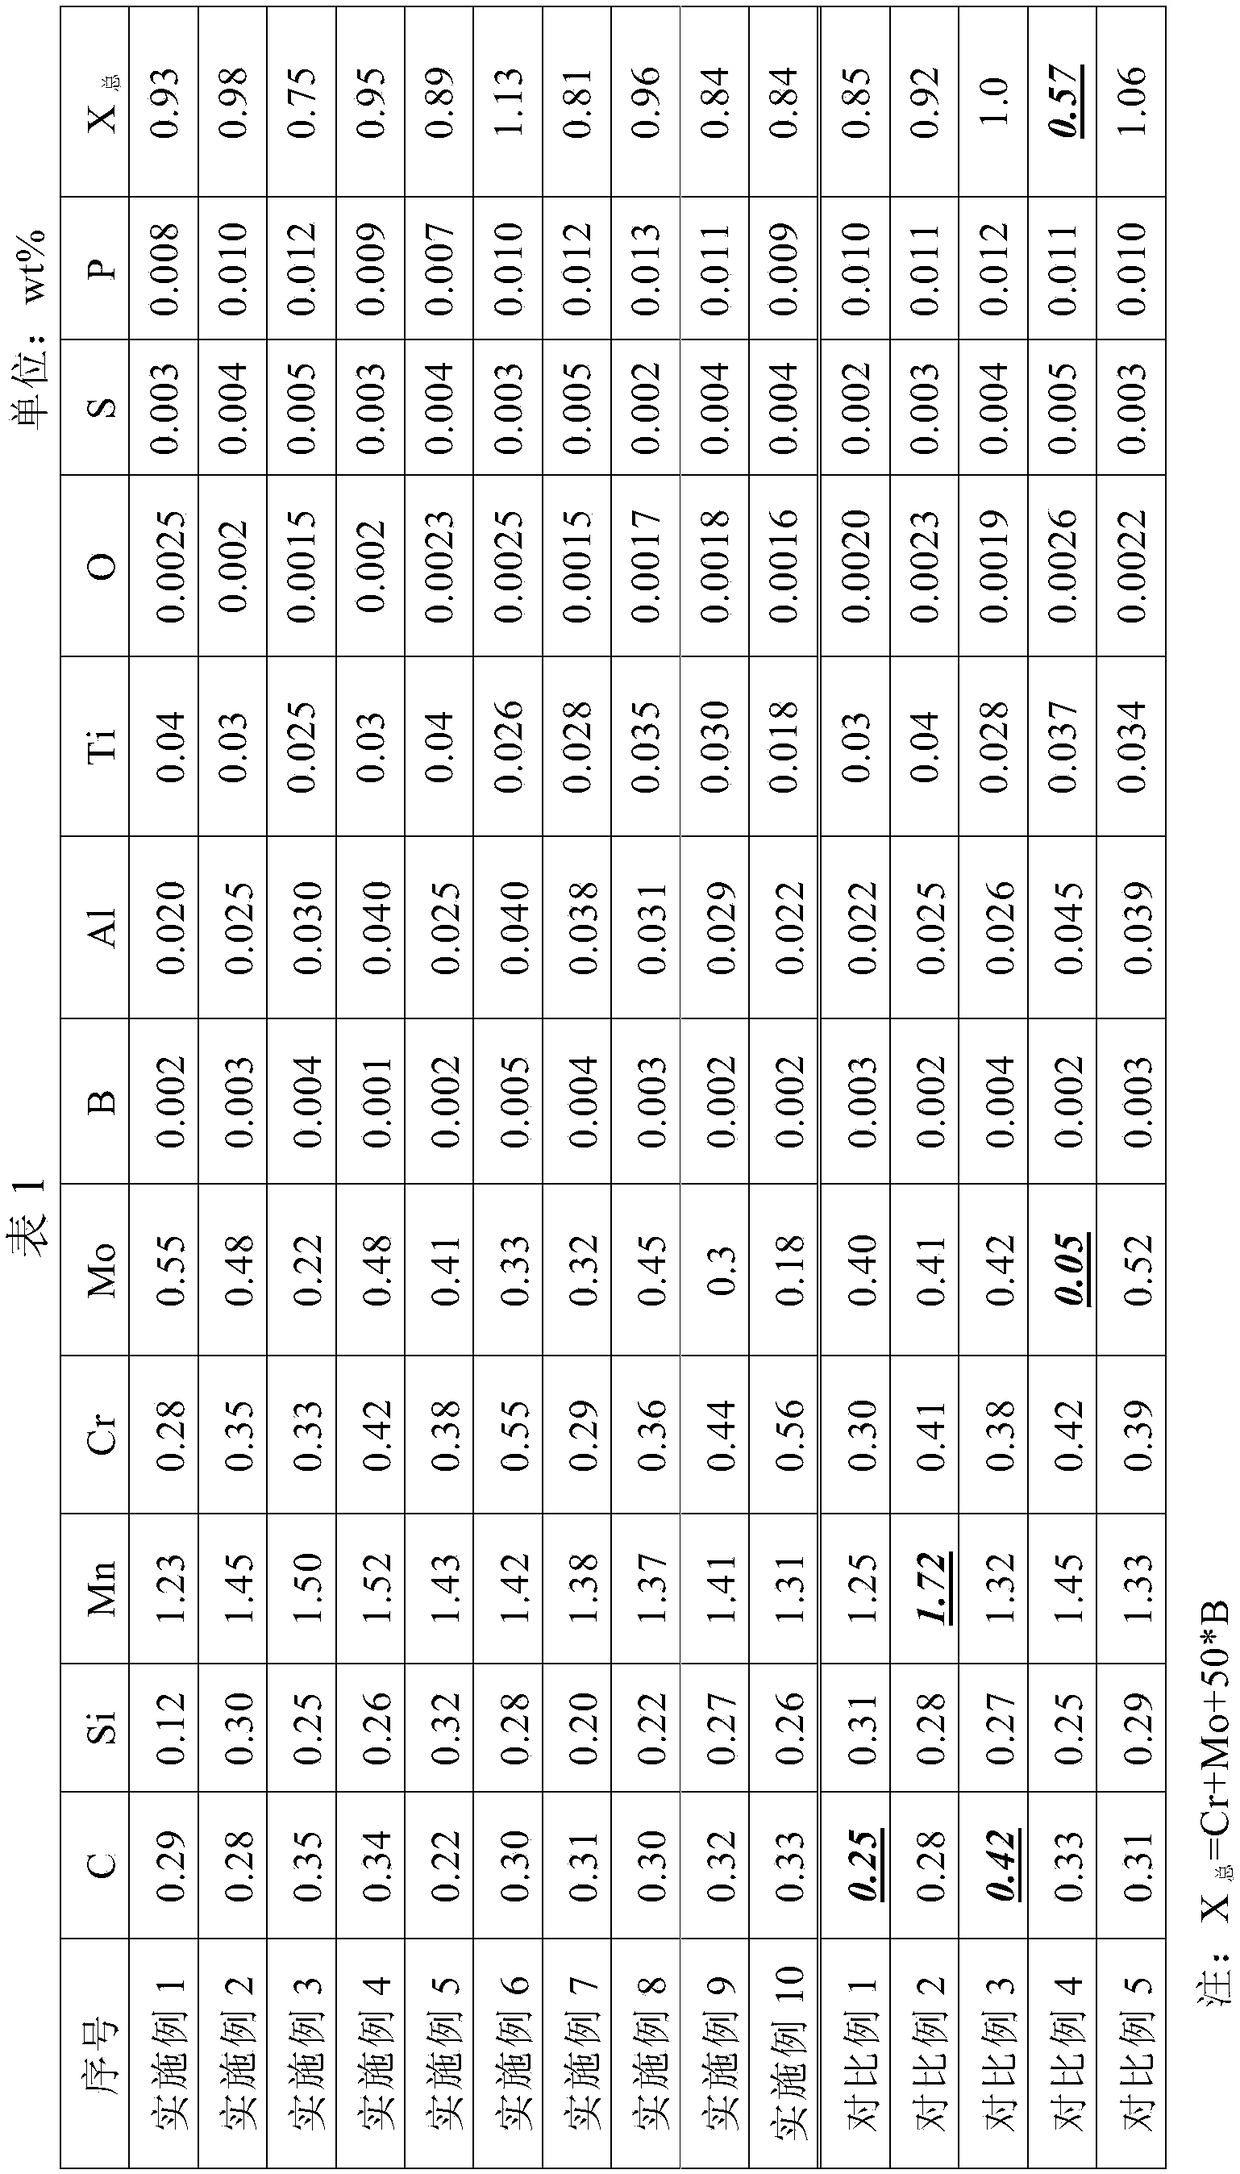
Figure 3
Abstract
Description
technical field
[0001] The invention relates to a steel pipe for a hollow stabilizer bar of an automobile and a manufacturing method thereof. Background technique
[0002] The stabilizer bar for the automobile transmission shaft is an auxiliary elastic component in the automobile suspension system. The function of the lateral stabilizer bar is to prevent the body from excessive lateral roll when turning, and to keep the body as balanced as possible. Roll degree and improved ride comfort. The stabilizer bar is actually a horizontal torsion bar spring, which can be regarded as a special elastic element in function. When the body only moves vertically, the suspension on both sides deforms the same, and the stabilizer bar does not work. When the car turns, the body rolls, the suspension on both sides jumps inconsistently, the outer suspension will press against the stabilizer bar, and the stabilizer bar will be twisted, and the elastic force of the bar body will prevent the wh...
Examples
Embodiment 1-10 and comparative example 1-5
[0052] Manufacture steel pipe 1-10 for automobile hollow stabilizer bar of the present invention and comparative example 1-5 according to the following steps, and it comprises steps as follows:
[0053] (1) Carry out smelting, casting and rolling coils according to the mass percentage ratio of the chemical elements shown in Table 1, the coiling temperature of the coils is 780-900°C;
[0054] (2) Uncoiling and stripping the coil;
[0055] (3) The mother tube is obtained by welding by high-frequency resistance welding, the internal and external burrs are removed, and the temperature of the on-line induction heat treatment after welding is 550-800 °C;
[0056] (4) Carry out pickling, phosphating and saponification to the welded mother pipe;
[0057] (5) Use cold drawing or cold rolling to carry out cold processing to the finished product size. The elongation coefficient of each cold processing is 1.3-1.8. Between each cold processing, an intermediate heat treatment process of 50...