
Method for producing wear-resistant composite roller
A manufacturing method and technology of composite rolls, which are applied in the field of roll manufacturing, can solve problems such as low strength of the roll core, easy occurrence of slag inclusions in the joint layer of the roll core and the roll body, and roll peeling, so as to achieve good wear resistance of the roll and improve the joint layer quality, anti-oxidation effect
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Applications(China)
- Current Assignee / Owner
- Publication Date
- 2010-06-16
- Estimated Expiration
- Not applicable · inactive patent
Smart Images
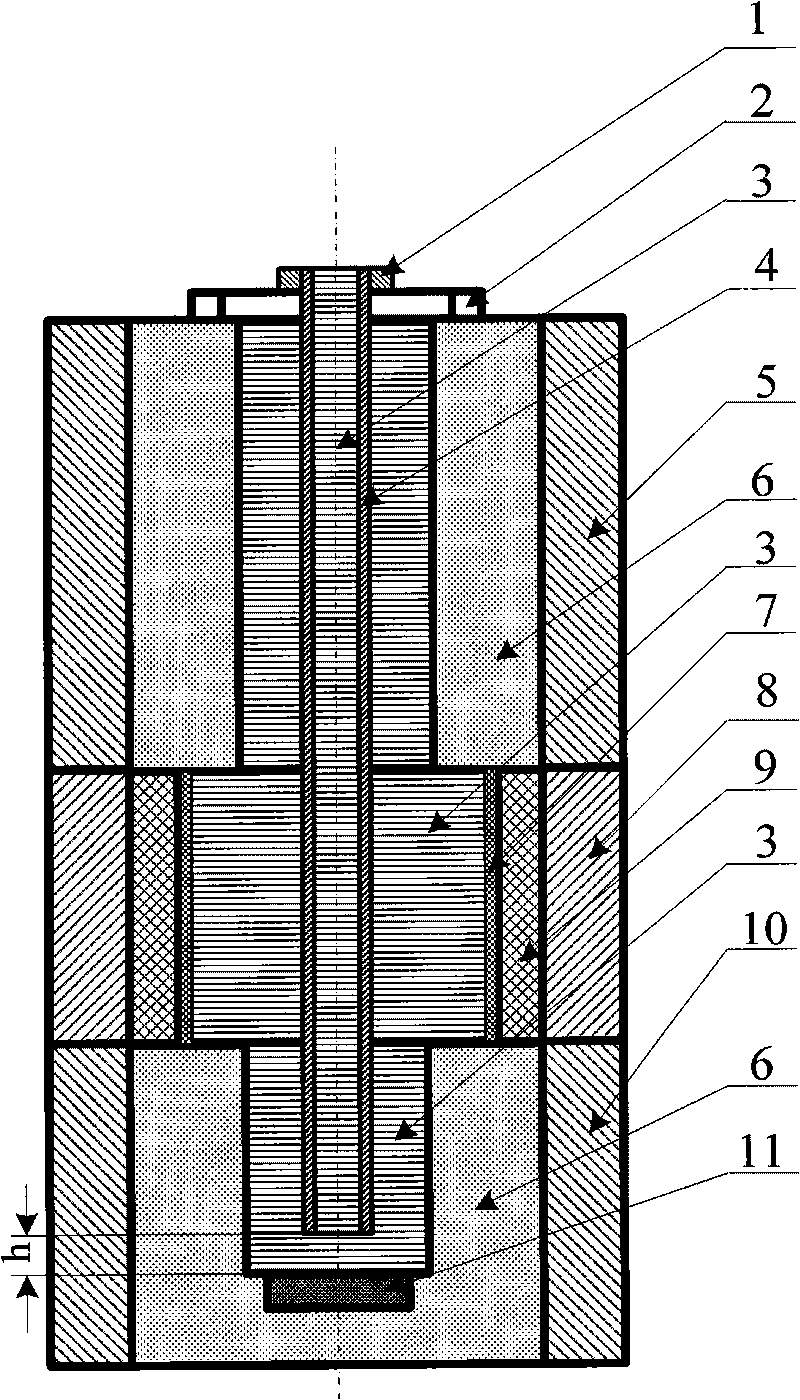
Figure 1 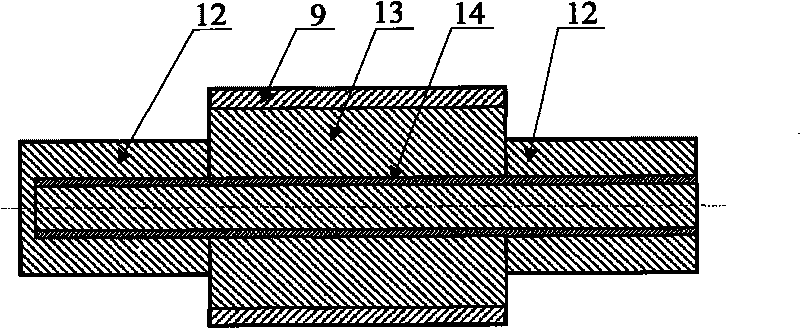
Figure 2
Abstract
Description
technical field
[0001] The invention relates to a method for manufacturing a composite roll, in particular to a method for manufacturing a large-scale wear-resistant composite roll with a roll body diameter greater than 500mm, and belongs to the technical field of roll manufacturing. technical background
[0002] Composite casting roll refers to the composite casting of the outer layer, the core and the roll neck of the roll body, which are made of two or more materials. performance. There are three types of roll compound casting methods: semi-flush compound casting, centrifugal compound casting and overflow compound casting. Centrifugal cladding is widely used in the casting production of large clad rolls because it is easy to achieve good metallurgical bonding between the roll body and the core and is easy to operate. Centrifugal casting composite roll technology has three forms: vertical centrifuge casting method, horizontal centrifuge casting method and inclined centri...
Examples
Embodiment 1
[0024] The centrifugal casting method is used to cast φ650mm×1700mm high-speed steel composite roll, the outer layer of the roll is high-speed steel, and the roll center and roll neck are ductile iron. First, the high-speed steel and the ductile iron are smelted separately in an electric furnace. Then pour the wear-resistant outer layer high-speed steel metal liquid of the composite roll into the cold type (8) installed on the horizontal centrifuge. After the roll outer layer high-speed steel metal liquid has been poured, add 300 ℃ baked steel into the cold type Glass slag (7), the composition (mass fraction) of glass slag is 42.5% SiO 2 , 41.8% Na 2 O, 9.5% B 2 o 3 and 6.2% Al 2 o 3 , the amount added is controlled at 2.0kg / m 2 (the inner surface of the wear-resistant outer layer of the roll), which evenly covers the inner surface of the outer layer of the roll under the action of centrifugal force. After the outer layer of high-speed steel liquid is solidified, the ce...
Embodiment 2
[0026] The centrifugal casting method is used to cast φ730mm×2600mm high-nickel-chromium cast iron composite roll. The outer layer of the roll is high-nickel-chromium cast iron, and the roll center and roll neck are nodular cast iron. First use electric furnace to smelt high-nickel-chromium cast iron and nodular cast iron respectively. Then pour the wear-resistant outer layer high-nickel-chromium cast iron metal liquid of the composite roll into the cold mold (8) installed on the horizontal centrifuge. The glass slag (7) baked at ℃, the composition (mass fraction) of the glass slag is 51.3% SiO 2 , 33.1% Na 2 O, 7.6% B 2 o 3 and 8.00% Al 2 o 3 , the amount added is controlled at 2.5kg / m 2 (the inner surface of the wear-resistant outer layer of the roll), which evenly covers the inner surface of the outer layer of the roll under the action of centrifugal force. After the outer layer of high-nickel-chromium cast iron liquid is solidified, the centrifugal cold form is hois...