
Large cylindrical forge piece forging and rolling composite production technology
A rolling compounding and production process technology, applied in the field of large cylindrical forging forging rolling compounding production process, can solve the problems of complex free forging process, low production efficiency, high energy consumption, etc., and is beneficial to final forming and production. The effect of high efficiency and low energy consumption
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Applications(China)
- Current Assignee / Owner
- Publication Date
- 2018-12-14
- Estimated Expiration
- Not applicable · inactive patent
Smart Images
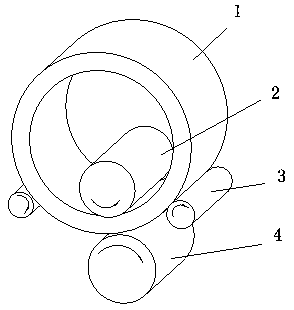
Figure 1
Abstract
Description
technical field
[0001] The invention relates to the technical field of pressure vessel manufacturing, in particular to a composite production process of forging and rolling large cylindrical forgings. Background technique
[0002] Cylindrical forgings refer to axisymmetric hollow forgings whose axial length is greater than its outer diameter. Large cylindrical forgings usually refer to cylindrical forgings with a forging weight greater than 5 tons, including large nuclear power cylindrical forgings, large hydrogenation reactor cylinders Shaped forgings and cylindrical forgings for coal liquefaction reactors belong to the key components required in the fields of nuclear power equipment, petrochemical equipment and coal liquefaction equipment, respectively. At present, the production and manufacture of large-scale cylindrical forgings in my country is basically produced by free forging. Process size.
[0003] The size of large cylindrical forgings produced by the free forging...
Examples
Embodiment Construction
[0021] The present invention will be described in further detail below in conjunction with the accompanying drawings.
[0022] A kind of forging and rolling composite production process of large cylindrical forgings, it comprises the following preparation steps:
[0023] Step 1. Heat the steel ingot according to the design requirements and place it on the free forging equipment for upsetting, elongating and punching. When the forging ratio of the steel ingot is ≥ 4.6, prepare a cylindrical forging blank 1. Measure the surface temperature of the blank 1. When When the surface temperature of the blank 1 is lower than the final forging temperature + 100°C, the blank 1 is heated until the surface temperature of the blank 1 is greater than or equal to the final forging temperature + 100°C; the blank 1 that meets the temperature requirements is lifted to the top of the rolling equipment, The cylinder wall of the blank 1 is loaded between the upper roll 2 and the lower roll 4, and th...