
An electrochemical layer-by-layer polishing device for additively manufactured metal tubular parts
A technology of additive manufacturing and polishing device, which is applied in electrolytic components, electrolytic process, etc., can solve the problems of low selectivity of polishing area, uneven polishing, etc., and achieve the effect of avoiding excessive polishing and improving polishing precision
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Patents(China)
- Current Assignee / Owner
- Publication Date
- 2021-05-04
Smart Images
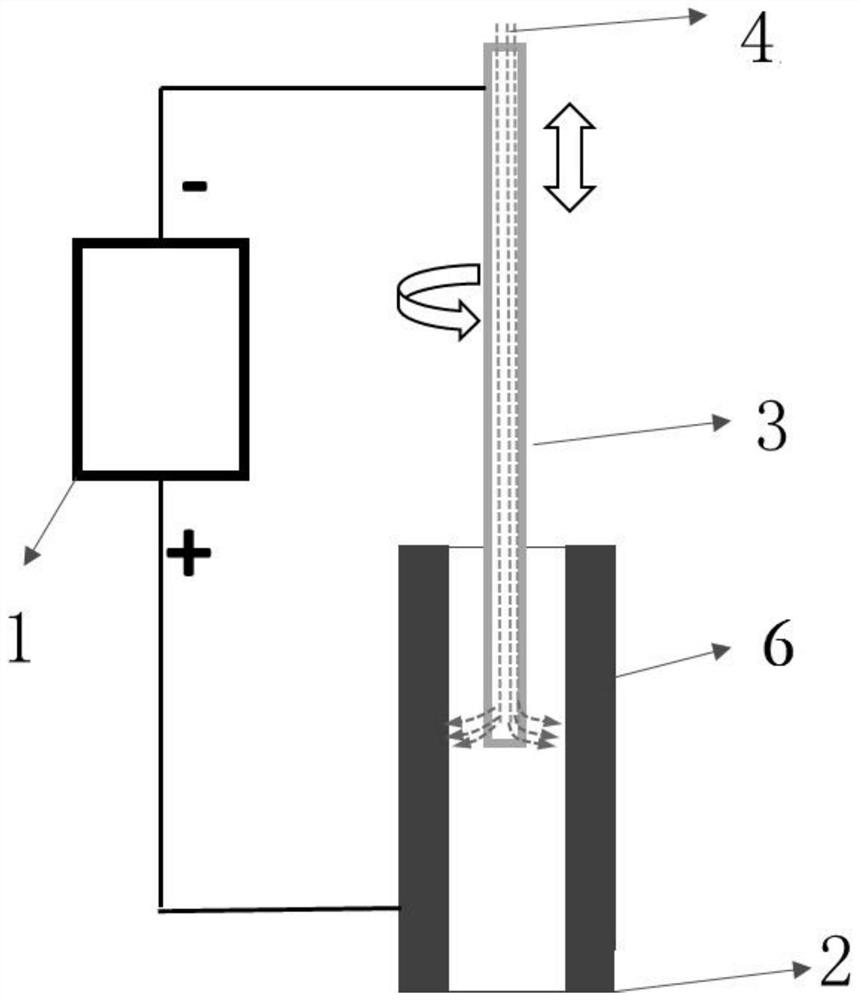
Figure 1 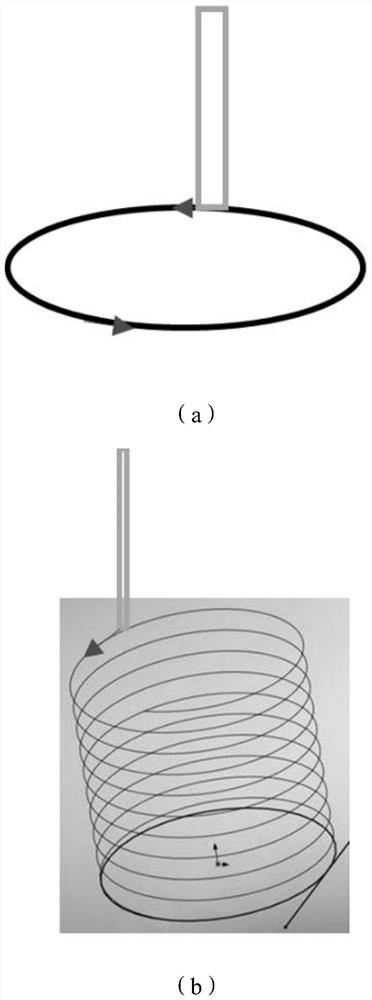
Figure 2 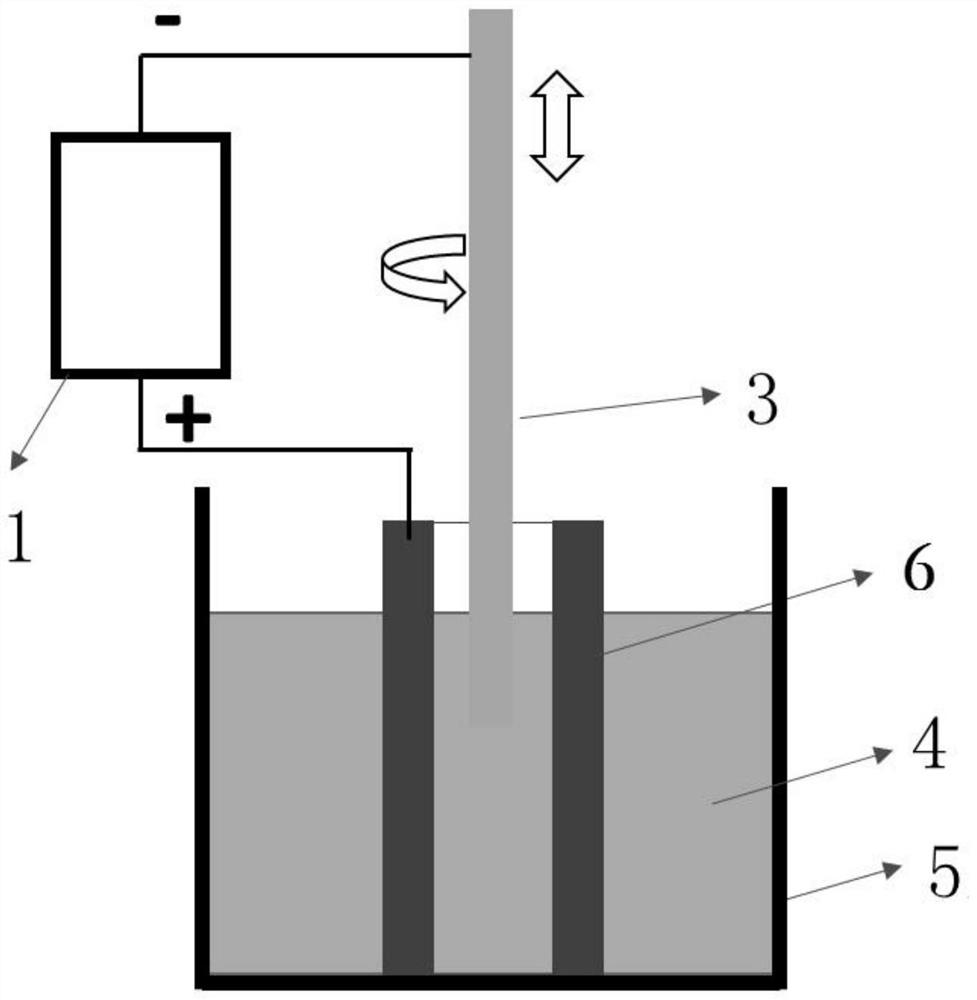
Figure 3
Abstract
Description
technical field
[0001] The invention relates to the technical field of precision surface treatment, in particular to an electrochemical layer-by-layer polishing device for additively manufacturing metal tubular parts. Background technique
[0002] Additive manufacturing technology, also known as 3D printing technology, is an advanced technology that directly manufactures physical parts from CAD design data through material layer-by-layer accumulation. Additive manufacturing technology can complete the manufacture of many complex structural parts that are difficult to complete by traditional processing, and greatly reduce the processing steps and shorten the construction period. However, due to the characteristics of 3D printing processing technology, the surface roughness of metal parts manufactured by 3D printing is generally still between Ra10μm and 50μm, while the surface roughness of mechanical finishing can reach below Ra2.5μm. Due to the high roughness of metal compon...
Examples
Embodiment 1
[0035] Such as figure 1 As shown, the electrochemical liquid spraying layer-by-layer polishing device for additively manufactured metal tubular parts provided in this embodiment includes a control drive part, a power supply 1 , a workpiece placement area 2 , an electrode 3 and a working liquid 4 . Wherein, the workpiece placement area 2 is used to place the additively manufactured metal tubular member 6 to be polished; the electrode 3 is a hollow structure, and a spray hole is opened around the lower end of the electrode 3 .
[0036]When working, the additively manufactured metal tubular part 6 to be polished is placed on the workpiece placement area 2, the electrode 3 extends into the interior of the additively manufactured metal tubular part 6, and the working fluid 4 is transferred from the storage of the working fluid 4 through an external pump. The working fluid is extracted from the working fluid tank and flows into the inside of the electrode 3; the positive pole of the...
Embodiment 2
[0051] Such as image 3 As shown, the electrochemical immersion layer-by-layer polishing device for additively manufactured metal tubular parts provided in this embodiment includes a control drive unit, a power supply 1 , electrodes 3 , a working solution 4 and a working solution tank 5 . Wherein, the working fluid tank 5 is used for placing the additively manufactured metal tubular part 6 and the working fluid 4 to be polished.
[0052] When working, the additive manufacturing metal tubular part 6 to be polished and the working fluid 4 are placed in the working fluid tank 5, and the electrode 3 extends into the inside of the additive manufacturing metal tubular part 6; the positive electrode of the power supply 1 is connected to the additive manufacturing metal Tubular part 6, the negative pole of power supply 1 is connected to electrode 3; the control driving part is connected to electrode 3 and / or the metal tubular part 6 of additive manufacturing, and the control driving p...
Embodiment 3
[0065] In this embodiment, additive manufacturing technology is used to manufacture a stainless steel cylindrical part with an outer wall diameter of 10 mm and an inner wall diameter of 6 mm, and the device provided in Embodiment 1 is used for electrochemical polishing.
[0066]After configuring the working fluid according to the experimental data, assemble the device provided in Example 1, use the electrode as the cathode, and the stainless steel cylindrical part to be polished as the anode, and extend the electrode into the stainless steel cylindrical part; then start the control drive part and connect When the pulse power is turned on, the working fluid is sprayed onto the inner surface of the stainless steel cylindrical part through the liquid spray holes around the lower end of the electrode; finally, the driving part is controlled to control the electrode to move from top to bottom at a predetermined speed and rotate to realize layer-by-layer polishing. After a period of ...