
Reduction of no2 emissions in process gases
The combination of SCR with a sulfur-resistant dual-purpose catalyst system effectively reduces NO2 and SO2 in process gases, addressing inefficiencies in carbon capture by minimizing NO2 slip and enhancing CO2 capture efficiency and reducing operational costs.
Patent Information
- Application Number
- PCT/EP2025/050689
- Authority / Receiving Office
- WO · WO
- Patent Type
- Applications
- Current Assignee / Owner
- Priority Date
- 2024-01-17
- Filing Date
- 2025-01-13
- Publication Date
- 2025-07-24
AI Technical Summary
Existing carbon capture processes are hindered by the irreversible reaction of NO2 and SO2 with alkaline absorption solutions, leading to degradation and increased energy consumption, necessitating additional chemical replacement and waste management, while current NOx removal methods like SCR result in minor NO2 slip and CO oxidation inefficiencies.
A process combining SCR with a sulfur-resistant dual-purpose catalyst system that reduces NO2 to NO and oxidizes CO to CO2, using CO and O2 present in the gas, followed by SO2 oxidation to SO3 and condensation, achieving sub-ppm NO2 concentrations suitable for carbon capture.
The process significantly extends the life of carbon capture absorbents by minimizing NO2 and SO2 concentrations, reducing operational costs and waste, and enhancing energy efficiency by integrating CO oxidation and sulfuric acid production.
Smart Images
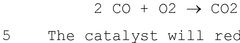
Figure IMGF000010_0001 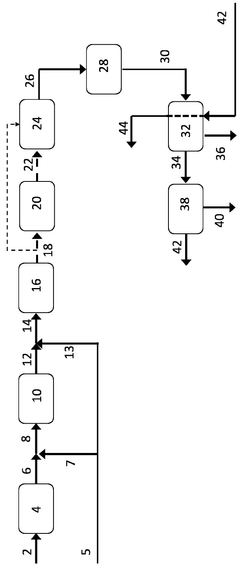
Figure 00000027_0000 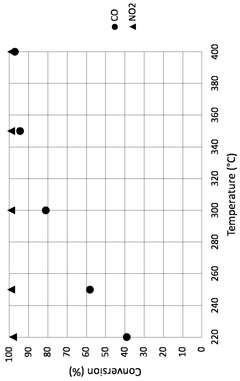
Figure 00000028_0000
Abstract
Description
[0001] Reduction of NO2 emissions in process gases TECHNICAL FIELD The invention relates to a process for reduction of NO2 emissions from a process gas denitrification and desulfurization plant, to provide a cleaned process gas fora carbon capture process or emission to the atmosphere as anon-opaque gas. BACKGROUND Due to climate change concerns, there is an increasinginterest in capturing CO2 in process gases from processesinvolving oxidation of carbonaceous feed stocks, e.g., cement production, power plants firing biomass or fossil fuels, metal production, carbon black production andrefinery operations such as fluid catalytic cracking (FCC).The CO2 concentration in these process gases will typicallybe in the concentration range 5-30 vol% and thus a process plant to capture the CO2 and concentrate the CO2 into analmost pure CO2 stream is required to be able to use theCO2 for sequestration, enhanced oil recovery or utilization for food / beverages or production of chemicals. The most mature technologies for CO2 capture are the so- called regenerative amine-based or hot potassium carbonate (HPC) processes. Common for these two processes is that the(acidic) CO2 gas is absorbed into an alkaline solution inan absorption process, typically an irrigated packed bedabsorption tower. The CO2 loaded absorption liquid leavingthe absorption process is then transferred to adistillation / stripping process in which the CO2 is releasedas an almost pure CO2 stream and the CO2-depletedabsorption solution is recovered and returned to the CO2absorption process. The CO2 desorption typically take placein a stripping column, where heat is supplied in a reboiler in the bottom of the column and the overhead from the column is cooled and partly condensed; the condensate,which is primarily water, is returned and only the pure CO2leaves the column. The heat supplied is typically low- pressure steam but can be any stream with high energy density and temperatures low enough to protect theabsorption liquid from thermal degradation. This could beheat transfer oil, process gas or hot air. The absorption solution is not CO2 specific, which meansthat other acidic compounds such as SO2 and NO2 also areabsorbed into the solution. These two compounds will reactalmost irreversibly with the absorption solution and formso-called heat-stable salts, which will degrade the absorption solution, resulting in lower CO2 capture efficiency and / or increased energy consumption in the distillation / stripping process.To maintain high efficiency of the CO2 capture process, itwill then be necessary to either take out a fraction of the degraded absorption solution and replace it with fresh absorption solution or carry out a chemical regeneration of the absorbent solution. Both solutions will increase the operating cost of the carbon capture process and provide a waste stream, which need to be taken care of.It is therefore desirable to minimize the concentration ofSO2 and NO2 in the process gas before it enters the carboncapture plant. The most common means for removal of SO2 from process gases is by absorbing and reacting the (acidic) SO2 with an alkaline reactant, such as aqueous solutions of e.g. NaOH, NH3, Mg(OH)2 and CaCO3. These processes typically takeplace in the 40-60 °C range. These processes have been usedfor decades and are characterized by being effective and relatively cheap and simple. The drawbacks of these processes are that a chemical needs to be supplied and a (waste-) product needs to be removed, requiring additional logistics and storage facilities. Low local availability of chemicals or no use of the product can significantly increase the operating expenses of this solution. Another way to remove SO2 from a process gas is to catalytically oxidize the SO2 to SO3 and, in combination with water, condense sulfuric acid which can be sold as a valuable chemical. This process is often referred to as a wet gas sulfuric acid technology, abbreviated WSA. It requires that H2O and O2 is present in the process gas, which is very often the case. However, they could be addedas O2 or air and liquid water or steam, should they not bepresent in sufficient amounts. NOx is commonly removed by the so-called selective catalytic reduction (SCR) process, in which NH3selectively reacts with NOxto form N2and H2O. The process will have an inevitable small slip of NO, NO2and / or NH3and ifoxidation of SO2 is also included in the process this stepwill increase the NO2 concentration as the step of SO2oxidation also oxidizes NO and NH3. Due to the deterioration of the amine capture solution by the NO2, a step of NO2removal is desired.KR20220075898 discloses a process in which CO and NO2 arereacted upstream an SCR process. This process will not avoid the minor slip of NO2from the SCR process. SUMMARY A process is therefore provided for reduction of NO, NO2 and optionally SO2 concentrations in a process gas, said process comprising subjecting said process gas to: a. an SCR step, catalytically converting NO and NO2in said process gas to N2 and H2O by reaction with a first NH3 stream, b. a combined NO2 reduction and CO oxidation step inthe presence of a sulfur resistant dual-purpose catalyst, thereby catalytically reducing NO2 to NO in said process gas by reaction with CO and oxidizing CO to CO2 by reaction with O2, characterized in that the NO2 / NOX molar ratio in the process gas, after passing through steps a and b, is lower than 0.05, preferably lower than 0.02 and most preferably lower than 0.01.Further details of the technology are presented in thefollowing description, examples, and patent claims.LEGENDS Figure 1 illustrates the overall process of the invention Figure 2 shows the efficiencies of the sulfur resistant dual-purpose catalyst from Example 2. DETAILED DISCLOSURE Conversion of SO2 and NOX (NO2+NO) in process gases is well known in the industry and there are numerous mature technologies to accomplish such gas phase conversions, each technology having inherent advantages and disadvantages. The present invention presents a novel layout of the combination of the SCR reaction and WSA process and introduction of a new sulfur resistant dual-purpose catalyst system to reduce NO2 emissions down to sub-ppm concentrations, while also eliminating CO emissions. The new layout is very suitable for process gases containing reducing species, such as CO, which is both used as a reactant and later oxidized to CO2. Such process gases could e.g. be from a Fluid Catalytic Cracking process, a Carbon black producing process, or a metallurgical process such as a steel mill. The present invention provides a process for reduction of NO, NO2 and optionally SO2 concentrations in a process gas.The process gas – prior to step (a) of the process –typically comprises 10-5,000 ppmv CO and 1-1,000 ppmv NO+NO2, as some NO may be converted to problematic NO2. The process gas typically comprises up to 30%, preferably 5-20% CO2.Suitably, the process gas – prior to step (a) – alsocomprises an excess of CO with respect to NO2, i.e., theCO / NO2molar ratio is greater than 1. The process gas also has one or more of the following: -an O2 concentration in the range 2-20 vol%,- an H2O concentration in the range 2-40 vol% and- an SO2 concentration in the range 100-10,000 ppmv.The remainder of the process gas is suitably N2, Ar and m nor impurities. The process gas containing SO2, NOX and a reducing species may be either heated or cooled to a temperature in the optimal 250-450 °C range. Before or after this temperature regulation, the process gas can have passed through aparticulate filter (e.g., bag filter, ceramic candlefilters or electrostatic precipitator) and / or an process gas blower to clean the gas from particulate matter (dust) and to provide the necessary gas pressure to pass theprocess gas through the process plant. Therefore, theprocess gas is suitably preconditioned by one or more preconditioning steps selected from: -removal of particulate matter e.g., in a bag housefilter, electrostatic precipitator or candle filter, -adjustment of temperature by heating or cooling e.g.by means of heat exchangers, burners, heaters, and -adjustment of pressure e.g., by means of a compressoror blower (e.g. to about atmospheric pressure).In the broadest aspect, the process comprises subjectingsaid process gas to:a. an SCR step, followed byb. a combined NO2 reduction and CO oxidation stepThe NO2 / NOX molar ratio in the process gas, after passing through steps a and b, is lower than 0.05, preferably lower than 0.02 and most preferably lower than 0.01. In the SCR step (a), NO and NO2 in said process gas is catalytically converted to N2 and H2O by reaction with a first NH3 stream. To reduce NOX from process gases, the so- called catalytic SCR (Selective Catalytic Reduction) process is the most widely used process to reach very low NOX concentrations. The process requires the addition of NH3 in order for the catalytic reactions to take place: 4NO + 4 NH3 +O2 ^ 4 N2 + 6 H2ONO2 + NO + 2 NH3 ^ 2 N2 + 3 H2OAn NH3 source is added to the process gas such that the NH3 / NOX ratio in the process gas becomes close to 1 in order to achieve high NOX conversion to N2 on the SCR catalyst. To obtain an even distribution of NH3 and NOX, a static mixing device is typically positioned between the NH3 injection point and the SCR catalyst. The NH3 source can be liquid NH3, an aqueous NH3 solution, NH3 vapor or urea and can be added to the process gas as a liquid via a number of spray nozzles or as a vapor, preferably together with an amount of carrier gas to ensure good mixing with the process gas. The NH3 used in step a is added to the process gas such that the obtained NH3 / (NO+NO2) ratio is between 0.9 and 1.1.The reaction typically takes place in the 250 – 450 °Ctemperature range, and at a pressure around 1 atm. The so-called SNCR process is the non-catalytic version of the SCR and requires temperatures in the 700-1000 °C range. The process is not as effective as the catalytic version. In a low temperature application, ozone (O3) can be added to the process gas to oxidize the NO to NO2 / HNO3, which can then be washed out in an absorption process. On the SCR catalyst, most of the NOX will react with the NH3, producing a SCR process gas with decreased concentrations of both NOx and NH3. Typically, the SCR catalyst is designed for more than 90% NOX conversion, up to 98-99%. If the NOX conversion requirement is very high, it is often the (local) NH3 / NOX ratio which is the determining factor and therefore it may be necessary to use a second SCR catalyst and install a mixing device between the first and second SCR catalyst to ensure an even NH3 / NOX ratio before the second catalyst. It may also be desired to add an additional amount of NH3. The SCR catalyst has been used for decades and many chemical formulations can be used for the purpose of this invention. The vanadium / titania / tungsten-based catalyst on a monolithic support is the most well-known type of SCR catalyst. Downstream the SCR catalyst, the process gas will have a very low concentration of NO, NO2 and unconverted NH3. The SCR catalyst will not convert CO and thus the CO concentration is unchanged.The combined NO2 reduction and CO oxidation step (b) takesplace in the presence of a sulfur resistant dual-purpose catalyst, thereby catalytically reducing NO2 to NO in said process gas by reaction with CO and oxidizing CO to CO2 by reaction with O2. The CO and O2 required in this step are typically presentin the process gas itself, in the necessary concentrations. However, it is possible to add CO and / or O2 from an external source, as required. The present disclosure describes the use of a sulfurresistant dual-purpose catalyst system, which first uses COto reduce the NO2 to NO and then oxidizes the remaining CO to CO2 according to the reactions: NO2 + CO ^ NO + CO2 the problematic NO2 to NO, which will not be absorbed into a downstream carbon capture plant and, thus, the lifetime of the carbon capture absorbent can be significantly increased. Furthermore, the catalyst oxidizes the toxic CO gas to the much less problematic CO2, which will be captured in a downstream carbon captureplant. The reaction rate of NO2 with CO should be higher than the reaction of CO with O2, otherwise the NO2 reduction will not take place. Reaction rates for thesereactions can be controlled by means of the catalyst selection, reaction temperature or combinations thereof. The dual-purpose catalyst system may comprise a platinumgroup metal, preferably palladium or platinum in combination with one or more oxides of a metal selected from the group consisting of vanadium, chromium, tungsten, molybdenum, cerium, niobium, manganese, and copper on asupport comprising one or more oxides of metals taken from the group of aluminum, silicon and titanium. Similar effect may also be observed by gold as the active metal. The catalyst is preferably in monolithic form, but pellet-types can also be used. In a development of the process of the invention, SO2 in the process gas may be removed. In this aspect, the process further comprises subjecting said process gas to: a1. an SO2 oxidation step, catalytically oxidizing SO2 in said process gas to SO3 by reaction with O2, between steps a and b (above), c. a cooling and condensation step, in which sulfuric acid vapor is condensed and withdrawn from said process gas, after step b., wherein the NO2 / NOX molar ratio in the process gas, after passing through steps a, a1, b and c is lower than 0.05, preferably lower than 0.02 and most preferably lower than 0.01. As an alternative, SO2 may also be removed in a scrubber or similar following step (b).The NOX depleted process gas from step a. is – in thisaspect - directed to a SO2 oxidation catalyst, which is awell-known vanadium-based alkali-melt catalyst. On thecatalyst, the main reaction is to oxidize the SO2 to SO3 by means of O2 present in the process gas. The SO2 oxidation catalyst reactor is typically designed for higher than 98% SO2 conversion, the maximum conversion is limited by the thermodynamical equilibrium between SO2 and SO3. The SO2 oxidation catalyst will also convert any NH3 slip from the SCR catalyst into either N2 or NOX. Depending on the gas composition and catalyst temperature, typically 40- 70 % of the NH3 is converted to N2, the remaining NH3 becomes NOX. The SO2 oxidation catalyst also equilibrates the reaction between NO and NO2: 2NO + O2 ^ NO2The reaction is exothermal and thus more NO2 is formed at lower temperature and with high O2 concentration. The O2 concentration is fixed from the process gas and the SO2 conversion typically determines the operating temperatureof the catalyst, i.e., there is not much which can be doneto reduce the formation of NO2. At 400 °C, around 30-50 % of the total NOX concentration will exist as NO2. In the 350-450 °C temperature range, the SO2 oxidation catalyst will not oxidize the CO. After SO2 oxidation (step a1), the NO2 concentration is typically in the 2-20 ppm range, which will have a highly negative impact on the downstream carbon capture plant and may also cause a brown / red plume in the stack, should it be directed to atmosphere. Also, the CO concentration is almost unchanged compared to the concentration in the process gas entering the plant.For sulfuric acid producing desulfurization plants, thedual-purpose catalyst system will typically be positionedjust downstream the SO2 oxidation catalyst for reduction ofNO2 to NO and oxidation of the remaining CO to CO2.The dual-purpose catalyst system may comprise a singledual-purpose catalyst arranged to perform both NO2reduction and CO oxidation, or comprise one or more catalyst beds, each one of which is arranged to perform NO2reduction and CO oxidation separately. One or more heatexchanger(s) may be arranged between the catalyst beds.Downstream the dual-purpose catalyst system the SO3 formed in the SO2 oxidation catalyst reacts with H2O present in the gas to form H2SO4 vapor. By process gas cooling e.g.,in an acid resistant glass tube heat exchanger, the H2SO4is condensed and withdrawn as a commercial grade sulfuric acid product. NO and NO2 exhibit very low solubility in the sulfuric acid and only up to a few % of the NOX will be absorbed into the sulfuric acid product. After passing through steps a and b, and optionally steps a, a1, b and c, the process gas suitably has a NO2 concentration below 2 ppmv, preferably lower than 1 ppmv. In one aspect of the process of the invention, CO may beadded to the process gas at any point upstream step b. Asnoted above, the process gas ideally comprises 10-5,000 ppmv CO.In a further aspect of the process, at least one of thecatalytic steps a, a1 and b independently, and preferablyall catalytic steps a, a1 and b, take place in thetemperature range 250-450 °C. More specifically, at leastcatalytic step a1 takes place in the temperature range 350- 450 °C. Suitably, at least one and preferably all of the catalytic steps a, a1 and b take place without active temperature control between the steps, such that heat exchangers between the catalytic steps can be avoided. The cleaned process gas is then highly reduced in concentration of SO2 and NO2 and can thus be directed to a carbon capture plant or be emitted to the atmosphere. Accordingly, following steps a and b, and optionally aftersteps a, a1, b and c – the process gas may be fed to acarbon capture plant, in which a CO2-rich stream isseparated from the process gas. The carbon capture plant is suitably based on absorption of CO2 into an amine blend (primary, secondary and / or tertiary amine), a hot (promoted or unpromoted) potassium carbonate solution or acombination thereof. To increase the carbon capture andenergy efficiency of the hot potassium carbonate process, so-called promoters can be added to the carbonate solution.Such promoters can be amines, amino acids and V-, B- andAs-containing compounds. Optionally, the cleaned processgas can be directed to a final SO2 polisher unit for even further reduction in SO2. FiguresFigure 1 shows a layout of a process plant using the dual-purpose catalyst system to reduce NO2 concentrations tosub-ppm concentrations.A process gas (2), containing NOX (NO+NO2), SOX (SO2+SO3),O2, H2O and CO, coming from an upstream process such as acarbon black process or a fluid catalytic cracker isdirected to a process gas conditioning section (4). In theprocess gas conditioning section (4), particulate mattercan be removed by means of e.g., bag house filter, candlefilter or electrostatic precipitator, the pressure can be increased by means of a blower / compressor and the temperature can be adjusted by heaters / coolers / burners orother means to provide a conditioned process gas (6) readyfor SCR reaction and NOX reduction.An ammonia containing stream (5) is optionally split into afirst ammonia containing stream (7) and a second ammoniacontaining stream (13). A major part of the ammonia isfound in stream (7) and is added to the conditioned processgas (6) and mixed to provide a process gas (8) with anNH3 / NOX ratio close to 1. In (first) SCR reactor (10) most of the NOX is reacted with NH3 to form N2 and H2O. The NOXdepleted process gas (12) leaves the SCR reactor and isoptionally mixed with a minor amount of NH3-containingstream (13) to form a process gas (14) ready for anoptional second SCR reactor (16) where the remaining NOXreduction takes place. The SCR off gas (18) contains lowconcentrations of NO, NO2 and NH3 and is optionally directed to the SO2 oxidation reactor (20) in which SO2 is oxidized to SO3, NH3 oxidized to N2 and NOX and NO is partly oxidized to NO2.The converted process gas (18, 22) is passed to the dual-purpose catalyst reactor (24) in which NO2 is reduced to NO by reaction with CO and CO is oxidized to CO2 by reactionwith O2. The converted process gas, containing very low NO2concentration (26) is cooled to 220-290 °C in heatexchanger (28) and the cooled converted process gas isdirected to the sulfuric acid condenser (32) via line (30).By indirect heat exchange with a colder cooling stream(42), typically air, the cooled converted process gas isfurther cooled to around 70-100 °C and sulfuric acid iscondensed and leaves the corrosion resistant condenser (32)via bottom line (36). The practically sulfuric acid-, SO2-and NO2-free cooled process gas (34) may then be directedto a carbon capture plant (38) in which CO2 is captured andconcentrated and leaves the plant as an almost pure CO2stream (40). The CO2 depleted process gas (42) is then directed to the atmosphere via a stack.Another benefit of integrating WSA and carbon capture isthat the heated cooling stream (44) leaving the sulfuricacid condenser (32) can be used for heating purposes, e.g.,to meet the high energy requirements of the strippingsection of the carbon capture plant, and / or as preheatedcombustion air in other processes and / or carrier gas forthe NH3 for the SCR process. The present technology has been described with respect to a number of embodiments and figures. The person skilled in the art may combine elements from these embodiments and figures as required, within the scope of the invention as defined in the appended claims. All documents referred to herein are incorporated by reference.Example 1This example describes the evolution in NOX concentrationin the process gas as it passes through the process layout(as depicted in figure 1) and shows that the outlet NO2concentration is insensitive to the operation of the SCR system for NOX reduction. The basis is a process gas with 350 ppm NOX from an upstream process, such as a FCC unit or a carbon black production plant. The SCR is designed for 98 % NOX conversion at a NH3 / NOx ratio of 1.0. The actual NH3 / NOx ratio will determine theactual NOX conversion – increasing the NH3 concentration will increase NOX conversion but at the same time increaseNH3 slip from the reactor. Decreasing the NH3 concentrationwill decrease the NOX conversion and result in a higher NOX slip from the reactor. The SO2 oxidation catalyst is very efficient in converting NH3 but is not very selective towards N2. 100% NH3conversion is achieved with an estimated selectivitytowards N2 of 40%, i.e., the remaining 60% becomes NOX.The NO / NO2 ratio depend on the chemical equilibrium in theSO2 oxidation catalyst – at the operating conditions theNO2 / NOX ratio out of the catalyst is approximately 0.4.The sulfur resistant dual-purpose NO2 reduction catalyst ispositioned downstream the SO2 oxidation catalyst and has asNO2 reduction efficiency of 99% when the CO to NO2 molarratio exceeds 1.All three catalyst systems operate in the same temperaturerange of 350-450 °C and it is desirable to operate thethree catalysts at the same temperature, in that way eliminating the need for installing heat exchangers between the catalysts. This simplifies the process layout, process control and reduce the cost of process equipment. The operational NH3 / NOX ratio is not constant as it depends on the evolution in the NOX concentration in the processgas and the speed of analyzing the NOX concentration andadjusting the NH3 flow. Therefore, both spatial and time- wise variations in the NH3 / NOX ratio must be expected. The NO and NO2 concentrations in table 1 show that there isa minimum in NOX slip from the SCR when operating close tothe design conversion efficiency – moving away from thisoptimal operating point in both directions increase the NOX slip. With too low NH3 / NOX ratios, unconverted NOX will leave the SCR, whereas at too high NH3 / NOX ratios, the NOX slip is very low but the NH3 slip is high and the NH3 will be partly converted to NOX on the downstream SO2 oxidation catalyst. The sulfur resistant dual-purpose catalyst systemefficiently reduces the NO2 concentrations, such thatoperation with NO2 concentrations below 0.5 ppm is achievedover a wide range of operation of the SCR reactor.Without the dual-purpose catalyst system, the NO2 emissionoutlet the SO2 oxidation catalyst would be above 3-4 ppm,even during optimal operation.Using a layout with two SCR reactors in series, with process gas mixing between the reactors, will allow for ahigher design SCR conversion, i.e., a lower emission atoptimal operation. However, underdosing or overdoing NH3 will still result in an increase in NOX emissions as seen in Table 1 for NH3 / NOX ratios of 0.9 and 1.10. So-called Ammonia Slip Catalyst (ASC’s) are able to convert NH3-slips from the SCR reactor into N2 with a much betterselectivity than the SO2 oxidation catalyst, i.e., 90%instead of 40%. They will typically be positioned justdownstream the SCR reactor and ensure that the total NOX concentration to the SO2 oxidation catalyst is reduced when NH3 is overdosed. However, it will not ensure NO2 concentration below 2-3 ppm in the SO2 oxidation catalyst outlet gas in the present example.ASC’s can also have CO oxidation capabilities and thuslimit the use of a dual-purpose catalyst system downstreamthe SO2 oxidation catalyst as there will be less or no CO to reduce the NO2 to NO. Similarly installing the dual-purpose catalyst system between the SCR and SO2 oxidation catalyst will reduce both NO2 and CO to the SO2 oxidation catalyst, but NO will bereoxidized to NO2 in the SO2 oxidation catalyst.
[0002] Table 1:. NH3 / NOX0.90 0.95 0.98 1.00 1.02 1.05 1.10ratio SCR-90% 95% 98% 98% 98% 99% 99.5%conversion NOX slip 3517 ppm 7 ppm 7 ppm 73 2 ppm from SCR ppm ppm ppm NH3 slip 00 ppm 0 ppm 7 ppm 1421 37 from SCR ppm ppm ppm ppm Outlet SO2 oxidation catalyst NO slip 2111 ppm 4 ppm 7 ppm 910 14 ppm ppm ppm ppm NO2 slip 147 ppm 3 ppm 4 ppm 66 10 ppm ppm ppm ppm NH3 slip 00 ppm 0 ppm 0 ppm 00 0 ppm ppm ppm ppm Outlet dual purpose catalyst NO slip 3517 ppm 7 ppm 11 ppm 1516 24 ppm ppm ppm ppm NO2 slip 0.2 0.1 < 0.1 0.1 0.1 0.1 0.1 ppm ppm ppm ppm ppm ppm ppm Example 2This example shows the efficiencies of the sulfur resistantdual-purpose catalyst, i.e. it’s ability to first reduce NO2 to NO by means of CO and then oxidize CO to CO2 by means of O2. The data have been measured in a laboratory scale reactorusing a simulated process gas, i.e., containing both NO,NO2, O2, CO and SO2. SO2 does not take part in the reactions but is a common poisoning agent for many catalyst systems. The simulated process gas had the following composition: 3 vol% O2 5 vol% H2O 1000 ppm CO50 ppm NOX (25 ppm NO / 25 ppm NO2) 500 ppm SO2 Balance N2 Pressure was close to atmospheric. Data from different operating temperatures show that theNO2 to NO reduction by CO as reductant is almost completein the 220-400 °C range, whereas the slower CO to CO2 oxidation by O2 requires a temperature above 350 °C to reach a similar conversion, cf. Figure 2. This means that the dual-purpose catalyst has optimalperformance around 350-450 °C, which is the normaloperating temperature for the SO2 oxidation catalyst. Thedual-purpose catalyst system can thus beneficially beinstalled in direct connection with the SO2 oxidation reactor. The same high NO2 reduction and CO conversion can also be obtained at the lower 250 °C, but it will require a largercatalyst volume to reach the very high CO conversion. Inthe process layout shown in Figure 1, an alternative is to locate the sulfur resistant dual-purpose catalyst between the process gas cooler (28) and sulfuric acid condenser (32).
Claims
Claims:
1. A process for reduction of NO, NO2 and optionally SO2concentrations in a process gas (2), said processcomprising subjecting said process gas to: a. an SCR step (10), catalytically converting NO andNO2 in said process gas to N2 and H2O by reactionwith a first NH3 stream (7),b. a combined NO2 reduction and CO oxidation step(24) in the presence of a sulfur resistant dual- purpose catalyst system, thereby catalyticallyreducing NO2 to NO in said process gas by reaction with CO and oxidizing CO to CO2 by reaction with O2, characterized in that the NO2 / NOX molar ratio in theprocess gas, after passing through steps a and b, islower than 0.05, preferably lower than 0.02 and most preferably lower than 0.
01.
2. The process according to claim 1, said process furthercomprising subjecting said process gas to: a1. an SO2 oxidation step (20), catalytically oxidizing SO2 in said process gas to SO3 by reaction with O2, between steps a and b, c. a cooling and condensation step (32), in which sulfuric acid vapor is condensed and withdrawn from saidprocess gas, after step b., wherein the NO2 / NOX molar ratio in the process gas, after passing through steps a, a1, b and c is lowerthan 0.05, preferably lower than 0.02 and most preferably lower than 0.01.
3. The process according to any one of the precedingclaims, wherein the process gas – prior to step (a) -comprises 10-5,000 ppmv CO and 0-1,000 ppmv NO+NO2.
4. The process according to any one of the precedingclaims, wherein the process gas – prior to step (a) –has a CO:NO2molar ratio greater than 1:1.
5. The process according to any one of the precedingclaims, wherein the process gas, after passing throughsteps a and b, steps a, a1, b and c or steps a, b, a1and c, has a NO2 concentration below 2 ppmv, preferably lower than 1 ppmv.
6. The process according to any one of the precedingclaims, wherein the process gas is obtained from aFluid Catalytic Cracking process, a Carbon black producing process, or a metallurgical process such as asteel mill.
7. The process according to any one of the precedingclaims, wherein – prior to step (a) – the process gasfulfils at least one of the following: -an O2 concentration in the range 2-20 vol%,- an H2O concentration in the range 2-40 vol% and- an SO2 concentration in the range 100-10,000 ppmv.
8. The process according to any one of the precedingclaims, wherein CO is added to the process gas at anypoint upstream step b.
9. The process according to any one of the precedingclaims, wherein at least one of the catalytic steps a,a1 and b independently, and preferably all catalyticsteps a, a1 and b, take place in the temperature range 250-450 °C.
10. The process according to any one of the precedingclaims, wherein at least catalytic step a1 takes placein the temperature range 350-450 °C.
11. The process according to any one of the precedingclaims, wherein at least one and preferably all of thecatalytic steps a, a1 and b take place without activetemperature control between the steps.
12. The process according to any one of the precedingclaims, wherein the NH3 used in step a is added to theprocess gas such that the obtained NH3 / (NO+NO2) ratiois between 0.9 and 1.1.
13. The process according to any one of the precedingclaims, wherein – prior to step (a) – the process gasis preconditioned by one or more preconditioning steps(4) selected from: -removal of particulate matter e.g., in a bag housefilter, electrostatic precipitator or candle filter, -adjustment of temperature by heating or cooling e.g.by means of heat exchangers, burners, heaters, and- adjustment of pressure e.g., by means of a compressoror blower (e.g. to about atmospheric pressure).
14. The process according to any one of the precedingclaims, wherein the sulfur resistant dual-purposecatalyst system in step b. is a sulfur resistant dual- purpose catalyst comprising a platinum group metal(e.g., Pt and / or Pd) in combination with one or moreoxides of vanadium, chromium, tungsten, molybdenum, cerium, niobium, manganese and copper, on a supportfrom the group of aluminum, silicon and titanium.
15. The process according to claim 14, wherein the sulfurresistant dual-purpose catalyst system used in step b is monolithic in structure.
16. The process according to any one of the precedingclaims, wherein – in step b. - the reaction rate of NO2with CO is higher than the reaction of CO with O2.
17. The process according to any one of the precedingclaims, wherein – following steps a and b, steps a, a1,b and c or steps a, b, a1 and c – the process gas isfed to a carbon capture plant, in which a CO2-richstream (40) is separated from the process gas.
18. The process according to claim 17 wherein the carboncapture plant is based on absorption of CO2 into an amine blend (primary, secondary and / or tertiary amine),a hot (promoted or unpromoted) potassium carbonate solution or a combination thereof.
19. The process according to any one of the precedingclaims, wherein – in step c - sulfuric acid vapor iscondensed in an indirectly cooled corrosion resistant heat exchanger.
Citation Information
Patent Citations
A method and an apparatus for matching couples using genomic information
KR1020230174812A
Purifying carbon dioxide and producing acid
US20100080747A1
System and Process for Efficient SCR at High NO2 to NOx Ratios
US20210180791A1