
Method for automatically zeroizing a universal edger stand
A technology of edge rolling machine and stand, applied in the direction of metal rolling stand, metal rolling mill stand, metal rolling, etc., can solve problems such as unusability
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Patents(China)
- Current Assignee / Owner
- Publication Date
- 2009-12-09
Smart Images
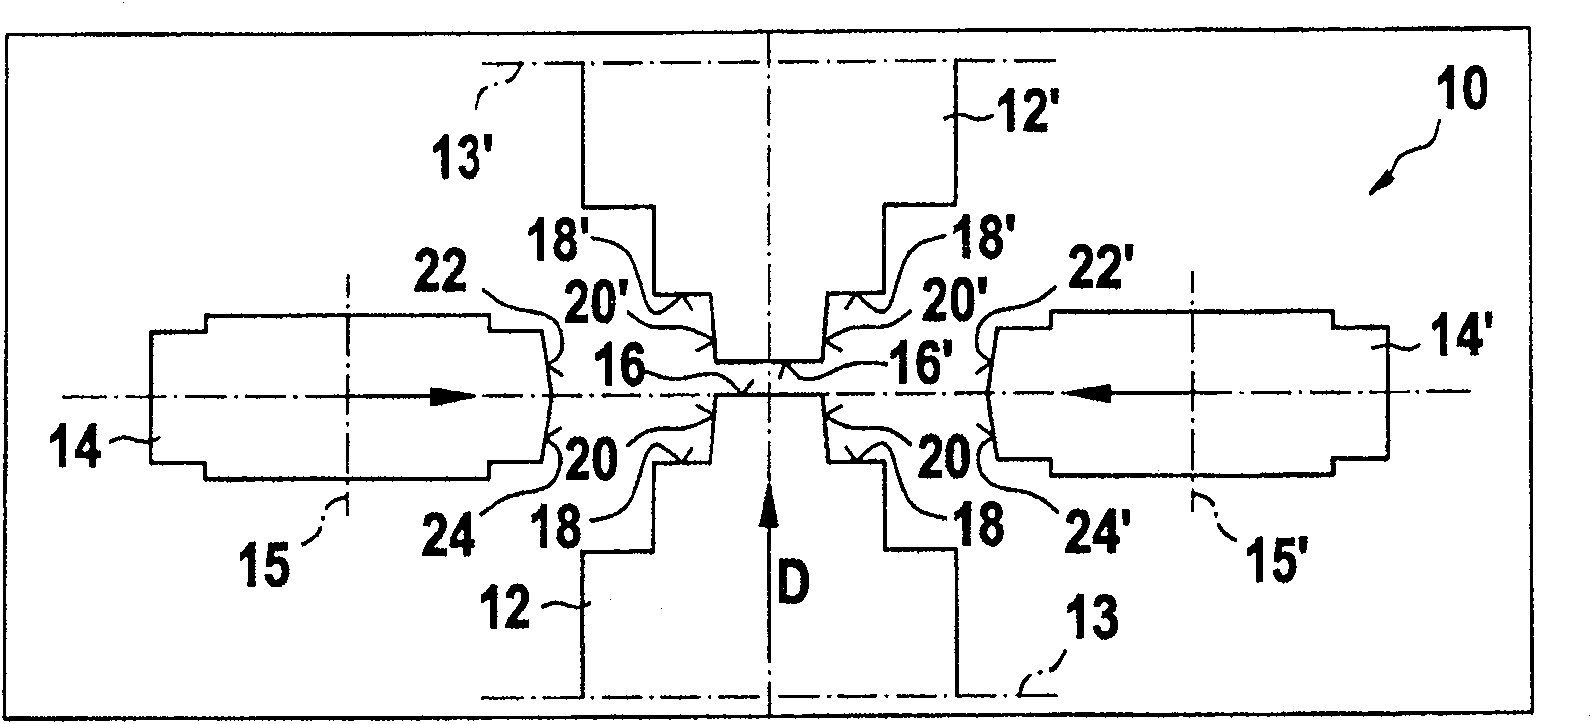
Figure 1 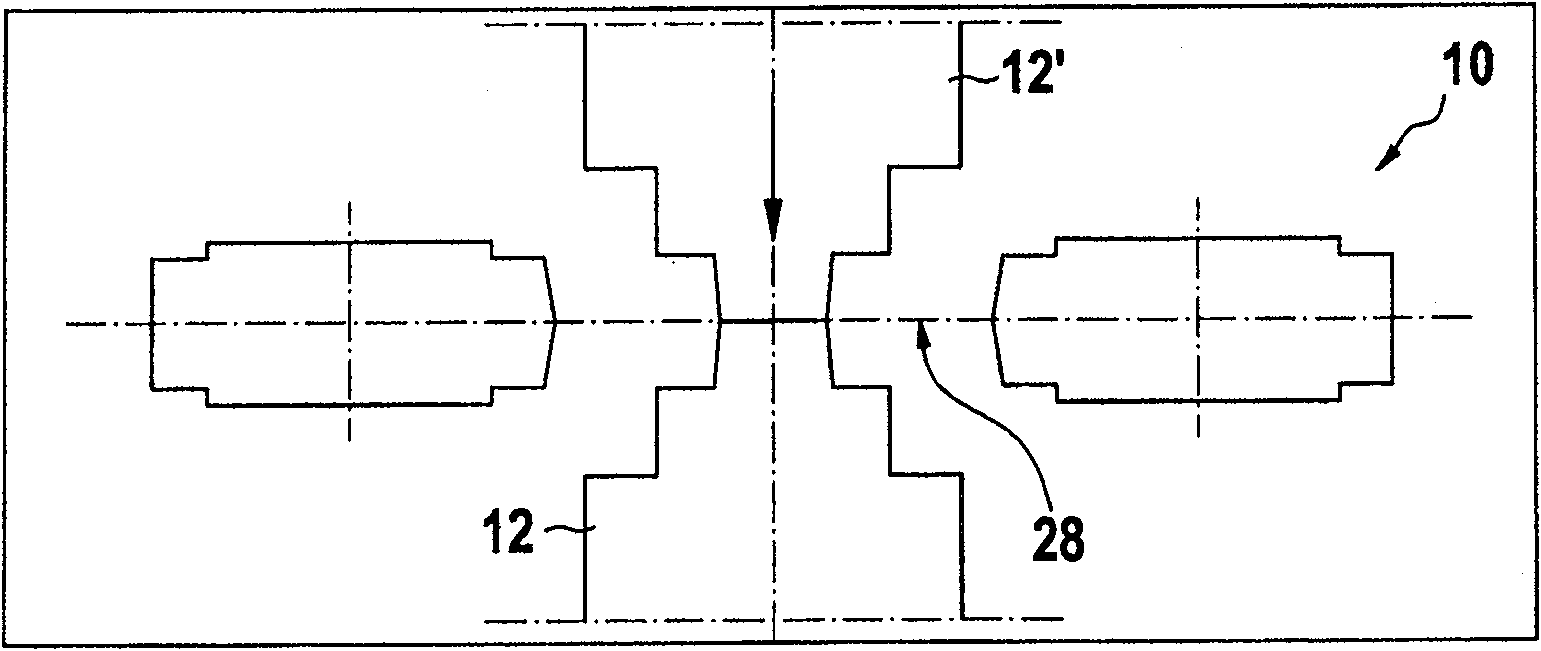
Figure 2 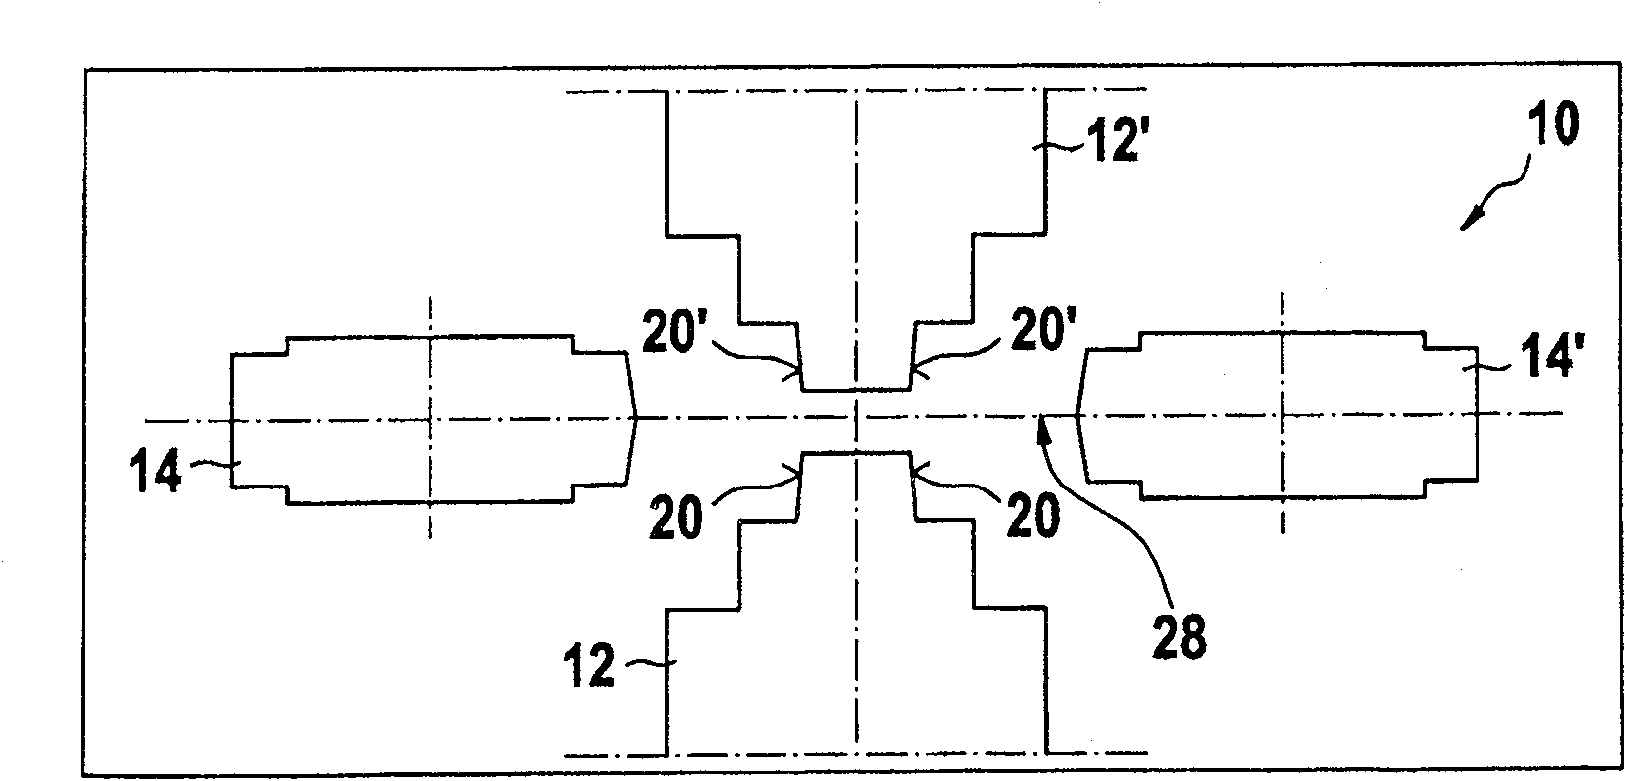
Figure 3
Abstract
Description
technical field
[0001] The invention mainly relates to a method for automatically zeroing the frame of a universal edger for rolling H-shaped cross-section products. Background technique
[0002] The universal edger stand (UE stand) is a rolling stand that can realize the functions of the traditional universal rougher stand (UR stand) and the edger stand (E stand) at the same time, in which The function of the traditional universal roughing mill stand is to rough-roll the flange and web of H-section products, and the function of the edger stand is to rough-roll the flange ends of such products. rolling. Typically, such UE stands are used tandem with conventional UR stands to ensure good dimensional accuracy while increasing the productivity of the rolling operation.
[0003] Like a conventional UR stand, a UE stand includes a set of four rolls, namely an upper horizontal roll, a lower horizontal roll, a left vertical roll and a right vertical roll. Each horizontal roll ha...
Examples
Embodiment Construction
[0020] Further details and advantages of the invention will become apparent from the following detailed description of a number of non-limiting embodiments with reference to the accompanying drawings, in which:
[0021] Figure 1 to Figure 6 Schematic illustration of the rolls of a Universal Edger Stand (UE Stand) for rolling H-section products with a web and two flanges, such as H-beams or H-sheet piles Group 10. The roll set 10 includes: a pair of horizontal rolls 12, 12' (only one half shown), each roll 12, 12' having a horizontal axis of rotation 13, 13'; and a pair of vertical rolls 14, 14', each 14, 14' has a vertical axis of rotation 15, 15'. Each horizontal roll 12, 12' has: a cylindrical rolling surface 16, 16' for rolling the H-section web; two shoulder rolling surfaces 18, 18' for flange rolling. The ends are rolled; and the two conical rolled sides 20, 20'. Each vertical roll 14, 14' has a lower conical rolling surface 24, 24' cooperating with one of the two con...