
Drawing forming device and method of rotary part
A technology of rotary body and parts, applied in the field of deep drawing forming method and device of rotary body parts, can solve the problems of high qualified rate of metal thin-walled rotary body parts, prone to cracking and wrinkling, etc., so as to avoid local wrinkling, The effect of ensuring forming quality and improving wear resistance
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Applications(China)
- Current Assignee / Owner
- Publication Date
- 2016-03-23
Smart Images
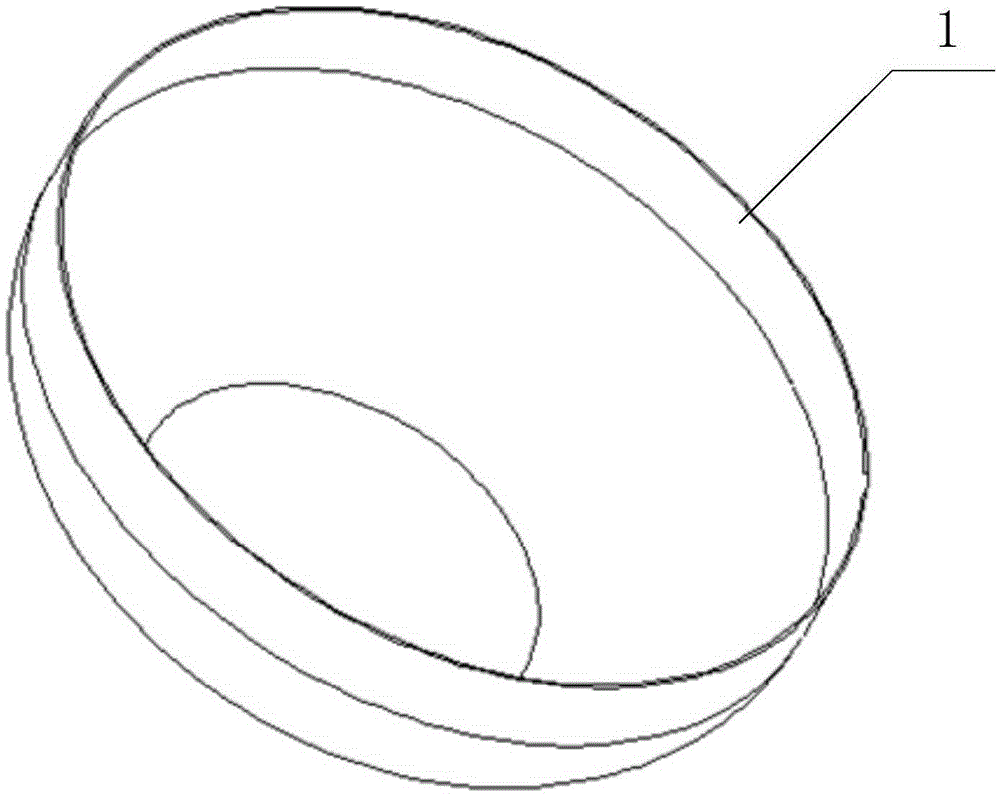
Figure 1 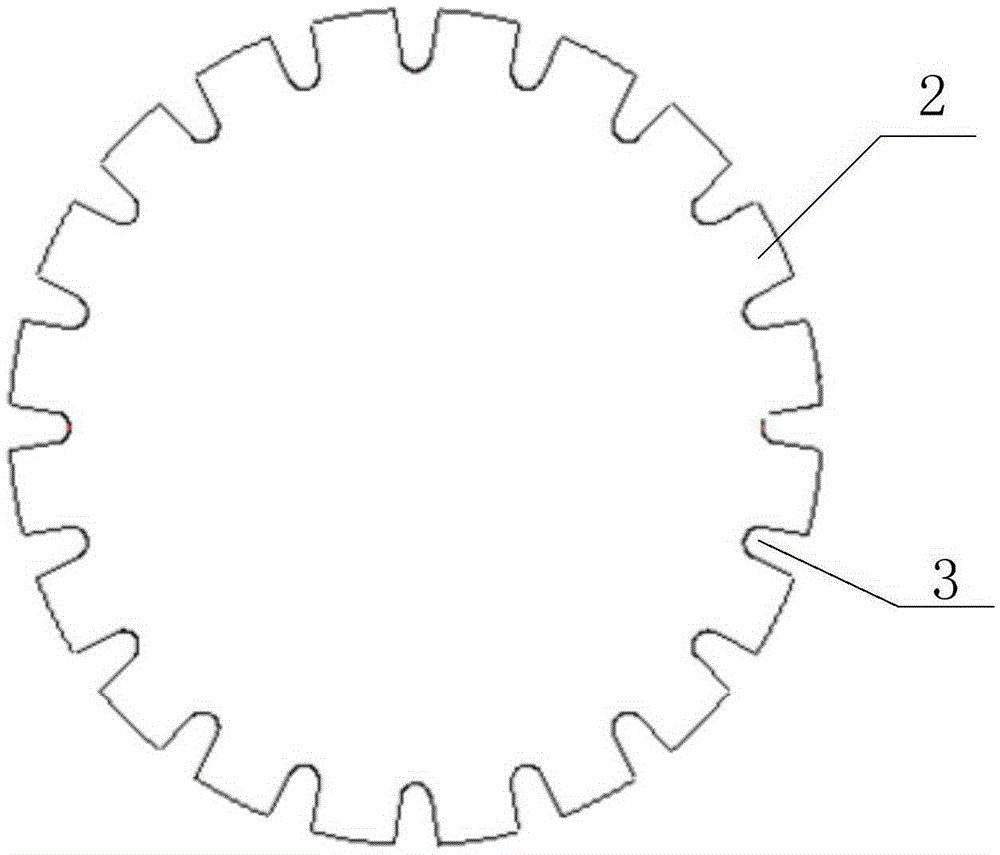
Figure 2 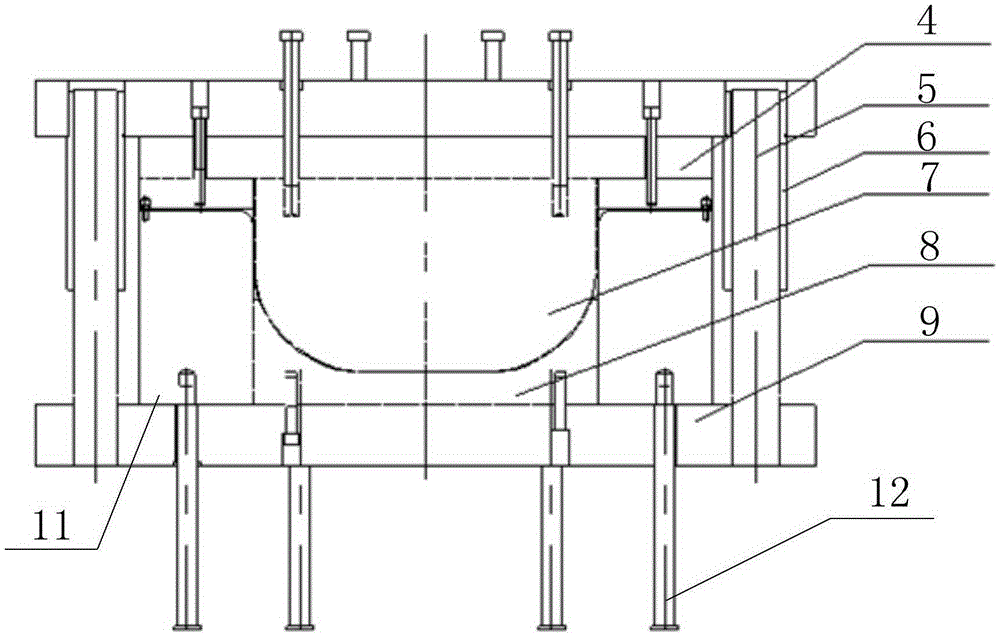
Figure 3
Abstract
Description
technical field
[0001] The invention relates to the technical field of metal material processing and forming, in particular to a method and device for deep drawing and forming of revolving body parts. Background technique
[0002] Pressure vessels, as airtight equipment carrying a certain pressure, have strict requirements on airtightness and pressure resistance. Common pressure vessels include metal pressure vessels, non-metal pressure vessels, and metal-lined composite pressure vessels. The common structure of the metal-lined composite material pressure vessel is a thin-walled rotary body. The thick-walled small-volume structure in the thin-walled rotary body is mainly formed by integral machining of half parts and then welded. The thin-walled large-volume structure is mainly formed by spinning or A method of deep drawing and then welding.
[0003] Stainless steel has become a common material for metal linings due to its excellent corrosion resistance, high temperature ox...
Examples
Embodiment Construction
[0030] The embodiment of the present invention provides a method and device for deep-drawing and forming of rotary parts, which solves the technical problems in the prior art that the metal thin-walled rotary parts are prone to defects such as cracking, wrinkling, and scratches during the deep-drawing process. , Realize the one-time deep drawing forming of metal thin-walled rotary parts, and the qualified rate of formed metal thin-walled rotary parts is high.
[0031] see Figure 1 ~ Figure 4 , the embodiment of the present invention provides a rotary part deep drawing device, the device is used to process the blank 2 into a rotary part 1, and the thinnest wall thickness of the processed rotary part 1 is required to be greater than 0.8mm. The deep-drawing device for rotary parts provided by the embodiment of the present invention includes: an upper combination die 4, a punch 7, a die 8, a die frame 11, a lower die 9, a guide post 5, a guide sleeve 6, a ejector rod 12 and an ej...