
Iron plate finishing coat spraying process
An iron plate and process technology, applied in the field of iron plate topcoat spraying technology, can solve problems such as unfavorable construction personnel and the environment, multiple VOCs, etc., and achieve the effects of good environmental protection effect, shortened construction time, and high paint utilization rate.
Patent Information
- Authority / Receiving Office
- CN · China
- Current Assignee / Owner
- Publication Date
- 2019-03-08
- Estimated Expiration
- Not applicable · inactive patent
Smart Images
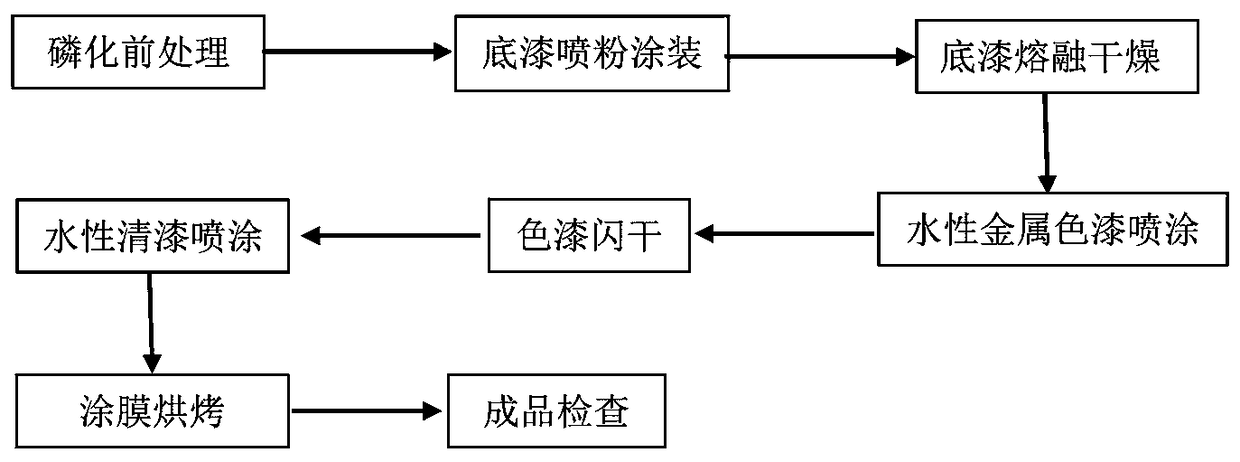
Figure 1 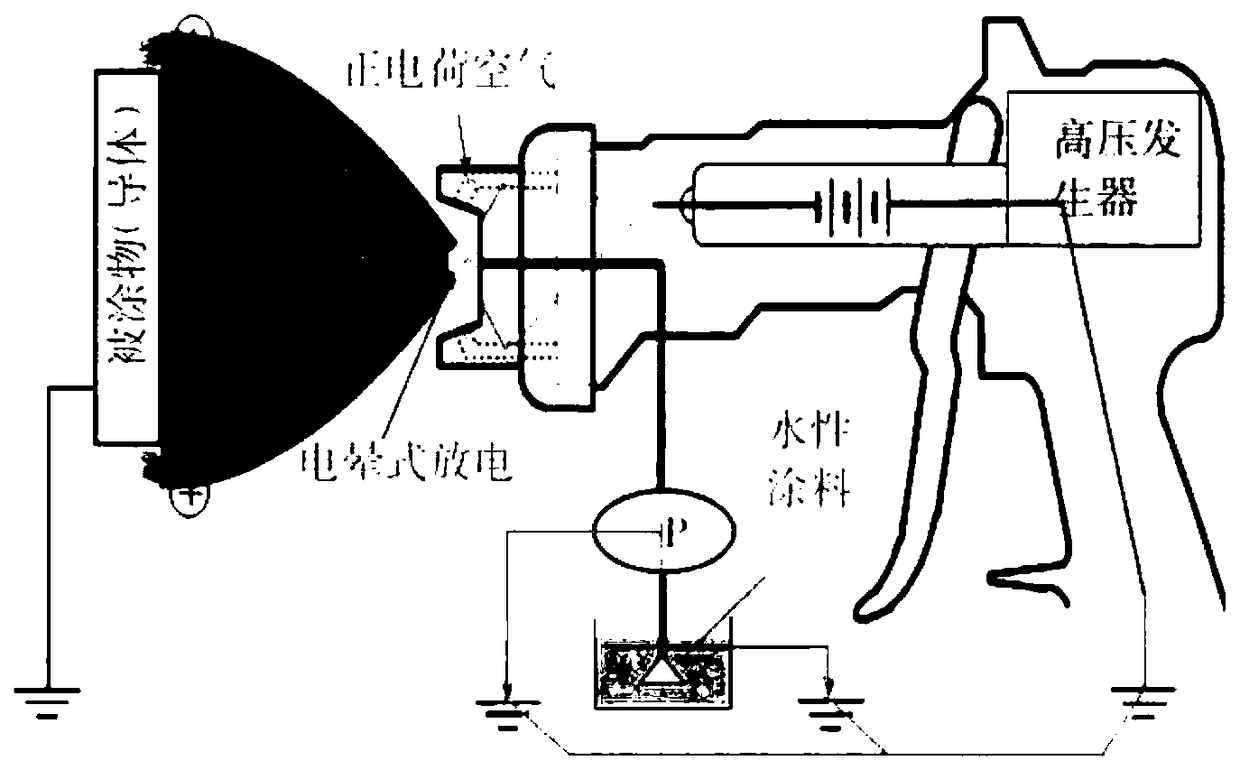
Figure 2 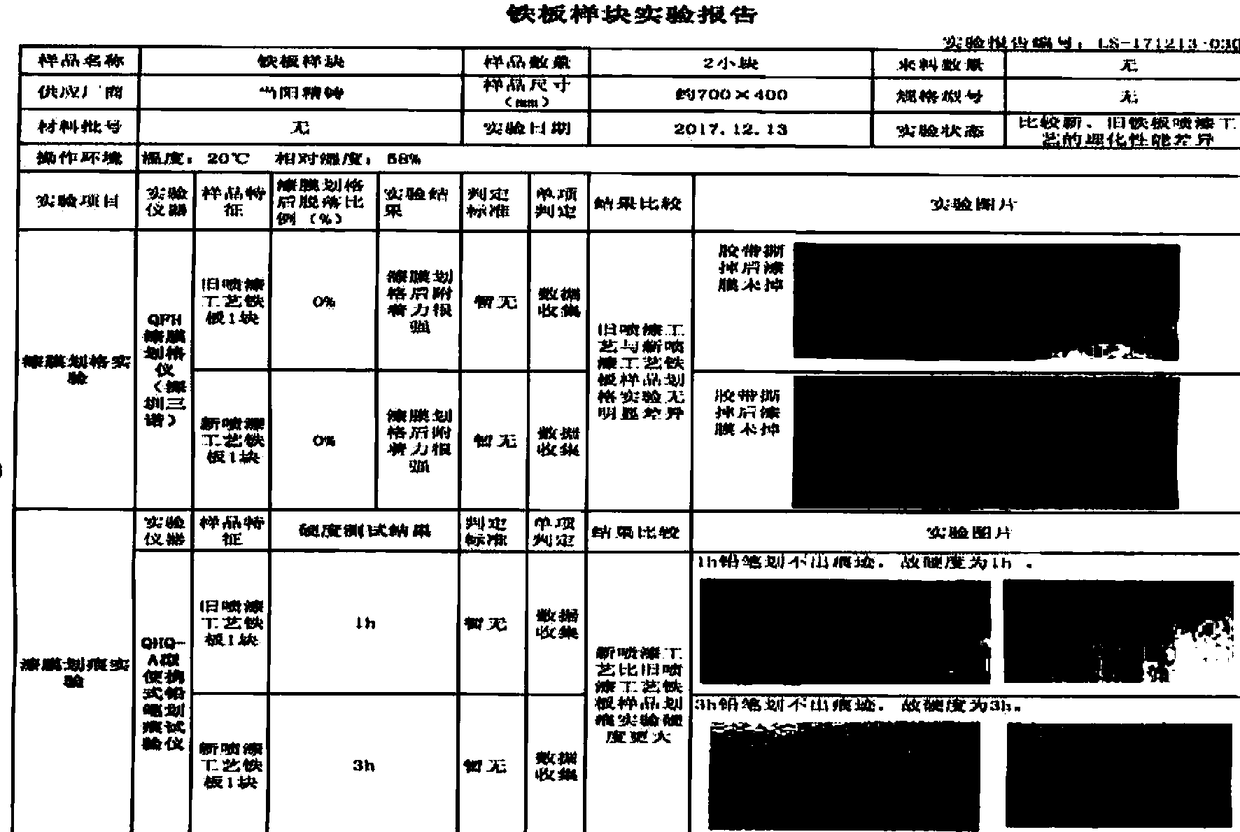
Figure 3
Abstract
Description
technical field
[0001] The invention relates to the technical field of iron plate finish spraying, in particular to an iron plate finish spraying process. Background technique
[0002] The iron plate is an important part of the piano. It is made of cast iron and is the only large piece of metal in the piano that needs to be protected by a paint film. The traditional iron plate topcoat consists of a metal decorative layer and a varnish protective layer, both of which are solvent-based paints with low solid content. During the spraying process, more VOC will be generated, which is not good for construction personnel and the environment. Contents of the invention
[0003] In order to solve the above-mentioned technical problems, the present invention provides a spraying process of iron plate finish paint, which can improve the quality of iron plate paint film and reduce environmental pollution and paint waste.
[0004] The technical scheme adopted by the present invention is...
Examples
Embodiment 1
[0027] Iron plate water-based topcoat spraying process:
[0028] Pre-treatment→dusting→curing→inspection→water-based metallic paint→flash-drying→water-based varnish→baking→finished product
[0029] 1.1 Pre-processing
[0030] The powder can be sprayed only after the iron plate is pre-treated to remove the oil and dust on the surface. At the same time, the surface treatment of the workpiece enhances the adhesion after powder spraying. The film thickness of the surface treatment is 1.5-2g / m 2 .
[0031] The pre-treated workpiece is completely dried and cooled to below 35°C to ensure the physical and chemical properties and appearance quality of the iron plate after powder spraying. The drying of the pre-treatment iron plate is heated by spiral fins, kept at a temperature below 55-65°C for 25-30 minutes and the circulation fan is turned on.
[0032] 1.2 Powder coating
[0033] The construction process powder of electrostatic spraying is specifically glitter powder, and its co...
Embodiment 2
[0063] A kind of iron plate topcoat spraying process, comprises the following steps:
[0064] 1) Use normal temperature shot blasting and sanding treatment, dry and cool for later use;
[0065] 2) Electrostatically spray powder on the iron plate obtained in step 1), then solidify, check the appearance and thickness requirements, if there is any defect, it needs to be sprayed and solidified again; the powder described is glitter powder, and the surface temperature of the workpiece entering the powder spraying room is: ≤50℃, interfering air flow lateral velocity within 2 m near the workpiece in the powder spraying chamber: ≤0.3m / s; electrostatic voltage 60-90kV, current 10-20μA, flow rate pressure 0.30-0.55MPa, atomization pressure 0.30-0.45MPa , The gun cleaning pressure is 0.5MPa, the fluidization pressure of the powder supply barrel is 0.04~0.10MPa, and the distance from the nozzle of the spray gun to the workpiece is 150~300mm. When curing, it is heated by high far infrared...