
Anti-wrinkling cold rolling method for 443 ultra-pure ferritic stainless steel
A stainless steel and ultra-pure iron technology, applied in metal rolling, metal rolling, rolling mill control devices, etc., can solve the problems of strip wrinkling and stripes, and improve cold rolling reduction rate and grinding efficiency. , The effect of improving the production efficiency of the rolling mill
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Applications(China)
- Current Assignee / Owner
- Publication Date
- 2022-02-25
Smart Images
Figure 1 
Figure 2 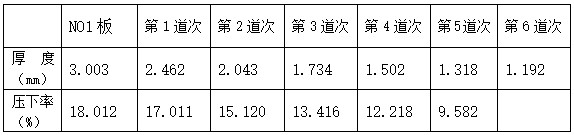
Figure 3
Abstract
Description
technical field
[0001] The invention belongs to the technical field of steel rolling, and relates to a 443 ultra-pure ferritic stainless steel and a cold rolling method thereof. Background technique
[0002] 443 stainless steel is a new generation of ferritic stainless steel developed in recent years. Because it does not contain nickel, its production cost is significantly lower than that of 300 series stainless steel. Corrosion resistance and processability. 443 ferritic stainless steel has excellent corrosion resistance similar to that of austenitic stainless steel, especially good resistance to chloride ion corrosion. It is considered as a substitute for 304 austenitic stainless steel and has been widely used in the fields of elevators, architectural decoration and kitchen utensils. widely used.
[0003] 443 is used as a decorative material. In the post-processing process of the product, oil grinding and wire drawing are required to form a good wire drawing surface. Ho...
Examples
Embodiment 1
[0031] (1) Hot metal pretreatment, using conventional ultra-pure ferritic stainless steel smelting methods to decarburize and desulfurize the hot metal to control the internal components of the slab. Specifically, the hot metal is decarburized through the AOD converter and the VOD vacuum smelting furnace in sequence. Two times of decarburization can effectively reduce the carbon content in the molten iron, and finally put the decarburized molten iron into the LF refining furnace for desulfurization to complete the pretreatment.
[0032] (2) Casting slabs, the pretreated molten iron is continuously cast to form ferritic stainless steel slabs (the size of the slabs is 220mm*1270mm*11000mm), and the slabs are placed in the heat preservation pit for heat preservation and slow cooling. The internal composition of the blank is: w (C) ≤ 0.025%, w (Si) ≤ 1.00%, w (Mn) ≤ 1.00%, w (S) ≤ 0.030%, w (P) ≤ 0.030%, 20.50% ≤ w (Cr)≤23.00%, 0.30%≤w (Cu)≤0.80%, w(N)≤0.025%, w(C+N)≤0.1%, w(Ti+Nb...
Embodiment 2
[0048] (1) Pretreatment of molten iron, the molten iron is decarburized through the AOD converter and VOD vacuum smelting furnace in turn, and then the decarburized molten iron is placed in the LF refining furnace for desulfurization to complete the pretreatment.
[0049] (2) Casting slab, the pretreated molten iron is continuously cast to form a ferritic stainless steel slab (the size of the slab is 220mm*1270mm*11000mm), and the slab is placed in the heat preservation pit for heat preservation and slow cooling, and the slab The internal composition of the blank is: w (C) ≤ 0.025%, w (Si) ≤ 1.00%, w (Mn) ≤ 1.00%, w (S) ≤ 0.030%, w (P) ≤ 0.030%, 20.50% ≤ w (Cr)≤23.00%, 0.30%≤w (Cu)≤0.80%, w(N)≤0.025%, w(C+N)≤0.1%, w(Ti+Nb)≤0.8%, the balance is iron and unavoidable impurities. (2) Slab grinding, thermal grinding of the slab surface.
[0050] (3) Heating the slab, and then heating the ground slab to 1150°C to 1200°C and keeping it warm for 20-60min to facilitate subsequent rolli...