
Method for smelting high-nitrogen steel by compression electroslag furnace
A pressurized electroslag and high-nitrogen steel technology, which is applied in the field of smelting high-nitrogen steel, can solve problems such as uneven distribution of nitrogen, and achieve the effects of simple process, avoiding secondary remelting, and uniform composition
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Applications(China)
- Current Assignee / Owner
- Publication Date
- 2008-09-10
- Estimated Expiration
- Not applicable · inactive patent
Smart Images
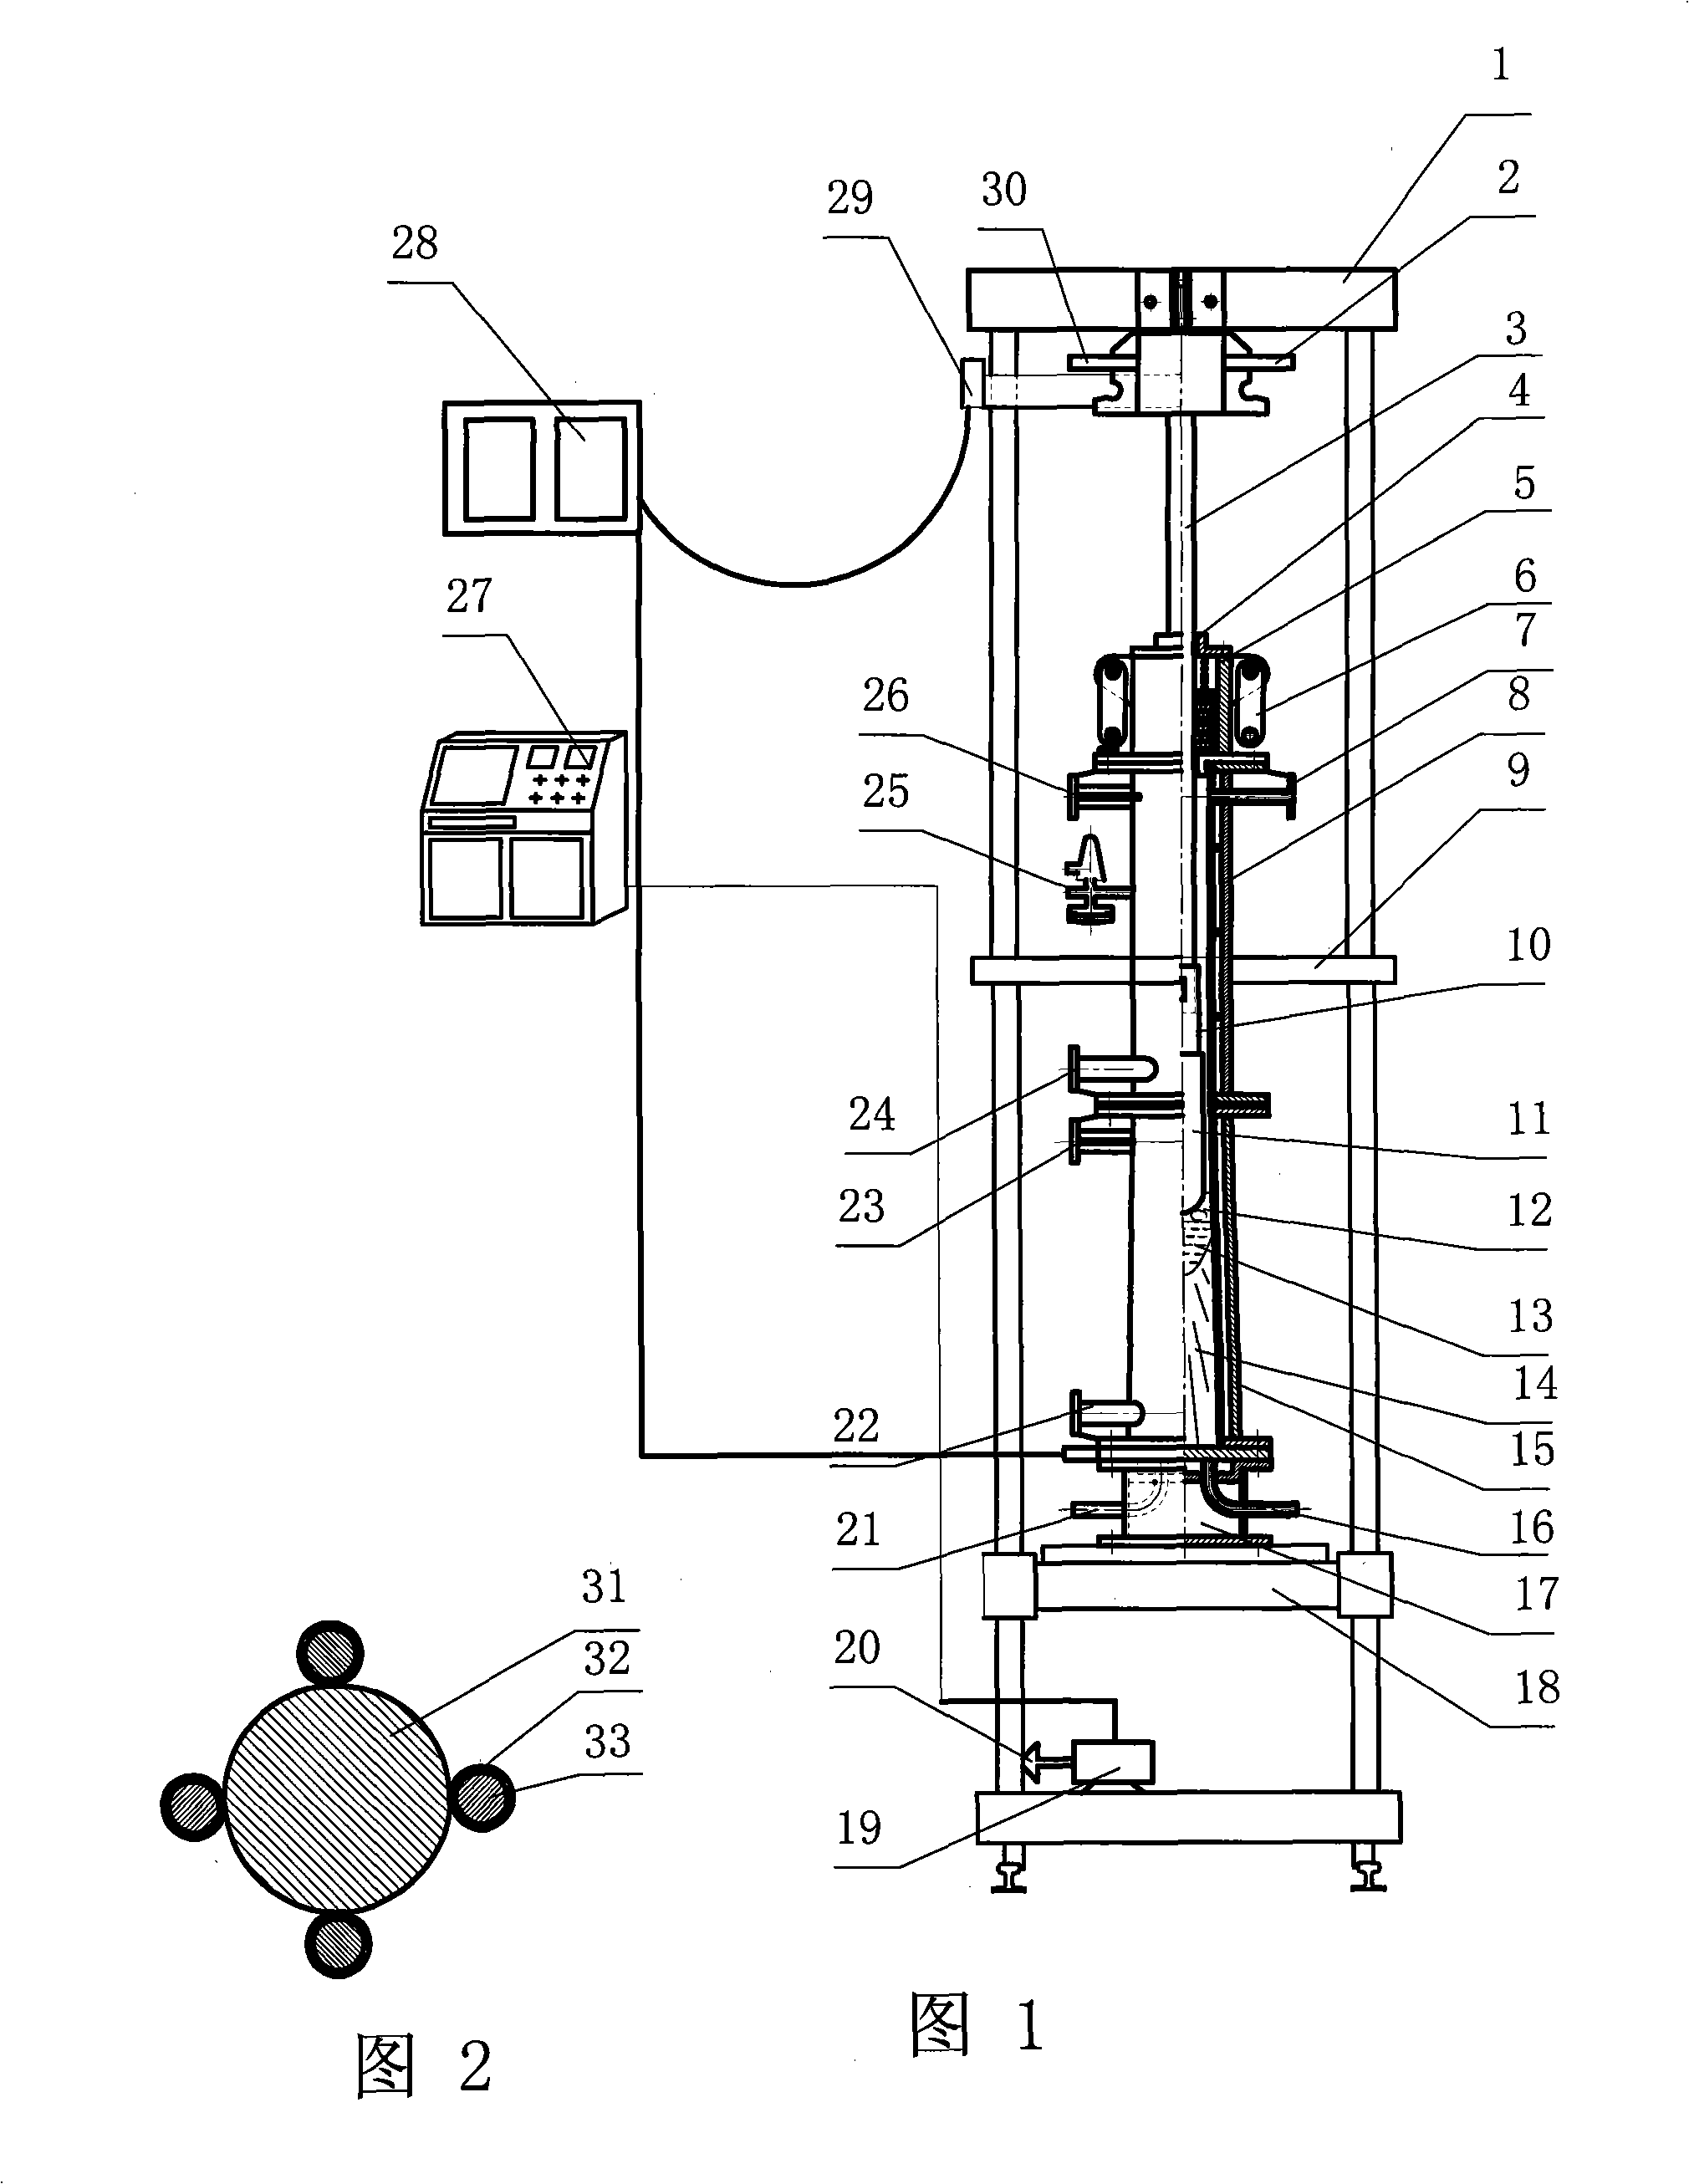
Figure 1 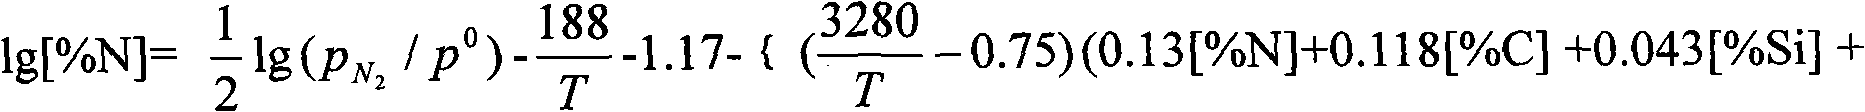
Figure 2 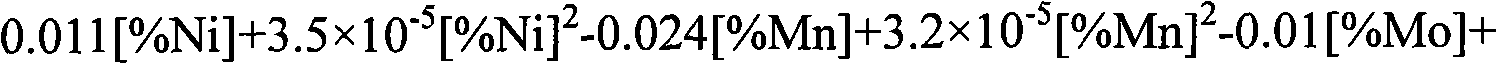
Figure 3
Abstract
Description
technical field
[0001] The invention relates to a method for smelting high-nitrogen steel, in particular to a method for smelting high-nitrogen steel using a pressurized electroslag furnace. Background technique
[0002] As an interstitial element in steel, nitrogen can improve various properties of steel, including strength, toughness, creep resistance, wear resistance, etc. performance, corrosion resistance, etc. In a broad sense, the so-called "high nitrogen steel" refers to the steel whose actual nitrogen content in the material exceeds the limit value that can be achieved by preparing the material under normal pressure (0.1MPa). It is generally believed that according to the content of nitrogen in austenitic stainless steel, nitrogen-containing austenitic stainless steel can be divided into nitrogen-controlling type (nitrogen content 0.05% ~ 0.10%), medium nitrogen type (nitrogen content 0.10% ~ 0.40%) and high nitrogen type. Nitrogen type (nitrogen content above 0.40...
Examples
Embodiment 1
[0030] Embodiment 1: as shown in Figure 1, the present invention comprises sealing device 5, is provided with the electrode 3 that is connected with its sliding sealing in sealing device 5, is equipped with smelting chamber 8 below sealing device 5, is housed below smelting chamber 8 Crystallizer 15, bottom water tank 17 is housed below crystallizer 15, is contained on the trolley lifting platform 18 below bottom water tank 17. The upper end of the electrode 3 is welded on the cross-arm beam 1, and a conductive connector 29 is welded on the electrode 3. The conductive connector 29 is connected to one end of the water-cooled cable, and the other end of the water-cooled cable is connected to the AC power supply 28. The electrode cooling water inlet 2 and the electrode cooling water outlet 30 are welded on the side, and the lower end of the electrode 3 is a dummy electrode 10 , and the consumable composite electrode 11 is welded at the lower end of the dummy electrode 10 . A safe...
Embodiment 2
[0060] Example 2: Target steel for smelting 0Cr17.5Mn14.5Mo3.2N1
[0061] 1. Through the calculation formula
[0062] lg [ % N ] = 1 2 lg ( p N 2 / p 0 ) - 188 T - 1.17 - { ( 3280 T - 0.75 ) ( 0.13 [ % N ] + 0.118 [ % C ] + 0.043 [ % Si ] +
[0063] 0.011 [ % Ni ] + ...
Embodiment 3
[0071] Example 3: Target steel for smelting 0Cr23Mo2Ni1N1
[0072] 1. Through the calculation formula
[0073] lg [ % N ] = 1 2 lg ( p N 2 / p 0 ) - 188 T - 1.17 - { ( 3280 T - 0.75 ) ( 0.13 [ % N ] + 0.118 [ % C ] + 0.043 [ % Si ] +
[0074] 0.011 [ % Ni ] + 3...