
Production method for polypropylene spun-bonded needle-punched geotextile
A technology of polypropylene spunbonding and production methods, which is applied in the direction of non-woven fabrics, textiles, and papermaking, and can solve the problem of cloth surface tensile strength and elongation at break (the influence of elongation, the long production process of staple fiber polypropylene geotextiles, and the restriction of polypropylene geotextiles) Geotextile performance indicators and other issues, to achieve the effect of shortening the production process, stabilizing various indicators, and stabilizing heat shrinkage
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Patents(China)
- Current Assignee / Owner
- Publication Date
- 2015-06-03
Smart Images
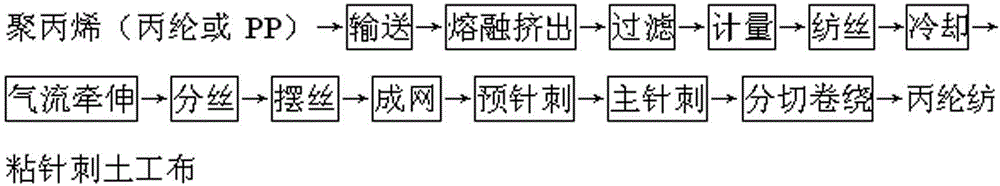
Figure 1
Abstract
Description
technical field
[0001] The invention relates to a method for preparing a synthetic fiber nonwoven product. Background technique
[0002] Those skilled in the art know that geotextiles have functions such as filtration, drainage, isolation, reinforcement, and enhancement. For this reason, geotextiles have become the fourth largest building material after my country's steel bars, cement, and wood. At present, the production process of polypropylene geotextiles in my country is mainly to use polypropylene staple fibers to form geotextiles by carding, cross-lapping, and needle-punching consolidation. Polypropylene staple fiber is melt-spun from polypropylene chips through a screw extruder, cooled, clustered, wound, and doffed to form primary fiber bundles, and then multiple primary fiber bundles are bundled again, stretched, crimped, and shaped and dried , cutting, packaging and other processes to make finished staple fibers. This process is made by a two-step process, ...
Examples
Embodiment 1
[0020] The polypropylene raw material is transported into the screw extruder for melt extrusion. The screw extruder has a large length-to-diameter ratio, that is, a polypropylene screw extruder with a length-to-diameter ratio of 29:1. The temperature of each zone: 165°C, 200°C, 230°C, 250°C ℃, 250℃, 260℃, 265℃, 265℃. After the melt passes through the filter, the pressure is 11Mpa, and then enters the spinning box, and is sprayed out from the spinneret after metering. The component pressure is 15Mpa, the spinning temperature is 265°C, the single-filament fineness is controlled at 6dpf, and the single-filament strength is greater than 4.2CN / dtex. The spun filaments are cooled by side blowing, the wind speed of the side blowing: 0.7m / s, the temperature of the side blowing: 17°C, and the humidity of the side blowing: above 70%. The cooled filaments are air-drawn by a tubular air-flow drawing device, and the air-flow drawing speed is 5000m / min. The drawing pressure is 0.60 Mpa. ...
Embodiment 2
[0022] The PP raw material is conveyed into the screw extruder for melt extrusion. The screw extruder has a large aspect ratio, that is, a polypropylene screw extruder with an aspect ratio of 30:1. The temperature of each zone: 165°C, 200°C, 240°C, 255°C ℃, 255℃, 260℃, 270℃, 270℃. After the melt passes through the filter, the pressure is 12Mpa, and then enters the spinning box, and is sprayed out from the spinneret after metering. The component pressure: 16Mpa, the spinning temperature: 270°C, the monofilament fineness is controlled at 8dpf, and the monofilament strength is greater than 4.2CN / dtex. The spun filaments are cooled by the side blowing, the wind speed of the side blowing: 0.9m / s, the temperature of the side blowing: 16°C, and the humidity of the side blowing: above 70%. The cooled filaments are air-drawn by a tubular air-flow drawing device, and the air-flow drawing speed is 4600m / min. The drawing pressure is 0.65 Mpa. After spinning, the frequency of the spinn...