
Backlash compensation method for laser welding and device implementing same
A technology of gap compensation and laser tailor welding, applied in the direction of planer, metal processing equipment, manufacturing tools, etc., to achieve the effect of small vibration, less processing waste and simple structure
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Patents(China)
- Current Assignee / Owner
- Publication Date
- 2012-11-07
- Estimated Expiration
- Not applicable · inactive patent
Smart Images
Figure 1 
Figure 2 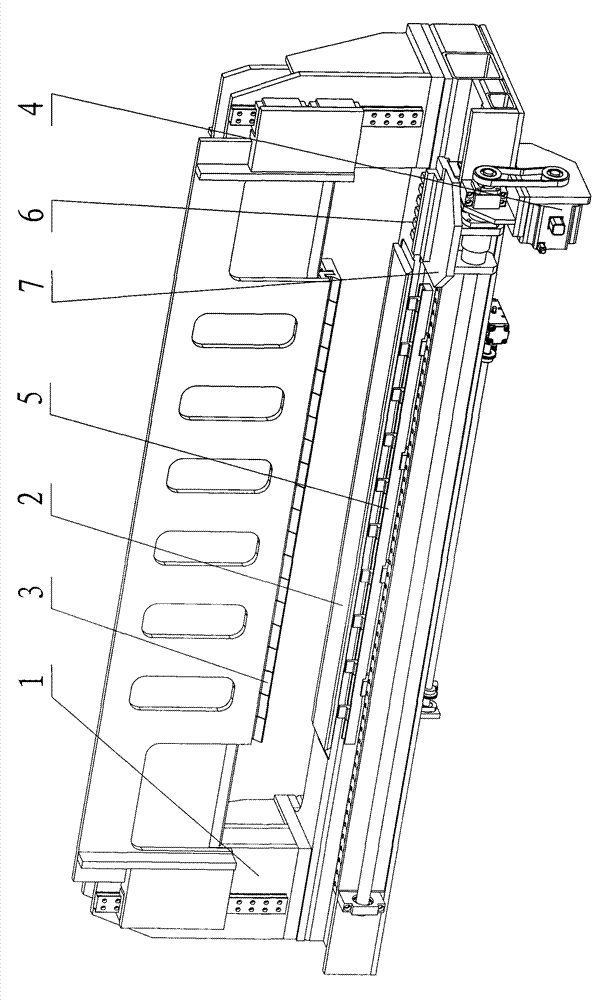
Figure 3
Abstract
Description
technical field
[0001] The invention belongs to the field of laser welding, in particular to a gap compensation method for laser tailor welding and a device for implementing the method. Background technique
[0002] Tailored laser welding uses laser as welding energy to butt weld a number of plates with different materials, different thicknesses and different coatings. Since the diameter of the focused spot of the laser beam in laser welding is generally less than 1mm, the straightness of the plate welding edge and the cross-sectional shape of the butt end face have a direct impact on the welding quality. The straightness of the welding edge and the cross-sectional shape of the butt end face not only affect the tailor welding The size of the gap between the plates will also affect the accuracy of weld tracking.
[0003] In order to ensure the welding quality, it is usually necessary to further process the welding edge of the welding base metal before welding to improve the ...
Examples
Embodiment Construction
[0052] The present invention will be described in further detail below in conjunction with the accompanying drawings.
[0053] The gap compensation method for laser tailor welding of the present invention: planing the edge to be welded of the base metal to be welded, planing a butt end face with high straightness and high flatness, reducing the gap between the plates when the base metal is butted, and improving Seam tracking accuracy. Include the following steps:
[0054] A. Position and fix the welding base metal to prevent disturbances such as jumping and vibration during the planing process of the welding base metal, so as to ensure the processing quality;
[0055] B. Determine the amount of planing by adjusting the positioning reference of the welding base metal or the position of the tool;
[0056] C. Determine the planing angle by adjusting the attitude of the tool relative to the edge to be welded of the welding base metal;
[0057] D. Use a cutter to plan the edge t...