
Control method and device for arc energy and computer readable medium
An arc energy and control method technology, applied in arc welding equipment, manufacturing tools, welding equipment, etc., can solve the problems of uncontrollable welding power output, poor heat input control effect, etc., and achieve good quality and small heat input. Effect
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Applications(China)
- Current Assignee / Owner
- Publication Date
- 2018-01-12
Smart Images
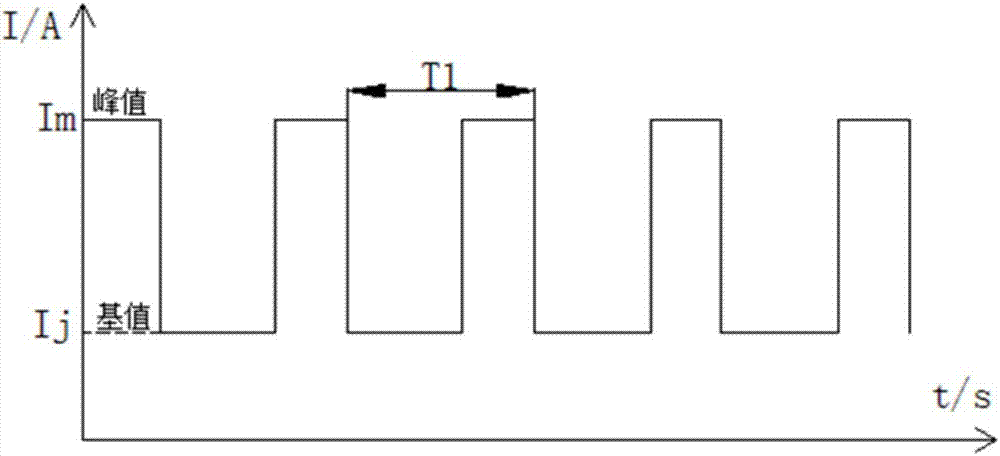
Figure 1 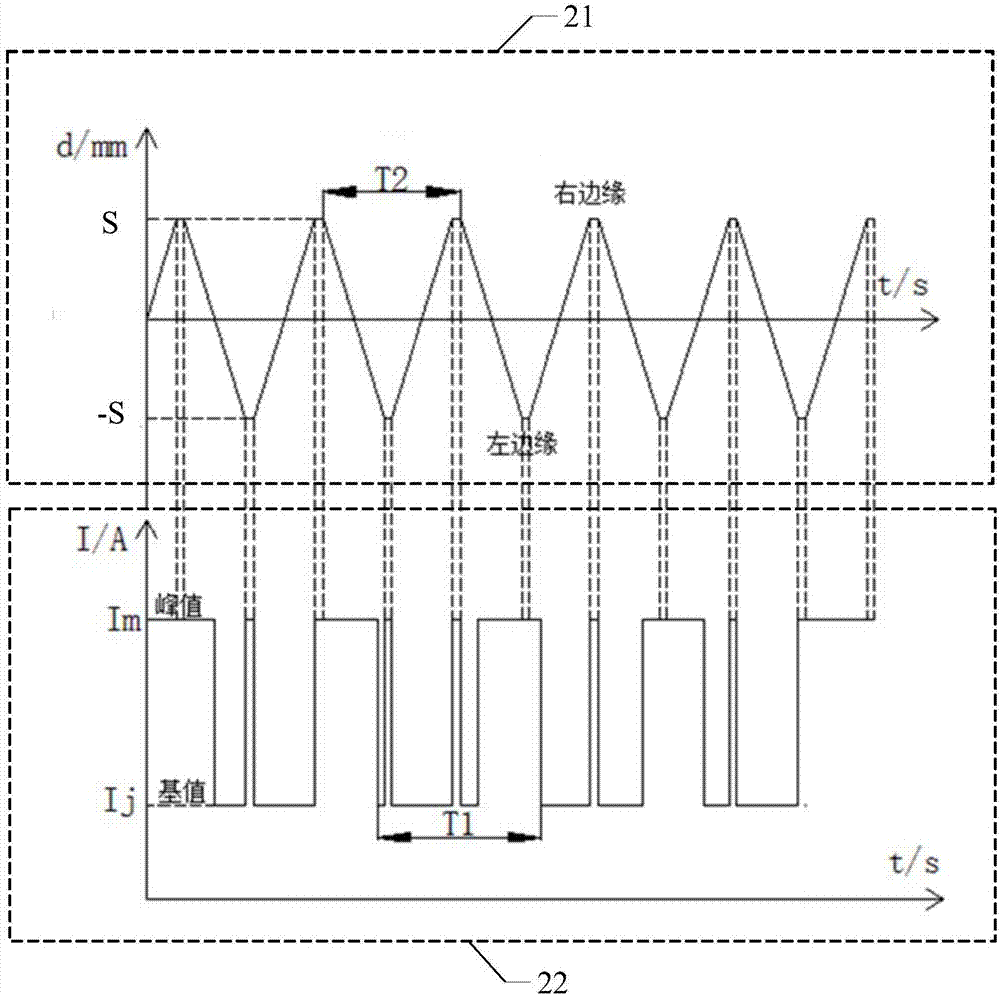
Figure 2 
Figure 3
Abstract
Description
technical field
[0001] Embodiments of the present invention relate to the field of welding, and in particular, to a control method and control device for arc energy, and a computer readable medium. Background technique
[0002] Among various welding methods, arc welding is the most widely used welding method, and arc is the most obvious distinguishing feature of arc welding compared with other welding methods. The arc is an energy carrier, which can convert the electric energy output by the welding power source into light and heat energy and transfer it to the base material of the workpiece. It consists of three parts: the cathode area, the anode area and the arc column area. For different arc welding methods, the area where the arc heat is concentrated is also different. For example, the heat of plasma arc welding is concentrated in the arc column area, and the heat of tungsten argon arc welding is concentrated in the anode area. In the actual welding process, it is necess...
Examples
Embodiment Construction
[0037] figure 1 A schematic diagram of the output waveform of an existing pulse welding power supply is given. In the existing pulse welding, the welding power supply periodically outputs pulse current I (unit is ampere A) with time t (unit is second s), the period of pulse current is T1, the peak value of pulse current is Im, and the pulse current The base value of is Ij.
[0038] For oscillating arc welding, the existing control method based on the arc position is applied to control the output current of the pulse welding during the welding process. When the arc reaches the edge of the weld, the output of the welding power supply is forced to the base value of the pulse current or pulse peak current. The schematic diagram of the power output waveform of pulse welding based on arc position control is as follows: figure 2 shown.
[0039] see figure 2 , the upper figure 21 is a schematic diagram of the periodic swing of the arc position with time t (unit is second s), wh...