
A kind of ultrafine ball mill liner and its preparation method
A fine ball and liner technology, applied in grain processing and other directions, can solve the problems of difficult to meet the use requirements of ultra-fine ball mills, low wear resistance, etc., and achieve the effect of improving service life, improving wear resistance, and avoiding wear failure.
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Patents(China)
- Current Assignee / Owner
- Publication Date
- 2020-10-16
Smart Images
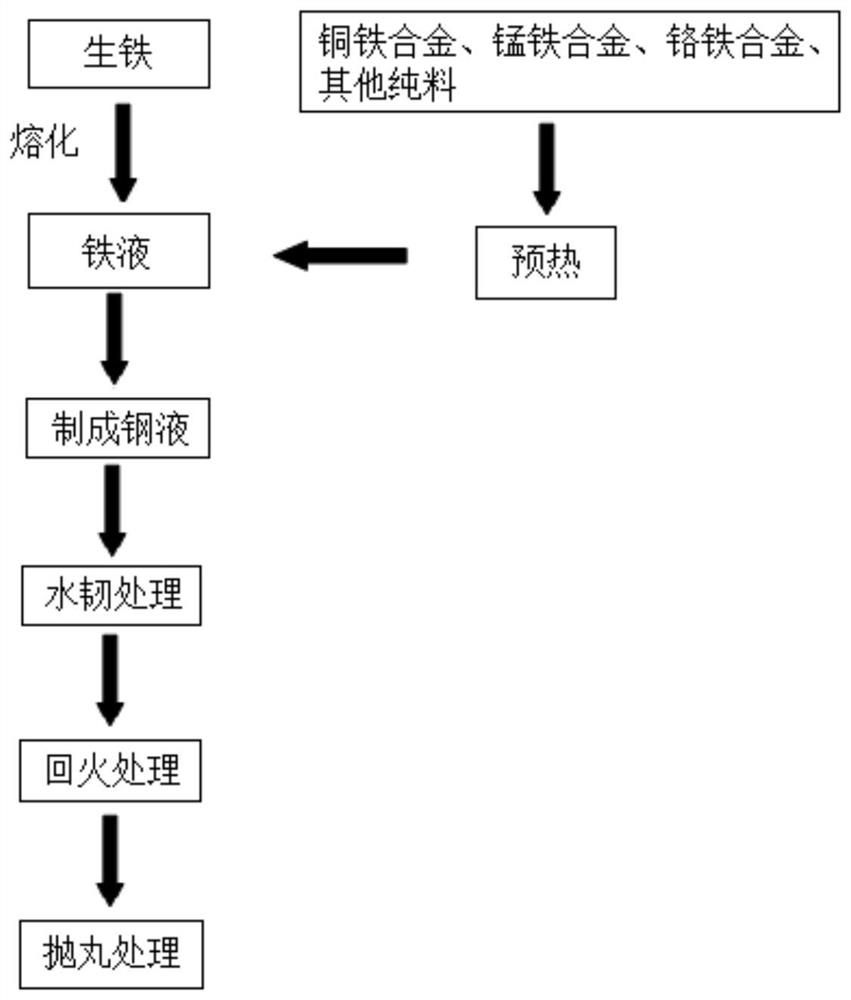
Figure 1
Abstract
Description
technical field
[0001] The invention relates to a ball mill liner, in particular to an ultrafine ball mill liner and a preparation method thereof, belonging to the field of ball mills. Background technique
[0002] Ball mills are widely used in ore, building materials, metallurgy, electric power and many other industries. As a part of the ball mill, the ball mill liner mainly protects the ball mill cylinder and prevents the steel balls and materials in the cylinder from impacting and causing failure and damage. At present, the types of metal lining plates of traditional ball mills include high manganese steel, medium and high carbon alloy steel, and chromium cast iron. High manganese steel plates are widely used. Protrusions reduce the service life of the liner.
[0003] Compared with traditional ball mills, ultra-fine ball mills have relatively low requirements on the impact resistance of the lining board, but have extremely high requirements on the wear resistance of the ...
Examples
Embodiment 1
[0021] In terms of weight percentage, the composition of the ultrafine ball mill liner is: C 1.2%, Si 0.5%, Cu 0.9%, Mn 8%, Cr 1.2%, Ta 0.5%, Bi 0.5%, Sn 1%, rare earth 0.5%, S=0.02%, P=0.02%; the balance is Fe.
[0022] (1) Preheat manganese-ferroalloy, copper-iron alloy, chromium-ferroalloy and other pure materials at 200°C for 2 hours. After the pig iron is completely melted in the smelting furnace, the temperature is 1520°C. Add mixed pure materials and wait for complete melting to obtain molten steel. The tapping temperature is above 1500°C, the pouring temperature is 1450°C, and the mold is poured.
[0023] (2) Water toughening treatment for cold castings: Put the cold castings in a heat treatment furnace, raise the temperature from room temperature to 620°C at a rate of 50°C / h, keep it warm for 2 hours, and then raise the temperature to 1080°C at a rate of 150°C / h. ℃, heat preservation for 2 hours, after the heat preservation is completed, quickly quench the casting i...
Embodiment 2
[0028] In terms of weight percentage, the composition of the ultrafine ball mill liner is: C 1.2%, Si 0.5%, Cu 0.9%, Mn 8%, Cr 1.2%, Ta 0.7%, Bi 1%, Sn 1.5%, rare earth 0.5%, S=0.02%, P=0.02%; the balance is Fe.
[0029] (1) Preheat manganese-ferroalloy, copper-iron alloy, chromium-ferroalloy and other pure materials at 180°C for 2 hours. After the pig iron is completely melted in the smelting furnace, the temperature is 1500°C. Add mixed pure materials and wait for complete melting to obtain molten steel. The tapping temperature is above 1500°C, the pouring temperature is 1480°C, and the mold is poured.
[0030] (2) Water toughening treatment for cold castings: Put the cold castings in a heat treatment furnace, raise the temperature from room temperature to 650°C at a rate of 50°C / h, keep it warm for 2 hours, and then raise the temperature to 1050°C at a rate of 150°C / h. ℃, heat preservation for 4 hours, after the heat preservation is completed, quickly quench the casting w...
Embodiment 3
[0035] In terms of weight percentage, the composition of the ultrafine ball mill liner is: C 1.2%, Si 0.5%, Cu 0.9%, Mn 8%, Cr 1.2%, Ta 0.5%, Bi 1.2%, Sn 1.5%, rare earth 0.5%, S=0.02%, P=0.02%; the balance is Fe.
[0036] (1) Preheat manganese-ferroalloy, copper-iron alloy, chromium-ferroalloy and other pure materials at 230°C for 1.5h. After the pig iron is completely melted in the smelting furnace, the temperature is 1520°C. Add mixed pure materials and wait for complete melting. Get molten steel. The tapping temperature is above 1500°C, the pouring temperature is 1470°C, and the mold is poured.
[0037] (2) Water toughening treatment for cold castings: Put the cold castings in a heat treatment furnace, raise the temperature from room temperature to 600°C at a rate of 60°C / h, keep it warm for 1h, and then raise the temperature to 1000°C at a rate of 180°C / h. ℃, heat preservation for 4 hours, after the heat preservation is completed, quickly quench the casting in water, th...