
Die forging press stroke improved compensation method
A technology of die forging press and compensation method, which is applied in the direction of the driving device of the forging press, can solve the problems of deviation between the actual displacement of the press and the expected displacement, the axial deformation of the column of the press, and the lack of precision of the die forging, so as to prevent the accuracy from being affected. loss, reduction of repair times, and precise compensation
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Applications(China)
- Current Assignee / Owner
- Publication Date
- 2021-01-29
Smart Images
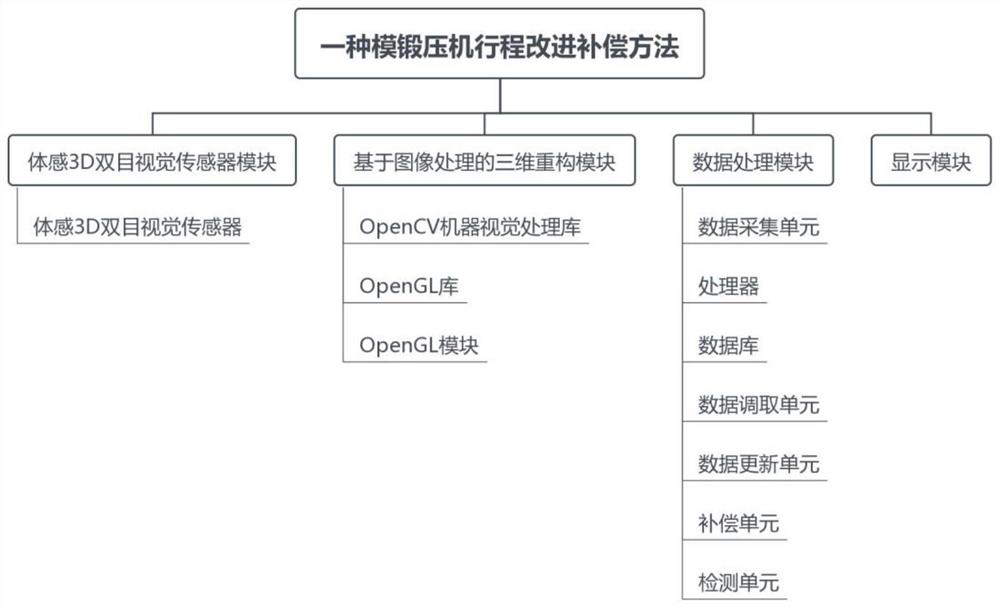
Figure 1 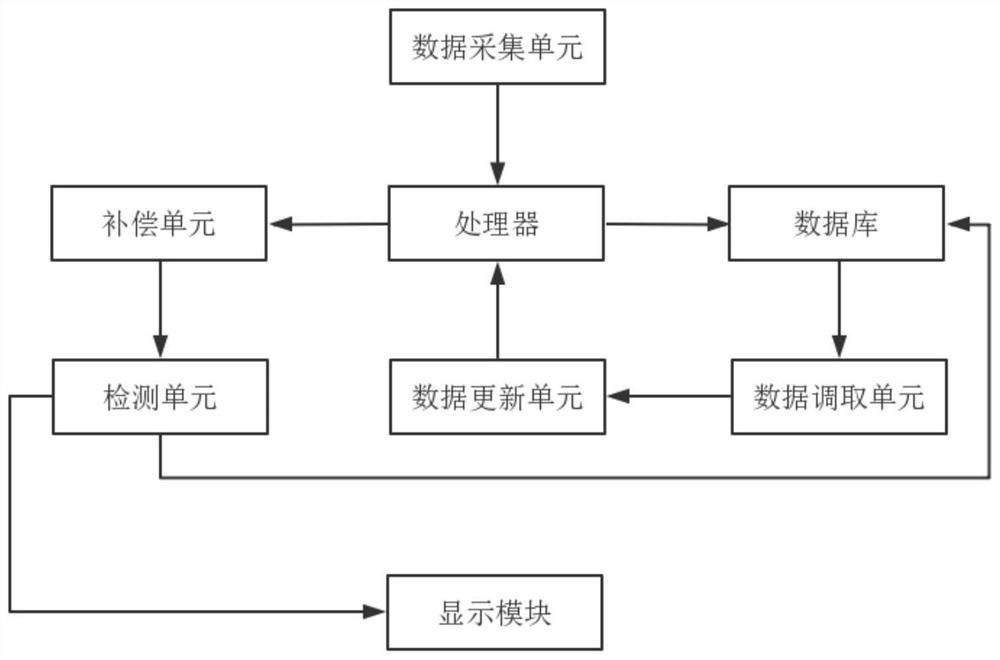
Figure 2 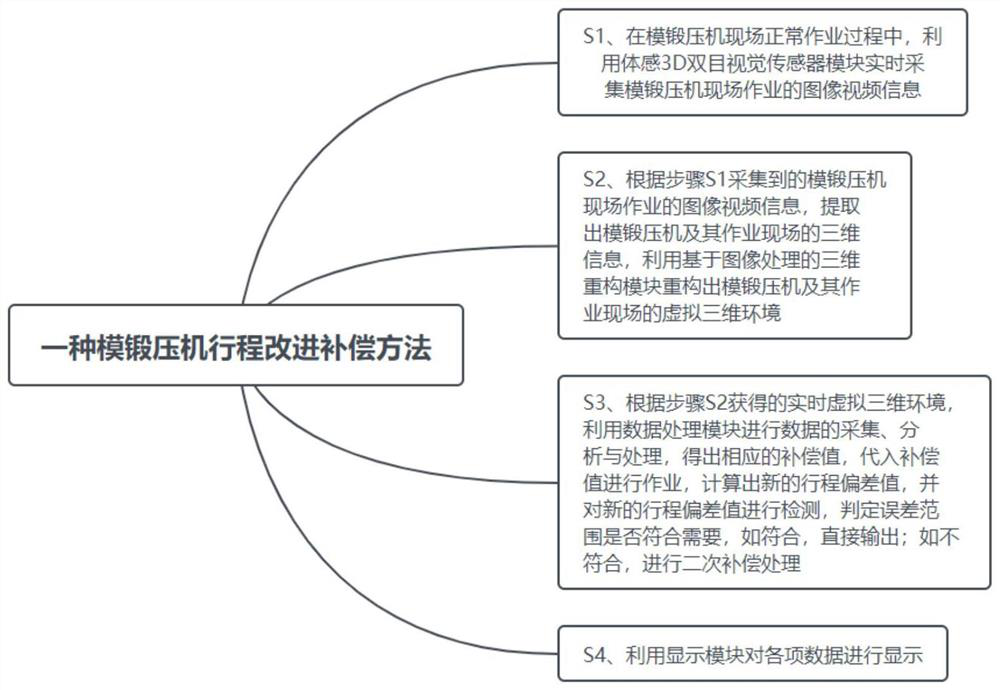
Figure 3
Abstract
Description
technical field
[0001] The invention relates to the technical field of die forging, in particular to a method for improving and compensating the stroke of a die forging press. Background technique
[0002] In large-scale mechanical equipment and important equipment, such as steel rolling, power stations (hydropower, thermal power, nuclear power), petroleum, chemical industry, shipbuilding, aviation, aerospace, heavy weapons, etc., large free forgings and large die forgings are used. These large forgings are It is forged with a large free forging hydraulic press and a large die forging hydraulic press. Therefore, the production of large forgings has a very important position in advanced industrial countries, and even from the variety, quantity and grade of large free forging hydraulic presses and large die forging hydraulic presses owned by a country, its industrial level and national defense strength can be measured.
[0003] For large-scale precision die forgings, such as ...
Examples
Embodiment 1
[0104] Use the somatosensory 3D binocular vision sensor and the 3D reconstruction module based on image processing to reconstruct the virtual 3D environment. With the worktable as the center, the x-axis is established in the left and right parallel direction of the worktable, the y-axis is established in the front and back direction of the worktable, and the up-down direction of the worktable Establish the z-axis, take mm as the unit, use the data acquisition unit to collect the position data of the movable beam H={0.1,0.2,0.5} under different clamping pressures,
[0105] Define the degree of extrusion of the workbench backing plate into grades 0-3, including:
[0106] Level 0: no extrusion at all;
[0107] Level 1: Extrusion is not greater than 0.1mm;
[0108] Level 2: Extrusion is not greater than 0.5mm;
[0109] Level 3: extrusion greater than 0.5mm;
[0110] Defining the degree of deformation of the press pillar is divided into 0-3 grades, including:
[0111] Level 0: ...