
High-speed steel roll and preparation method thereof by centrifugal compounding in electromagnetic field
A technology of centrifugal compounding and centrifugal compound casting, which is applied in the direction of rolls, metal rolling, metal rolling, etc., can solve the problems of coarse composite carbides, rare and expensive Nb elements, and increase the cost of rolls, so as to achieve less loose defects and improve strengthening Effect, the effect of improving the finished product rate and qualified rate
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Patents(China)
- Current Assignee / Owner
- Publication Date
- 2012-12-19
- Estimated Expiration
- Not applicable · inactive patent
Smart Images
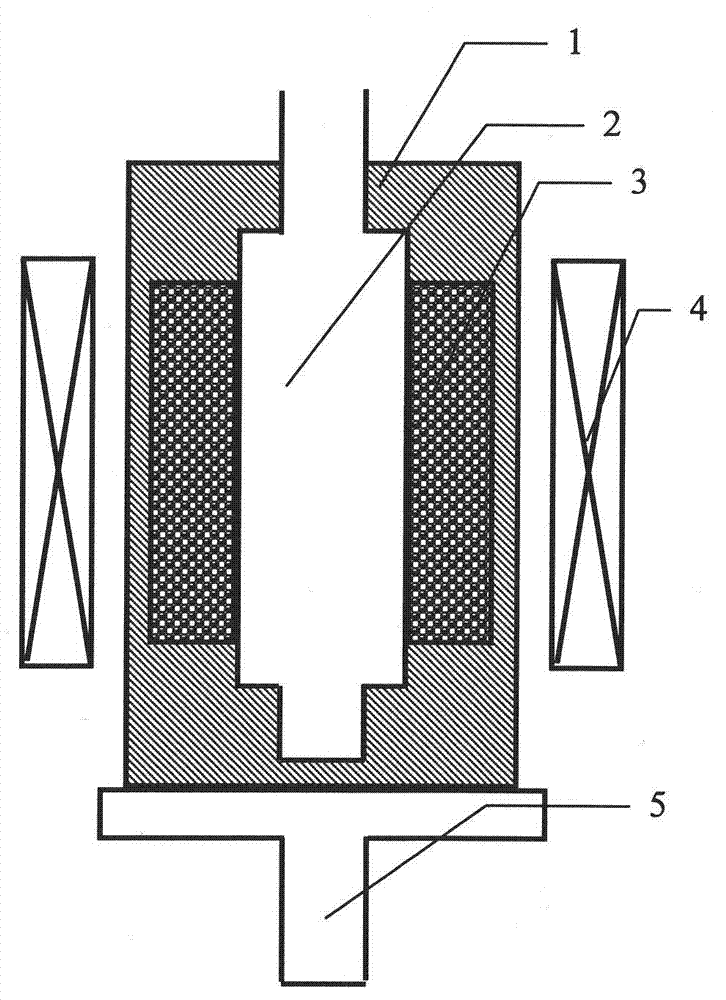
Figure 1 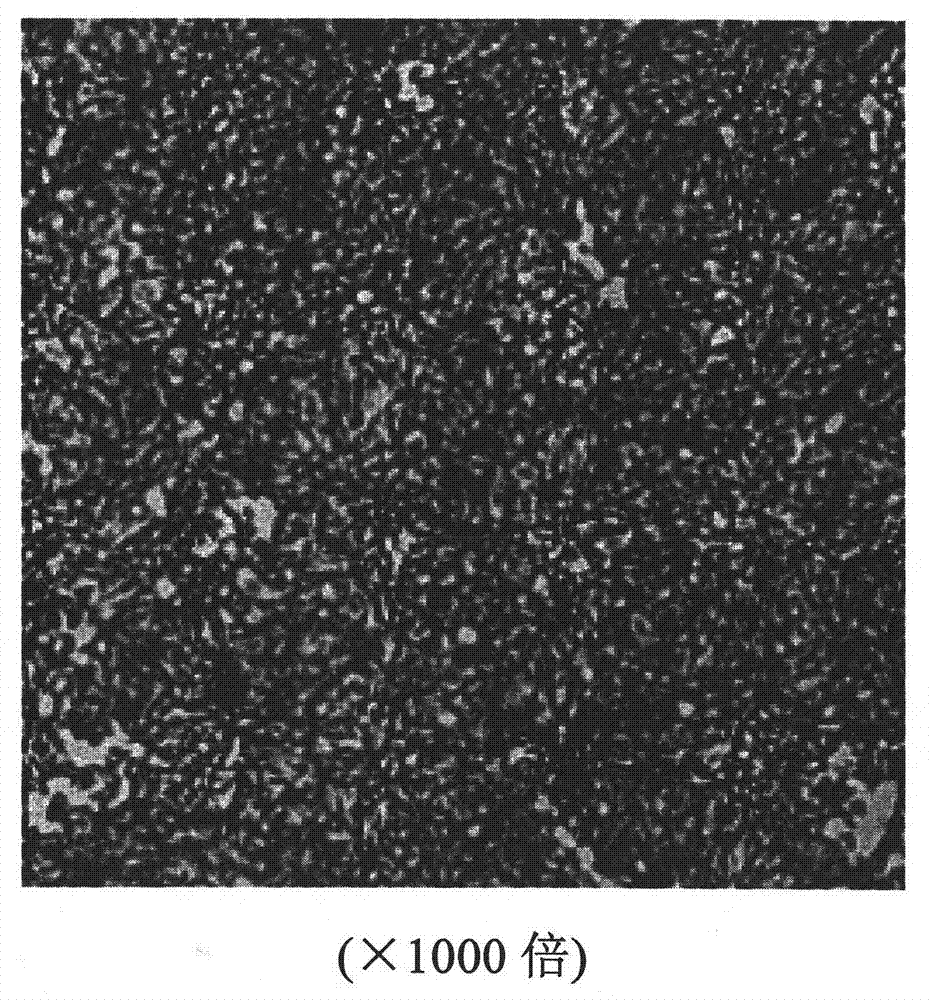
Figure 2 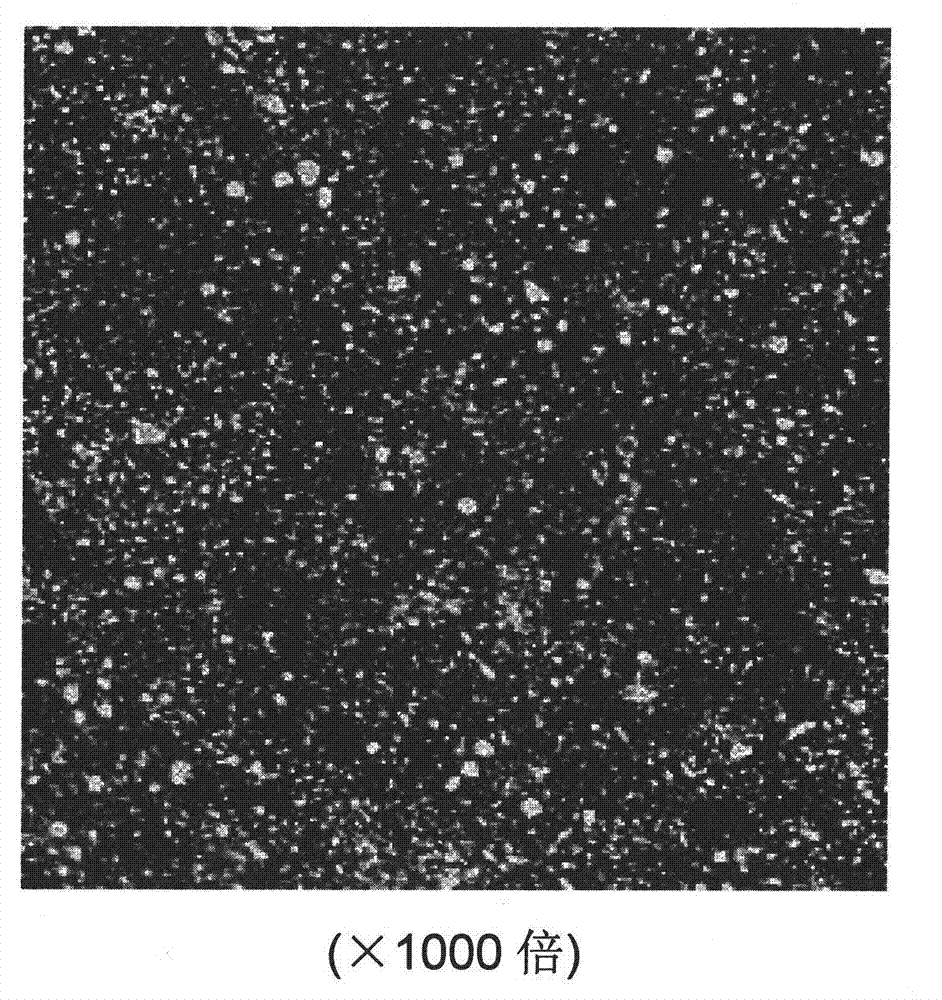
Figure 3
Abstract
Description
technical field
[0001] The invention belongs to the technical field of preparation of high-speed steel rolls, and in particular relates to a high-performance high-speed steel roll and a centrifugal composite preparation method thereof under an electromagnetic field. Background technique
[0002] Roll is a key wear-resistant part consumed in large quantities in steel rolling production, and its quality directly affects the quality of rolled steel products, labor productivity and production costs. Due to the extremely harsh service conditions of the roll, it is required that the roll must withstand quite strong force and heat. In addition to having high strength and toughness to prevent the roll from breaking during use, the surface of the roll should also have good wear resistance and heat resistance. , a single roll material is difficult to meet the requirements of hot rolls. Composite rolls composed of roll core materials with good strength and toughness and roll body mate...
Examples
Embodiment 1
[0049] The body size of the high-performance high-speed steel composite roll in this example is φ500×1700mm. The material of the wear-resistant working layer of the composite roll and the ductile cast iron of the roll core are respectively melted in a 4t intermediate frequency induction furnace and a 5t / h cupola furnace. The manufacturing process steps are as follows :
[0050] The first stage: smelting of high-speed steel and smelting of roll core ductile iron
[0051] Note: The smelting of high-speed steel and the smelting of ductile iron of the roller core are carried out at the same time
[0052] The melting process of high-speed steel is:
[0053] 1. by composition requirement of the present invention, scrap steel 1390kg, pig iron (4.2%C) 1700kg, ferrochrome (50%Cr) 200kg, molybdenum iron (60%Mo) 100kg), tungsten iron (70%W) 260kg are mixed, in Compact the block on the press, put it into the smelting furnace and heat it to melt. After the molten steel is melted, when th...
Embodiment 2
[0073] The size of the high-performance high-speed steel composite roll in this embodiment is φ600×1400mm. The wear-resistant working layer material of the composite roll and the nodular cast iron of the roll core are smelted in a 4t intermediate frequency induction furnace and a 5t / h cupola respectively. The manufacturing process steps are as follows :
[0074] The first stage: smelting of high-speed steel and smelting of roll core ductile iron
[0075] Note: The smelting of high-speed steel and the smelting of ductile iron of the roller core are carried out at the same time
[0076] The melting process of high-speed steel is:
[0077] 1. by composition requirement of the present invention, scrap steel 1000kg, pig iron (4.2%C) 1600kg, ferrochrome (50%Cr) 290kg, molybdenum iron (60%Mo) 290kg), tungsten iron (70%W) 340kg are mixed, in Compact the block on the press, first put 30kg of recarburizer (95%C) into the furnace, then put the pressed block into the smelting furnace to...