
Flow control method for rolling temperature of hot rolled steel strip
A coiling temperature and flow control technology, applied in temperature control, mass flow control devices, metal rolling, etc., can solve problems such as unstable coiling temperature index control, to ensure coiling temperature and uniformity, and improve product quality. Performance, satisfying the effect of large flow and fast cooling
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Applications(China)
- Current Assignee / Owner
- Publication Date
- 2016-02-17
Smart Images
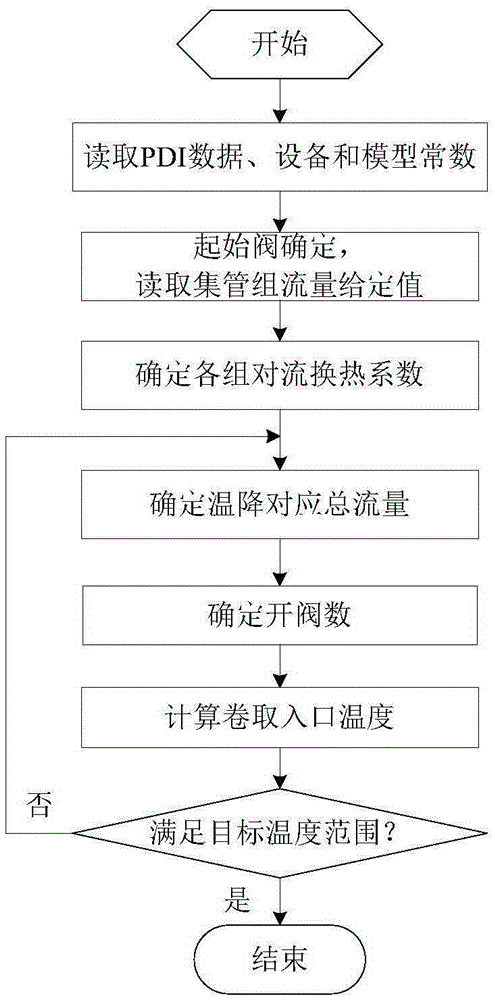
Figure 1 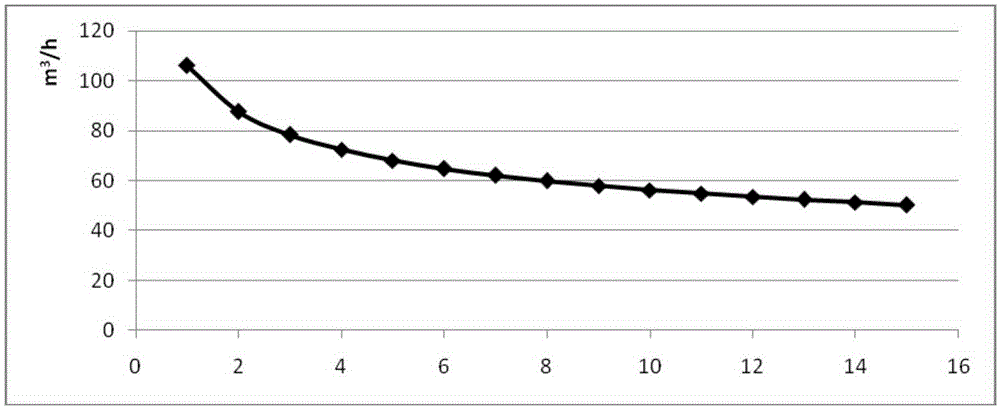
Figure 2 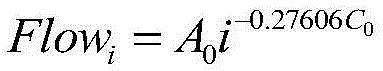
Figure 3
Abstract
Description
Technical field
[0001] The invention relates to a flow control method for the coiling temperature of hot-rolled strip steel, and belongs to the technical field of automatic control of steel rolling. Background technique
[0002] Coiling temperature is an important process parameter that affects the microstructure and properties of strip steel, and it is also an important index in hot rolling production control. In the production of hot-rolled strip steel, the control of the coiling temperature mainly relies on the configuration of the laminar cooling header group for timely opening and closing adjustments. In order to obtain qualified performance products, the number and flow of the header configuration need to be increased. Precision control. Generally, the main valves of each group in the laminar flow cooling equipment area are pneumatic on-off valves, and the valve opening and flow control are manually adjusted during commissioning or maintenance, and the flow adjustment of e...
Examples
Embodiment
[0041] The present invention takes a medium and wide band 950 hot rolling production line as an example, and combines figure 2 Explain as follows:
[0042] Step 1. Read the slab PDI data, the slab number is YG151004366, the steel grade is 08AL, the slab specification is 165*770*10000mm, the product target thickness is 3.0mm, the final rolling target temperature is 865℃, and the coiling target temperature is 550 ℃, read the equipment constant and the relevant parameters of the coiling temperature model. The measured value of the pyrometer at the entrance of the slab before the finishing mill is 988℃, and the measured value of the pyrometer at the exit of the finishing mill is 851℃; there are 15 sets of headers in the layer cold zone, The first 13 groups have 4 cooling units in each group, and the last two groups have 8 cooling units in each group, and each group of headers is equipped with a flow meter. The flow meter can better verify the flow control method of the present invent...