
Ultrahigh-strength steel wire for electric arc additive manufacturing and preparation method
An additive manufacturing and ultra-high-strength steel technology, applied in the direction of additive manufacturing, additive processing, etc., can solve the constraints on the application and promotion of ultra-high-strength steel arc additive manufacturing technology, the lack of ultra-high-strength steel wire, and the low rate of additive manufacturing. problems, to achieve the effect of low wire drawing cost, high arc additive manufacturing efficiency, and fast forming efficiency
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Applications(China)
- Current Assignee / Owner
- Publication Date
- 2021-02-05
Smart Images
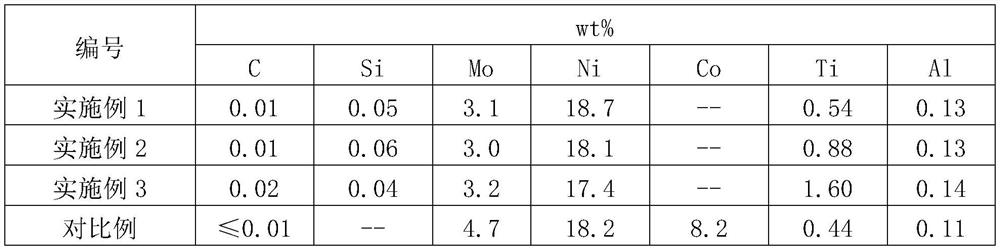
Figure 1
Abstract
Description
Technical field
[0001] The invention relates to the field of materials for arc additive manufacturing, in particular to an ultra-high-strength steel wire material for arc additive manufacturing and a preparation method.Background technique
[0002] Ultra-high-strength steel is widely used in aerospace, rail transit, ships, weapons and molds with its excellent strength and toughness. With the development of large-scale mechanical equipment and integration of work and structure, the structure of ultra-high-strength steel components has gradually become more complicated and diversified. However, traditional processing techniques such as casting, forging and welding are often difficult to meet the needs of complex and diversified manufacturing of large ultra-high-strength steel components. In recent years, the development of arc additive manufacturing technology has provided a new method for the manufacture of large and complex ultra-high-strength steel components. The ultra-high-strength ste...
Examples
Embodiment 1
[0035]1) Smelting and casting: Use a vacuum smelting furnace to first smelt ultra-high-strength steel wire alloy ingots, with a vacuum of 12 Pa, and cast to obtain an initial melting ingot; heat the initial melting ingot at 1150°C for 5 hours, and forge it into a Φ75mm For the electrode sample, the final forging temperature is not lower than 950℃, and the alloy is smelted twice by electroslag remelting, the electroslag speed is 1.6kg / min, the voltage is 30V, the current is 1.8kA, and the final ingot is obtained by casting.
[0036]2) Forging: The final ingot is forged at 1150℃ for 2h to form a 50mm×50mm square bar, the final forging temperature is not lower than 950℃, and then air-cooled.
[0037]3) Rolling: The forged square bar is kept at 1100°C for 2h, and then rolled into Φ6.5 wire rod after multiple passes of hot continuous rolling.
[0038]4) Annealing: Keep the wire rod at 1100°C for 1 hour, and then air cool.
[0039]5) Drawing: The wire rods softened by heat treatment are mechanically ...
Embodiment 2
[0043]1) Smelting and casting: Use a vacuum smelting furnace to first smelt ultra-high-strength steel wire alloy ingots, with a vacuum of 15 Pa, and casting to obtain an initial melting ingot; heat the initial melting ingot at 1200°C for 6 hours, and forging into a Φ70mm For the electrode sample, the final forging temperature is not less than 950℃, and the alloy is smelted twice by electroslag remelting, the electroslag speed is 1.8kg / min, the voltage is 35V, the current is 2.0kA, and the final ingot is obtained by casting.
[0044]2) Forging: The final ingot is forged at 1150℃ for 4h into a square bar of 50mm×50mm, the final forging temperature is not lower than 950℃, and then air-cooled.
[0045]3) Rolling: The forged square bar is kept at 1100°C for 2h, and then rolled into Φ6.5 wire rod after multiple passes of hot continuous rolling.
[0046]4) Annealing: Keep the wire rod at 1200°C for 2h, and then air cool.
[0047]5) Drawing: The wire rods softened by heat treatment are mechanically rem...
Embodiment 3
[0051]1) Smelting and casting: Use a vacuum smelting furnace to first smelt ultra-high-strength steel wire alloy ingots, with a vacuum of 12 Pa, and cast the ingots to obtain initial melting ingots; heat the initial melting ingots at 1250°C for 5 hours, and forge them to a diameter of 75 mm For the electrode sample, the final forging temperature is not lower than 950℃, and the alloy is smelted twice by electroslag remelting, the electroslag speed is 1.6kg / min, the voltage is 30V, the current is 2.0kA, and the final ingot is obtained by casting.
[0052]2) Forging: The final ingot is forged at 1150℃ for 4h into a square bar of 50mm×50mm, the final forging temperature is not lower than 950℃, and then air-cooled.
[0053]3) Rolling: The forged square bar is kept at 1100°C for 2h, and then rolled into Φ6.5 wire rod after multiple passes of hot continuous rolling.
[0054]4) Annealing: Keep the wire rod at 1100°C for 2h, then cool in air.
[0055]5) Drawing: The wire rods softened by heat treatment ...