
Patents
Literature
2results about How to "Improve variation" patented technology
Efficacy Topic
Property
Owner
Technical Advancement
Application Domain
Technology Topic
Technology Field Word
Patent Country/Region
Patent Type
Patent Status
Application Year
Inventor
Flame Imitation Manufacturing Device of an Electrical-Heated Fireplace
InactiveUS20080226267A1Improve fidelityIncrease authenticityDomestic stoves or rangesHot-air central heatingBackplaneLight source
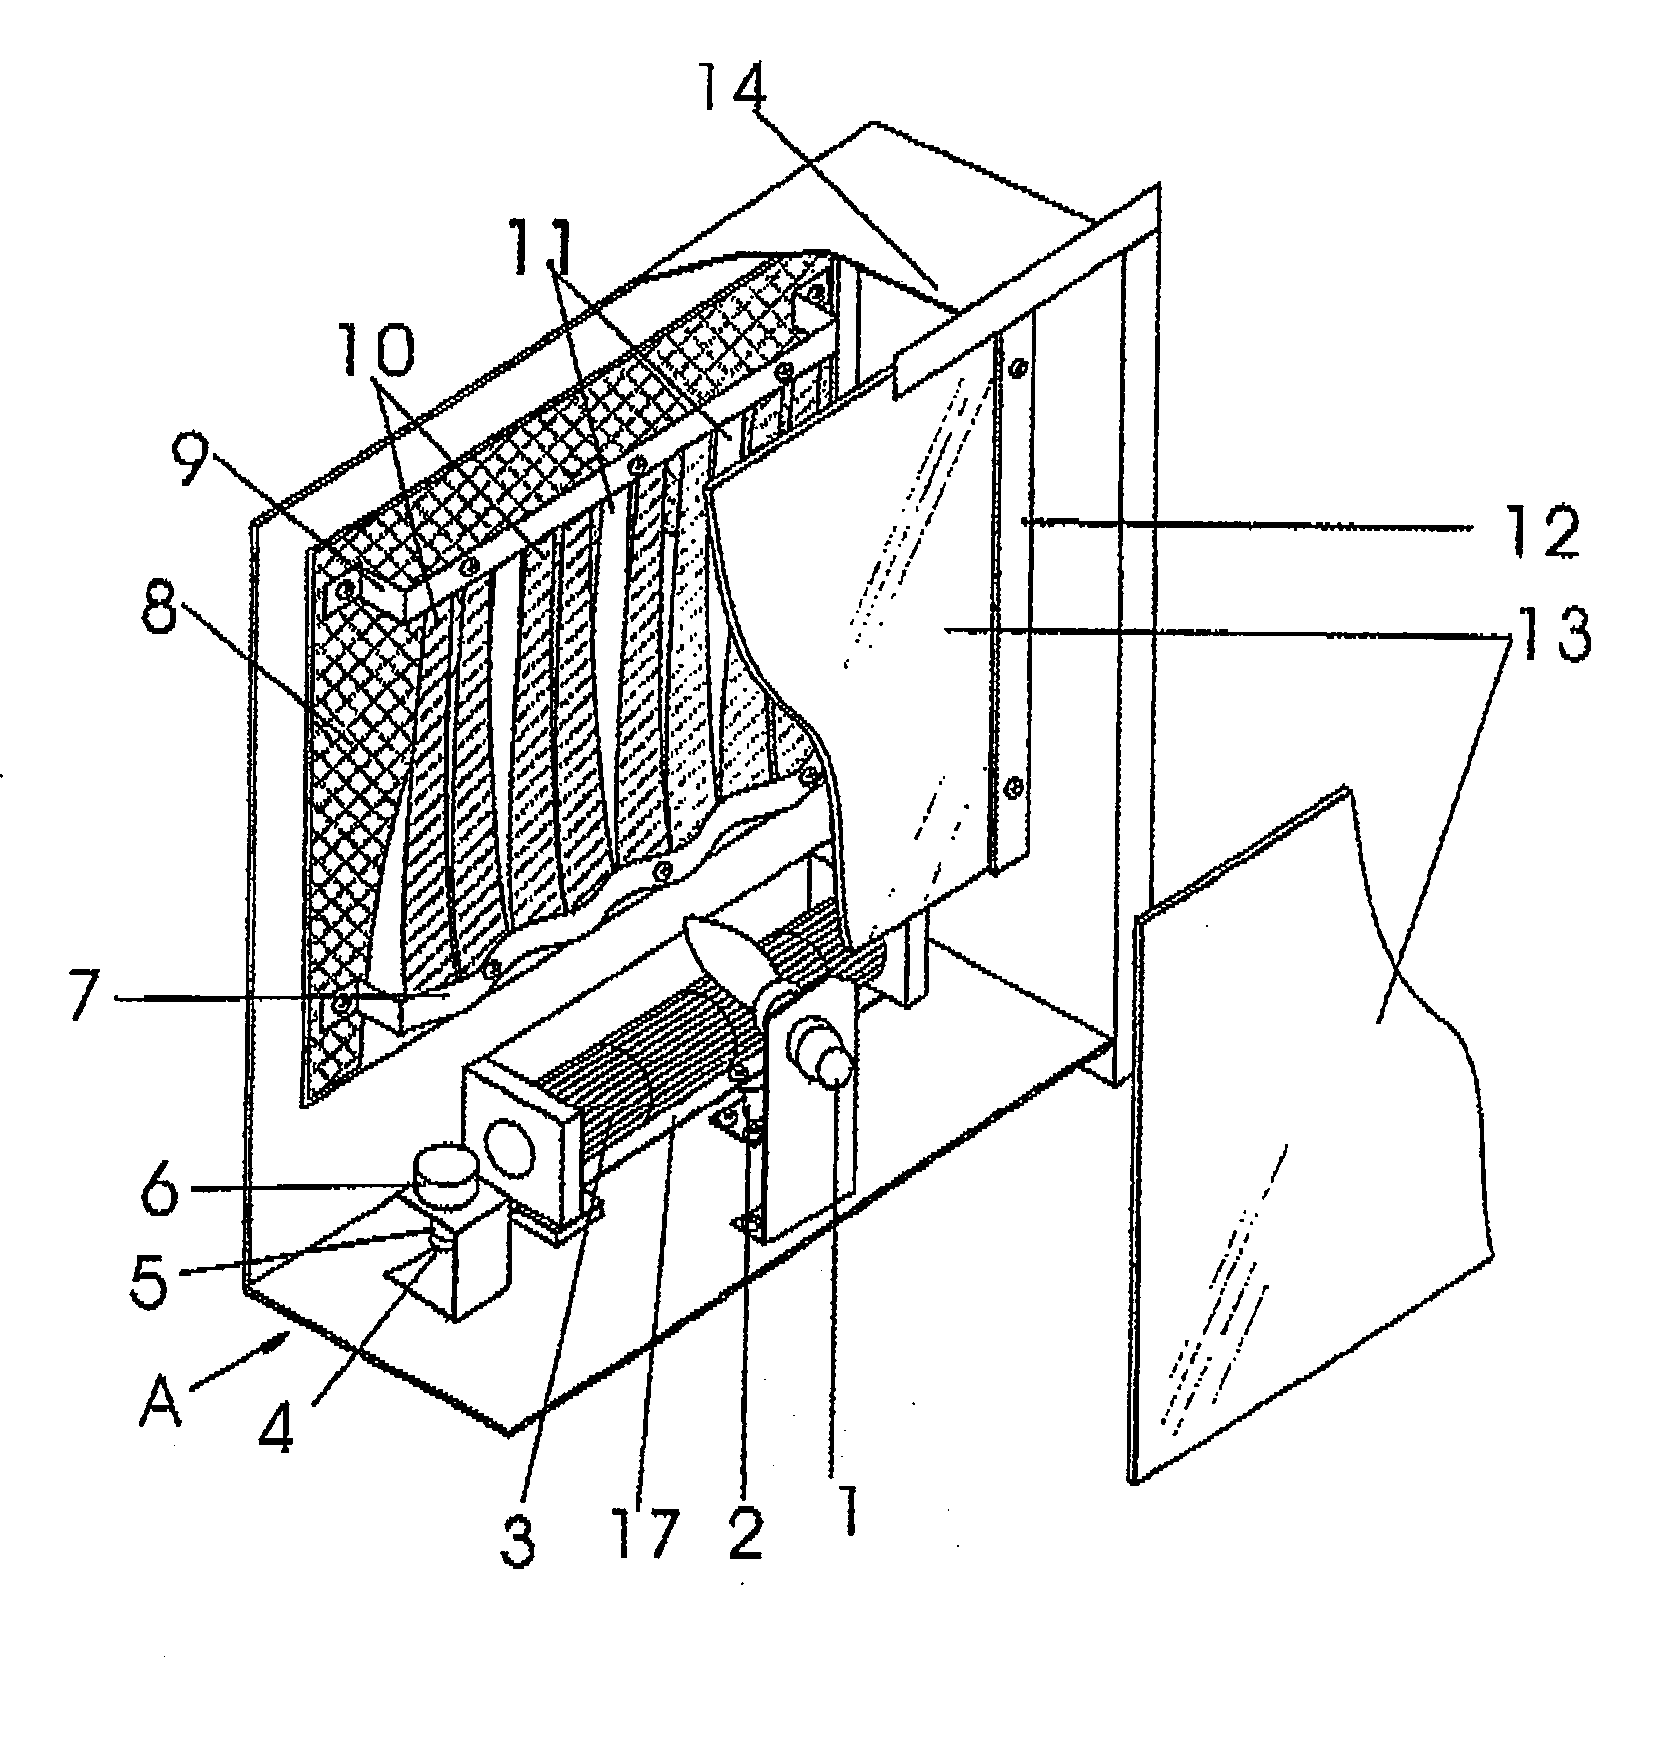
A flame imitation manufacturing device of a fireplace relates to a flame imitation manufacturing device for simulating the burning state in a fireplace in the field of household appliances. Said device comprises a housing, a cross flow fan and a light source mounted on a base plate of the housing, a simulated fire chamber mounted on a back plate of the housing, ribbons mounted on the back plate of the housing by means of upper and lower strip bars and above the cross flow fan, and a light-transmitting glass plate mounted on the housing and in front of said ribbons. This invention, characterized in that said cross flow fan is a swinging one, is advantageous in that supplying wind non-directively by utilizing the swinging of said fan improves the flying state of ribbons so as to make the image state of burning flames more vivid, greatly enhances the authenticity of flames and lowers the cost thereof, and thus is adaptable to various flame imitation electrical-heated fireplaces and electrical appliances.
Owner:WANG ZHUHONG
Non-oriented electromagnetic steel plate and manufacturing method thereof
PendingEP4400610A4reducing manufacturabilityhigh yield stressElectric machinesInorganic material magnetism
Proposed is a non-oriented electrical steel sheet as a steel material from which both a rotor core material having excellent fatigue properties and a stator core material having excellent magnetic properties after core annealing is performed can be obtained. The steel sheet is produced by hot-rolling a steel material including predetermined amounts of C, Si, Mn, and Al, followed by hot-band annealing, cold rolling, and cold-band annealing, wherein the steel sheet is cooled before the final cold rolling to a temperature of 90°C or below followed by aging conducted at a temperature of 100 to 300°, cold rolled in the first pass of the final cold rolling at a bite temperature of 70°C or below using a work roll with a surface roughness Ra of 0.05 to 3.0 µm, and subjected to the cold-band annealing at 700 to 950°C, so that D1 to D3 satisfy predetermined conditions, provided that the average crystal grain size of crystal grains with all orientations, the average crystal grain size of crystal grains with the orientation {411}<148>, and the average crystal grain size of crystal grains with the orientation {211}<011>, each measured by electron backscatter diffraction, are respectively represented by D1, D2, and D3.


Owner:JFE STEEL CORP