
Preparation method of coating on zircomium alloy coverage shell
A technology of zirconium alloy and cladding, which is applied in the field of preparation of coatings on zirconium alloy cladding, can solve the problems of not being able to obtain good bonding force and good surface smoothness at the same time, and achieve small friction coefficient, high bonding force, and high Effect of fine surface texture
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Applications(China)
- Current Assignee / Owner
- Publication Date
- 2019-06-28
Smart Images
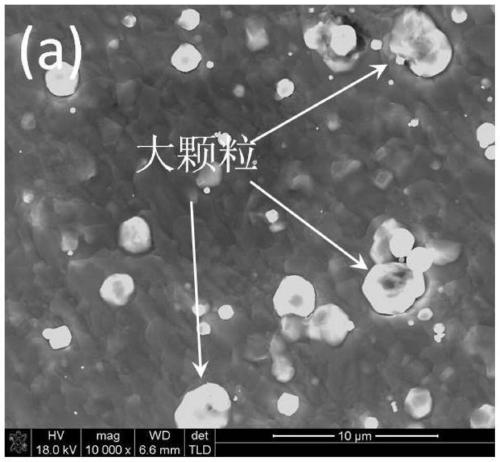
Figure 1 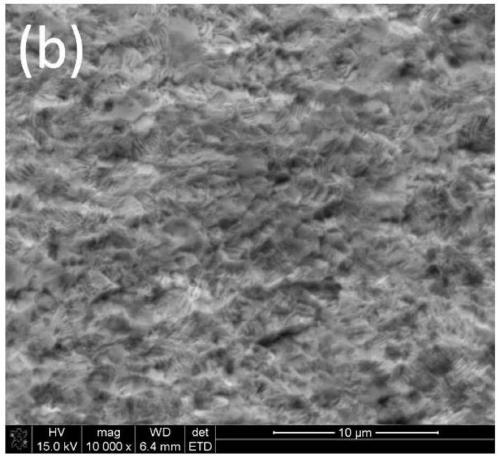
Figure 2 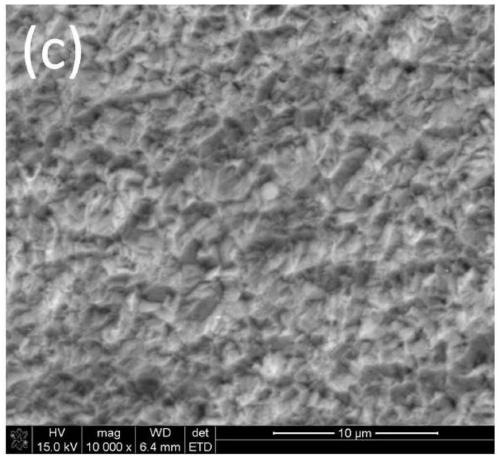
Figure 3
Abstract
Description
technical field
[0001] The invention relates to the field of high-temperature protective coatings, in particular to a preparation method for coatings on zirconium alloy cladding. Background technique
[0002] Zirconium alloys have long been used as fuel cladding materials for water-cooled reactors due to their low thermal neutron absorption cross section, moderate mechanical properties, good corrosion resistance and processability. But after the Fukushima nuclear accident in 2011, international efforts were made to research accident-tolerant fuel (ATF) to replace the existing UO 2 -Zr fuel system to improve the ability of nuclear fuel elements to maintain structural integrity under severe accidents, thereby improving the safety and reliability of nuclear reactors under accident conditions.
[0003] The concept of ATF accident-resistant fuel includes fuel pellets and fuel cladding. From the point of view of fuel cladding, the main consideration is to further improve its abi...
Examples
Embodiment 1
[0054] A method for preparing a coating on a zirconium alloy cladding, comprising:
[0055] (1) Pre-treatment: Place the obtained Zircaloy-4 alloy pipe or N36 alloy pipe in an ultrasonic container and clean them with carbon tetrachloride and acetone for 10 to 20 minutes respectively, then ultrasonically clean them with deionized water for more than 10 minutes, and finally Rinse the stage with deionized water. Dry the cleaned pipe samples in a vacuum oven at a temperature not exceeding 50°C. Clamp the pre-treated sample on the turntable of the coating equipment.
[0056] (2) Ion cleaning: evacuate the vacuum chamber of the coating equipment until the vacuum degree reaches above 1×10⁻³Pa, then fill it with argon gas at a certain flow rate to keep the pressure in the vacuum chamber at 0.1-5Pa. Adjust the bias voltage above -1000V for about 10 to 20 minutes, and bombard the surface of the zirconium alloy tube with the high-speed Ar ion flow to achieve the purpose of further clea...
Embodiment 2
[0067] A method for preparing a coating on a zirconium alloy cladding, comprising:
[0068] (1) Pre-treatment: Place the obtained Zircaloy-4 alloy pipe or N36 alloy pipe in an ultrasonic container and clean them with carbon tetrachloride and acetone for 10 to 20 minutes respectively, then ultrasonically clean them with deionized water for more than 10 minutes, and finally Rinse the stage with deionized water. Dry the cleaned pipe samples in a vacuum oven at a temperature not exceeding 50°C. Clamp the pre-treated sample on the turntable of the coating equipment.
[0069] (2) Ion cleaning: evacuate the vacuum chamber of the coating equipment until the vacuum degree reaches above 1×10⁻³Pa, then fill it with argon gas at a certain flow rate to keep the pressure in the vacuum chamber at 0.1-5Pa. Adjust the bias voltage above -1000V for about 10 to 20 minutes, and bombard the surface of the zirconium alloy tube with the high-speed Ar ion flow to achieve the purpose of further clea...
Embodiment 3
[0080] A method for preparing a coating on a zirconium alloy cladding, comprising:
[0081] (1) Pre-treatment: Place the obtained Zircaloy-4 alloy pipe or N36 alloy pipe in an ultrasonic container and clean them with carbon tetrachloride and acetone for 10 to 20 minutes respectively, then ultrasonically clean them with deionized water for more than 10 minutes, and finally Rinse the stage with deionized water. Dry the cleaned pipe samples in a vacuum oven at a temperature not exceeding 50°C. Clamp the pre-treated sample on the turntable of the coating equipment.
[0082] (2) Ion cleaning: evacuate the vacuum chamber of the coating equipment until the vacuum degree reaches above 1×10⁻³Pa, then fill it with argon gas at a certain flow rate to keep the pressure in the vacuum chamber at 0.1-5Pa. Adjust the bias voltage above -1000V for about 10 to 20 minutes, and bombard the surface of the zirconium alloy tube with the high-speed Ar ion flow to achieve the purpose of further clea...