
Method for preparing screw-thread wear-resistant corrosion-resistant anti-lock coating by adopting multi-arc ion plating
A multi-arc ion plating, anti-locking technology, applied in the direction of ion implantation plating, coating, superimposed layer plating, etc., to achieve good bonding ability, avoid corrosion damage, high hardness
Patent Information
- Authority / Receiving Office
- CN · China
- Current Assignee / Owner
- Publication Date
- 2018-06-19
Smart Images
Figure 1 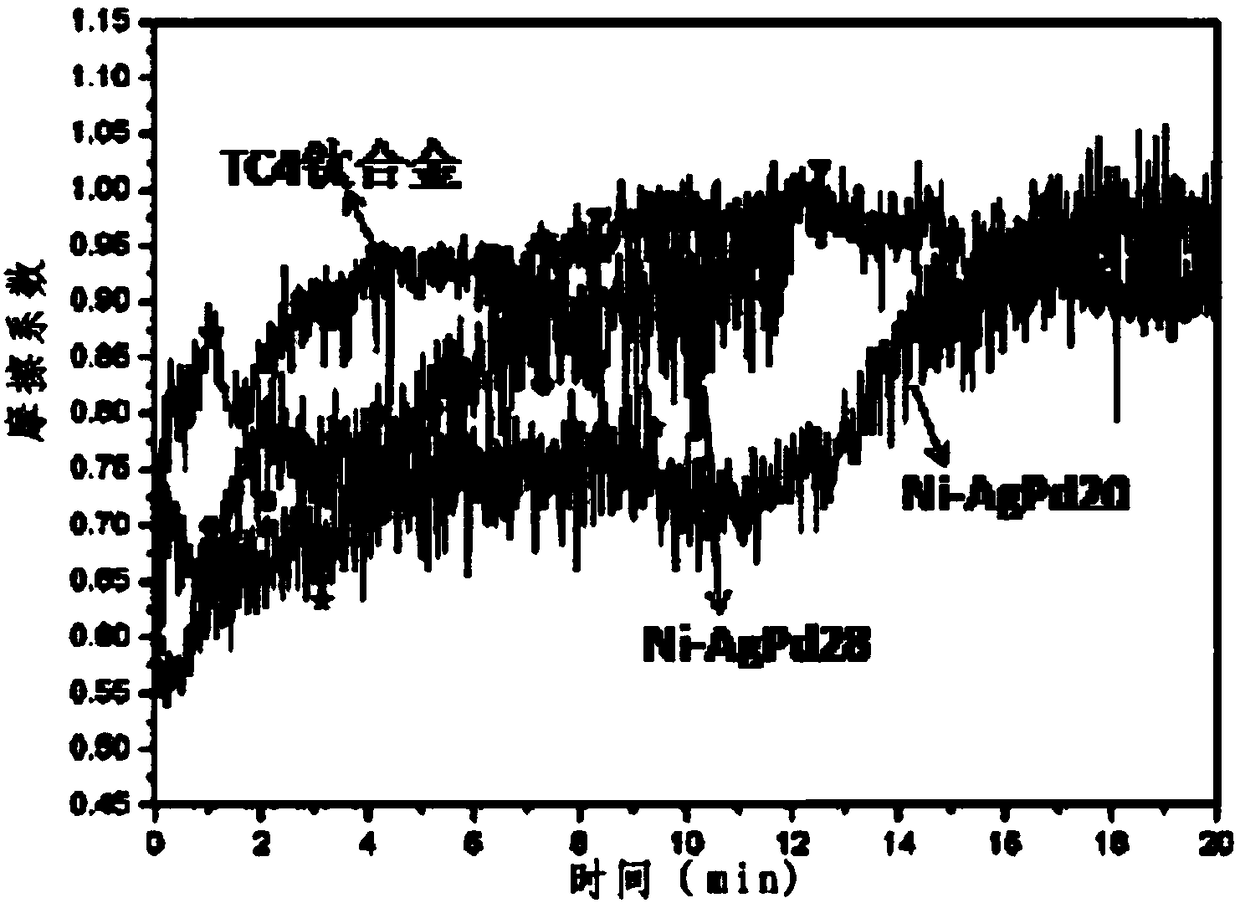
Figure 2
Abstract
Description
technical field
[0001] The invention belongs to the technical field of anti-locking coating preparation, and in particular relates to a method for preparing a wear-resistant, corrosion-resistant and anti-locking coating for threads by using multi-arc ion plating. Background technique
[0002] At present, stainless steel or titanium alloy fasteners widely used in the market are common materials in mechanical production and assembly, but it is easy to cause locking during the fastening process, that is, the connection between the bolt and the nut is too tight and cannot be opened. Stainless steel or titanium alloy fasteners often form a metal oxide layer on their surface in order to resist the erosion of the external environment during use. This metal oxide layer can protect the bolts from external erosion and avoid corrosion. Extends the life of the bolt, but also increases the risk of thread locking. When the bolt is tightened, the pressure and heat generated by the frictio...
Examples
Embodiment 1
[0025] This embodiment includes the following steps:
[0026] Step 1. Put the 316 stainless steel threads into a vibration polishing machine for polishing for 15 minutes, then use acetone, distilled water, and ethanol to ultrasonically clean the polished metal threads for 8 minutes, 2 minutes, and 2 minutes respectively, and then dry them; the polishing process Add white corundum balls with a diameter of 1mm to 5mm and diamond polishing fluid;
[0027] Step 2, the 316 stainless steel threads dried in step 1 are subjected to sandblasting roughening treatment; the sand grains of the sandblasting roughening treatment are 200 mesh quartz sand, the sandblasting pressure is 0.15MPa, and the sandblasting time is 600s;
[0028] Step 3. Place the 316 stainless steel threads that have been roughened by sandblasting in step 2 in the coating chamber of the multi-arc ion plating equipment, and then vacuumize the coating chamber to a vacuum degree of 0.004Pa, and put it into the vacuumized ...
Embodiment 2
[0033] This embodiment includes the following steps:
[0034] Step 1. Put the TC4 titanium alloy thread into a vibration polishing machine for polishing for 25 minutes, then use acetone, distilled water, and ethanol to ultrasonically clean the polished metal thread for 10 minutes, 5 minutes, and 5 minutes respectively, and then dry; Add white corundum balls with a diameter of 1mm to 5mm and diamond polishing fluid during the process;
[0035] Step 2, performing sandblasting roughening treatment on the dried TC4 titanium alloy thread in step 1; the sand grains of the sandblasting roughening treatment are 250 mesh quartz sand, the sandblasting pressure is 0.3MPa, and the sandblasting time is 200s;
[0036] Step 3. Place the TC4 titanium alloy thread after sandblasting and roughening treatment in step 2 in the coating chamber of the multi-arc ion plating equipment, and then vacuumize the coating chamber to a vacuum degree of 0.003Pa, and put it into the vacuumized reaction chambe...
Embodiment 3
[0040] This embodiment includes the following steps:
[0041] Step 1. Put the TC4 titanium alloy thread into a vibration polishing machine for polishing treatment for 40 minutes, then use acetone, distilled water and ethanol to ultrasonically clean the polished metal thread for 9 minutes, 3 minutes and 3 minutes respectively, and then dry; Add white corundum balls with a diameter of 1mm to 5mm and diamond polishing fluid during the process;
[0042] Step 2. Perform sandblasting roughening treatment on the dried TC4 titanium alloy thread in step 1; the sand grains of the sandblasting roughening treatment are 300 mesh quartz sand, the sandblasting pressure is 0.80MPa, and the sandblasting time is 20s;
[0043] Step 3. Place the TC4 titanium alloy thread after sandblasting and roughening treatment in step 2 in the coating chamber of the multi-arc ion plating equipment, and then vacuumize the coating chamber to a vacuum degree of 0.004Pa, and put it into the vacuumized reaction ch...