
Phosphatized cold-rolled strip steel and manufacturing method thereof
A technology for cold-rolled strip steel and a manufacturing method, which is applied to manufacturing tools, furnaces, heat treatment equipment, etc., can solve the problem of affecting the quality of the upper film and the service life of the phosphating agent, affecting the adhesion and corrosion resistance of the paint film, and phosphating treatment. Problems such as complex process flow, to achieve the effect of improving phosphating effect and efficiency, improving formation speed and uniform density, and ensuring cleanliness
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Applications(China)
- Current Assignee / Owner
- Publication Date
- 2019-06-28
Smart Images
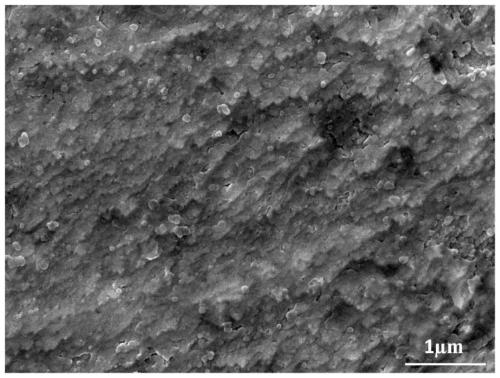
Figure 1 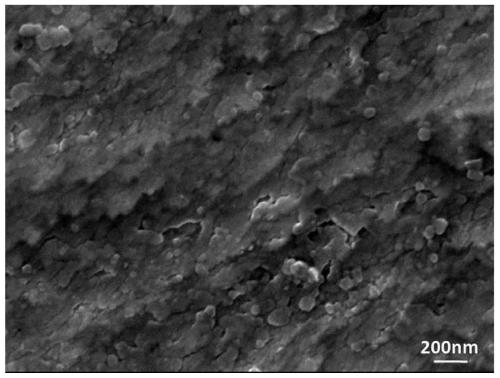
Figure 2 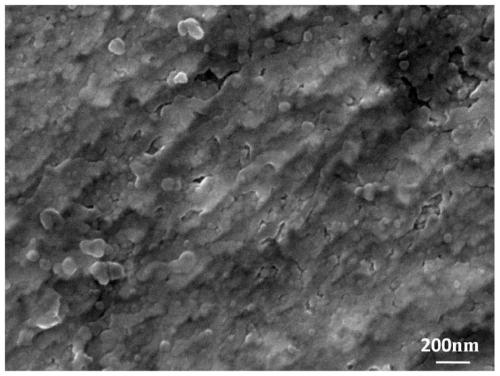
Figure 3
Abstract
Description
technical field
[0001] The invention belongs to the technical field of iron and steel production, in particular to a phosphating cold-rolled steel strip and a manufacturing method. Background technique
[0002] Cold-rolled strip steel has the advantages of good surface finish, good flatness, high dimensional accuracy, and good mechanical properties. It can be used to make oil barrels and containers, and can also be used to manufacture building panels, office supply cabinets, and electronic machinery. However, after processing and forming and before coating, the cold-rolled strip steel needs to be phosphating. Surface phosphating treatment is an extremely important process in the manufacturing process of steel drums, such as steel coil uncoiling and blanking, stamping and forming of drum bottom cover, welding and forming assembly of drum body, surface phosphating, internal and external coating, etc. Phosphating is the process in which metal reacts with dilute phosphoric acid...
Examples
Embodiment 1
[0036] The chemical composition of steel for oil barrels is: C 0.030%, Mn 0.40%, Si 0.01%, Al 0.05%, P 0.018%, S 0.0035%, and the balance is Fe and impurity elements.
[0037] The strip steel whose chemical composition meets the above requirements is subjected to conventional treatments such as decoiling, welding, degreasing cleaning, annealing, leveling and tension leveling on the continuous annealing line. was 1.4%. After the treatment, enter the phosphating treatment area, first enter the phosphating section for phosphating treatment, the phosphating section adopts a spray process, the pH value of the phosphating solution is 2.2, the phosphating time is 41s, and the temperature of the phosphating solution is 42°C. The phosphating solution is composed of the following components: zinc dihydrogen phosphate 80g / L, zinc nitrate 69g / L, phosphoric acid 15g / L, sodium chlorate 1.9g / L, tartaric acid 5.8g / L, sodium fluoride 1.5g / L, sulfuric acid Hydroxylamine 2.2g / L, phytic acid 1.7...
Embodiment 2
[0041] The chemical composition of steel for oil barrels is: C 0.040%, Mn 0.20%, Si 0.018%, Al 0.027%, P 0.005%, S 0.011%, and the balance is Fe and impurity elements.
[0042]The strip steel whose chemical composition meets the above requirements is subjected to conventional treatments such as decoiling, welding, degreasing cleaning, annealing, leveling and tension leveling on the continuous annealing line. was 1.1%. After the treatment, enter the phosphating treatment area, first enter the phosphating section for phosphating treatment, the phosphating section adopts a spray process, the pH value of the phosphating solution is 2.8, the phosphating time is 49s, and the temperature of the phosphating solution is 45°C. The phosphating solution is composed of the following components: zinc dihydrogen phosphate 65g / L, zinc nitrate 78g / L, phosphoric acid 11g / L, sodium chlorate 1.3g / L, tartaric acid 6.8g / L, sodium fluoride 1.9g / L, sulfuric acid Hydroxylamine 1.1g / L, phytic acid 1.2...
Embodiment 3
[0046] The chemical composition of steel for oil barrels is: C 0.035%, Mn 0.30%, Si 0.04%, Al 0.01%, P 0.012%, S 0.0047%, and the balance is Fe and impurity elements.
[0047] The steel strip whose chemical composition meets the above requirements is subjected to conventional treatments such as uncoiling, welding, degreasing cleaning, annealing, leveling and tension leveling on the continuous annealing line. was 1.2%. After the treatment, enter the phosphating treatment area, first enter the phosphating section for phosphating treatment, the phosphating section adopts a spraying process, the pH value of the phosphating solution is 2.5, the phosphating time is 49s, and the temperature of the phosphating solution is 48°C. The phosphating solution is composed of the following components: zinc dihydrogen phosphate 97g / L, zinc nitrate 52g / L, phosphoric acid 18g / L, sodium chlorate 3.0g / L, tartaric acid 5.4g / L, sodium fluoride 1.2g / L, sulfuric acid Hydroxylamine 1.7g / L, phytic acid ...