
CSPC highlight floor and preparation method thereof
A technology of flooring and PVC resin, applied in the field of CSPC high-gloss flooring and its preparation, can solve the problems of rough raw materials, low-quantity wear-resistant surface paper, and large changes in environmental temperature and humidity, and achieve the effect of eliminating hazards
Patent Information
- Authority / Receiving Office
- CN · China
- Current Assignee / Owner
- Publication Date
- 2022-04-12
Smart Images
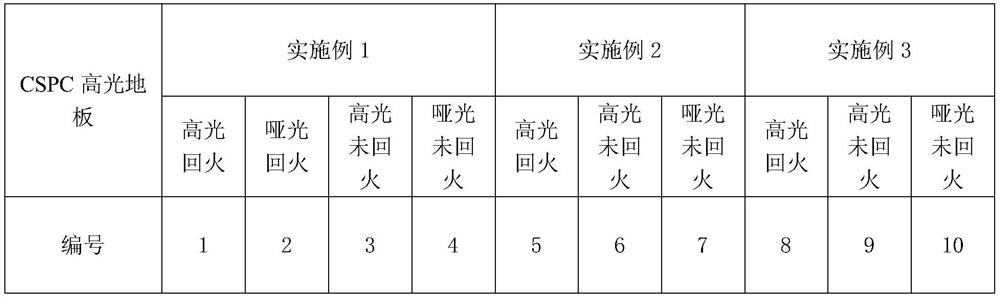
Figure 1 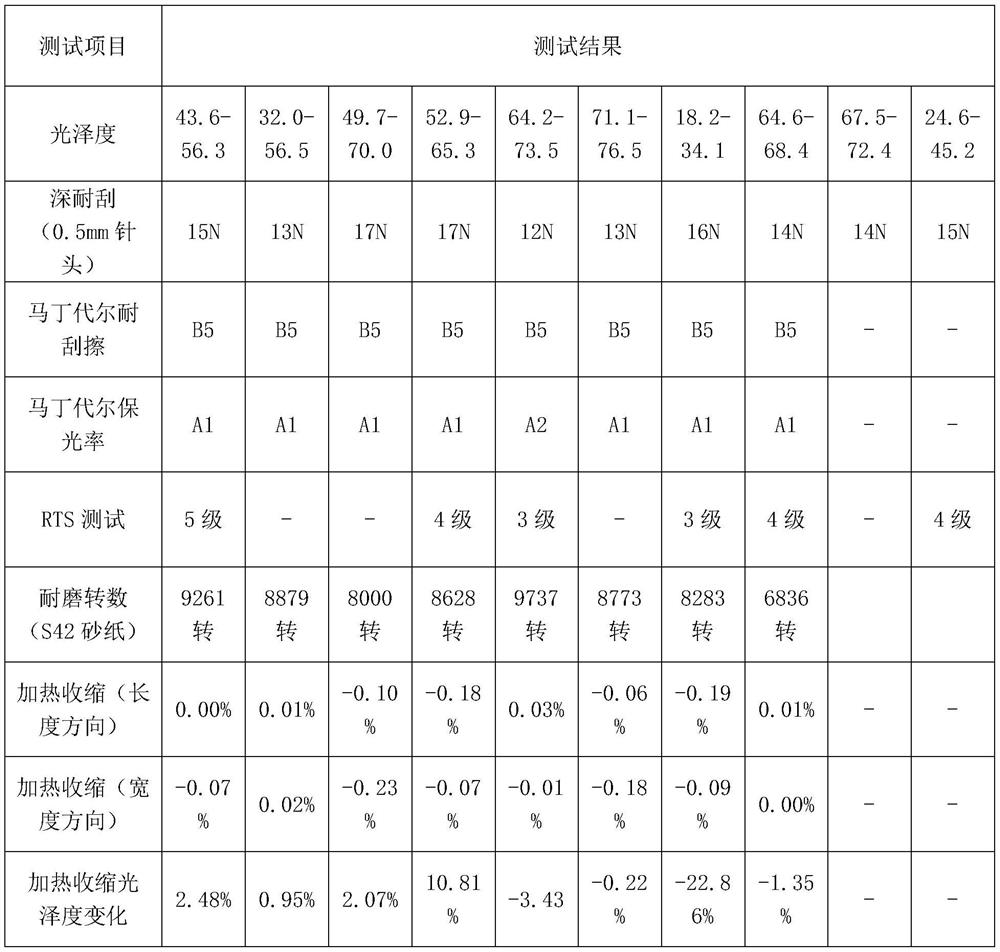
Figure 2
Abstract
Description
technical field
[0001] The invention relates to a high-gloss floor and a preparation method thereof, in particular to a CSPC high-gloss floor and a preparation method thereof. Background technique
[0002] At present, some laminate flooring products on the market have only 3000 revolutions on the surface, which is far lower than the 6000 revolutions stipulated by the national standard, and some even have only a few hundred revolutions. These products use low-quantity wear-resistant surface paper, and even the surface paper that does not contain alumina is shoddy, which greatly reduces the service life of laminate flooring. This is why the "five bad boards" frequently appear in recent years. one of the roots. However, some decorative paper manufacturers have low equipment precision, large changes in environmental temperature and humidity, and rough raw materials. The final products often appear: ① unnatural white spots, white spots, black spots and black spots; ② blurred tex...
Examples
Embodiment 1
[0017] For the CSPC high-gloss floor of the present embodiment, the base material of the floor comprises the following raw material components in parts by weight: 27 parts of PVC resin, 63 parts of stone powder, 6 parts of calcium zinc stabilizer, 10 parts of plasticizer and 2 parts of soybean oil.
[0018] The preparation method of the CSPC high-gloss floor of the present embodiment may further comprise the steps:
[0019] (1) PVC resin is mixed with stone powder, then calcium-zinc stabilizer, plasticizer and soybean oil are added and mixed to obtain a mixture;
[0020] (2) Extrude the mixture to form a stone-plastic base plate under the conditions of vacuuming and a temperature of 160°C;
[0021] (3) The color film and transparent sheet are hot-pressed with the stone-plastic base plate, and the hot-pressing temperature is controlled at 120°C;
[0022] (4) Carry out roller coating to the semi-finished product after hot-press forming, and the paint of roller coating adopts UV...
Embodiment 2
[0025] For the CSPC high-gloss floor of the present embodiment, the base material of the floor comprises the following raw material components in parts by weight: 37 parts of PVC resin, 73 parts of stone powder, 8 parts of calcium zinc stabilizer, 20 parts of plasticizer and 6 parts of soybean oil.
[0026] The preparation method of the CSPC high-gloss floor of the present embodiment may further comprise the steps:
[0027] (1) PVC resin is mixed with stone powder, then calcium-zinc stabilizer, plasticizer and soybean oil are added and mixed to obtain a mixture;
[0028] (2) Extrude the mixture to form a stone-plastic base plate under the conditions of vacuuming and a temperature of 180°C;
[0029] (3) The color film and transparent sheet are hot-pressed with the stone-plastic base plate, and the hot-pressing temperature is controlled at 140°C;
[0030] (4) Carry out roller coating to the semi-finished product after hot-press forming, and the paint of roller coating adopts UV...
Embodiment 3
[0033] For the CSPC high-gloss floor of the present embodiment, the base material of the floor comprises the following raw material components in parts by weight: 32 parts of PVC resin, 68 parts of stone powder, 7 parts of calcium-zinc stabilizer, 15 parts of plasticizer and 4 parts of soybean oil. The preparation method of the CSPC high-gloss floor of the present embodiment may further comprise the steps:
[0034] (1) PVC resin is mixed with stone powder, then calcium-zinc stabilizer, plasticizer and soybean oil are added and mixed to obtain a mixture;
[0035] (2) Extrude the mixture to form a stone-plastic substrate plate under the conditions of vacuuming and a temperature of 170°C;
[0036] (3) The color film and transparent sheet are hot-pressed with the stone-plastic base plate, and the hot-pressing temperature is controlled at 130°C;
[0037] (4) Carry out roller coating to the semi-finished product after hot-press forming, and the paint of roller coating adopts UV pai...