
Combined mould for precasting ring-type forge piece cast steel billet
A combined mold and ring forging technology, which is applied in the field of mechanical forging and casting, can solve the problems of mold bodies stuck together and cannot be separated, cracks or cracks, scrapping, etc., to reduce production costs, simplify forging process, and simple method and structure Effect
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Patents(China)
- Current Assignee / Owner
- Publication Date
- 2008-02-13
- Estimated Expiration
- Not applicable · inactive patent
Smart Images
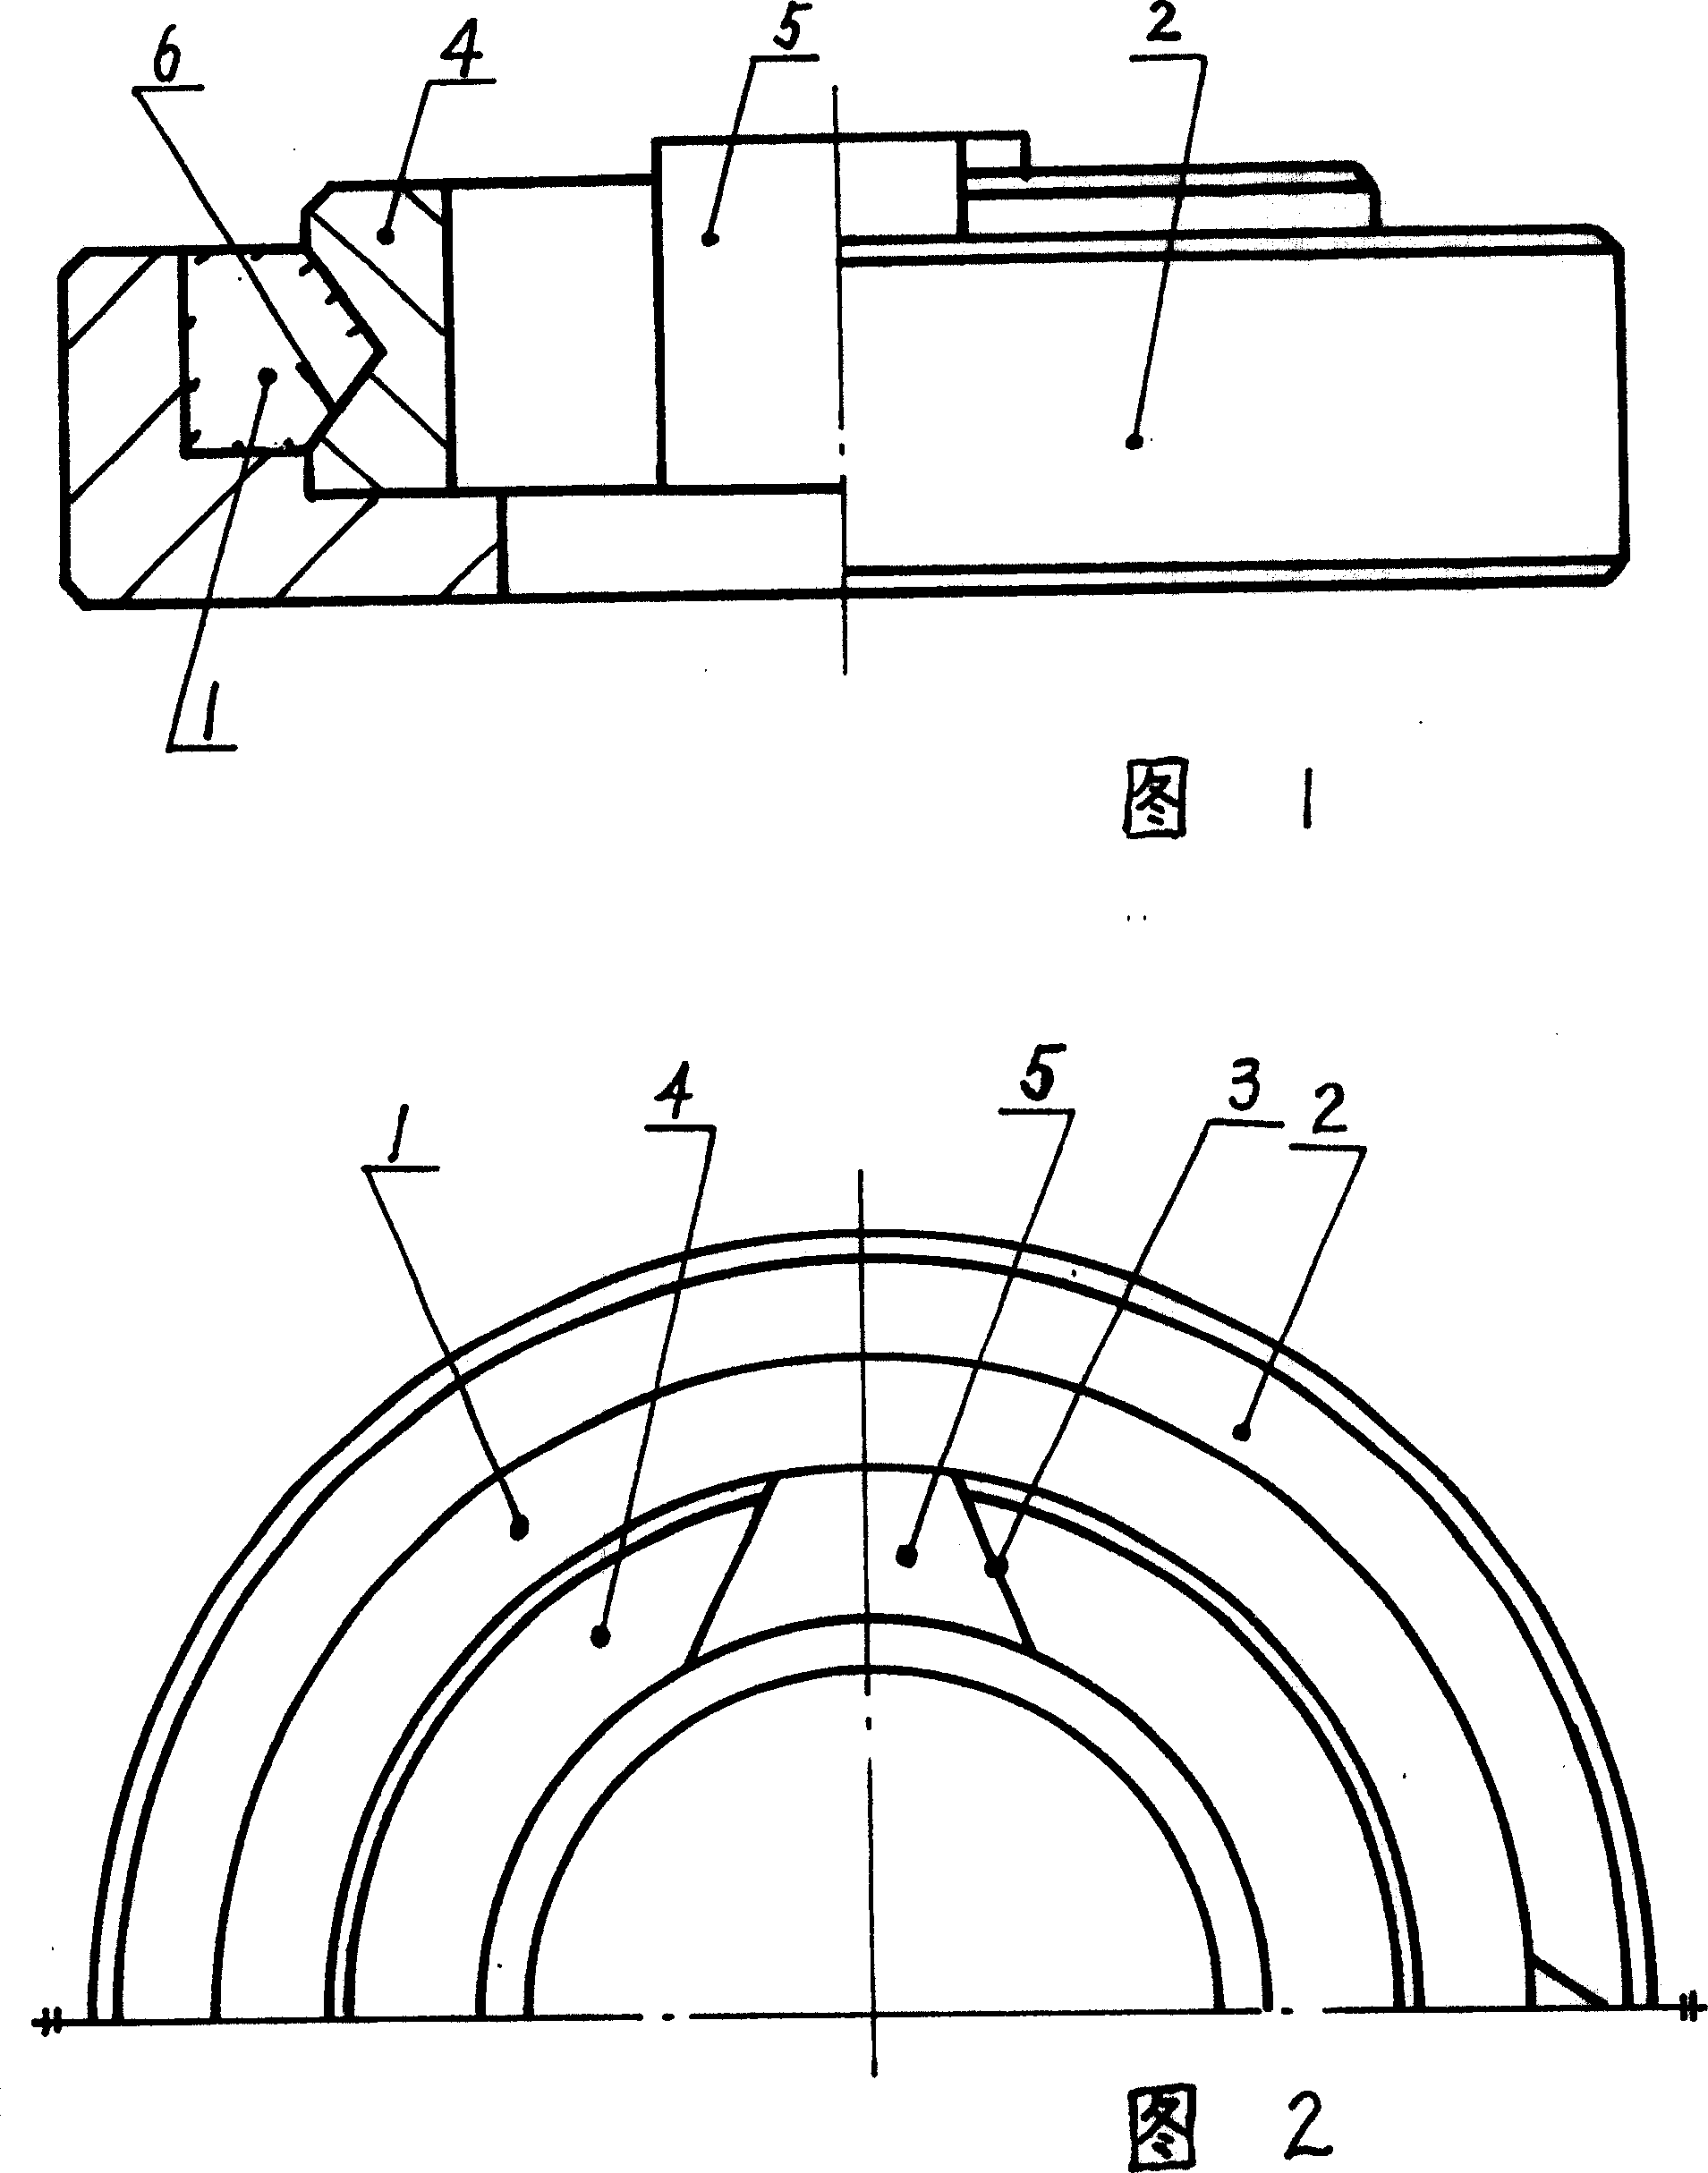
Figure 1
Abstract
Description
technical field
[0001] The invention relates to the technical field of mechanical forging and casting, in particular to a special mold for manufacturing a prefabricated part of a ring-shaped forging whose cross-section is circular or rectangular, that is, a cast billet. Background technique
[0002] At present, ring-shaped mechanical parts with a large load and special technical requirements, with circular or rectangular cross-sections and large geometric dimensions and weights, are all made of forgings made by free forging through machining and other processes. ; Both heat the hot-rolled square steel with a side length of 200-300 mm to the forging temperature and then cut it with a chisel or chop it, then heat the billet for the second time and upsetting, punching, and then pass through the third time After heating, reaming and forming; the forging can be formed when it has a rectangular cross-section, and it can only be pre-formed when its forging is a circular cross-secti...
Examples
Embodiment Construction
[0013] The present invention will be further described below in conjunction with accompanying drawing:
[0014] In Fig. 1 and Fig. 2: annular casting billet 1, lower mold body 2, inner ring body 3, small ring block 4, small wedge block 5, annular surface 6.
[0015] In the embodiment shown in the drawings, the inner ring body 3 of combined structure is provided in the annular cavity of the lower mold body 2, and the inner ring body 3 is arranged in the concave step at the bottom of the cavity of the lower mold body 2, and the inner ring body 3 The ring body 3 is composed of two small ring blocks 4 and two small wedge blocks 5 respectively. The upper end surface, and the annular outer surface of the inner ring body 3, that is, the cavity surface in contact with the annular cast billet 1, is provided with a concave isosceles triangular annular surface 6, and the draft slope is not selected.
[0016] During use, it is enough to assemble the inner ring body 3 of the combined stru...