
Forging molding technological method for multi-lug part
A technology of forging molding and process method, applied in the field of forging, can solve the problems of large flash rate of blanks, noise pollution, waste of time, manpower, etc., and achieve the effects of simple forging process, improvement of production efficiency, and reduction of waste of blanks
Patent Information
- Authority / Receiving Office
- CN · China
- Current Assignee / Owner
- Publication Date
- 2015-11-18
- Estimated Expiration
- Not applicable · inactive patent
Smart Images
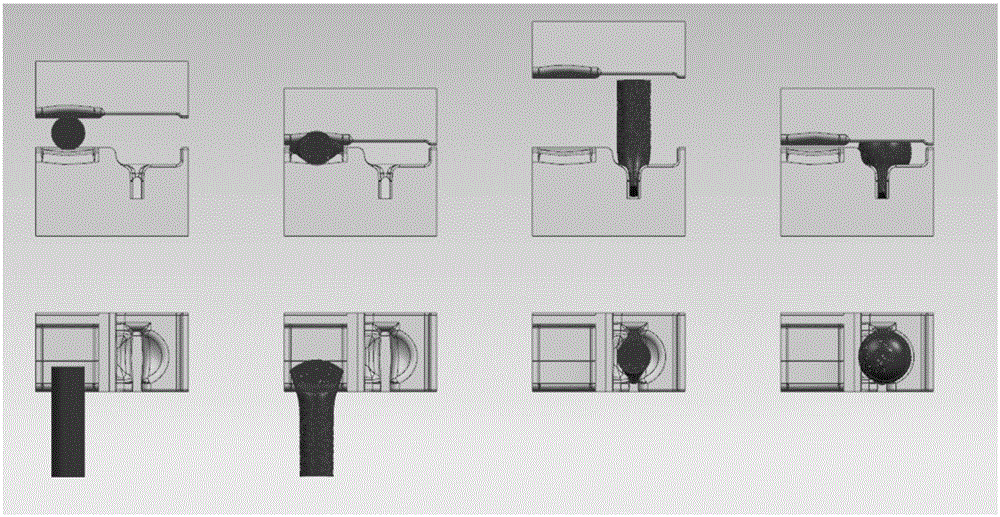
Figure 1 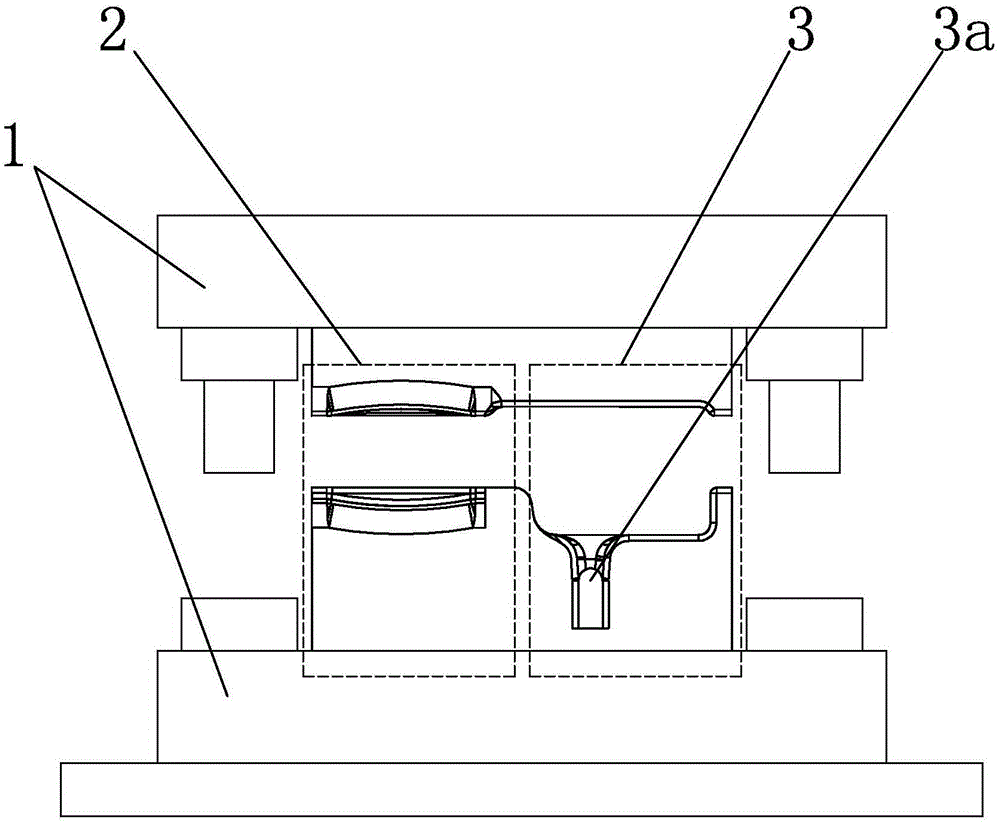
Figure 2 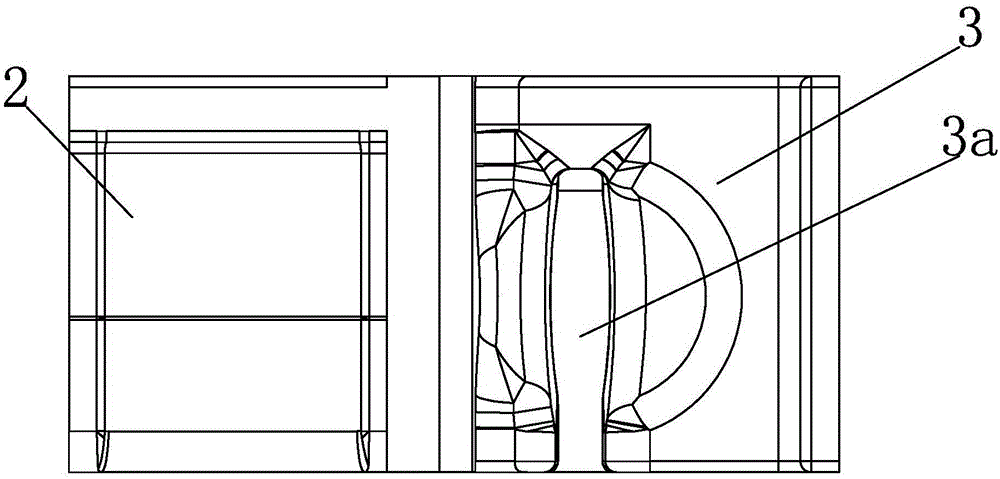
Figure 3
Abstract
Description
technical field
[0001] The invention belongs to the technical field of forging, and in particular relates to a forging forming process method of multi- lug parts. Background technique
[0002] When the current forging plants are forging parts with multiple lugs (such as automobile steering knuckles, crankshafts, and camshafts), the usual forming method is that the round bar is blanked by the blanking machine-heated by an intermediate frequency furnace-use air hammer, Forging machine, punching blank release - press pre-forging die forming - press final forging die forming - punching or press trimming correction, the most important of which is the link of billet unloading and pre-forging die forming, which determines the entire process. The blanking weight and forging time of parts forging, in the forming process of steering knuckles, crankshafts and other multi-lug parts of automobiles, air hammer or roller forging machine is required in the process of laying blanks, and the ...
Examples
Embodiment
[0019] A kind of forging forming process method of multiple lug parts, taking the crankshaft as an example to complete according to the following steps:
[0020] a. Heating for blanking: heating the round bar blank after blanking.
[0021] b. Flattening: if figure 1 As shown in the four figures on the left side of the middle, one end of the round bar blank is placed on the pressing die 1, and one end of the round bar blank is flattened after the pressing die 1 is closed once.
[0022] c. Pier rough pressing: such as figure 1 As shown in the four figures on the right side of the middle, the flattened end of the round bar blank is vertically inserted into the "V"-shaped groove 3a of the blank-making cavity of the pressing die 1, and the other end of the round bar blank is roughly pressed, thereby A blank whose contour matches the cavity of the pre-forging die is obtained; the two-step process of steps b and c is completed on one pressing die 1 .
[0023] d. Forging molding:...