
Preparation method for on-line pulling and extruding glass steel tube with multilayer annular weaving structure
A technology of circular braiding and fiberglass steel pipes, which is applied to household appliances, tubular objects, and other household appliances, etc. It can solve the problems of insufficient stretching of reinforcing fibers, loss of fiber prestressing effect, and inability to exert high tensile strength of fibers, etc., to achieve consistent strength , High production efficiency, uniform impregnation effect
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Patents(China)
- Current Assignee / Owner
- Publication Date
- 2010-01-20
- Estimated Expiration
- Not applicable · inactive patent
Smart Images
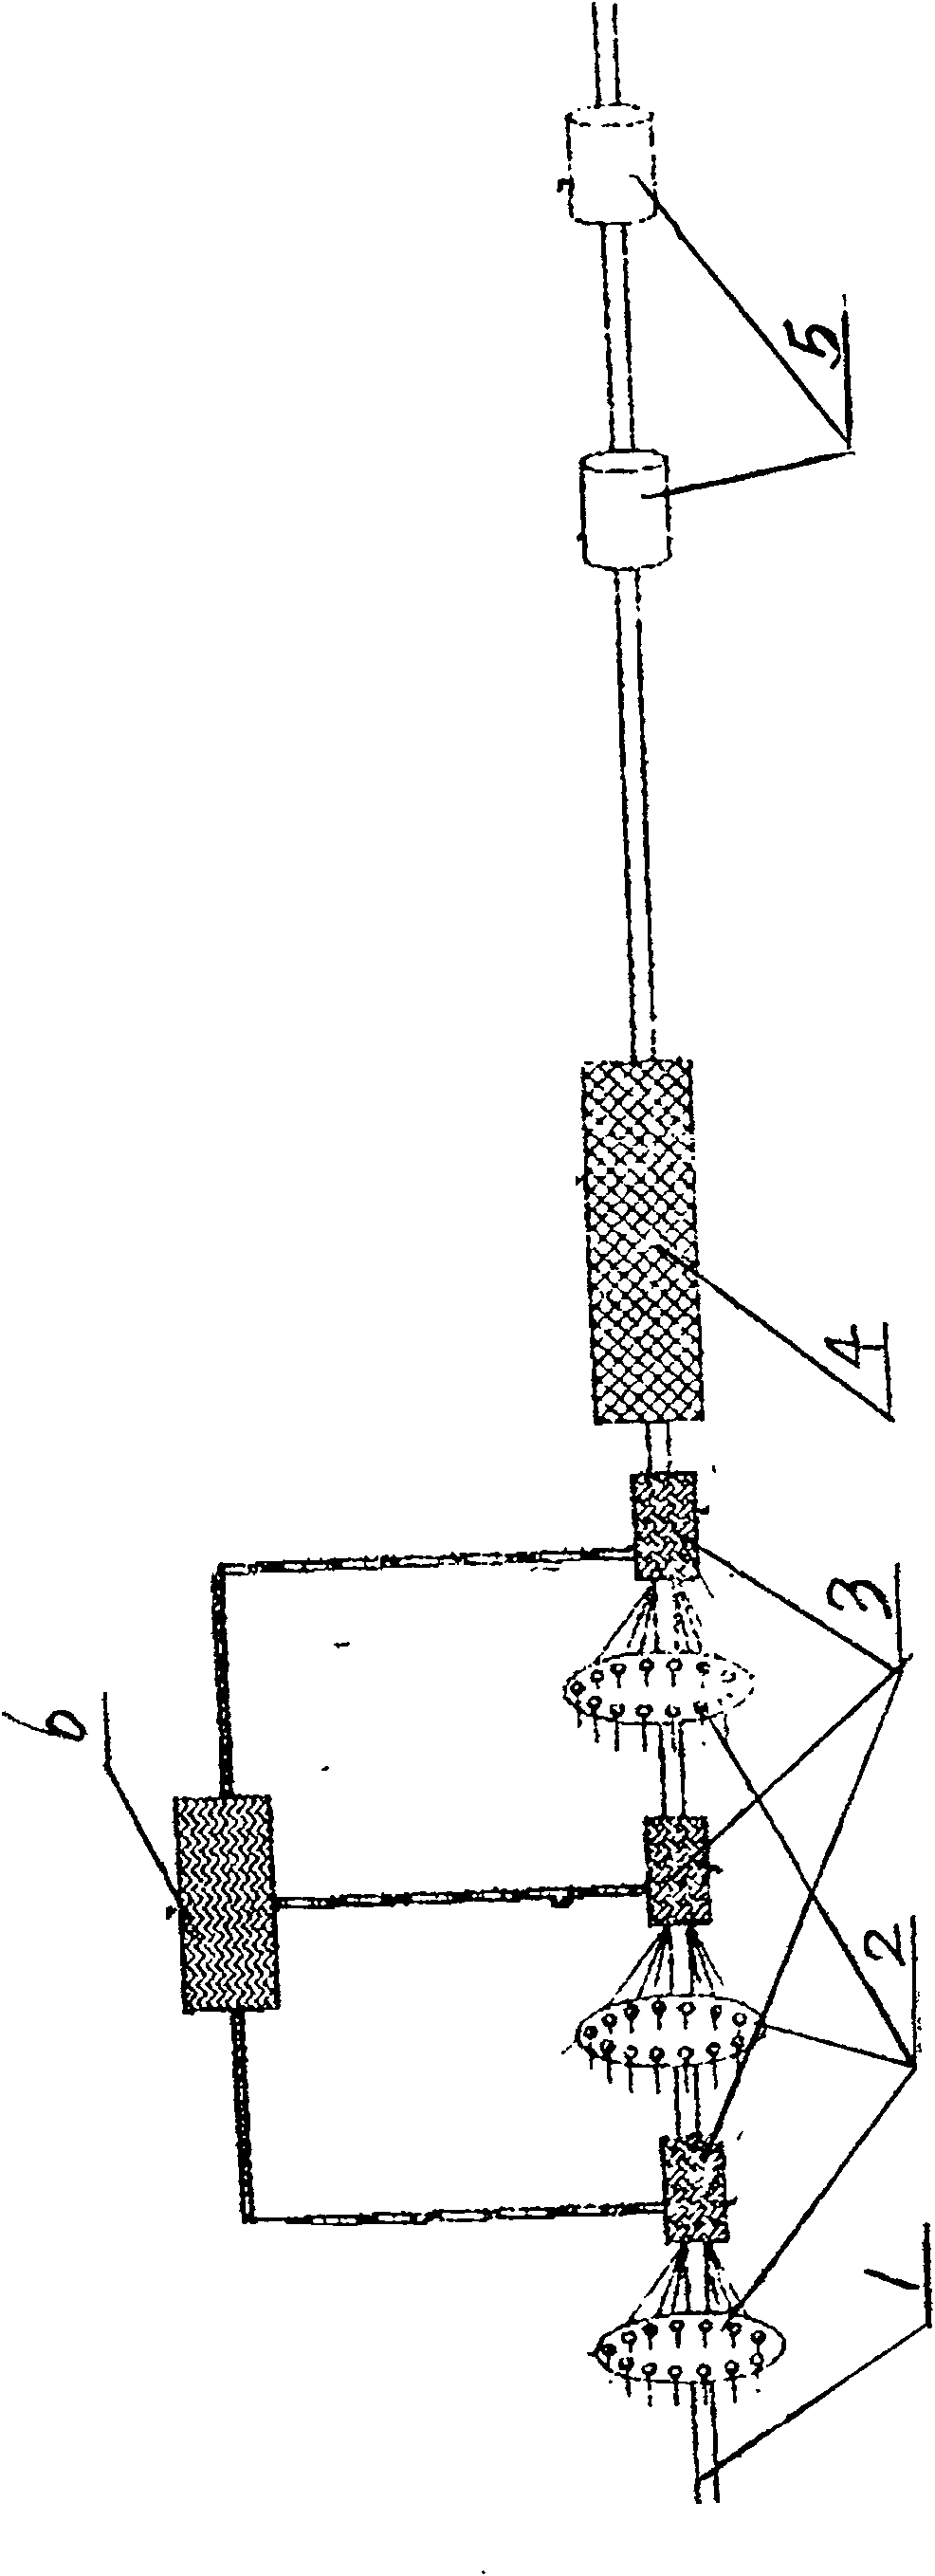
Figure 1
Abstract
Description
Technical field:
[0001] The invention relates to a method for preparing a glass steel pipe, in particular to a method for preparing a movable inner mandrel, a multilayer circular braid, and an online pultrusion multilayer circular braid structure and an online pultrusion glass steel pipe. Background technique:
[0002] At present, pultrusion is a widely used method for manufacturing FRP pipes. The method generally includes drawing multiple reinforcing fibers through a resin impregnation zone, and then pulling the impregnated fibers through a heated mold to solidify the resin and fibers. Together, the required glass steel pipe is formed. Since the pipe has only longitudinal unidirectional reinforcing fibers and only resin bonding force in the hoop direction, the bearing pressure is low. The pultrusion winding method is based on the pultrusion method. While pultruding, the longitudinal reinforcing fiber is hoop-wound, and then solidified by heating the mold. The glass steel pi...
Examples
Embodiment 1
[0023] Depend on figure 1 It can be seen that: the present invention adopts three computer-controlled two-dimensional horizontal braiding machines 1 to weave three-layer fiber annular braided layer composite glass steel pipes, and resin impregnation tanks 3 are arranged behind each braiding machine, and the third impregnation tank is arranged. Behind the groove is the pultrusion die 4; the core mold 1 is a uniform straight circular tube core mold with equal ends, the core mold is a mobile core mold that moves with the fiber annular braiding layer, and the core mold passes through the braiding machine and the dipping tank , the pultrusion die 4 moves with the horizontal movement of the drawn fiber by the drawing machine 5, by figure 1 It can also be seen that a storage tank 6 is installed above the dipping tank, and the storage tank communicates with the three dipping tanks through pipelines.
[0024] The operation process of the present invention is as follows: after the firs...