
Method for preparing hollow three-dimensional crimped polyphenylene sulfide staple fibers
A polyphenylene sulfide and three-dimensional crimping technology is applied in the preparation of hollow polyphenylene sulfide short fibers and the preparation of hollow three-dimensional crimped polyphenylene sulfide short fibers, and achieves the effects of superior performance, good operating performance and high hollow ratio.
Patent Information
- Authority / Receiving Office
- CN · China
- Current Assignee / Owner
- Publication Date
- 2011-08-24
- Estimated Expiration
- Not applicable · inactive patent
Smart Images
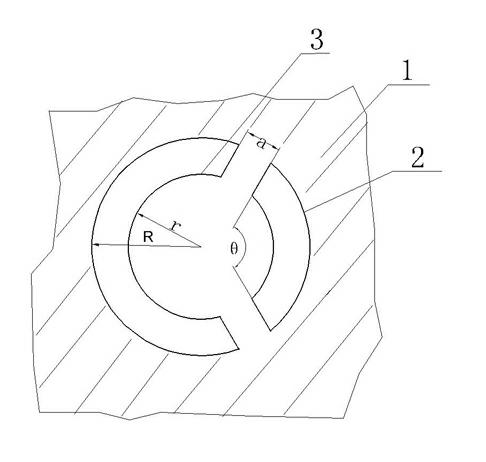
Figure 1 
Figure 2 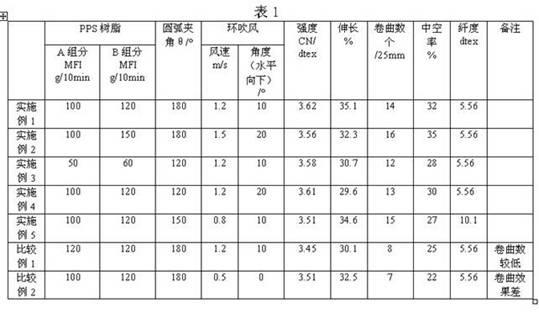
Figure 3
Abstract
Description
technical field
[0001] The invention relates to a method for preparing hollow polyphenylene sulfide short fibers, in particular to a method for preparing hollow three-dimensional crimped polyphenylene sulfide short fibers, and belongs to the technical field of high-performance fibers. Background technique
[0002] Polyphenylene sulfide (PPS) resin is a thermoplastic resin with phenylthio groups in the molecular main chain. PPS fiber made of PPS resin is a new type of high-performance fiber with excellent heat resistance, chemical resistance, Flame retardant properties and good mechanical properties, dimensional stability and textile processability. Therefore, PPS fiber has been widely used in industry and textile and garment fields.
[0003] The currently developed PPS fibers are mainly ordinary round short fibers. As disclosed in the publication number CN1603477, it is "a method for melt spinning and stretching heat setting of linear high molecular weight polyphenylene sul...
Examples
Embodiment 1
[0016] A method for preparing hollow three-dimensional crimped polyphenylene sulfide short fibers in this embodiment uses two components, wherein the first component uses linear polyphenylene sulfide with a melt index of 100g / 10min, and the second component uses Linear polyphenylene sulfide with a melt index of 120g / 10min; the two components are dried at 180°C for 8 hours and then passed through a twin-screw composite spinning device, and the temperature of each zone of the twin-screw composite spinning device is set at 280 ~320°C, after melting, it is sent into the spinning box by a metering pump, and melted and spun at a temperature of 325°C; figure 1 As shown, the spinneret hole of the spinneret 1 of the present invention is a ring formed by two concentric circles, and there are two gaps on the ring; the radius r of the inner ring 3 of the spinneret hole is 0.3mm, and the outer ring 2 The radius R is 0.8mm, and the notch spacing a is both 0.10mm, wherein the arc angle θ of ...
Embodiment 2
[0018] A method for preparing hollow three-dimensional crimped polyphenylene sulfide short fibers in this embodiment uses two components, wherein the first component uses linear polyphenylene sulfide with a melt index of 100g / 10min, and the second component uses Linear polyphenylene sulfide with a melt index of 150g / 10min; the two components are dried at 180°C for 8 hours and then passed through a twin-screw composite spinning device, and the temperature of each zone of the twin-screw composite spinning device is set at 280 ~320°C, after melting, it is sent into the spinning box by a metering pump, and melted and spun at a temperature of 325°C; figure 1 As shown, the spinneret hole of the spinneret 1 of the present invention is a ring formed by two concentric circles, and there are two gaps on the ring; the radius r of the inner ring 3 of the spinneret hole is 0.3mm, and the outer ring 2 The radius R is 0.8mm, and the notch spacing a is both 0.10mm, wherein the arc angle θ of ...
Embodiment 3
[0020] The preparation method of a hollow three-dimensional crimped polyphenylene sulfide short fiber in this embodiment adopts two kinds of components, wherein the first component adopts linear polyphenylene sulfide with a melt index of 50 g / 10min, and the second component adopts Linear polyphenylene sulfide with a melt index of 60g / 10min; the two components are dried at 180°C for 8 hours and then passed through a twin-screw composite spinning device, and the temperature of each zone of the twin-screw composite spinning device is set at 280 ~320°C, after melting, it is sent into the spinning box by a metering pump, and melted and spun at a temperature of 325°C; figure 1 As shown, the spinneret hole of the spinneret 1 of the present invention is a ring formed by two concentric circles, and there are two gaps on the ring; the radius r of the inner ring 3 of the spinneret hole is 0.3mm, and the outer ring 2 The radius R is 0.8mm, and the notch distance a is both 0.10mm, wherein ...