
Welding process of large-diameter annular part
A welding process and annular part technology, applied in the field of welding process of large-diameter annular parts, can solve the problems of reducing the production efficiency of parts, increasing the processing cost of parts, affecting the quality of products, etc. The effect of clamping
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Applications(China)
- Current Assignee / Owner
- Publication Date
- 2014-12-10
Smart Images
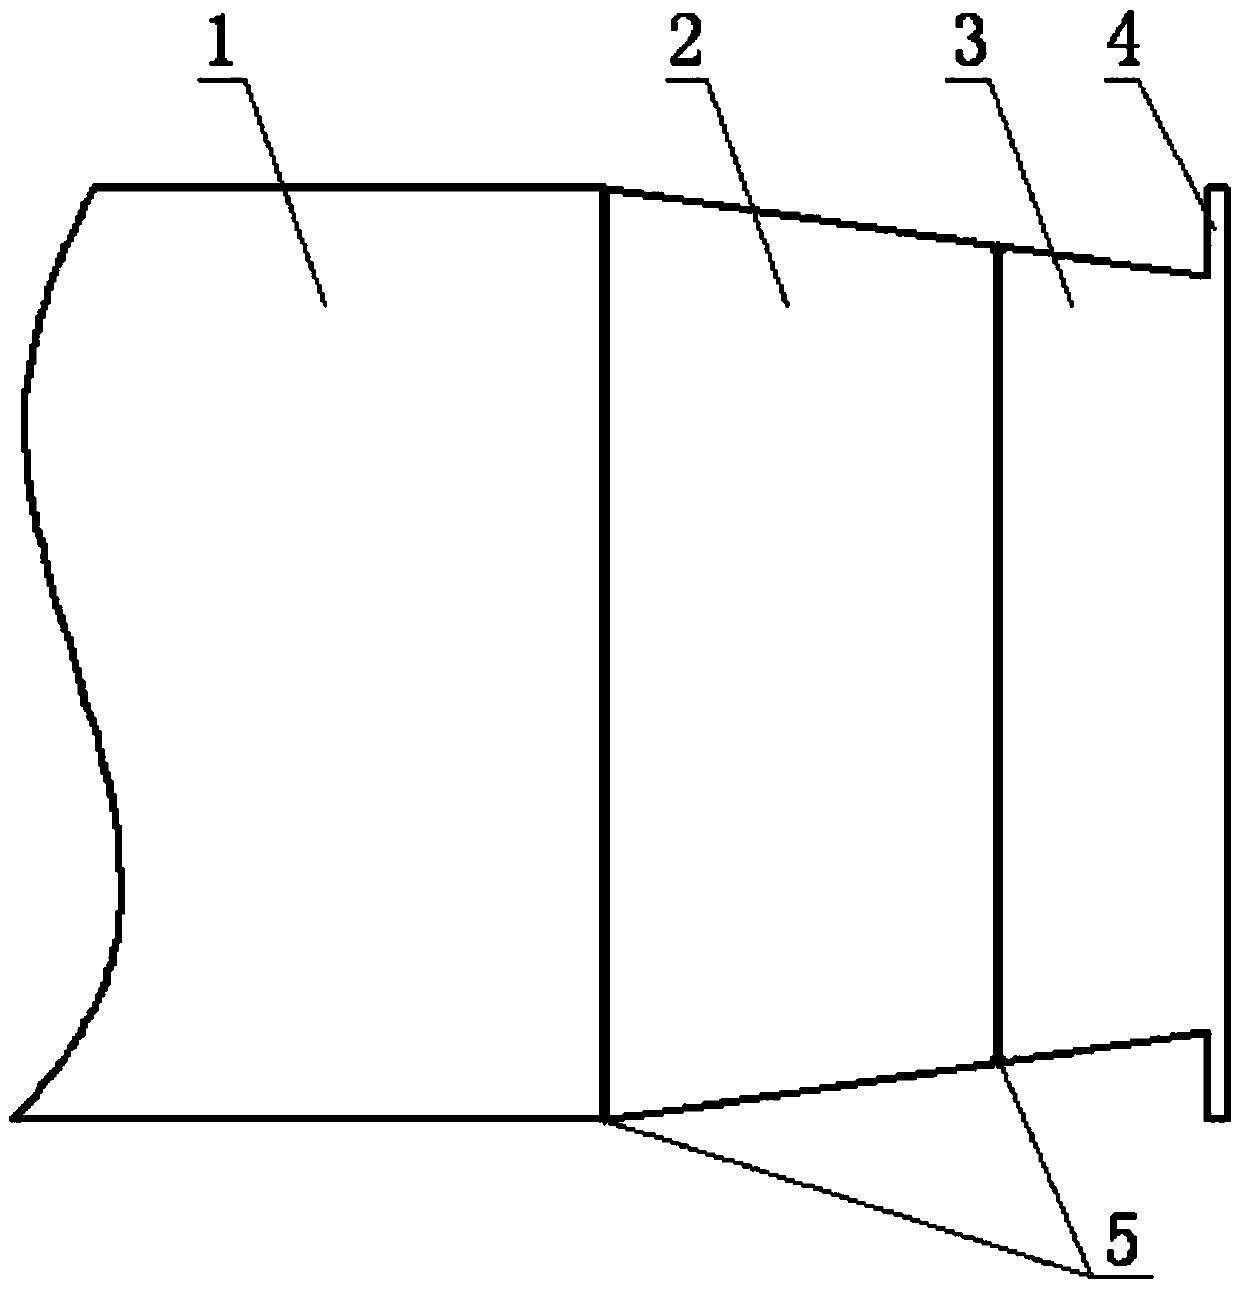
Figure 1
Abstract
Description
Technical field
[0001] The invention belongs to the technical field of welding processing, and relates to a welding process of a large-diameter annular part. Background technique
[0002] Welding is a processing technology and a connection method in which two workpieces are bonded together by heating, pressing, or both. In the field of welding, metal welding is very common. The quality of the welding process is directly related to the quality of the welding and affects the product qualification rate. Especially for the welding of large-diameter ring-shaped parts, for example, when three large-diameter ring-shaped parts are welded by vacuum electron beam, the butt joints of the parts are easily cracked on both sides due to the tensile stress on both sides, resulting in gaps at the joints. Too large can not be welded, in order to prevent the gap of the weld from being too large, the welding fixture is usually used to compress the welding. The specific method steps are as follows...
Examples
Embodiment Construction
[0023] The technical solutions of the present invention are further described below in conjunction with the accompanying drawings of the embodiments, but the scope of protection is not limited to the above.
[0024] Such as figure 1 As shown, part A1, part B2, and part C3 are large-diameter annular components, in which part C3 has a flange 4, and parts A1, part B2, and part C3 are welded together by the welding process of the present invention. The specific process steps are as follows:
[0025] (1) Cleaning before welding: Before welding, clean the welding grooves of part A1, part B2 and part C3 to remove the oxide scale, rust or oil around the annular weld, and ensure that there is no impurities around the groove of the weldment;
[0026] (2) Preliminary spot welding positioning and connecting parts: using manual argon arc welding with filler positioning spot welding to perform preliminary positioning and connection of the parts to be welded; due to the use of filler argon arc wel...