
Turning tooling and method for large thin-walled conical aluminum alloy parts
An aluminum alloy and cone technology, applied in metal processing equipment, metal processing mechanical parts, manufacturing tools, etc., can solve the problems of difficult to control wall thickness, inconsistent cutting depth, affecting processing efficiency, etc., to reduce processing costs and ensure processing. Quality, the effect of improving processing efficiency
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Patents(China)
- Current Assignee / Owner
- Publication Date
- 2020-11-20
Smart Images
Figure 1 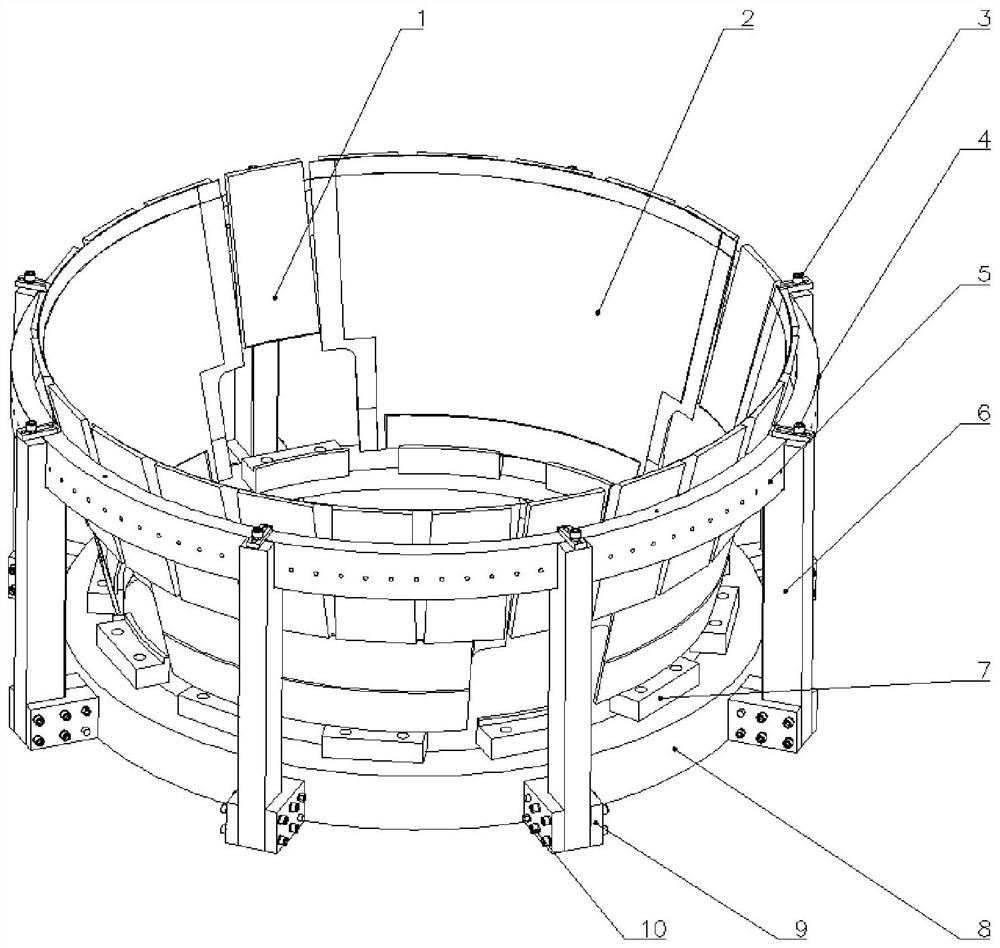
Figure 2 
Figure 3
Abstract
Description
technical field
[0001] The invention relates to a tooling and method for turning large-scale thin-walled conical aluminum alloy parts, belonging to the field of processing large-scale thin-walled conical aluminum alloy forgings, and in particular to a turning method for large-scale thin-walled conical aluminum alloy parts. The inner diameter of the aluminum alloy part is 1500-4000mm, and the thin wall means that the thickness-to-diameter ratio is 0.01-0.001. Background technique
[0002] The wall thickness of common large thin-walled aluminum alloy parts is only 0.5% to 0.3% of the diameter, and its own rigidity is poor. It is easy to vibrate under the action of cutting force during the overall turning process. At the same time, the release of cutting stress causes the parts to deform. Inconsistent depth of cut for each cut. Under the influence of this dual effect, the overall roundness of the part becomes poor, and the wall thickness is difficult to control, which is not c...
Examples
Embodiment
[0048] The supporting plate 1 described in the embodiment of the present invention is closely attached to the outer surface of the thin-walled conical aluminum alloy forging 2; Wall pre-drilled fixing holes for bolt support.
[0049] The invention provides a turning processing method of a large thin-walled conical aluminum alloy part. A new processing method is adopted to meet the thin-walled aluminum alloy forgings of different sizes, control the deformation of the parts during the processing, and ensure the consistency of the final processing wall thickness.
[0050] In order to achieve the above-mentioned purpose of the invention, the technical solution adopted by the present invention to solve the technical problem is to provide a turning method for large-scale thin-walled conical aluminum alloy parts, including:
[0051] Step 1. According to the size of the small end of the part, turn the reference bottom surface and the arc surface of the limit step on the surface of th...