
New technology of valve sealing element vacuum induction pile-up welding hard alloy and improved equipment
A vacuum induction, valve sealing technology, applied in metal processing equipment, welding equipment, metal processing and other directions, to achieve the effect of reducing maintenance time, convenient maintenance and operation, and saving consumption
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Patents(China)
- Current Assignee / Owner
- Publication Date
- 2010-08-18
- Estimated Expiration
- Not applicable · inactive patent
Smart Images
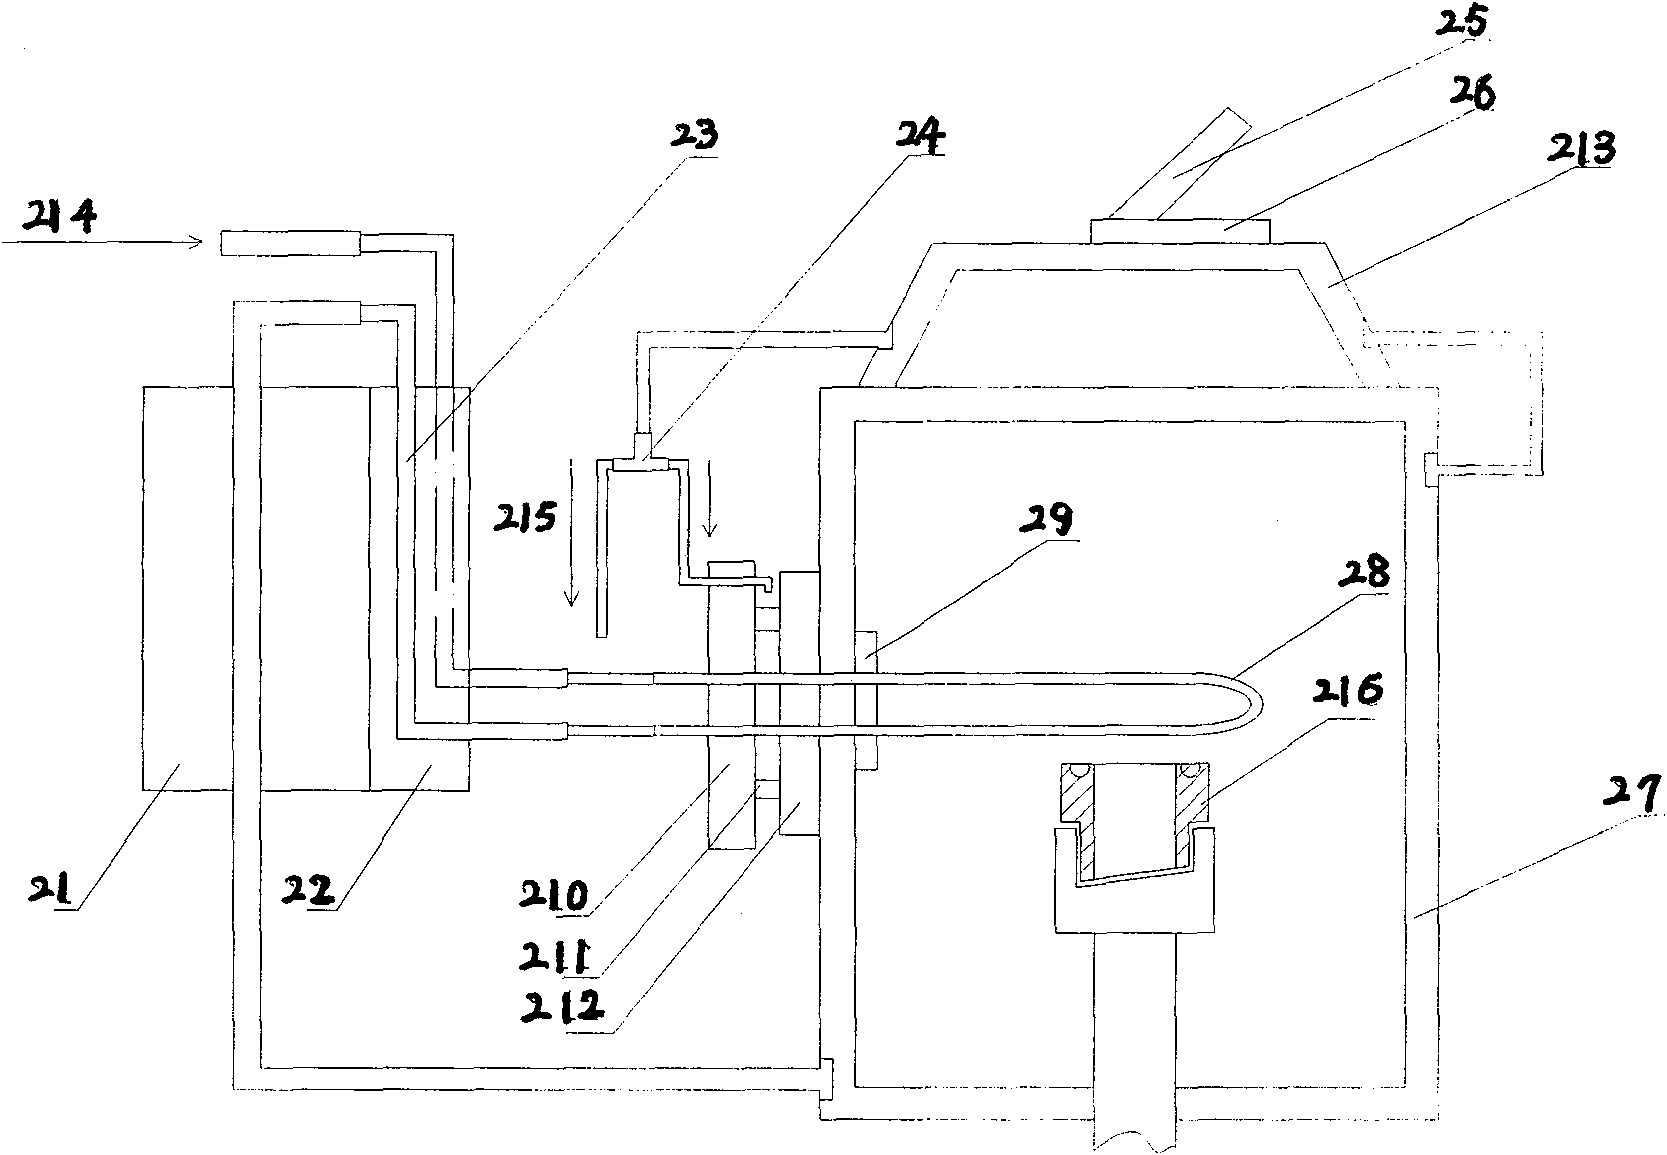
Figure 1 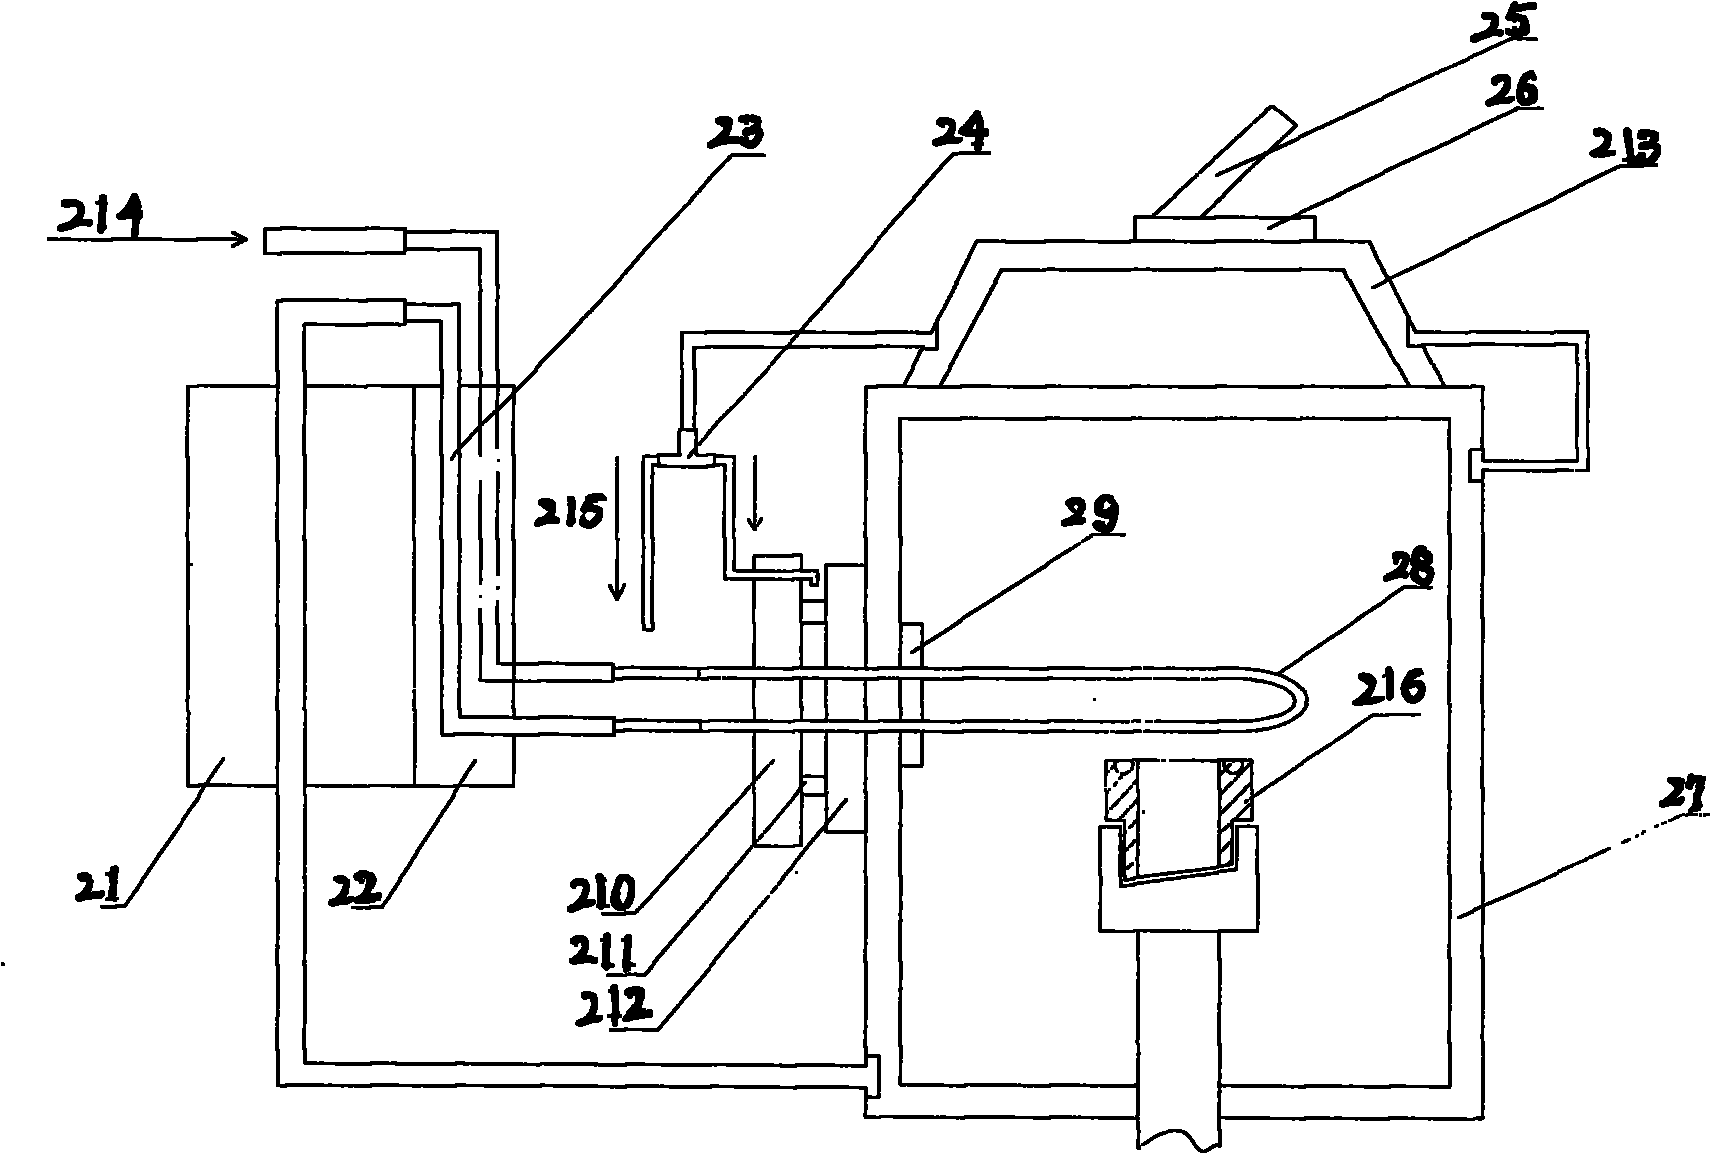
Figure 2 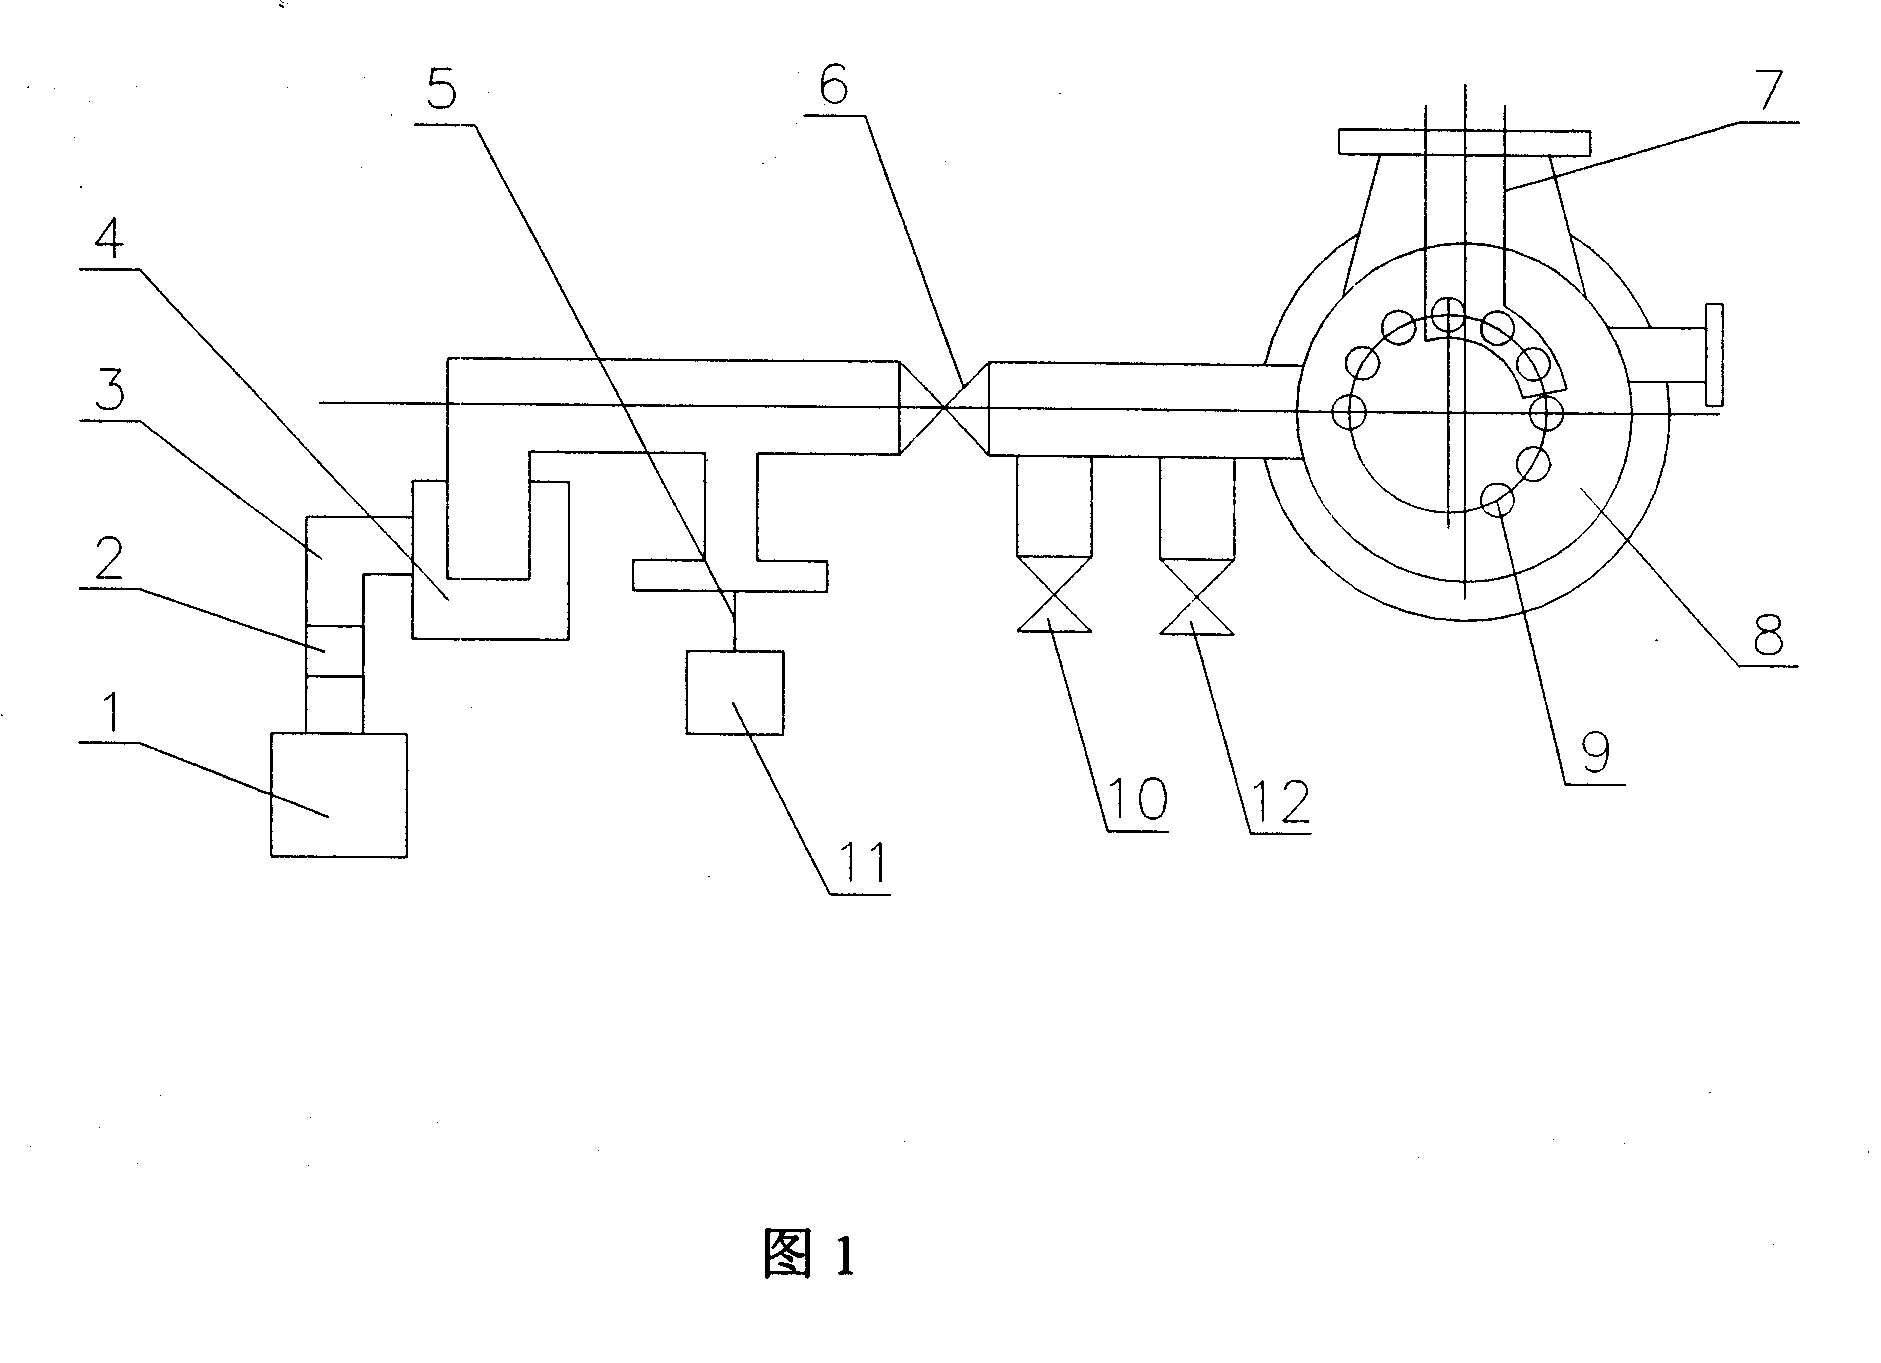
Figure 3
Abstract
Description
Technical field
[0001] The invention relates to a vacuum induction surfacing process and equipment, more specifically to a new process and improved equipment for vacuum induction surfacing of hard alloys of valve seals. Background technique
[0002] At the end of the last century, manual surfacing methods were generally used for valve sealing surfaces: flame, plasma or non-melting argon arc welding surfacing CoCrW hard alloy to improve the valve's corrosion resistance, wear resistance, heat resistance and surface size formability. However, the above-mentioned surfacing method has relatively high operating difficulties, high labor intensity, high material consumption, and large splashes of smoke (dust) during welding, which not only pollutes the environment but also easily causes damage to the operator’s body. At the same time, the workpiece is oxidized seriously, so Large machining allowances result in time-consuming and labor-intensive mechanical processing; moreover, the surfac...
Examples
Embodiment 1
[0017] An improved vacuum high-frequency induction surfacing equipment is connected to the GP60 high-frequency machine, and an example of the process of surfacing a valve seat of 3 / 4" (nominal passage 20mm).
[0018] The seat material is 1Cr13. Its main chemical components (mass fraction, %) are 0.10C, 1.00Mn, 1.00Si, 0.035P, 0.030S, 11.7Cr. The depth of the U-shaped groove on the pre-surfacing sealing surface is 2.0mm~2.2mm, and the wall thickness of the U-shaped groove is 0.8mm~1.0mm. The amount of surfacing welding is 15 per furnace each time. Choose 200 mesh (0.126mm) Stellite158D powder as surfacing flux, its chemical composition (mass fraction, %) is 0.50C, 22.7Cr, 2.4Fe, 0.01Mn, 0.01Mo, 2.2Ni, 1.7Si, 4.6W, Yu Co. Use 3 / 4” molds to be hand wiped and pressed, dried and then high-frequency sintered surfacing. The vacuum degree during surfacing is 10 -1 Pa~10 -2 pa, grid current 3.51A, anode current 1.6A, anode voltage 11KV, tank circuit voltage 5.5KV, surfacing temperature...
Embodiment 2
[0020] An improved vacuum high-frequency induction surfacing equipment is connected to the GP60 high-frequency machine, and an example of the process of surfacing a valve seat with a full diameter of 2" (outer diameter ¢58mm).
[0021] The valve seat material is 1Cr13, and its main chemical composition (mass fraction, %) is 0.10C, 1.00Mn, 1.00Si, 0.035P, 0.030S, 11.7Cr. The depth of the U-shaped groove of the pre-surfacing sealing surface is 2.0mm~2.1mm, the wall thickness of the U-shaped groove is 1.0mm~1.10mm, and the amount of surfacing welding is 6 per furnace. Choose 200 mesh (0.126mm) Co-L powder as the surfacing flux, and its chemical composition (mass fraction, %) of the surfacing flux is 0.70C, 0.95Si, 0.61B, 29.50Cr, 4.00W, 2.69Fe, residual Co. It adopts full-diameter 2" molds to be formed by hand rubbing, drying and then performing high-frequency sintering surfacing. The vacuum degree during surfacing is 10 -1 Pa~10 -2 pa. The grid current is 0.57A, the anode current ...
Embodiment 3
[0023] An improved vacuum high-frequency induction surfacing equipment is connected to the GP60 high-frequency machine, and a 11 / 4" (nominal passage 32mm) valve seat process example is surfacing.
[0024] The seat material is 1Cr13. Its main chemical components (mass fraction, %) are 0.10C, 1.00Mn, 1.00Si, 0.035P, 0.030S, 11.7Cr. The depth of the U-shaped groove on the pre-surfacing sealing surface is 2.0mm~2.2mm, and the wall thickness of the U-shaped groove is 0.9mm~1.10mm. The amount of surfacing welding per furnace is 12 each time. Choose 200 mesh (0.126mm) Stellite158D powder as surfacing flux, its chemical composition (mass fraction, %) is 0.50C, 22.7Cr, 2.4Fe, 0.01Mn, 0.01Mo, 2.2Ni, 1.7Si, 4.6W, Yu Co. Use 1 1 / 4" molds to be pressed and formed by hand, drying and then performing high-frequency sintering surfacing. The vacuum degree during surfacing is 10 -1 Pa~10 -2 pa, grid current 0.54A, anode current 1.7A, anode voltage 11.2KV, tank circuit voltage 6.2KV, surfacing t...