
Method for reducing fiber hairiness of polytetrafluoroethylene membrane cracks
A technology of polytetrafluoroethylene film and fiber, which is applied in the direction of suction liquid/gas/vapour removal, textile and papermaking, fabric surface trimming, etc. Problems such as large pores
Patent Information
- Authority / Receiving Office
- CN · China
- Patent Type
- Patents(China)
- Current Assignee / Owner
- Publication Date
- 2017-09-15
Smart Images
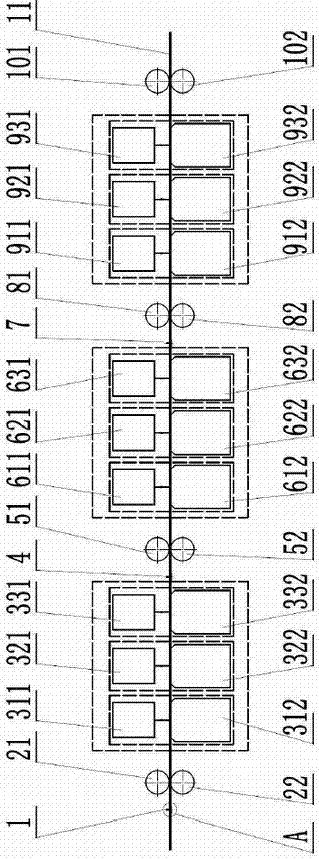
Figure 1 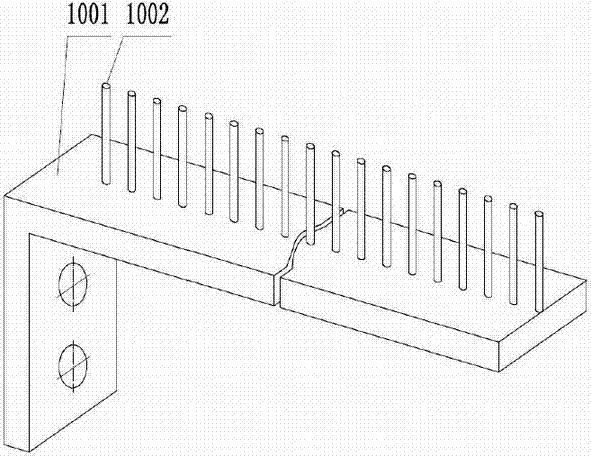
Figure 2 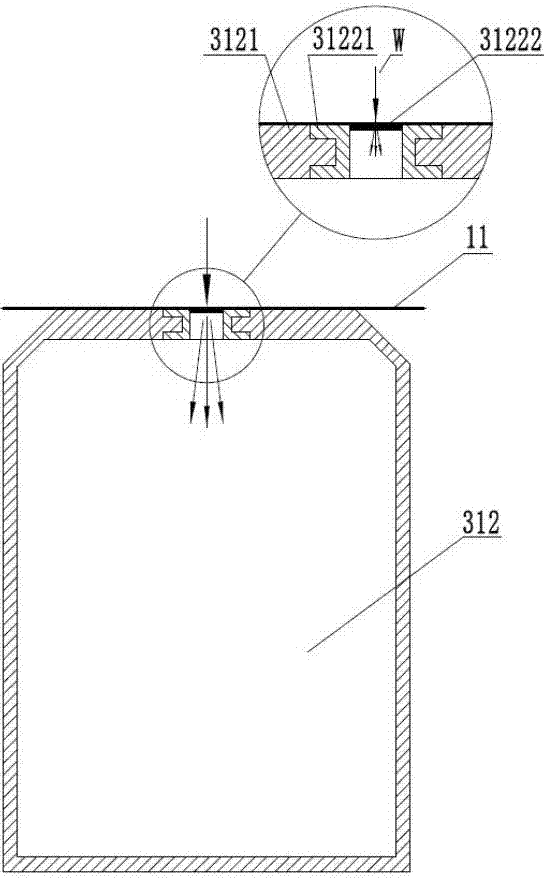
Figure 3
Abstract
Description
technical field
[0001] The invention relates to a method for manufacturing polytetrafluoroethylene split fibers, in particular to a method for reducing hairiness of polytetrafluoroethylene split fibers. The polytetrafluoroethylene membrane crack fiber prepared by this method has less hairiness, and when used to prepare filter material, its carding speed is high, and the net is uniform, and the pore of the prepared filter material is small, and the pore uniformity is high, so it can be widely used. High temperature resistant filter material for high dust removal efficiency. Background technique
[0002] PTFE has excellent physical and chemical properties, outstanding high and low temperature resistance, excellent chemical corrosion resistance, insoluble in any other chemical solvents except for its own fluoride and molten alkali metal; oxidation resistance it is good. In addition, PTFE has outstanding surface non-stick properties, especially when it is used as a high-temper...
Examples
Embodiment 1
[0071] The polytetrafluoroethylene film-split fiber tow with a linear density of 2000 denier and a number of hairiness per unit length of 48 produced by the conventional film-split method is used as the primary tow, and then 50 of them are flattened into a layer with a width of 250 mm. 1. The tow layer with a thickness of 1.5 mm is regularly arranged after being combed by the comb needles 1002 of the first comb part 1, and fed into the first horizontal layer with three spunlace head parts through the first pair of rubber feeding roller parts. Type spunlace unit performs the first horizontal spunlace impact dehairing, and its process parameters are: the surface linear speed of the first upper rubber feed roller and the first lower rubber feed roller are both 10 m / min, and the spunlace head The distance between the parts and the top of the dehydration box is 30 mm, the water pressure of the water thorn head parts is 20 MPa, the diameter of the water jets injected from top to bott...
Embodiment 2
[0073] The polytetrafluoroethylene membrane split fiber tow that is 2200 and the number of hairs per unit length is 46 as the primary tow is the linear density obtained by the conventional membrane split method, and then its 40 bundles are tiled into a layer with a width of 200 mm. The tow layer with a thickness of 1.5 mm is regularly arranged after being combed by the comb needles 1002 of the first comb part 1, and then fed into the first horizontal type with three hydroentanglement head parts through the first pair of rubber feeding roller parts. The spunlace unit performs the first horizontal spunlace impact dehairing, and its process parameters are: the surface linear speed of the first upper rubber feed roller and the first lower rubber feed roller are both 6.5 m / min, the spunlace head The distance between the parts and the top of the dehydration box is 20 mm, the water pressure of the water thorn head part is 17 MPa, the diameter of the water jets injected from top to bot...
Embodiment 3
[0075]The polytetrafluoroethylene film-split fiber tow with a linear density of 2400 denier and a number of hairiness per unit length of 45 produced by the conventional film-split method is used as the primary tow, and then 30 bundles are flattened into a layer with a width of 150 mm. 1. The tow layer with a thickness of 1.5 mm is regularly arranged after being combed by the comb needles 1002 of the first comb part 1, and fed into the first horizontal layer with three spunlace head parts through the first pair of rubber feeding roller parts. Type spunlace unit performs the first horizontal spunlace impact dehairing, and its process parameters are: the surface linear speed of the first upper rubber feed roller and the first lower rubber feed roller are both 3 m / min, the spunlace head The distance between the part and the top of the dehydration box is 10 mm, the water pressure of the water thorn head part is 15 MPa, the diameter of the water jet injected from top to bottom is 0.1...